Build Your Own 2x72 Belt Grinder
by Dankozi713 in Workshop > Metalworking
148 Views, 1 Favorites, 0 Comments
Build Your Own 2x72 Belt Grinder

.jpeg)


I currently have a 1x42-inch belt sander that I have been using for a few years now and it is great. I found it online and purchased it from a very nice old maker who was ready for retirement. $20 and several practice blades later, I found myself wanting more power, More Power! Sorry, I get too excited.
With my smart phone being a mind reader, the algorithm started feeding me tons of videos of folks doing exactly this; taking an old throw away treadmill & other scrap metal and making their own 2x72-inch belt grinder. Now it is my turn.
Supplies

Old Treadmill
Optional: old workout bench
Scrap metal
Angle Grinder (with various attachments)
Welder (I used Flux Core)
Clamps
Safety gear
Marking devices
Measuring devices
Hacksaw
Screws, nuts, bolts, washers
Some contact wheels (I started with skateboard wheels)
Optional: HDPE to recycle (in which case you'd need a saw or lathe)
Files
Drill with bits
Tap & die set
Cutting oil
Wrenches
Snips
Paint
2x72-inch sanding belts (I bought 36, 60, and 120 grit ceramic belts)
The Concept
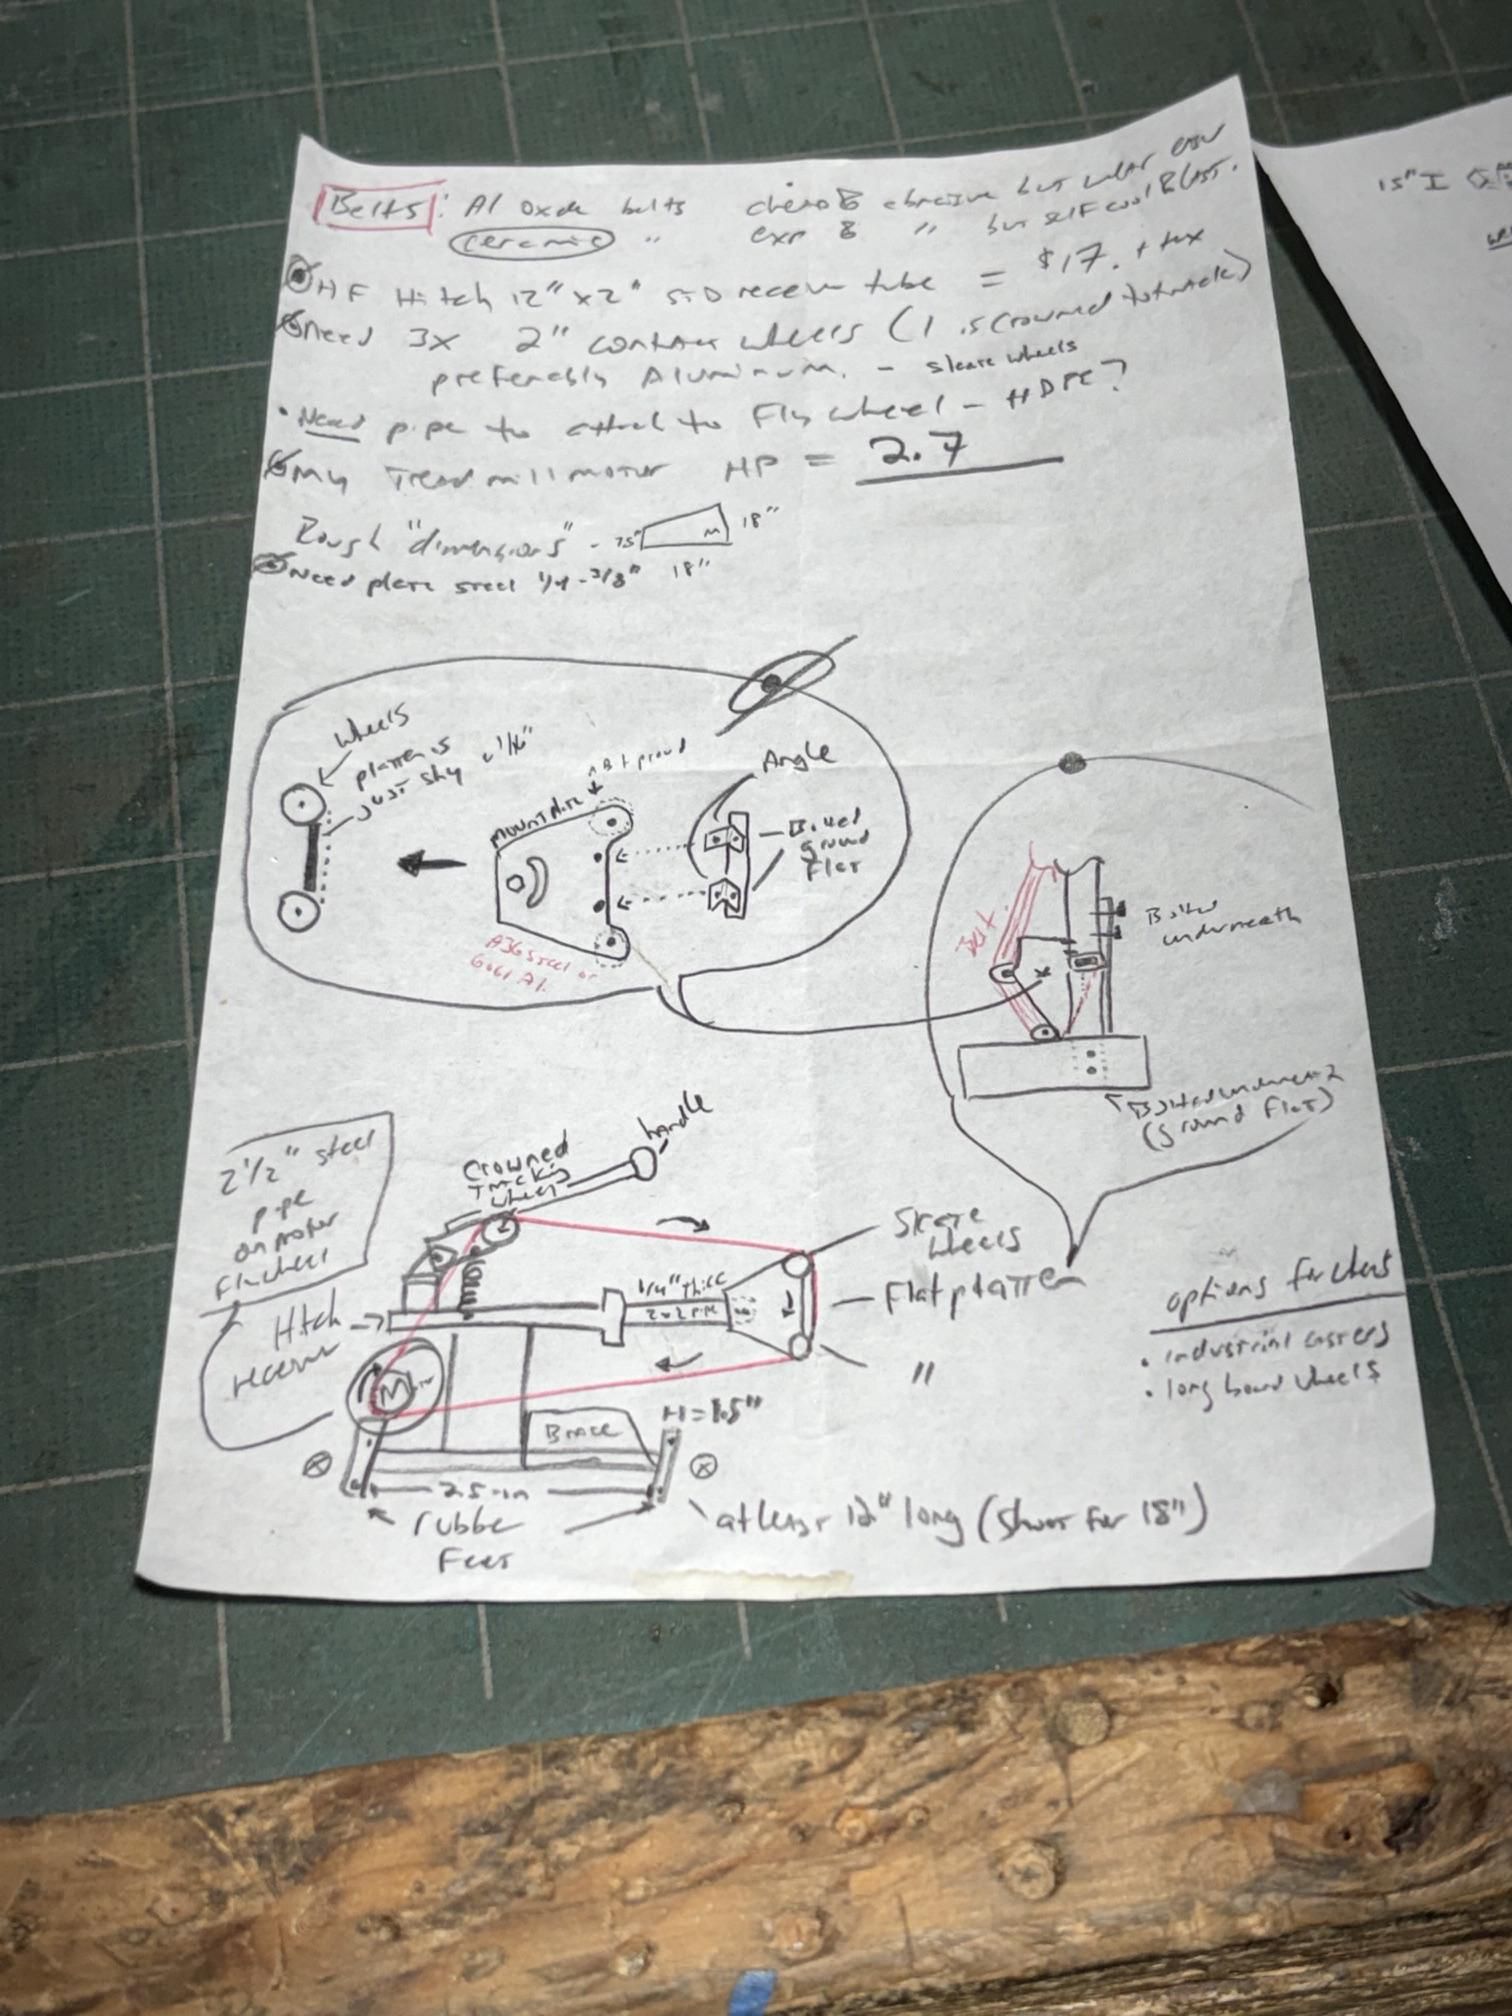
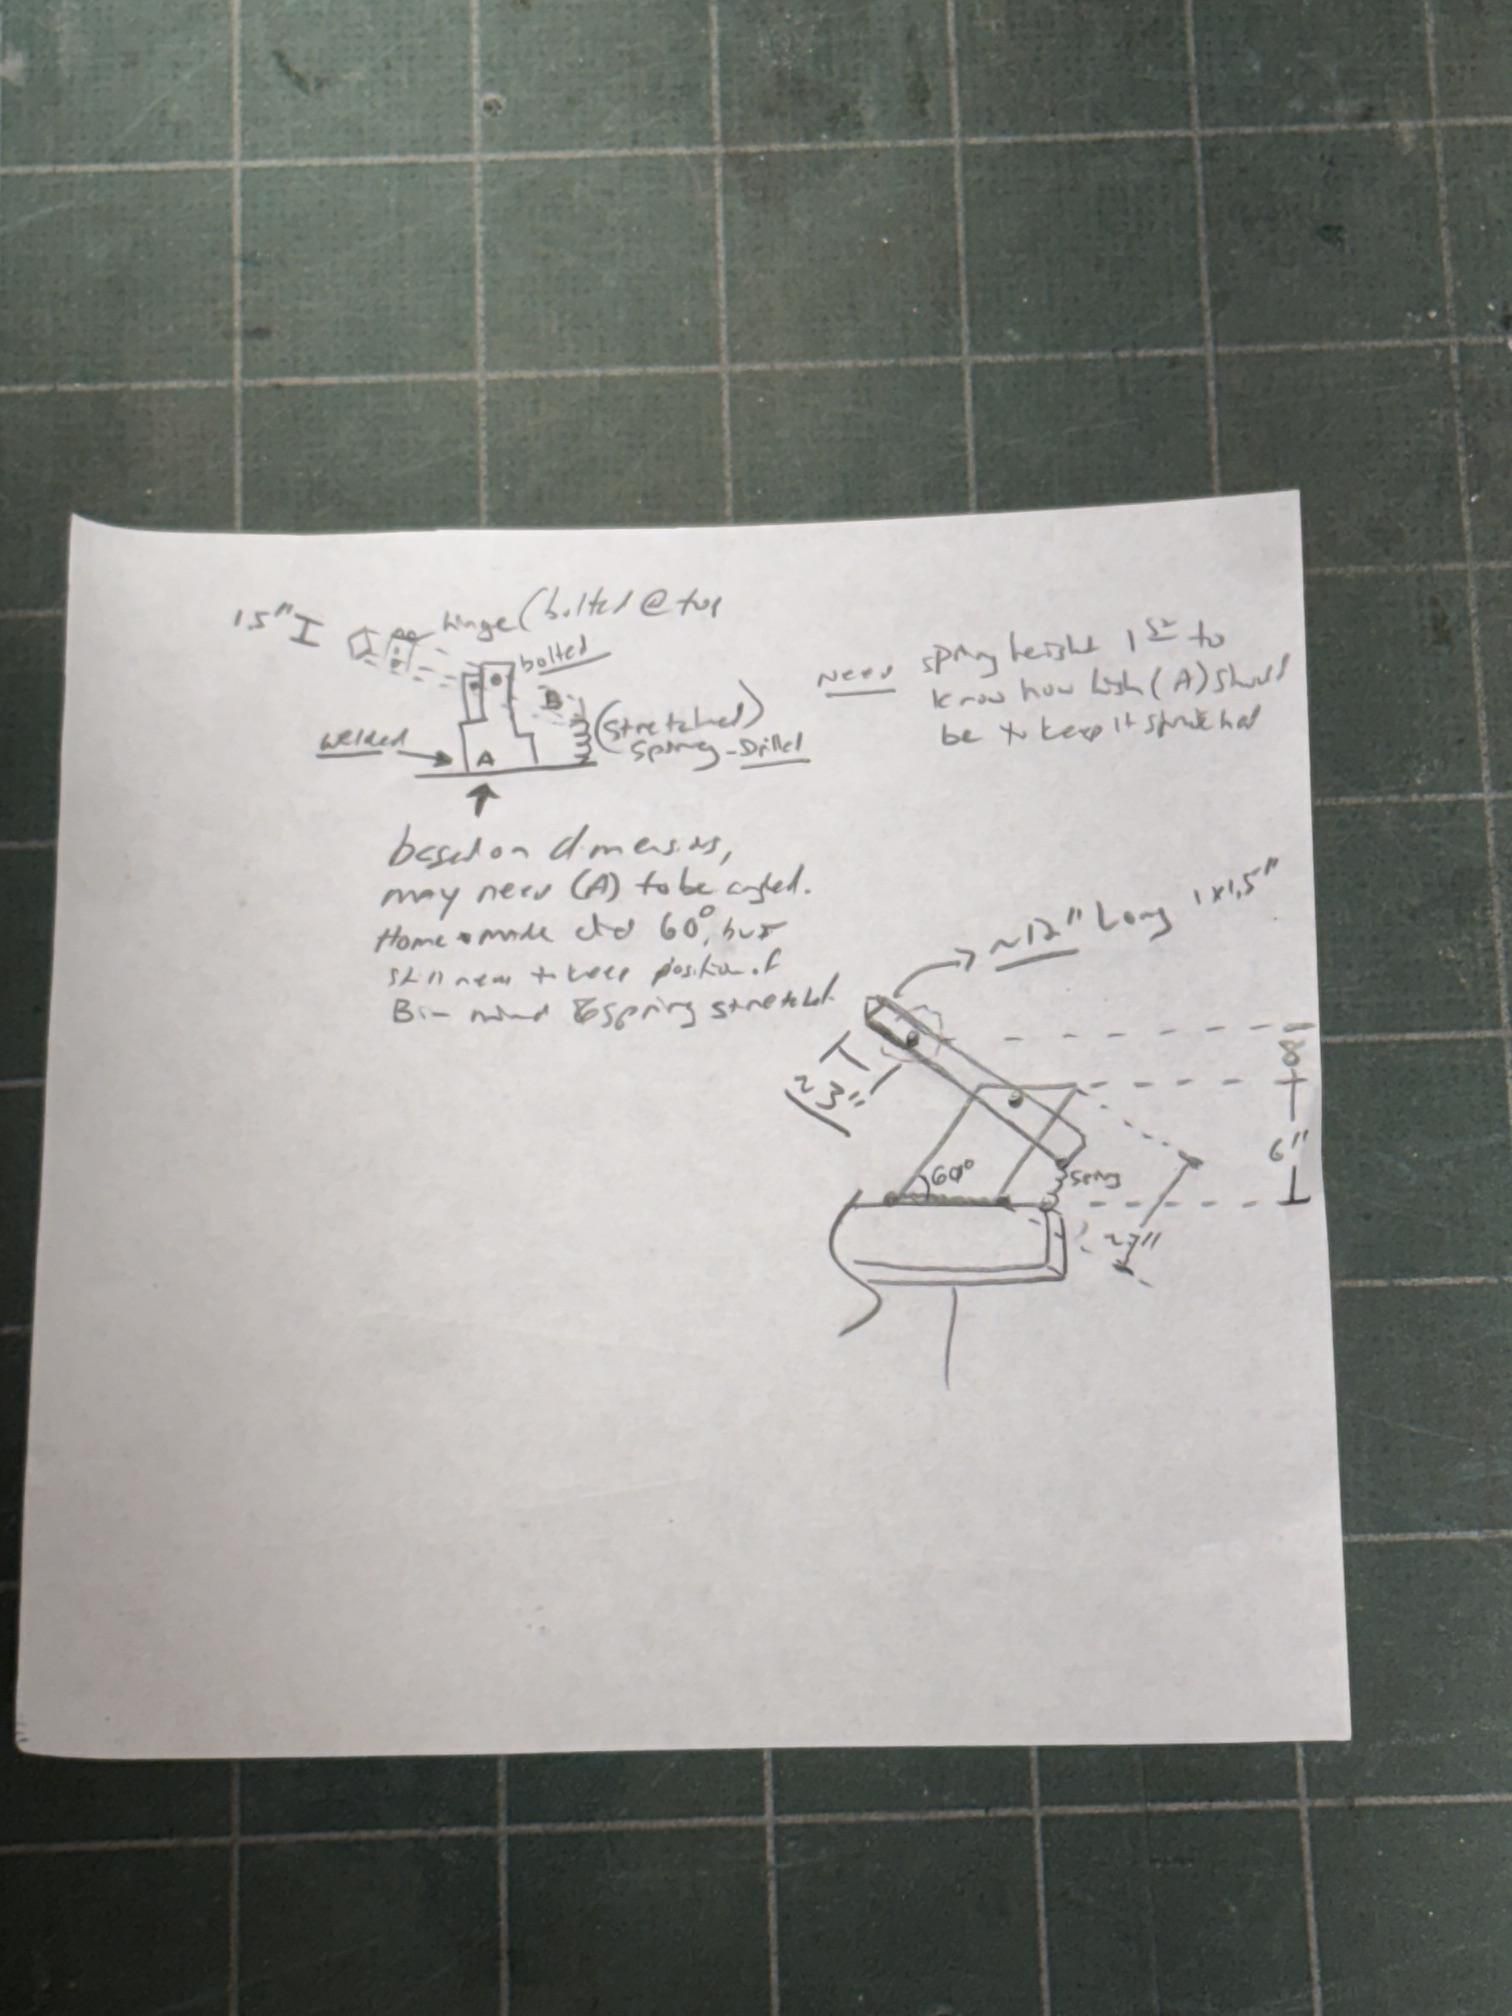
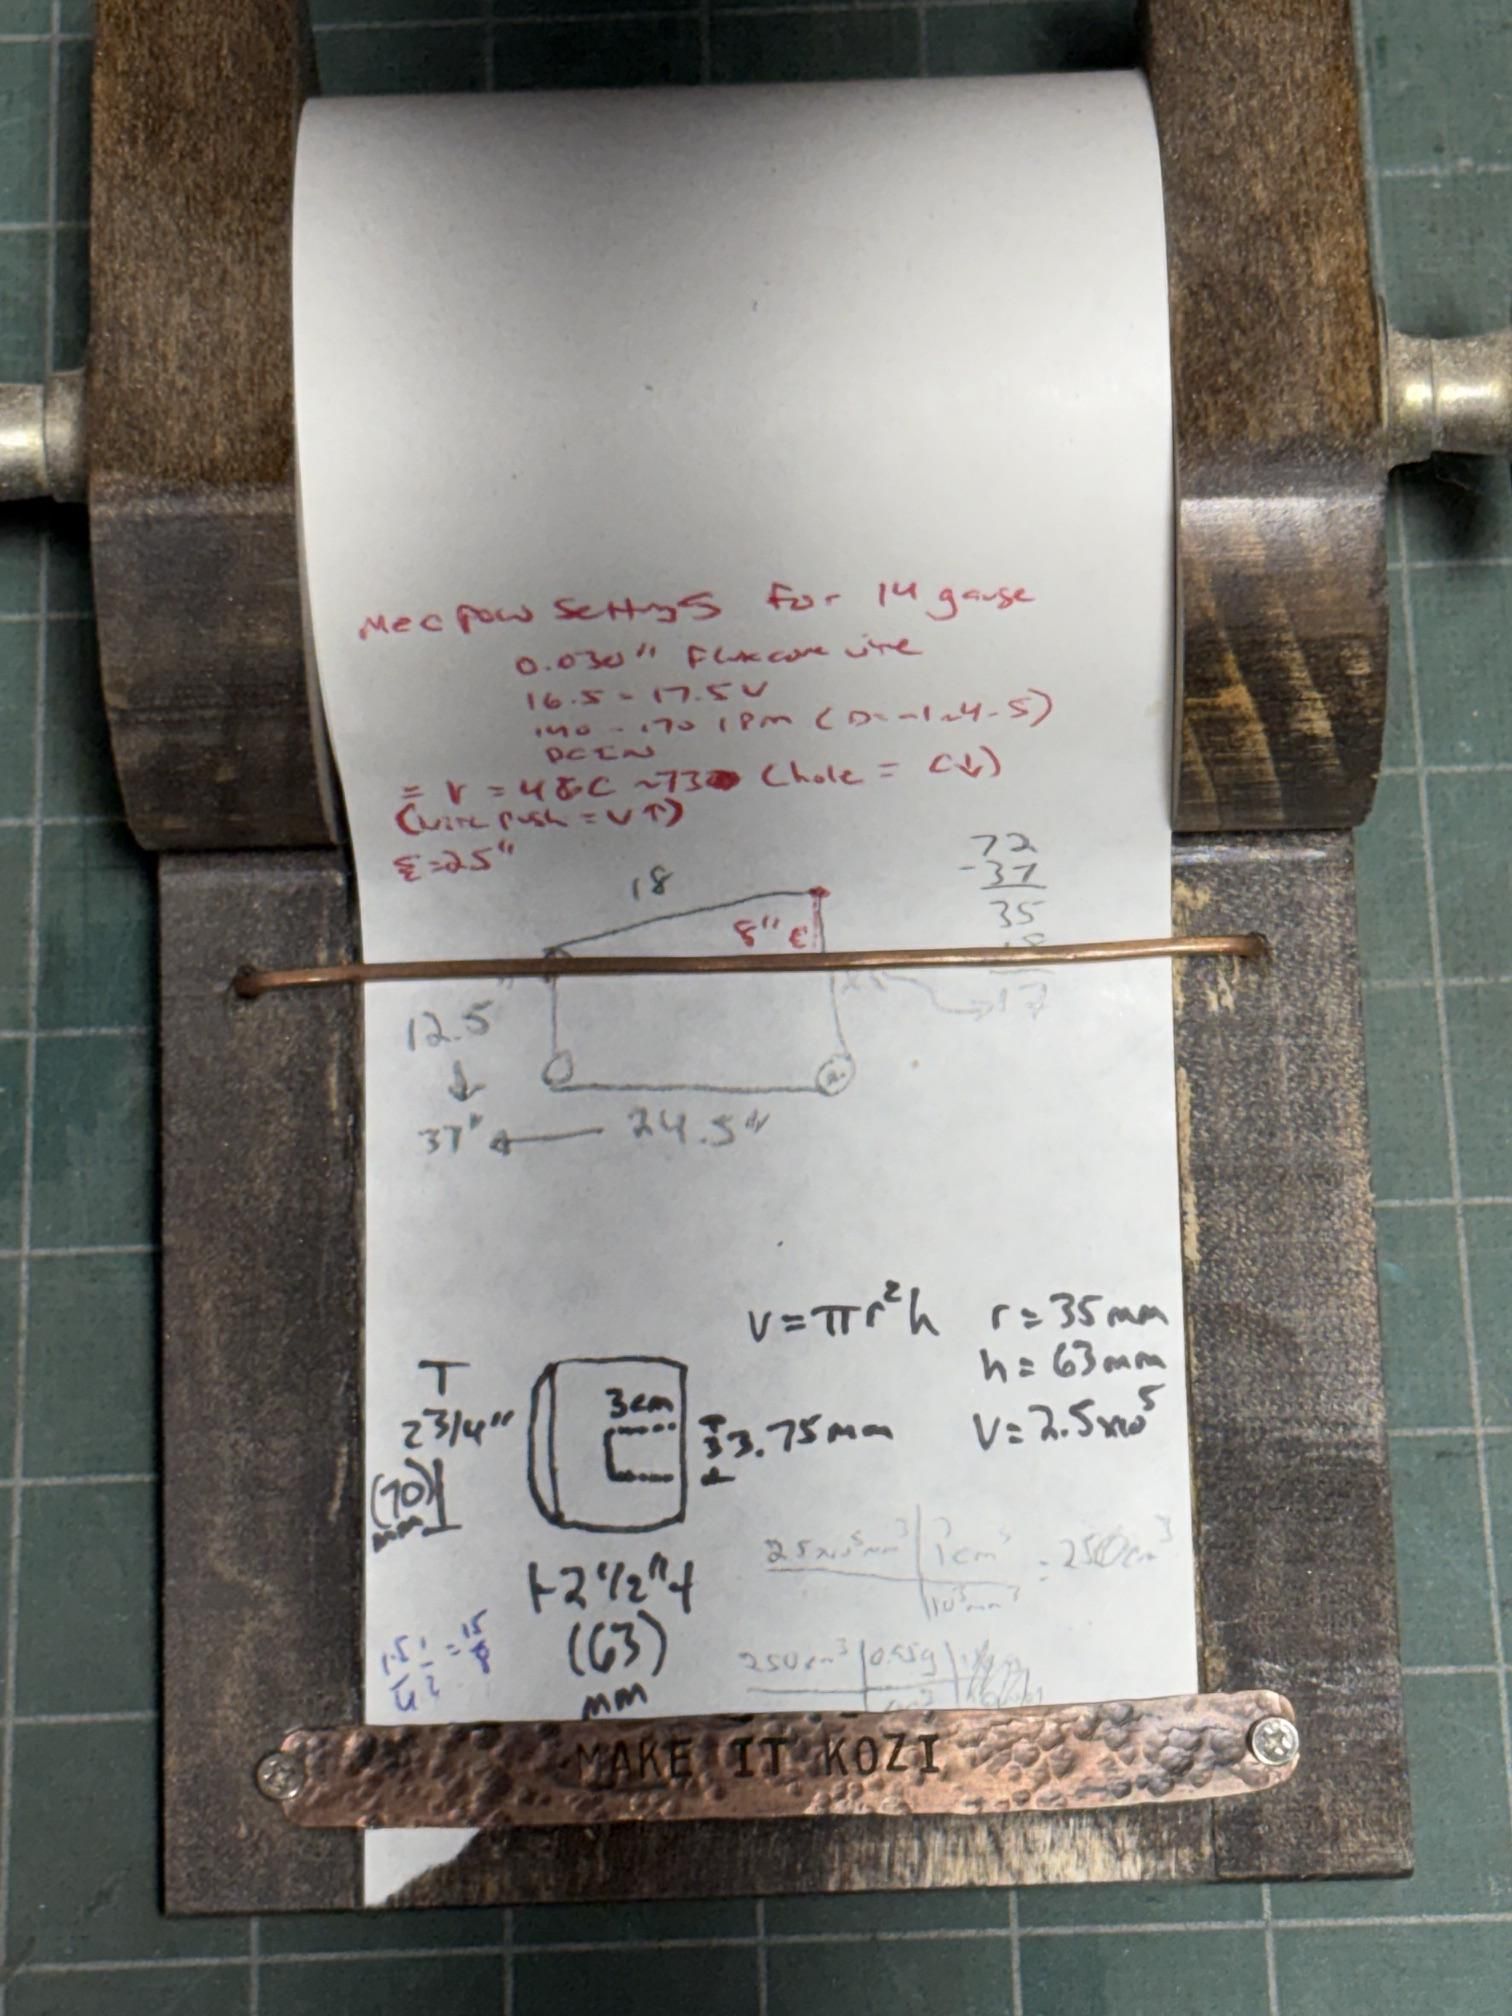


Big picture is to perform the following:
- From the treadmill, obtain the motor, control board, and steel for the frame,
- Secure the frame in order to accommodate the 2x72-in belts,
- Ensure the belt will stay aligned to the tensioner, motor hub, and the platen.
Sounds simple enough but this involved a lot of brainstorming. Watching videos & looking online at photos of other typical dimensions helped, but I needed some real deal dimensions to get this thing in order. I will share as much as I can along the way.
Treadmill Tear Down


I posted a video on YouTube where I tear down a free treadmill my neighbors were throwing out. I had a major component that provides the motor and structural pieces to complete this journey. I just had to tear it down into what was actually needed.
Check out the video for the complete teardown, however, I should mention that every model will be slightly different.
Ultimately, I made out with the 2.75 HP DC motor (with flywheel), the structural steel (0.07-in thick), and the motor control board.
On a side note: I also used the long treadmill roller to create an outfeed for my table saw. You can check out the video link HERE.
D-Plate
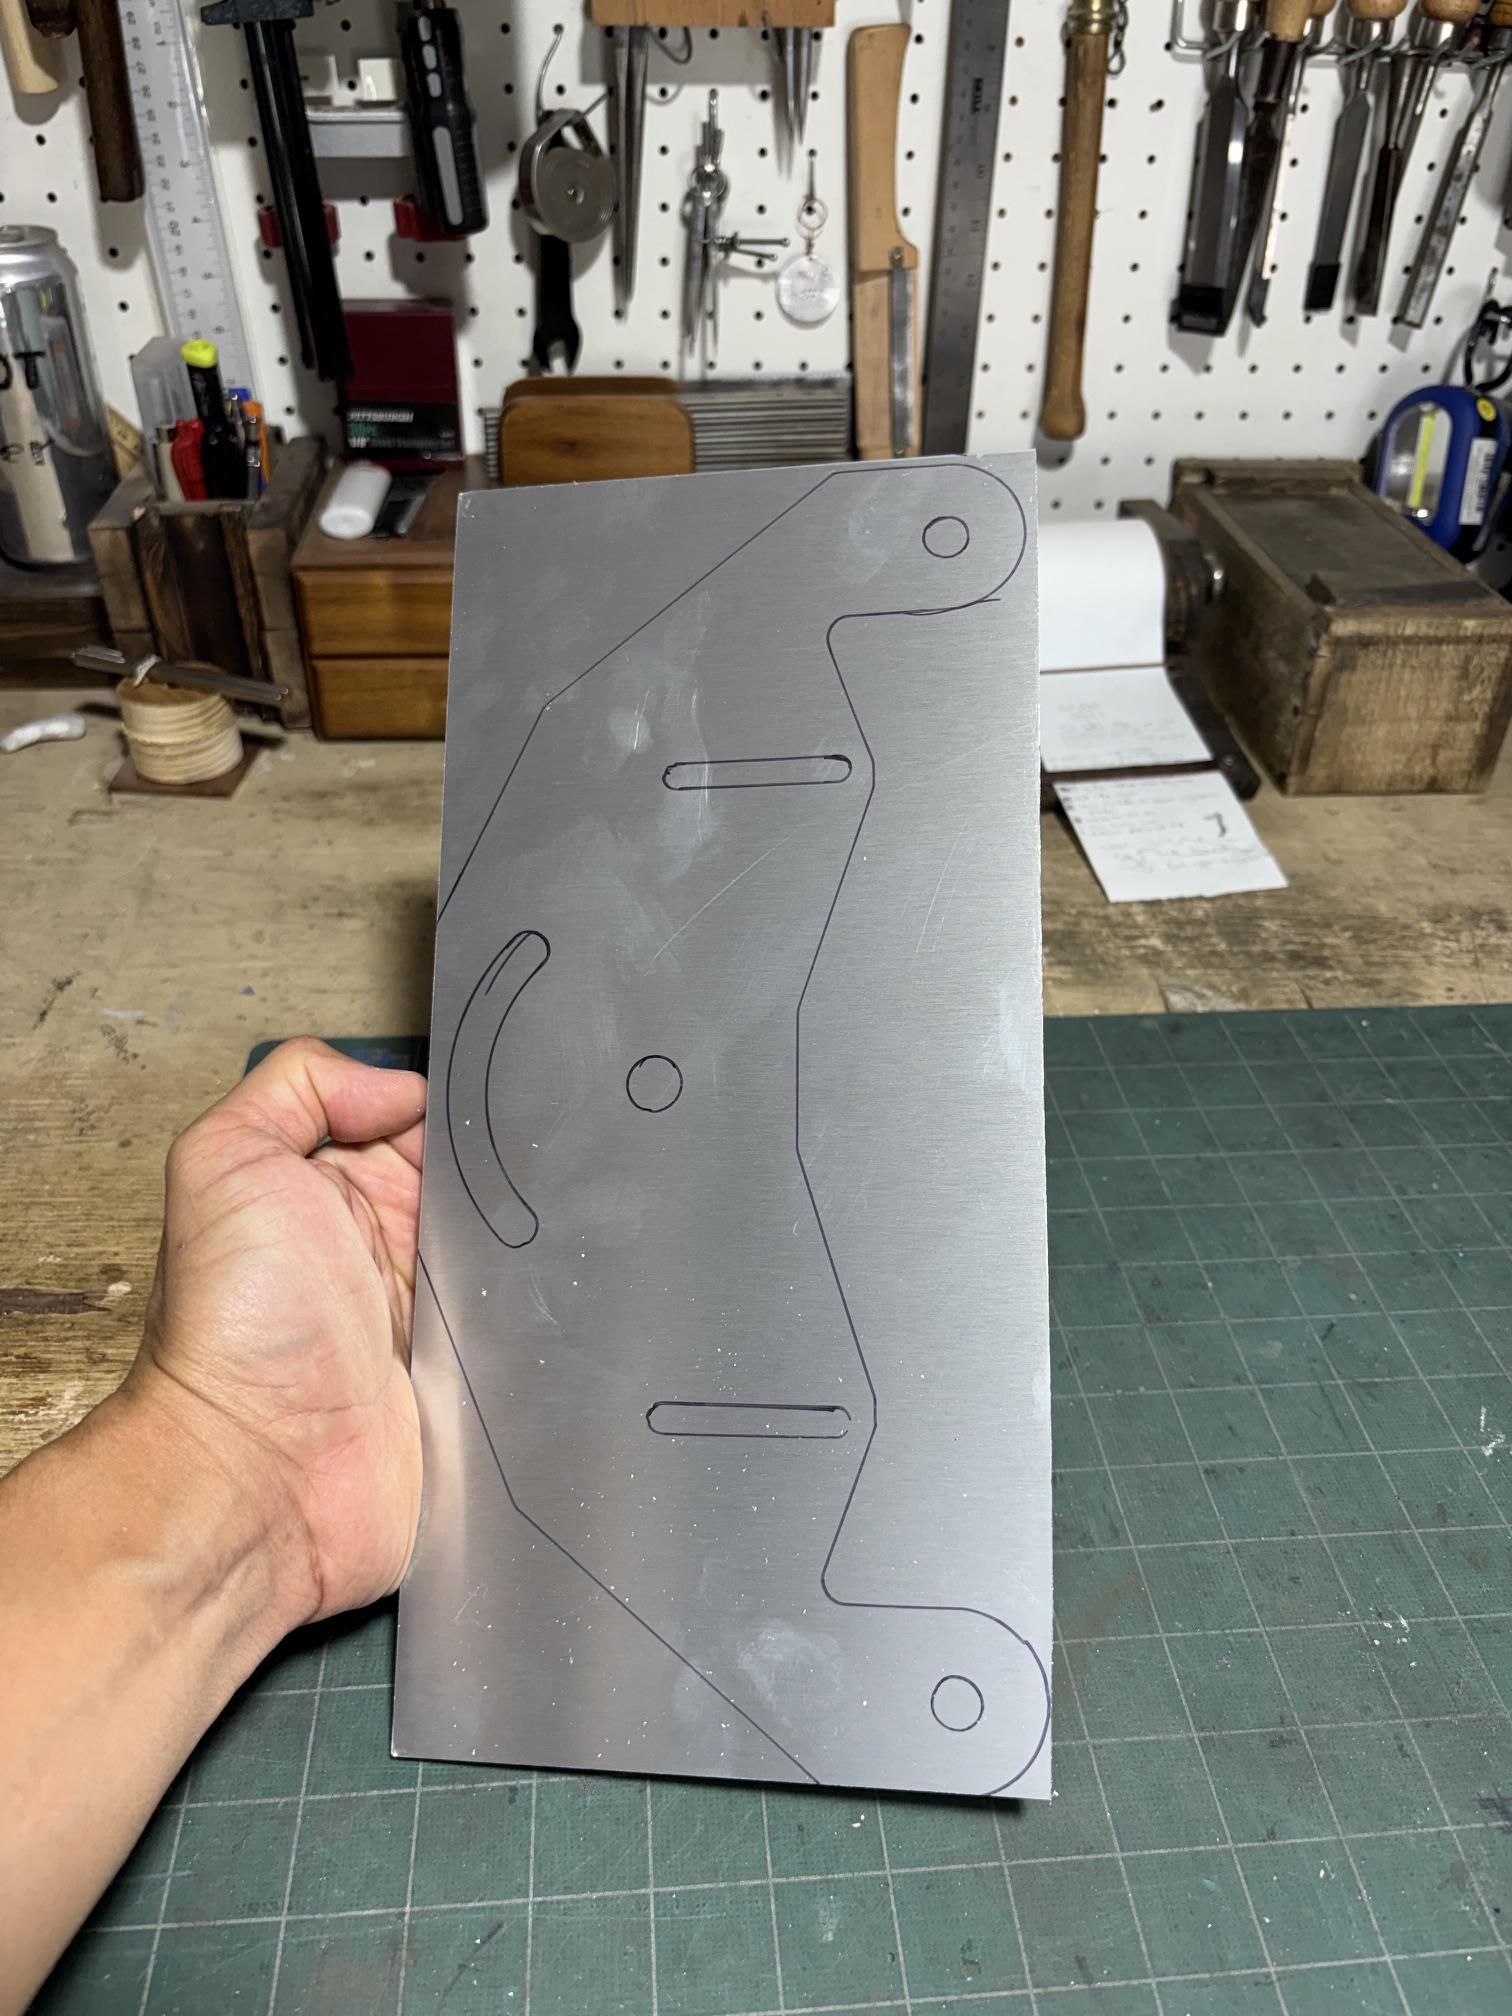
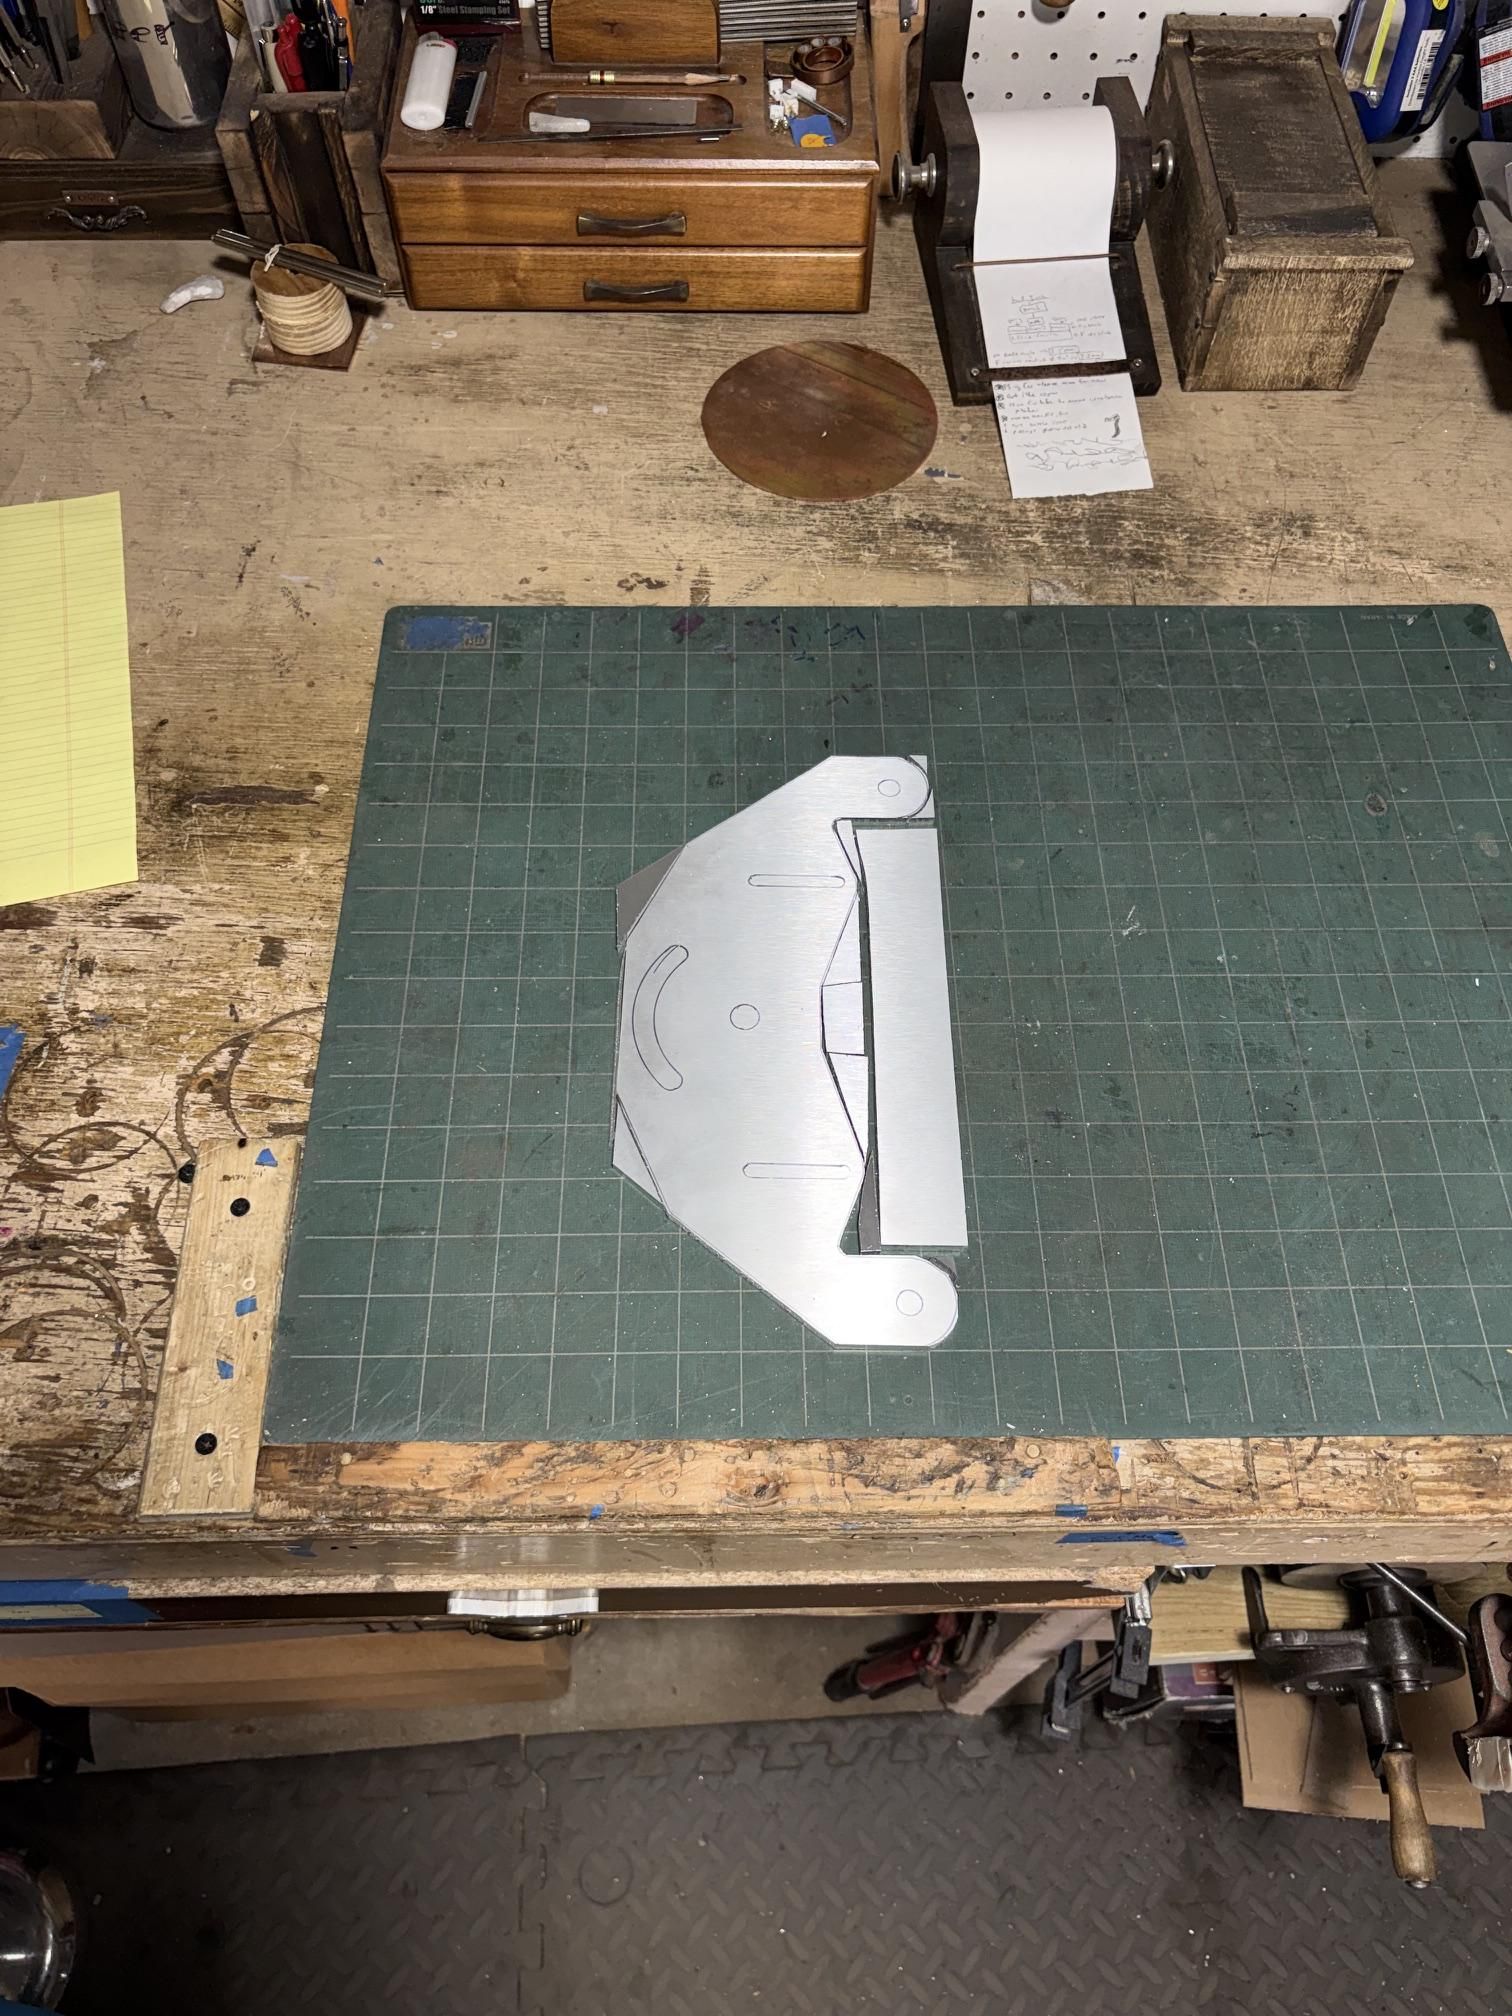


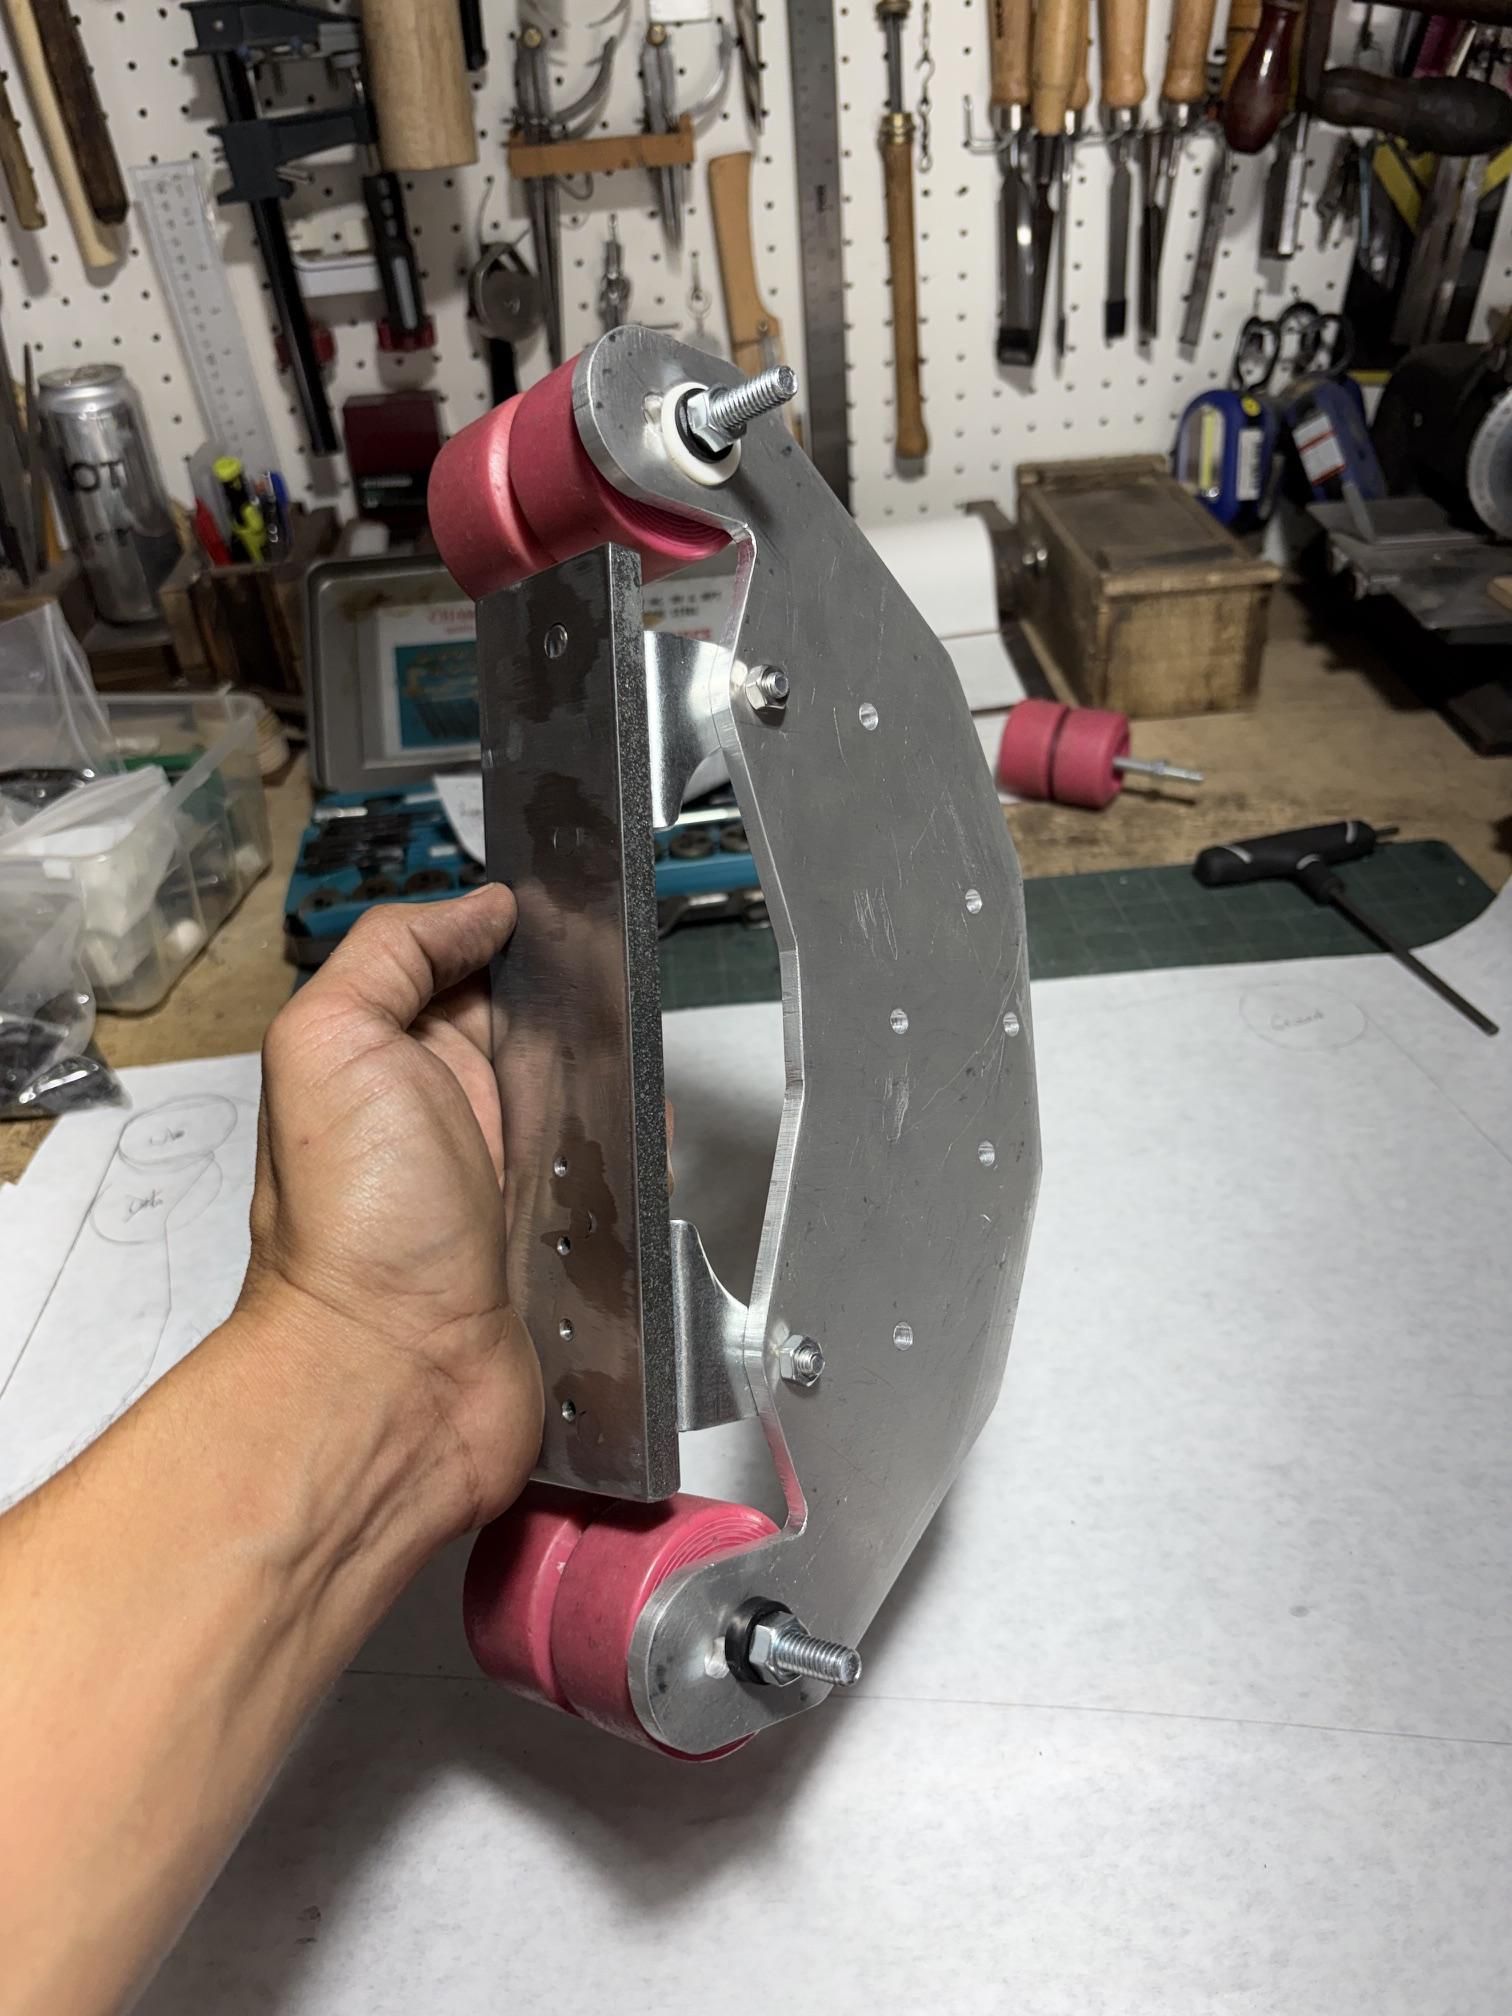
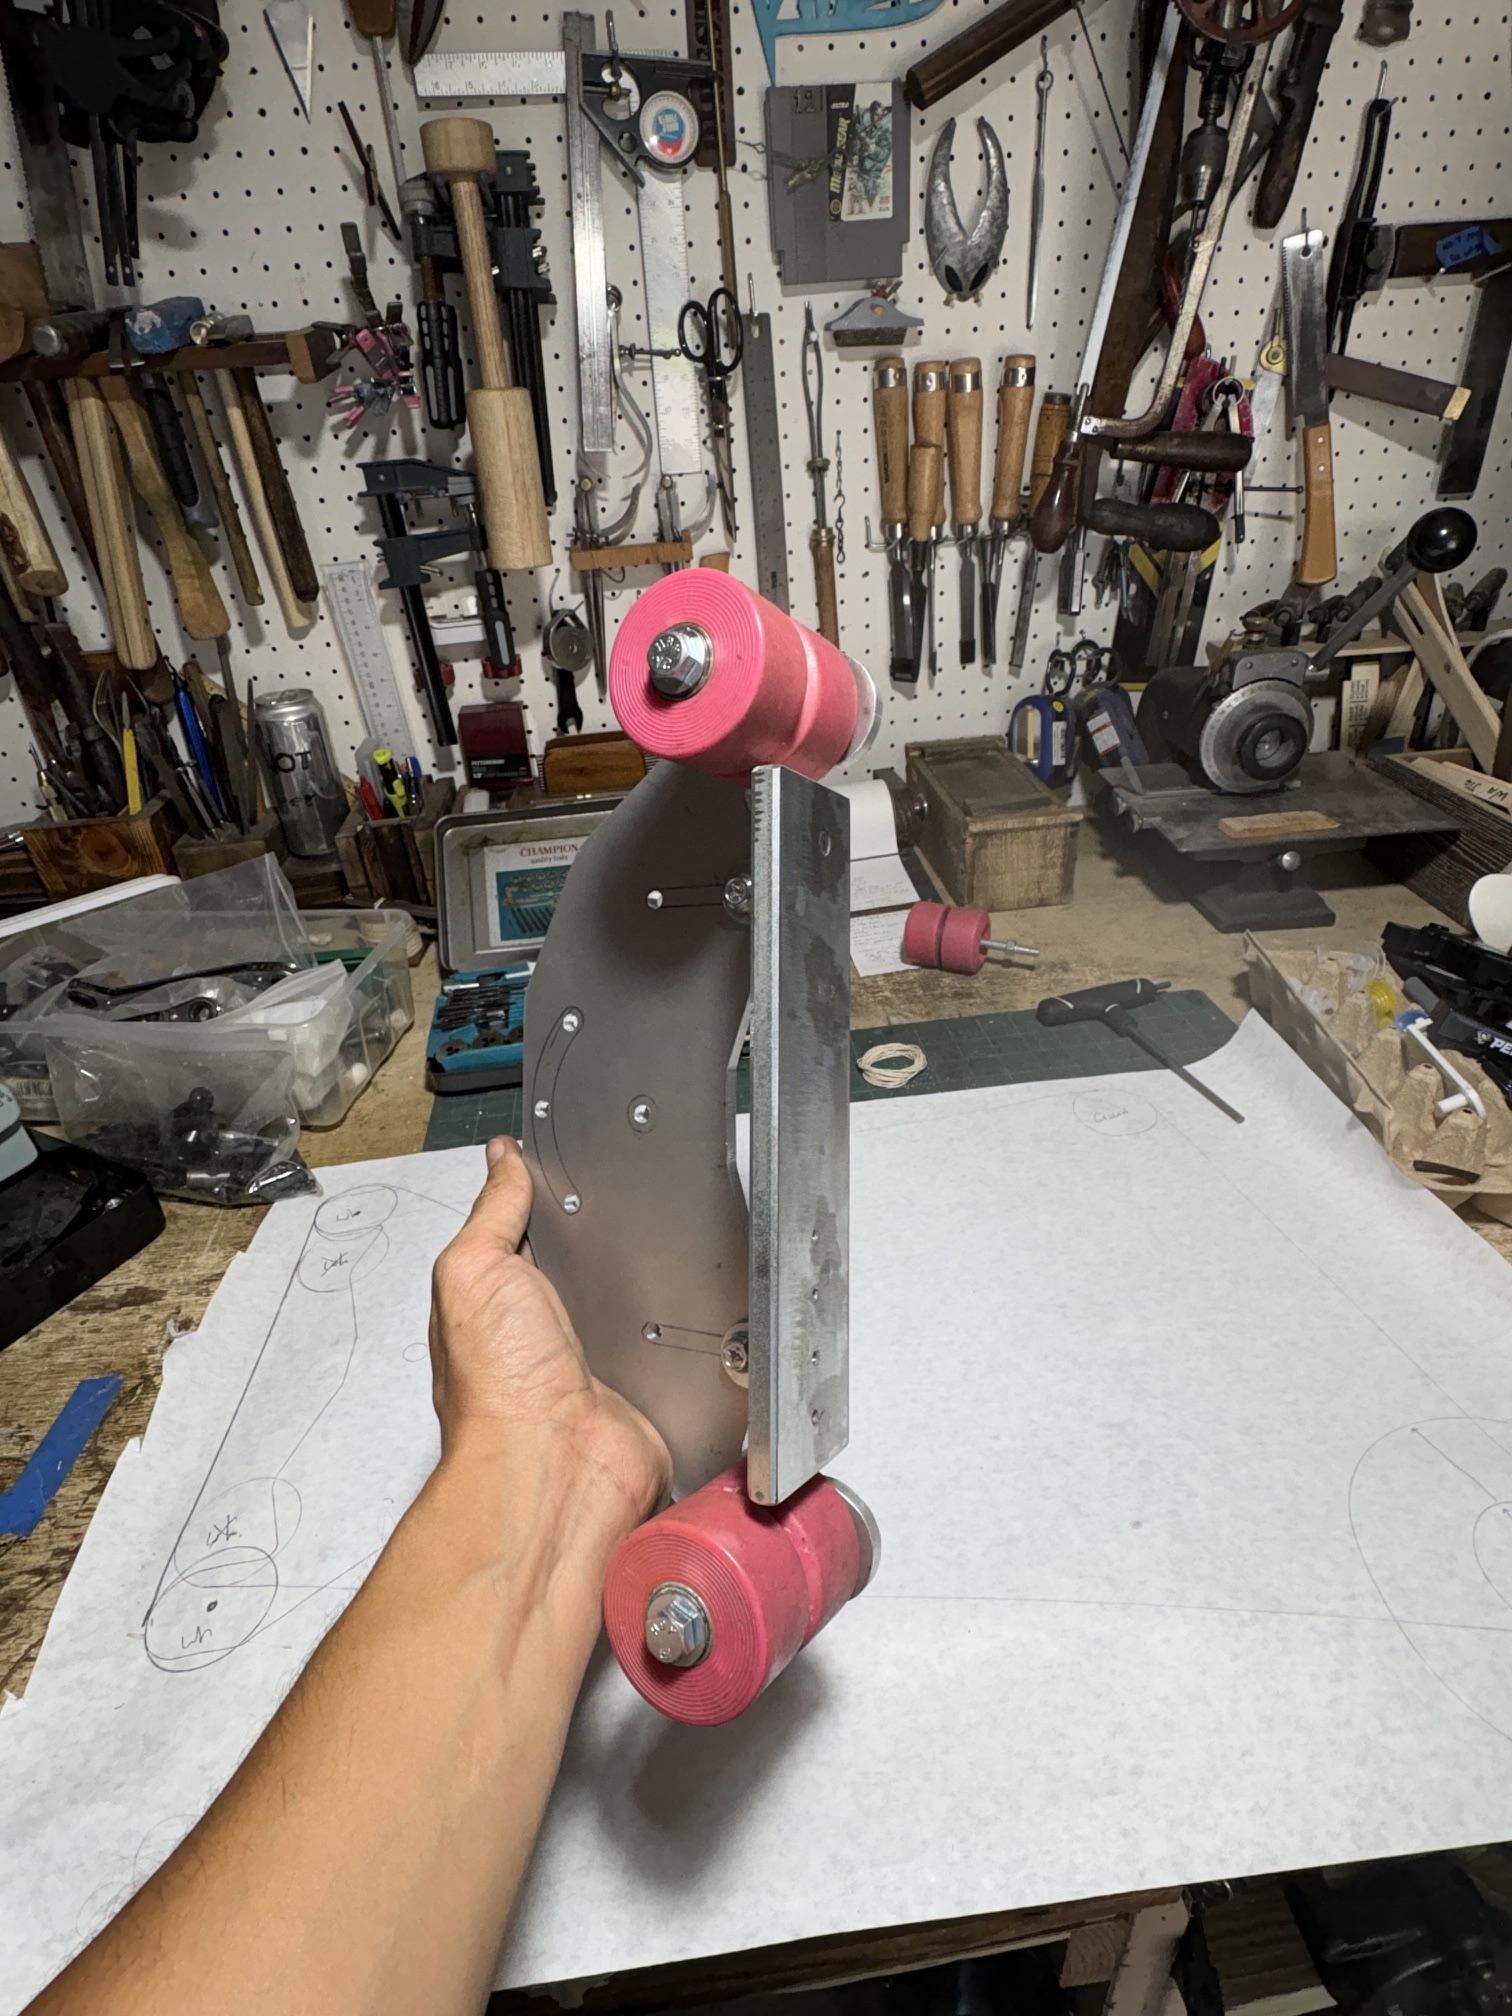
Using a template, I traced the D Plate out on a piece of 1/4-inch 6061 aluminum plate (pic 1). Funny enough, I won this aluminum plate on an auction site for like $5. I figure this is light enough to be easy to maneuver, cut, and form while also being strong enough to take the work / vibration.
I cut along the template lines using my bandsaw (pic 2) since it was aluminum but this can also be done with a hacksaw or a jigsaw equipped with a metal cutting blade.
That taken care of, I drilled the accompanying holes on my drill press. I have a lot of 3/16-inch bolts so I drilled holes accordingly. I also drilled holes for the curved lines and used a hacksaw to remove the excess (pic 3).
For the backing plate, I cut a 1/4-inch steel plate I recovered from an old 1980's TI typewriter. This steel was robust enough to handle what I need it for but it was surprisingly easy to drill and tap for the holes I needed to mount the thing. Mounting was performed using angle brackets I had lying around (pic 4-6). Actual angle iron may be preferable here, but time will tell. If anyone has experience, please share in the comments.
The last piece of this puzzle were the rollers (contact wheels) which are skateboard wheels stacked on top of each other. Together, these are a little over 2-inches wide which works for what I need them for. Others have used longboard wheels, too, or go with a kit online. If you follow me long enough, you know that I am cheap but that has come back to bite me, hehe. Again, we will see...
Frame
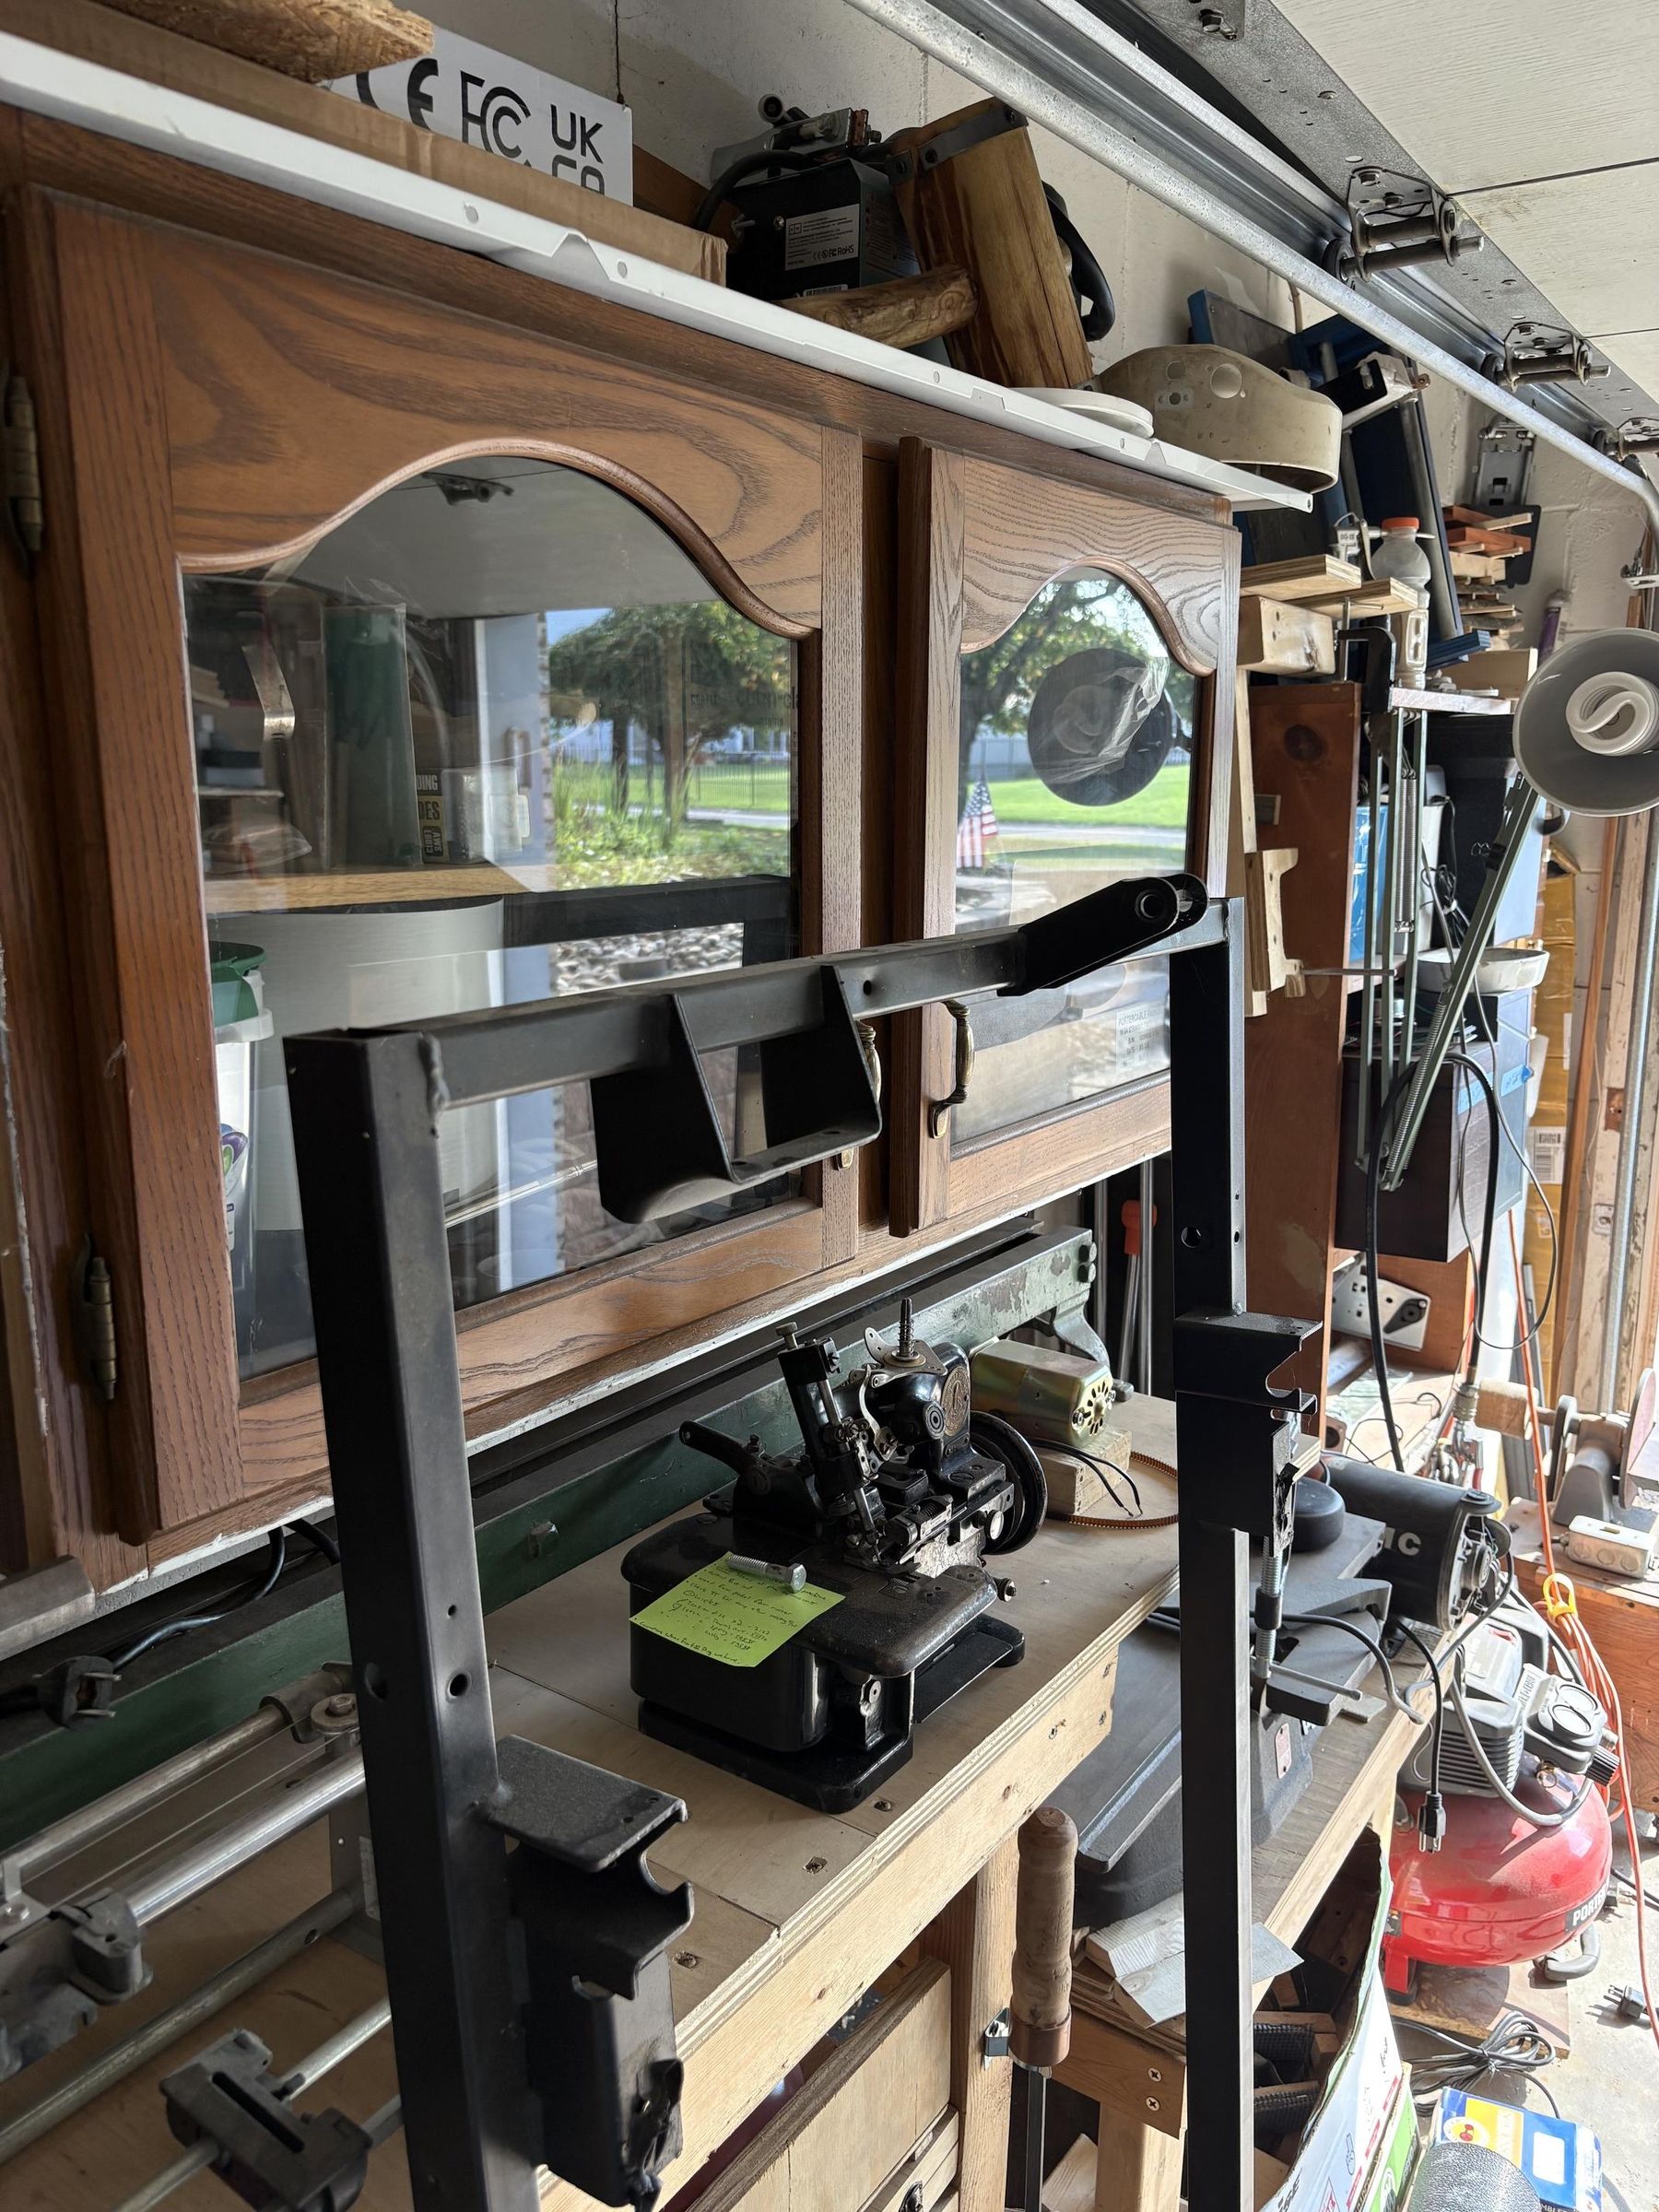

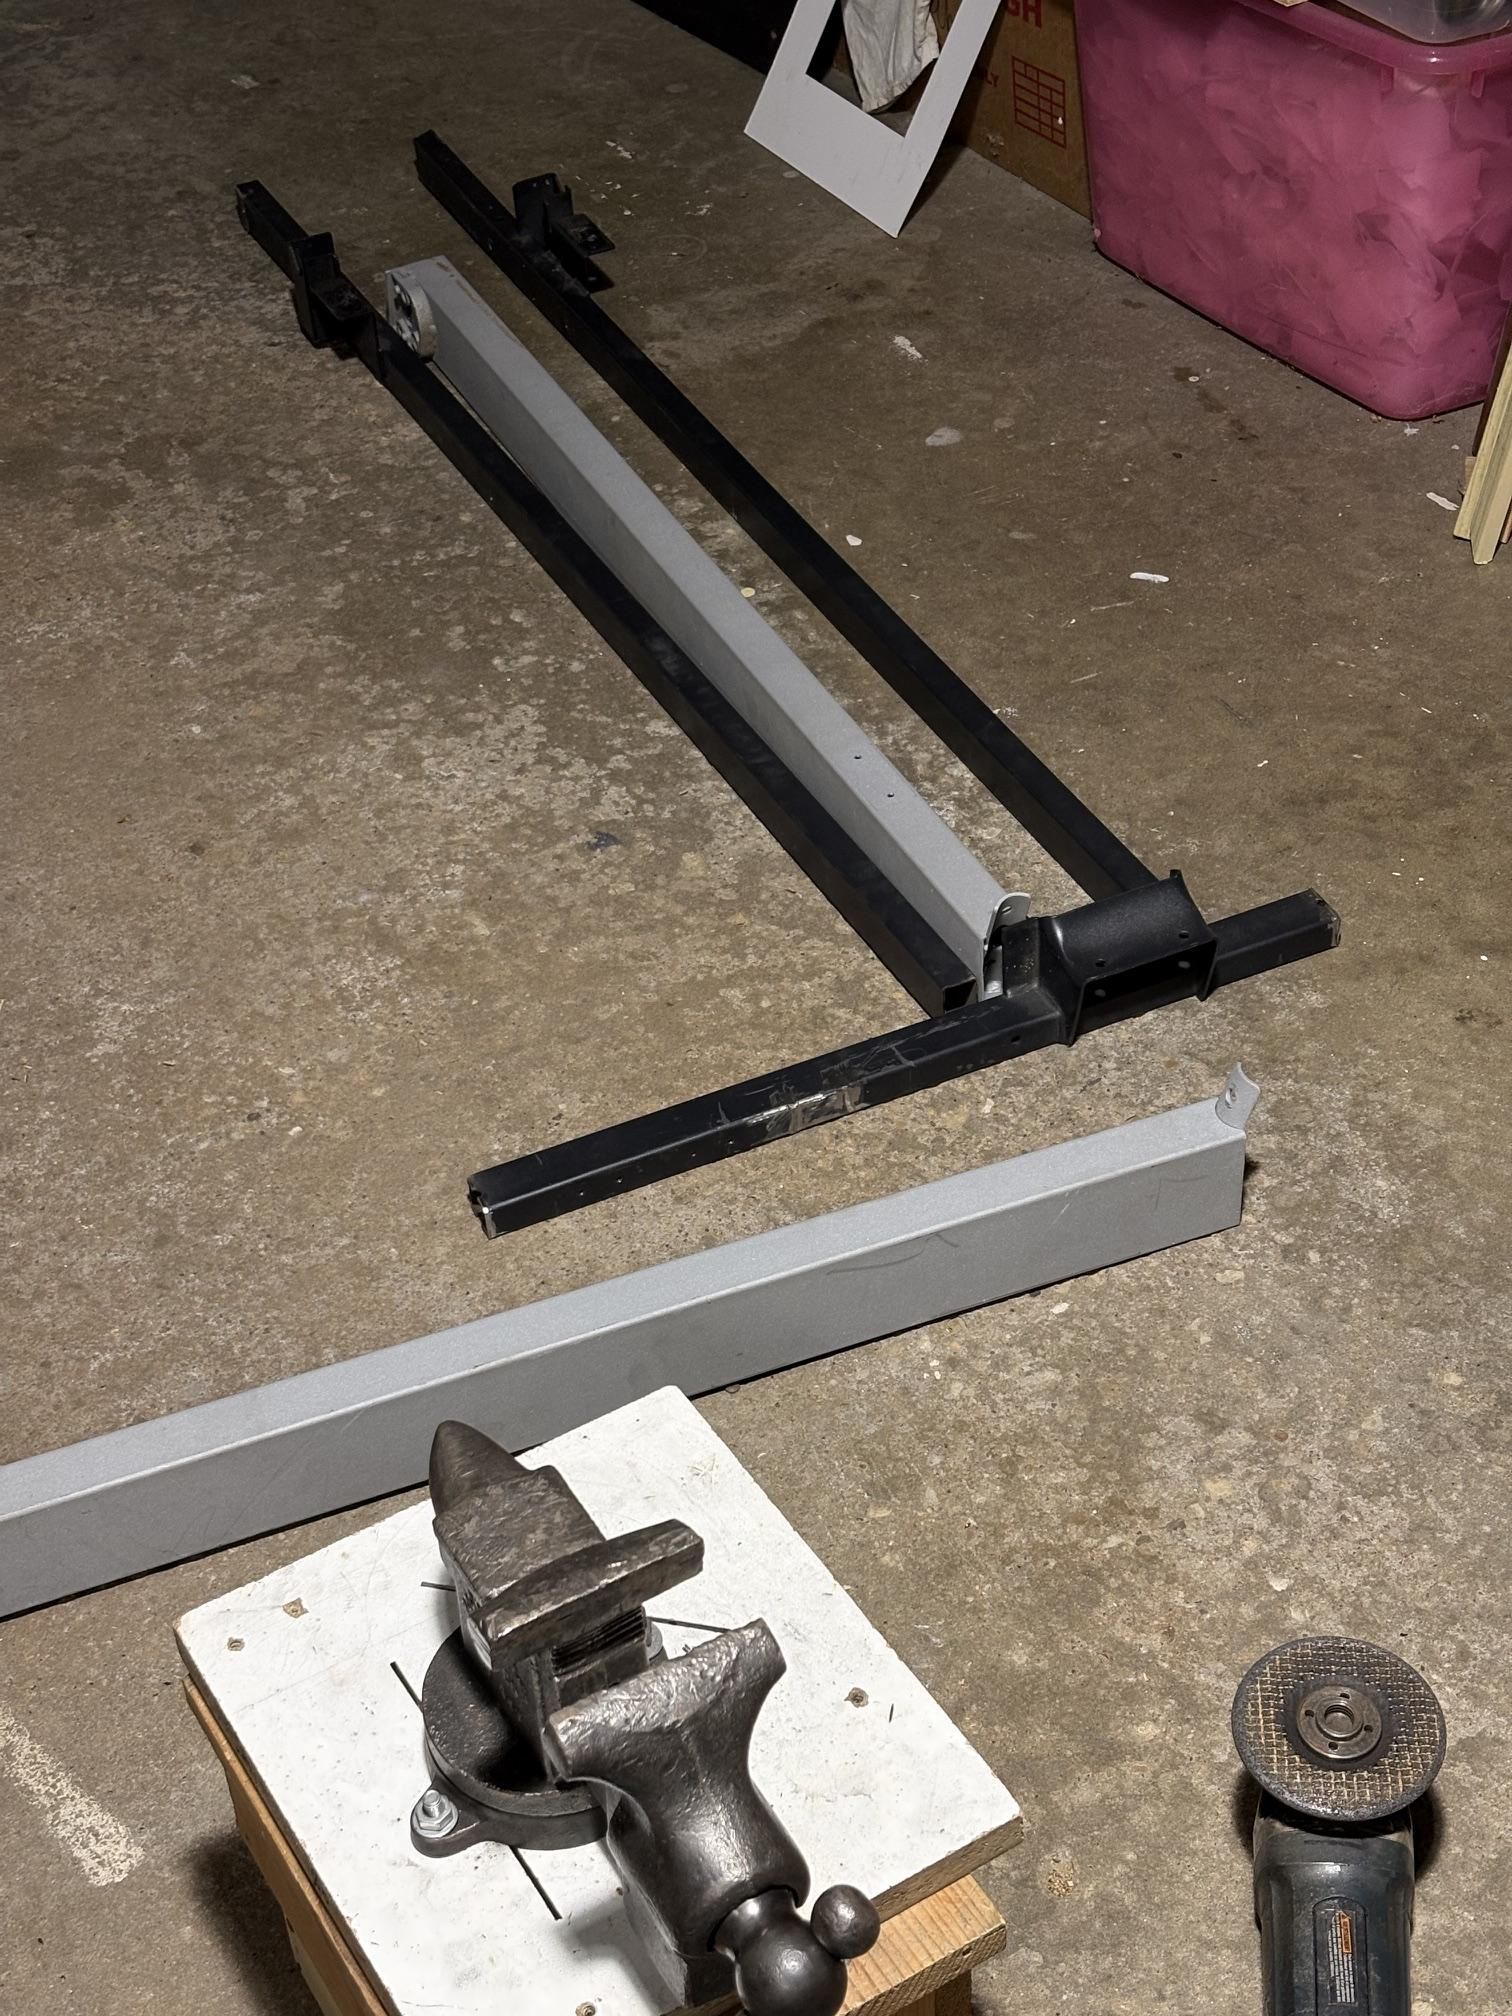





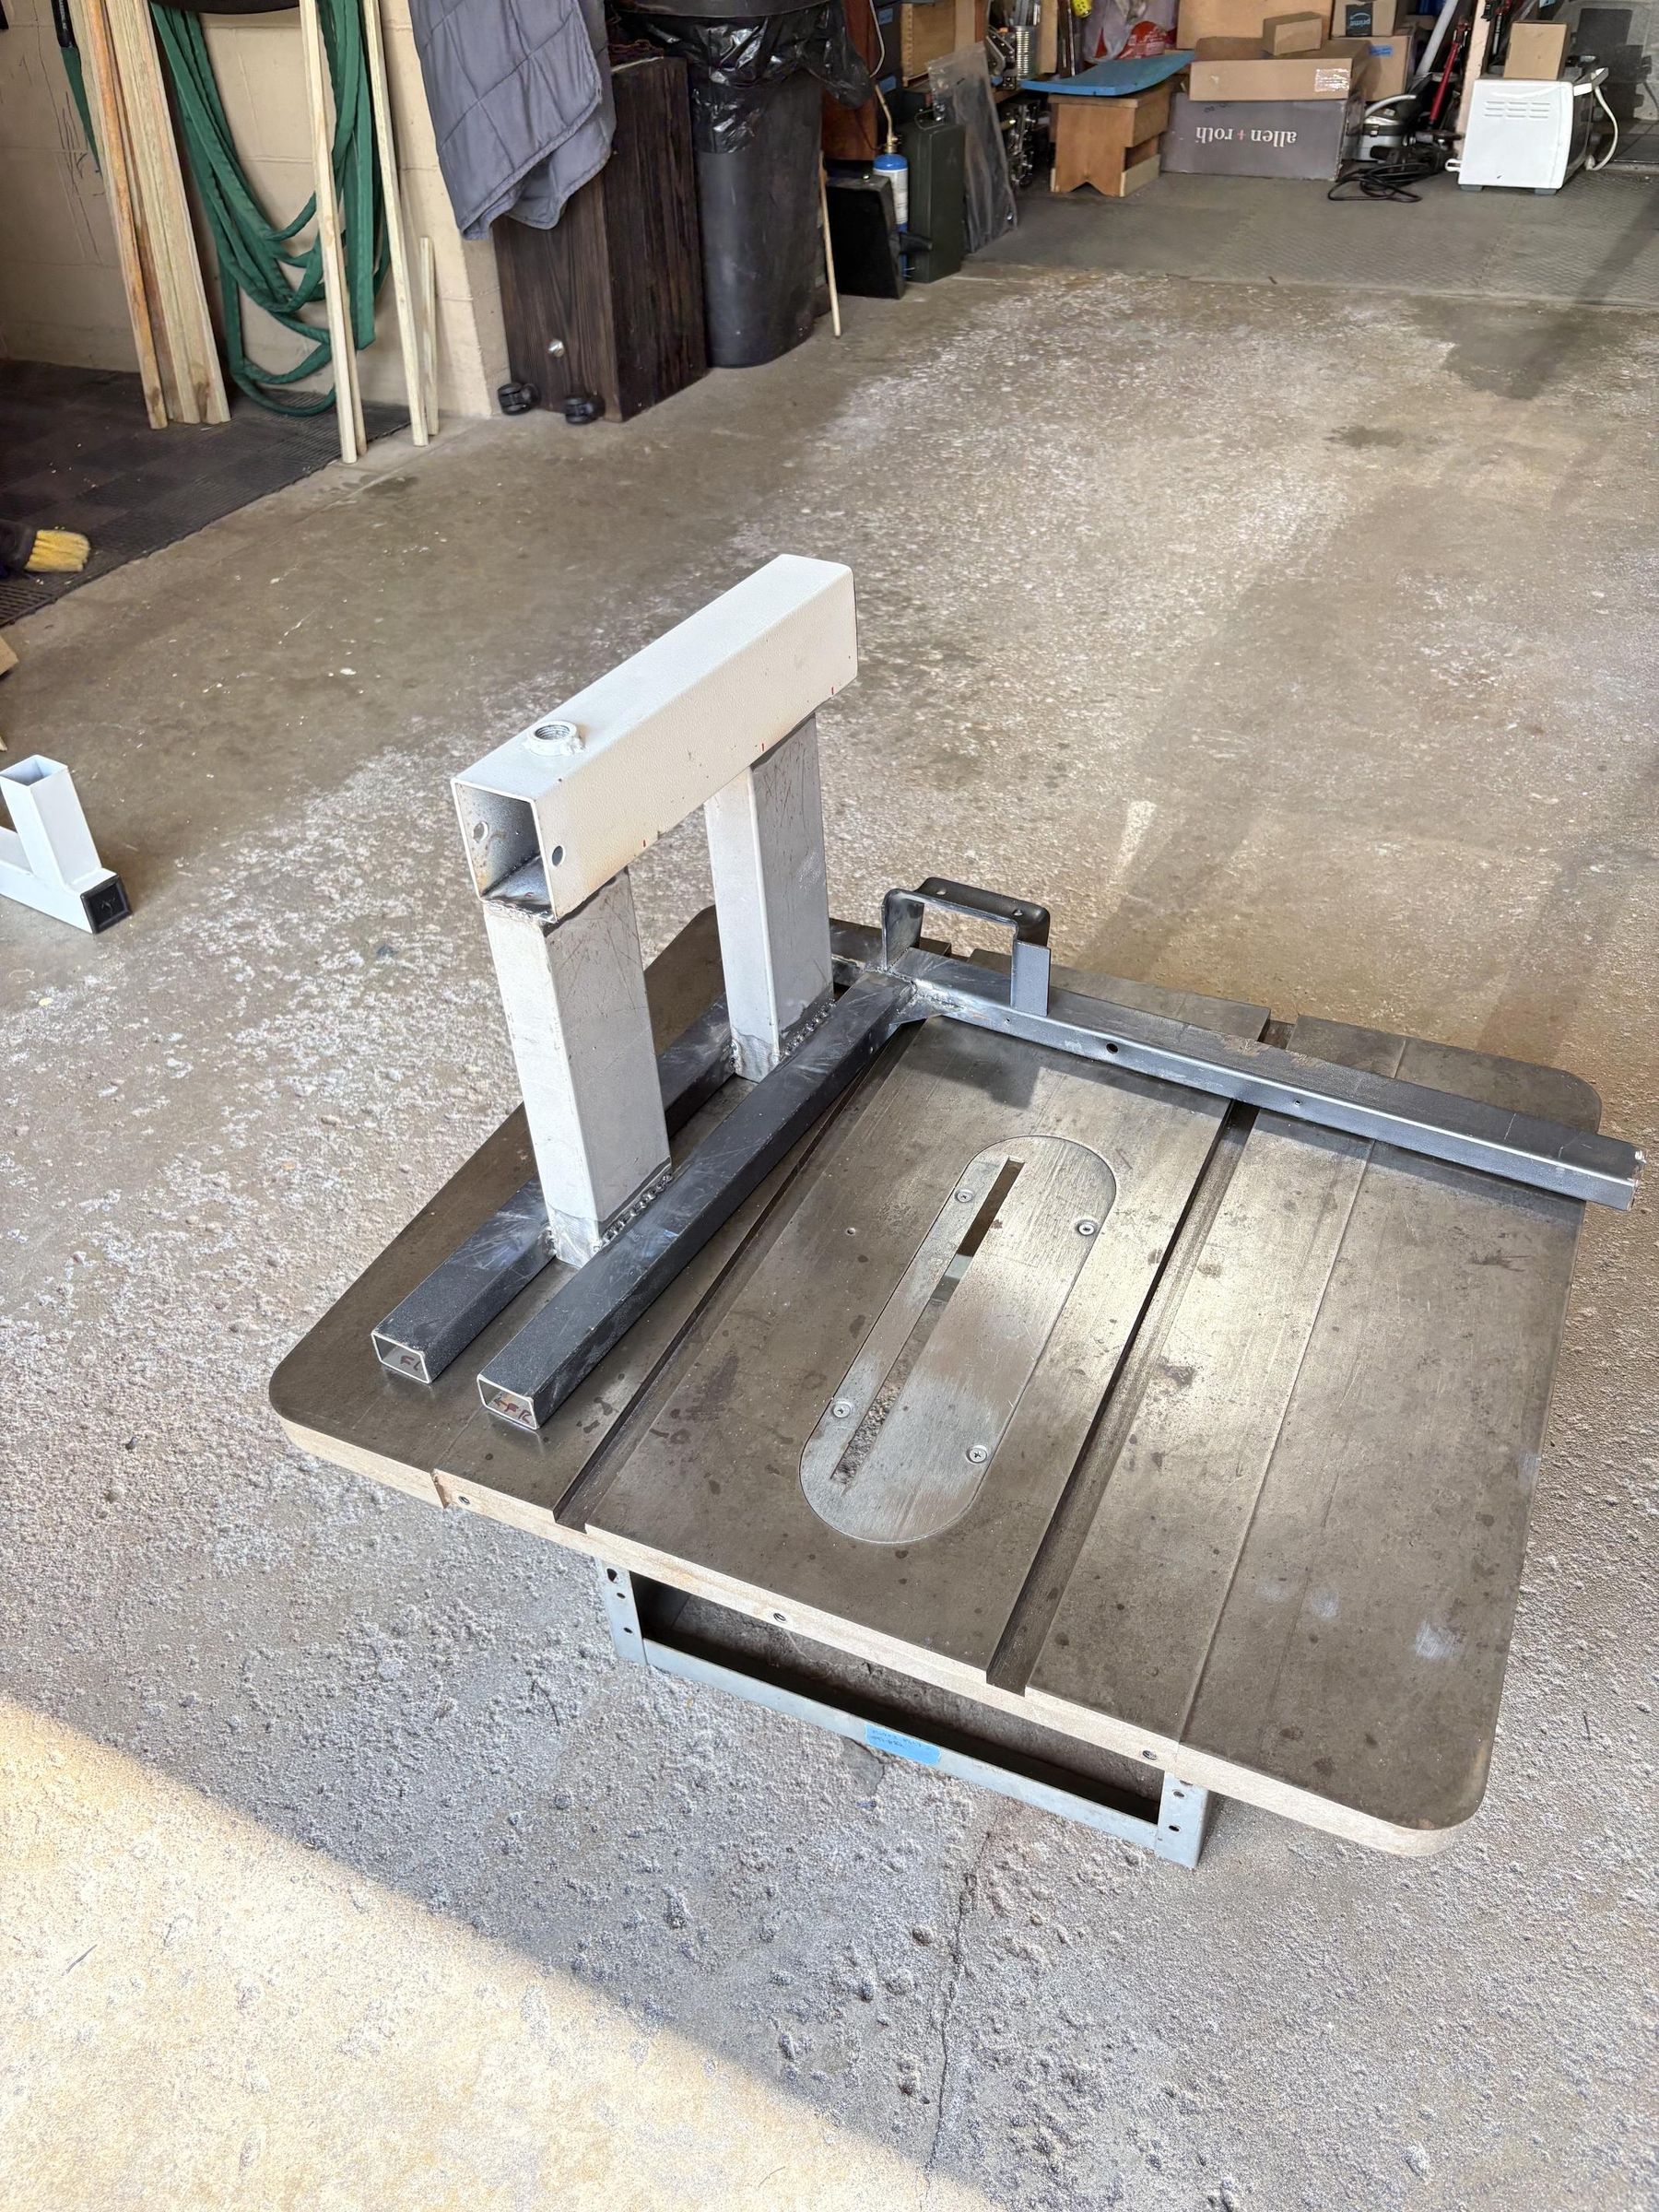

For the base, I used the treadmill steel from the 1x1.5-inch frame (pic 1), especially the motor mount (pic 2). Why make things harder for myself. The motor mount piece measures 18-inches long in the picture but I wound up cutting off around 7-inches of excess. The two middle black supports were cut to 17-inches.
My mindset here is that the platen and the motor wheel need to be aligned as much as possible for the belt to track and operate properly. This is why the pictures show 90% of the motor frame protruding to the right of the base. There was not a lot of room for what I had in mind for the motor wheel but you will see that in the next step. What you don't want to happen is welding (or drilling/securing bolt holes) incorrectly where you have to replan the next step and wasting time. Take the time to do it as correctly as possible the first time!
The silver vertical supports in the middle were cut from the vertical supports of my treadmill frame and their dimensions are 2x3-inches. These two were cut to 10-inches tall. Again, I cut them 10-inches with the tension arm in mind for later. Here, we need enough height to ultimately keep the 2x72-inch belt tight.
Now, the tooling arm of this build actually came from an old workout bench. This part is what moves the barbell rest up and down and is perfect for this exact purpose since it is telescoping. Plus, the wall thickness matches the treadmill support steel which makes my future welding a little simpler. This piece is 12-inches long.
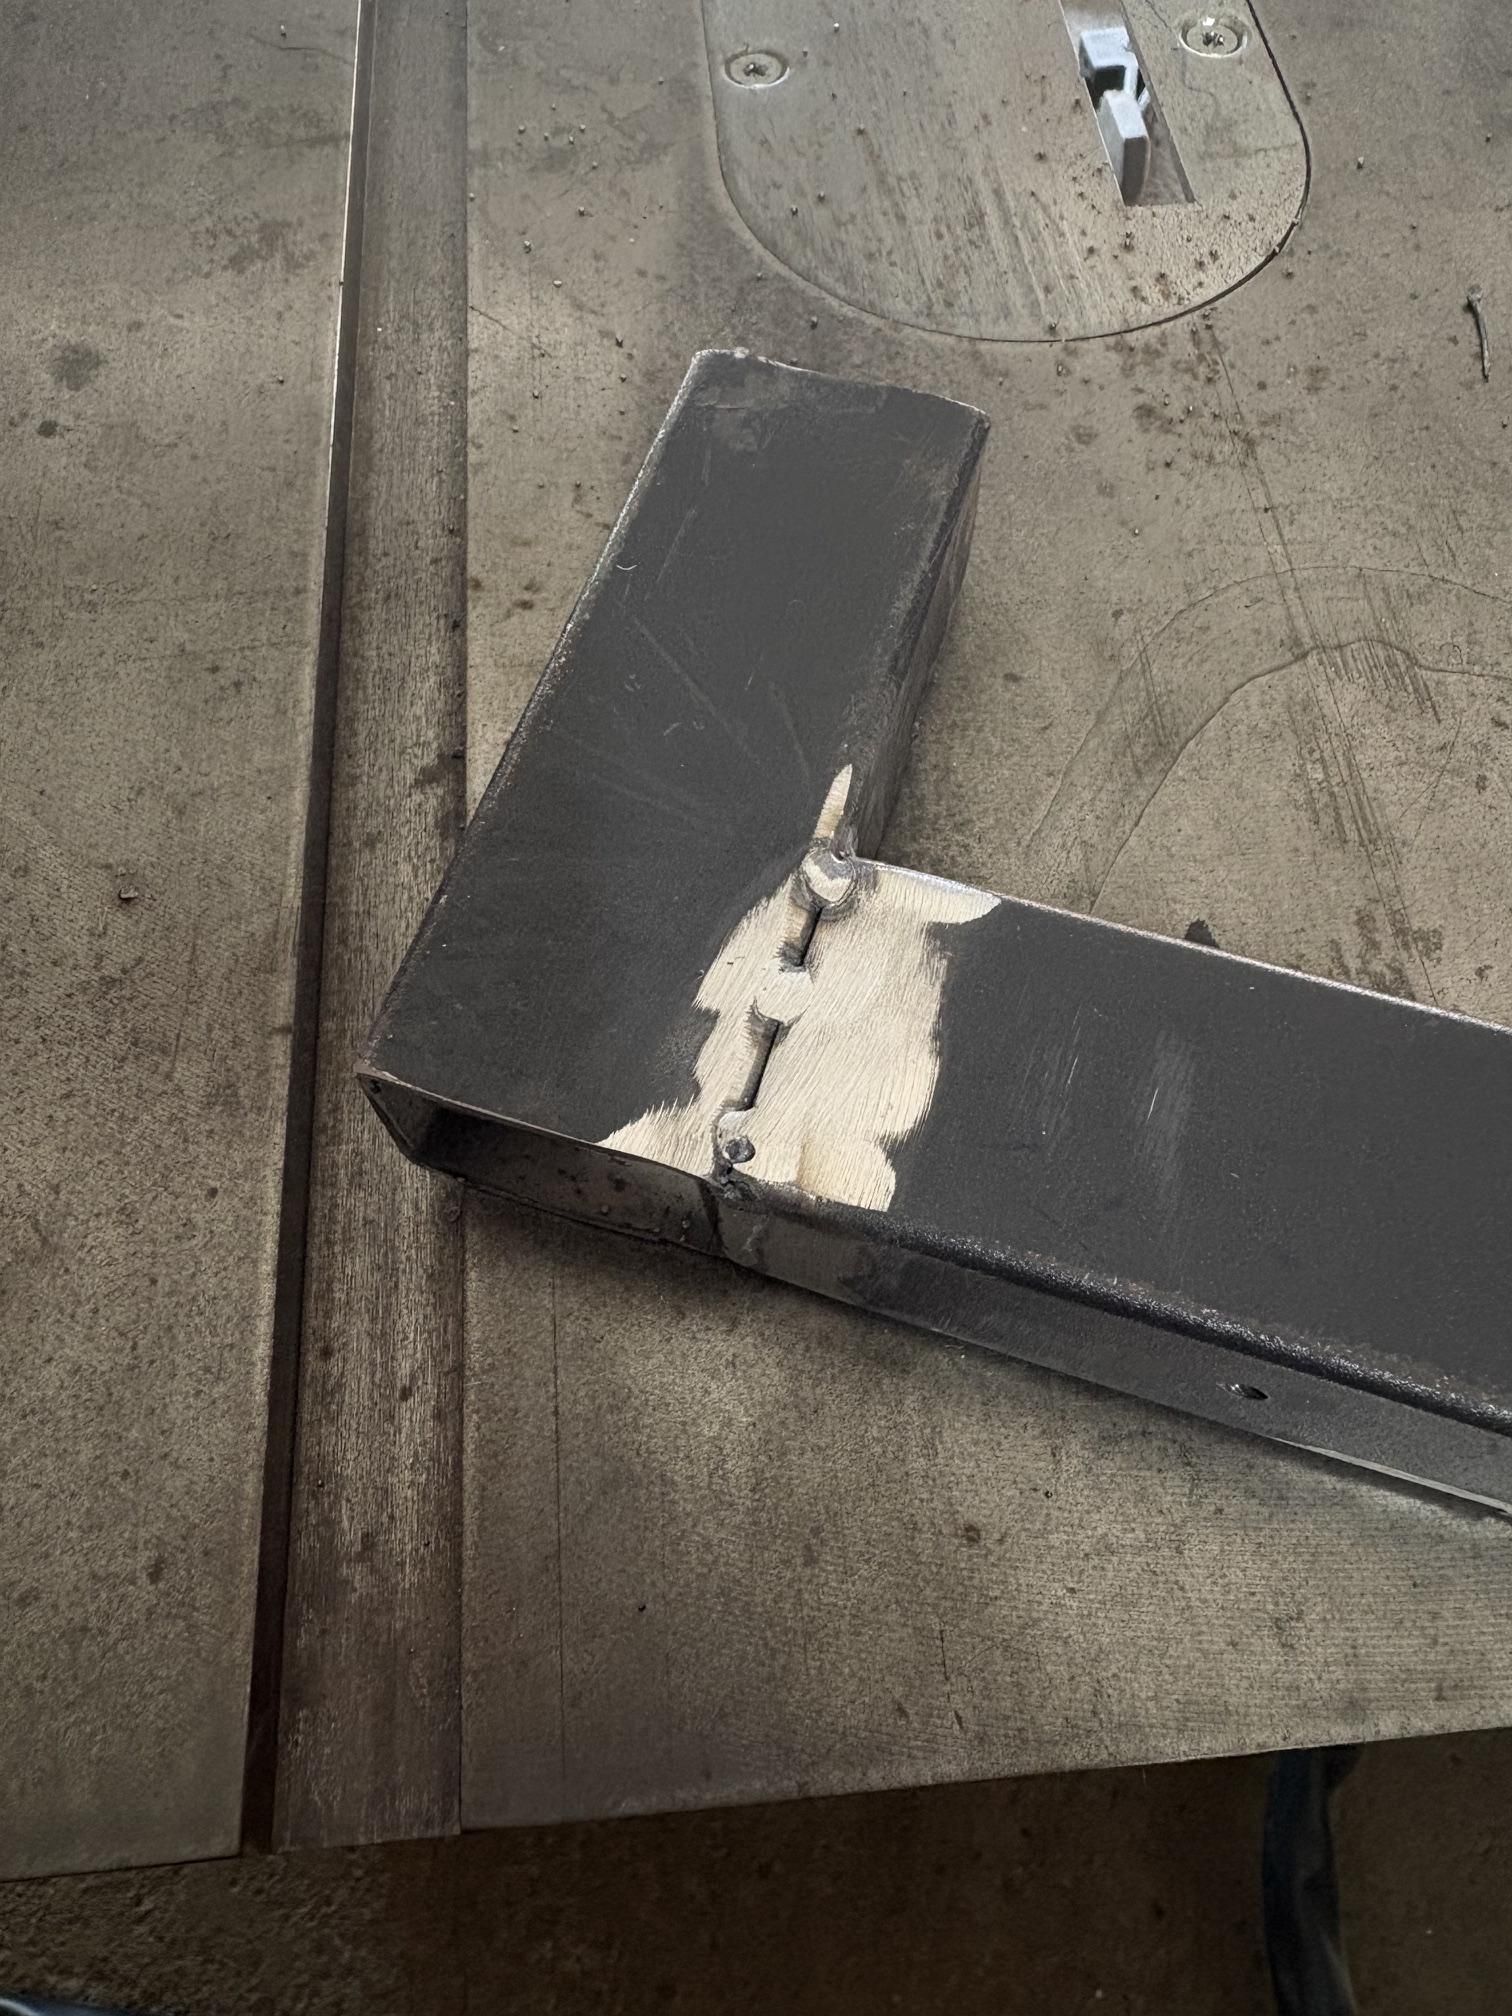
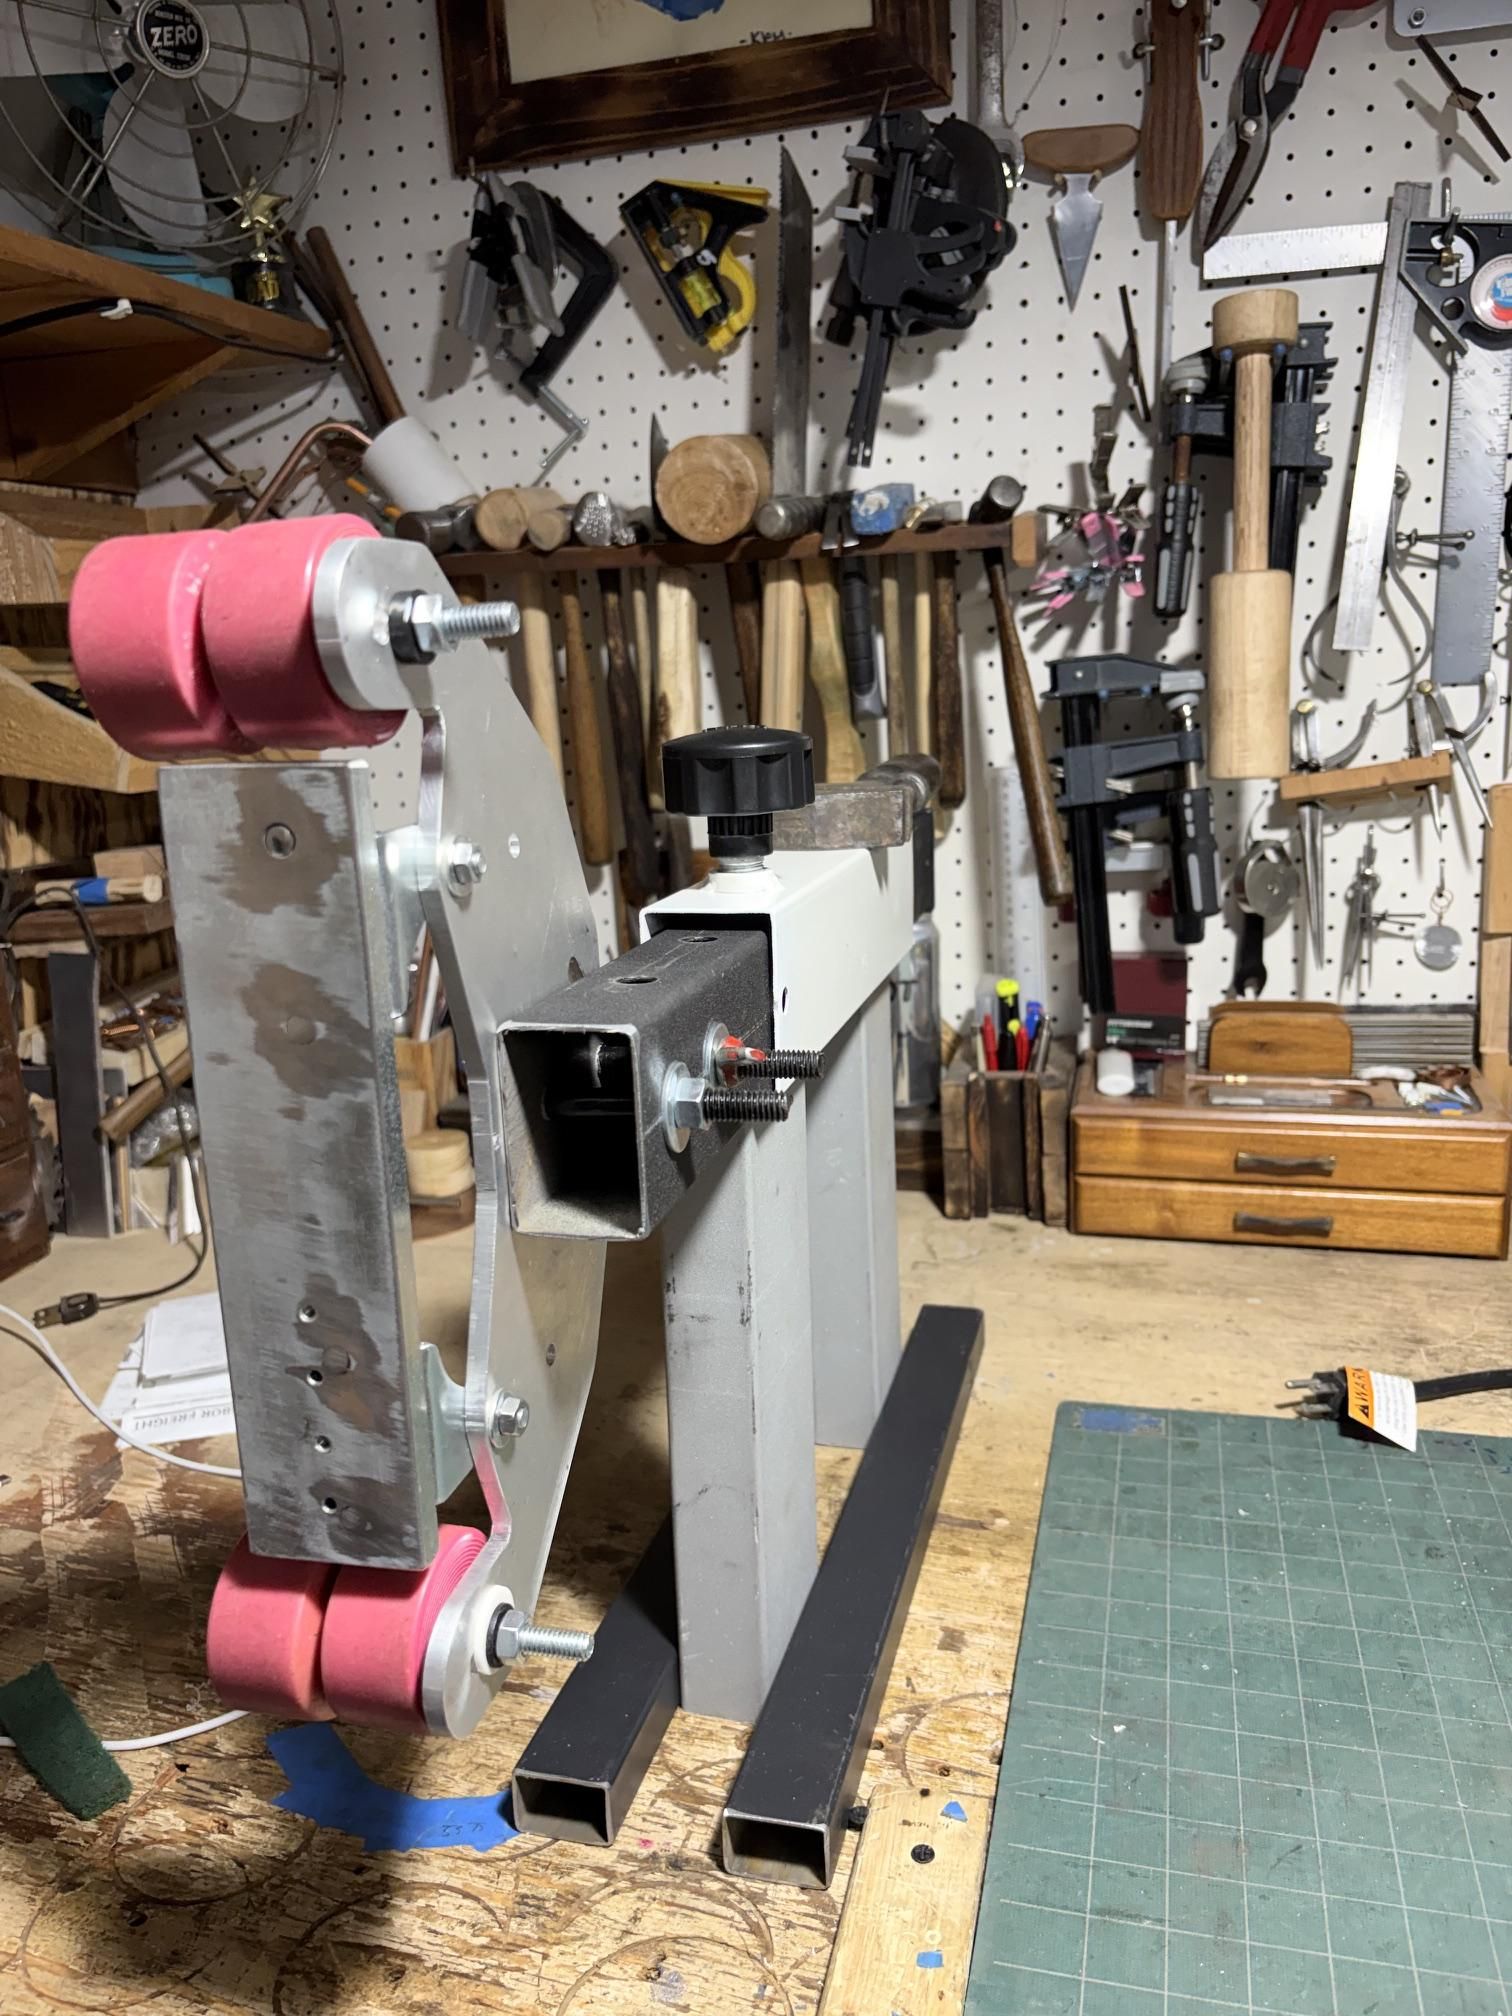
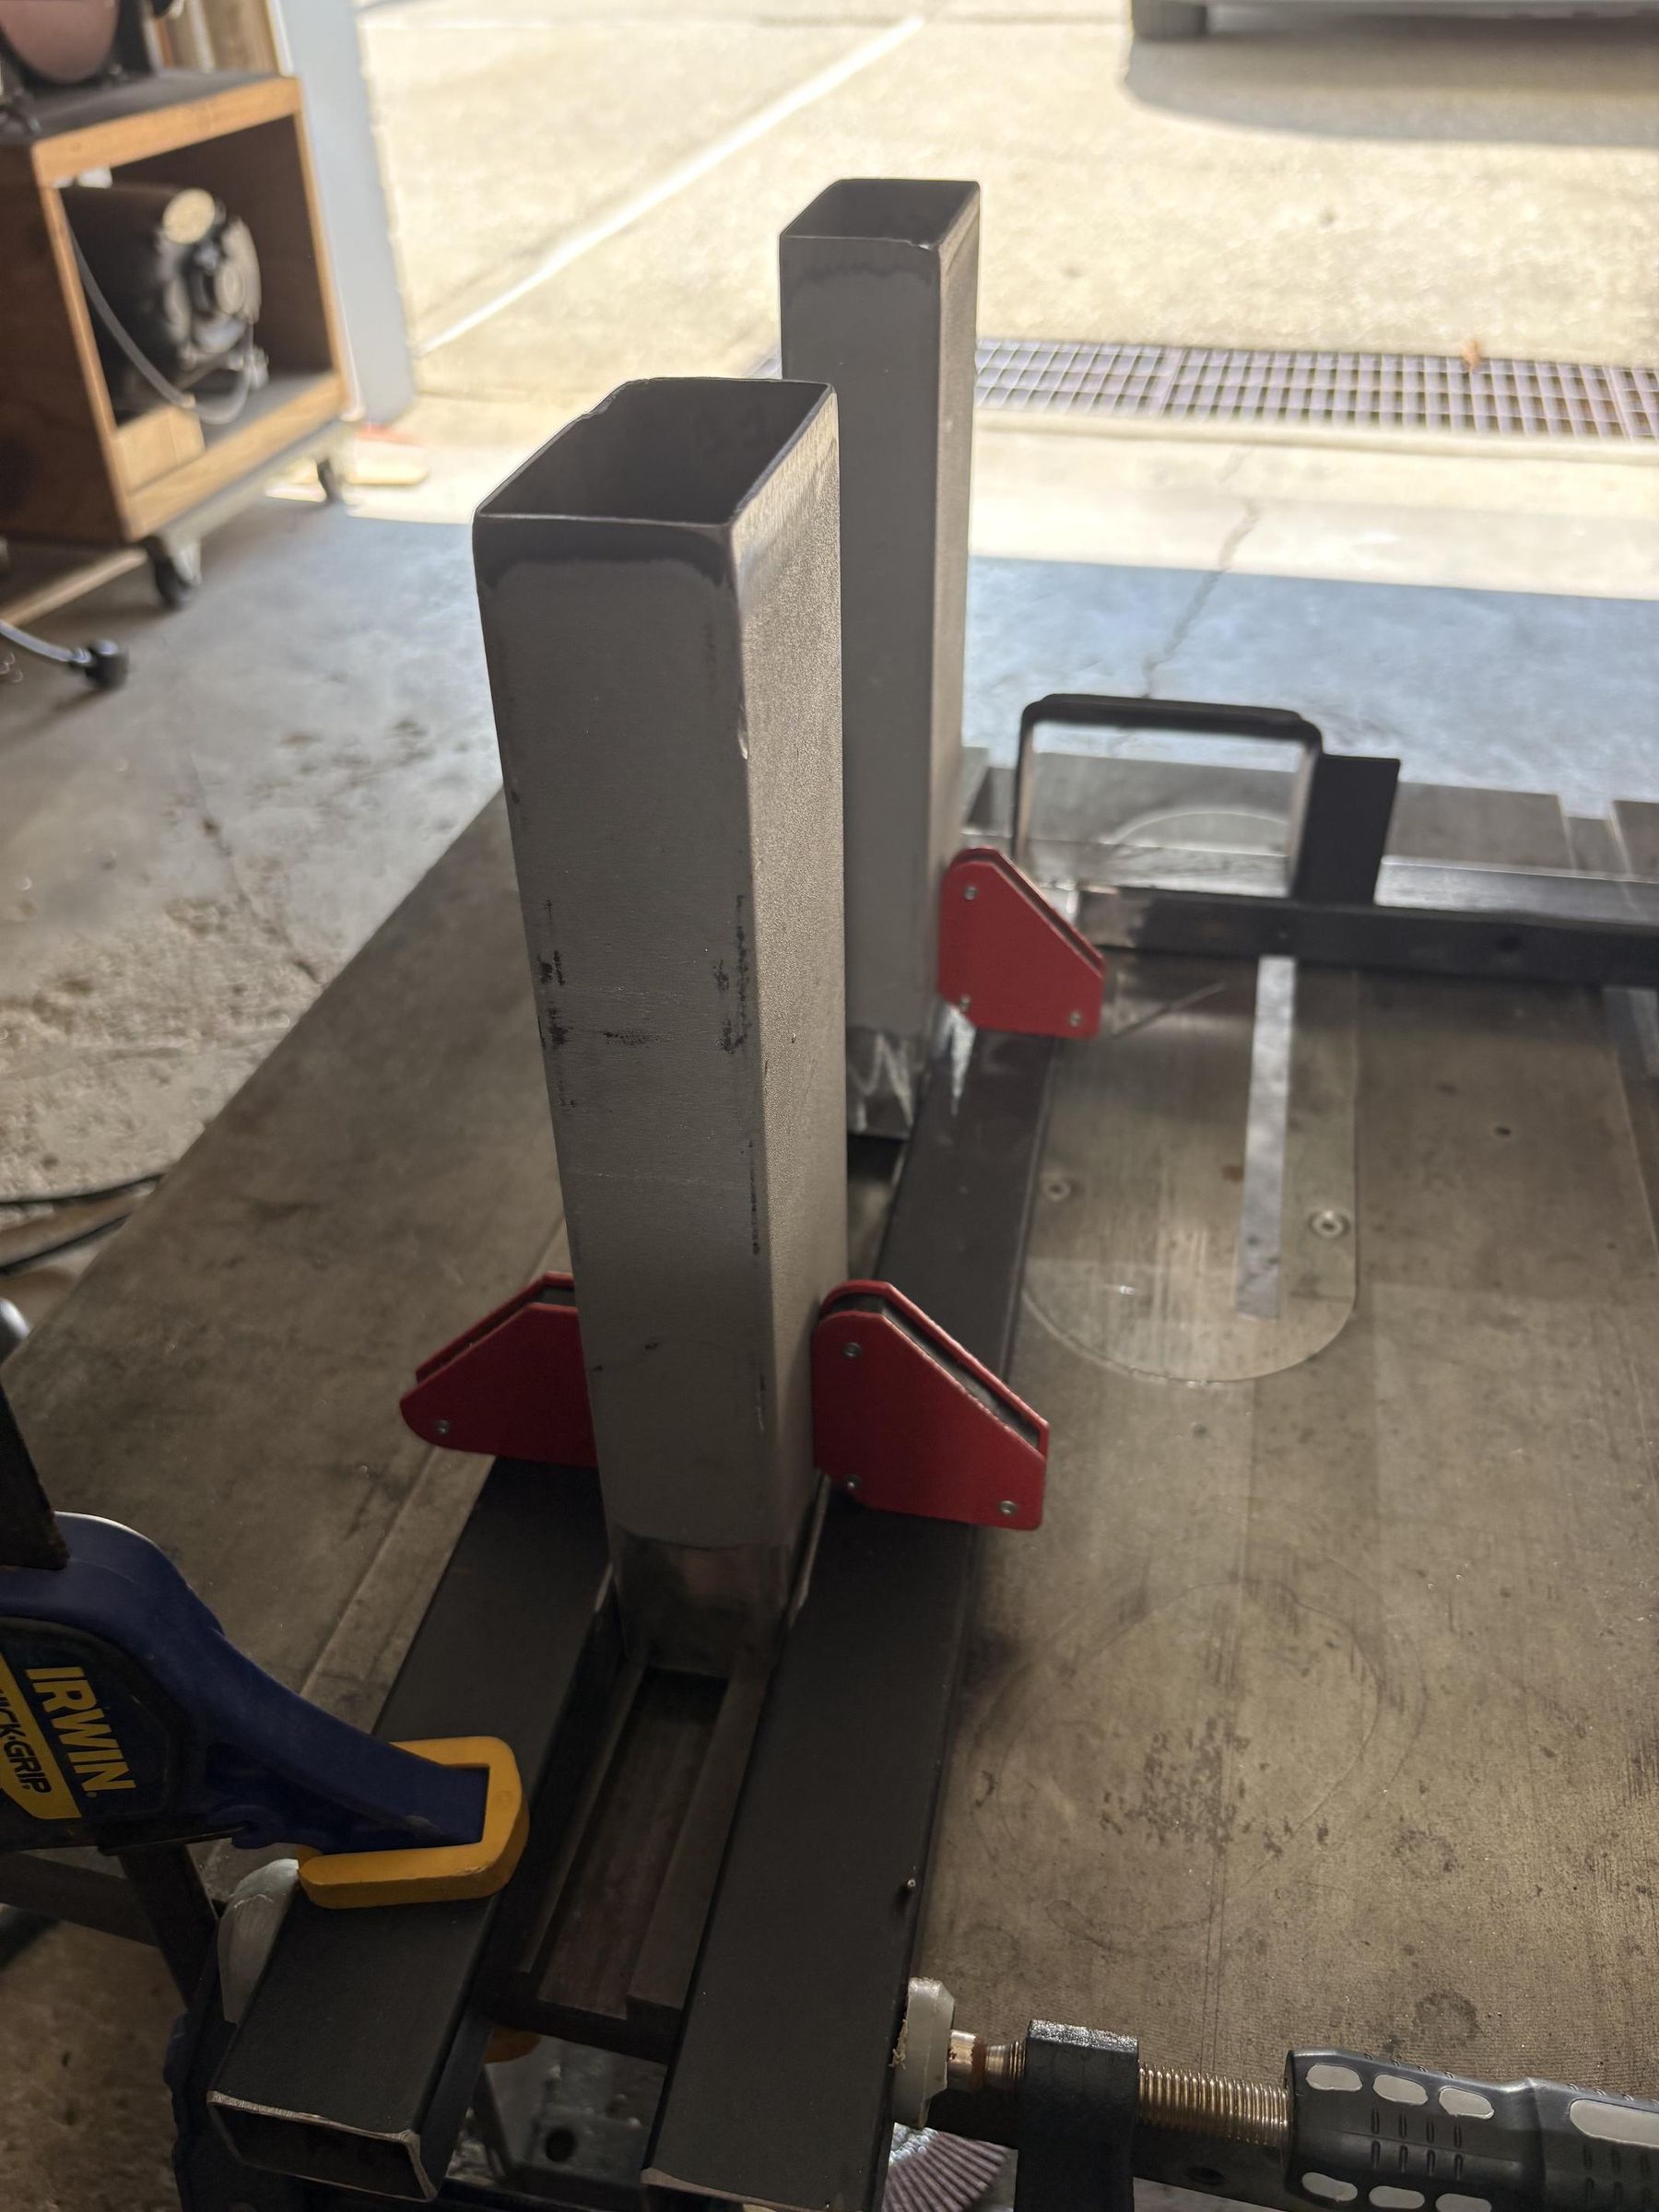
With all the pieces cut & "dry fit" (pic 6), it was time for welding. I took a couple of off cuts, removed paint and gave it a test weld to make sure it was penetrating sufficiently without blowing through the steel (pic 5). I kept my broken table saw (R.I.P.) bed to act as my "welding table" for this exact project in mind and it worked well (pic 7).
<Sigh> I have to mention that I am not a classically trained welder and so take this next part with a grain of salt. My flux core DCEN welder was set for 0.07-inch steel in mind, targeting 60 Amps with 0.03-inch flux core wire.
I prepped the frame by grinding to bare metal, tack welding, constantly removing slag and grinding, when necessary. I also put some 45-degree gussets (supports) to help with the inevitable vibration to come when operating. Starting with tacking and checking for square, I ran full beads around all the supporting metal. Tacking alone may lead to failure down the road.
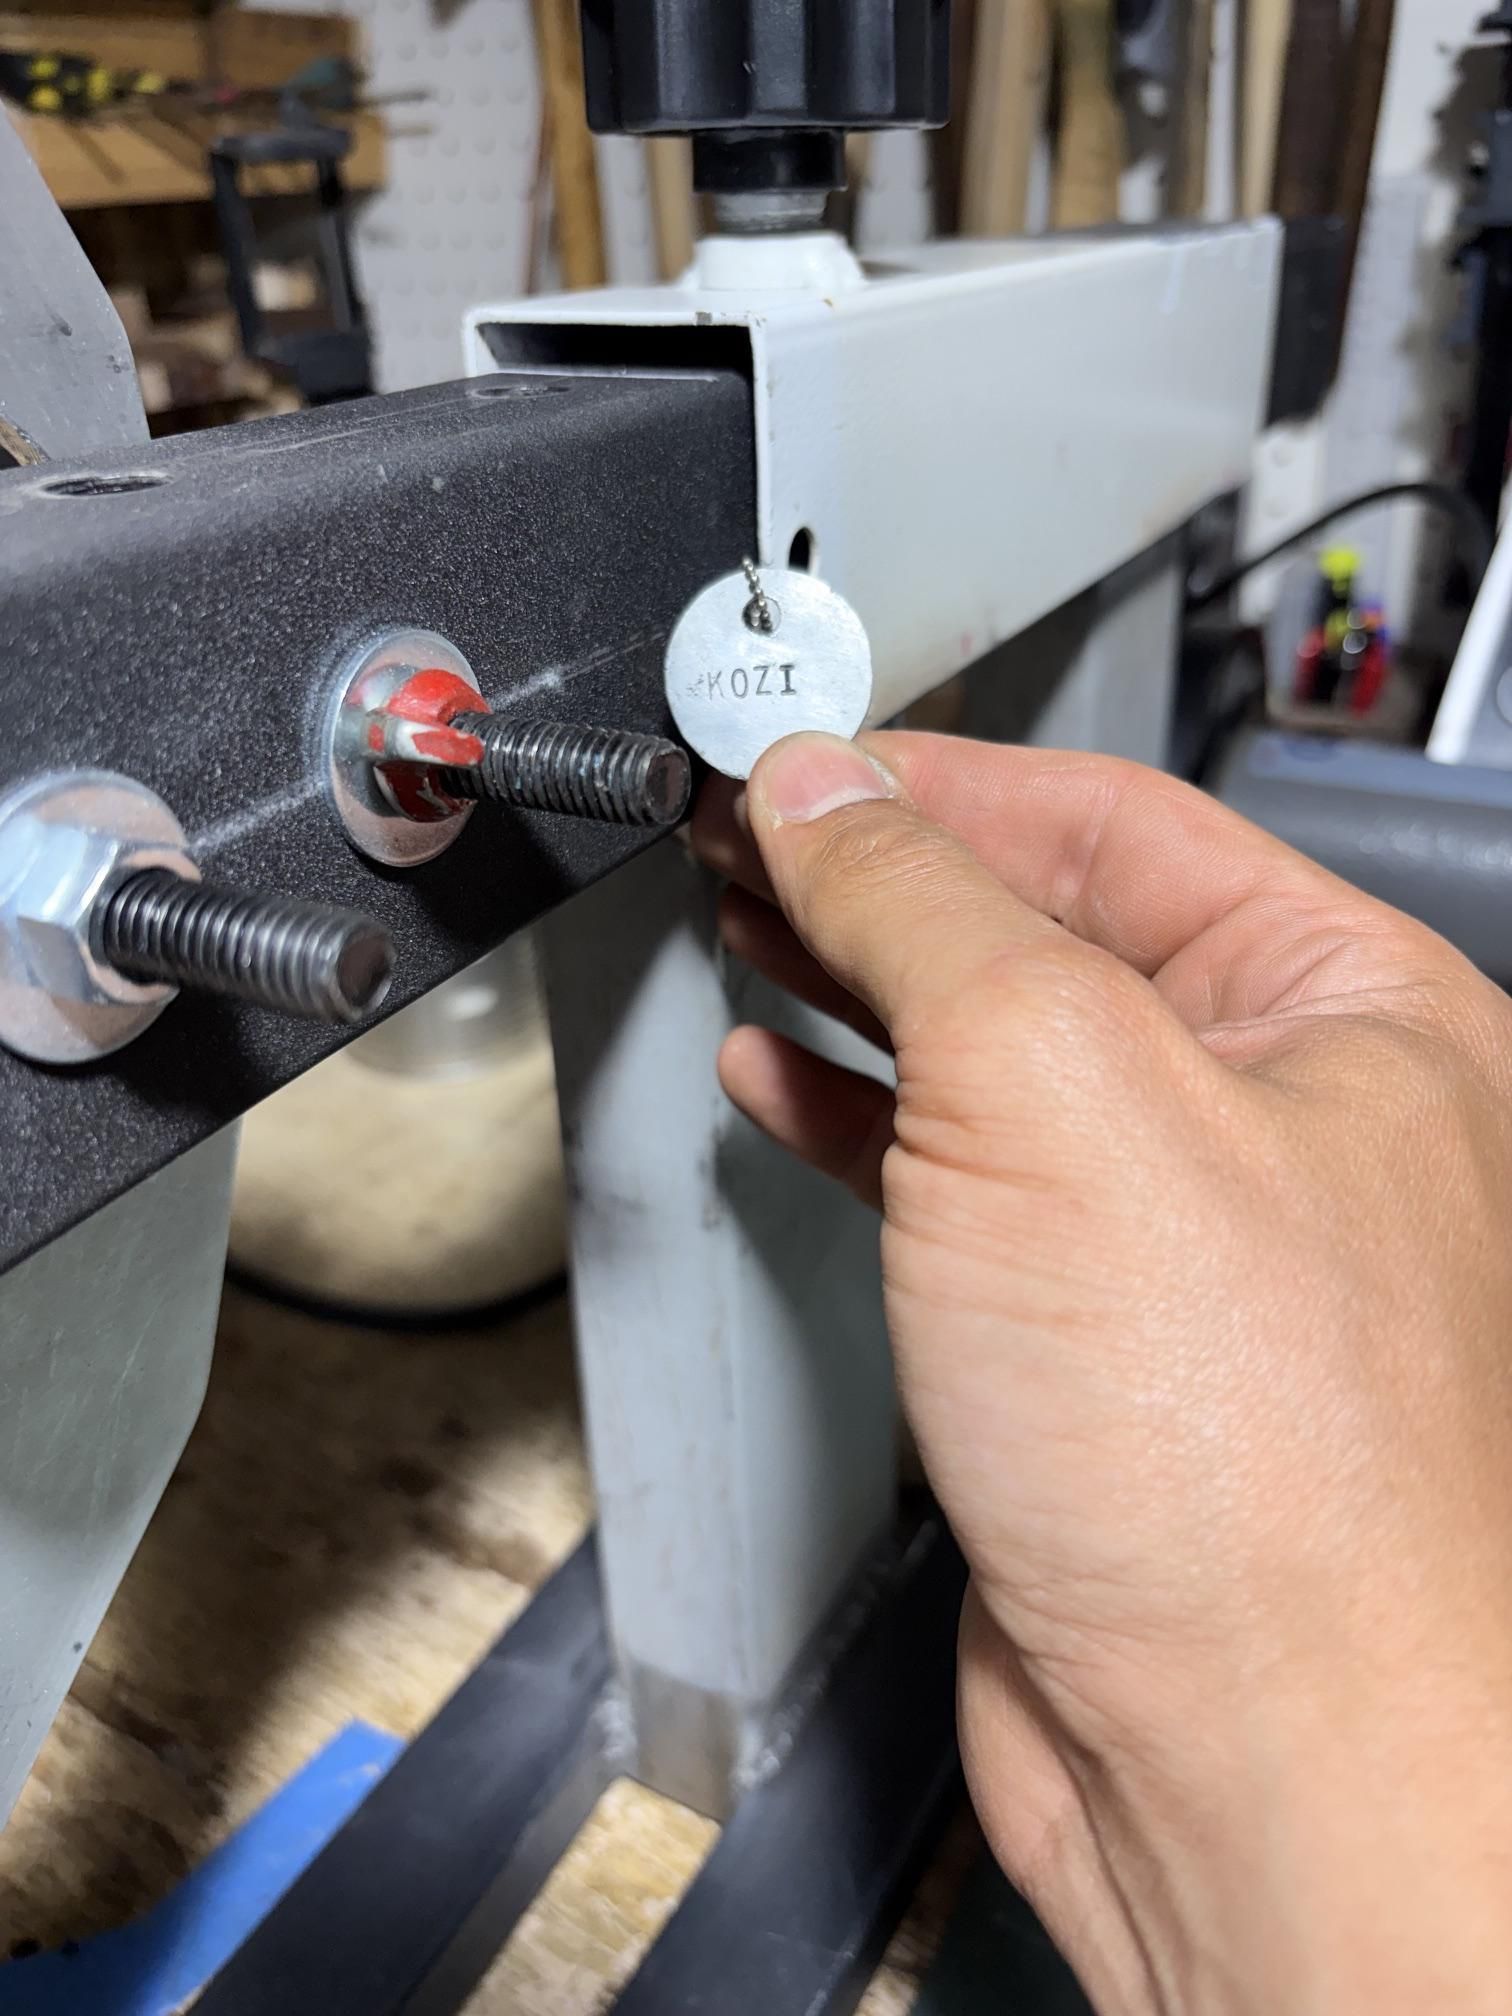
With the base complete (pics 12-13) I stuck my stamp of approval on it (pic 14)!
Treadmill Flywheel Hub Wheel - Thingy



I kept the flywheel attached to the treadmill motor knowing that this helps cool it while operating for long periods of time. The original belt hub attached to the treadmill flywheel, for me, was 34-mm in diameter and 30 mm long. I went metric to help keep the dimensions straight in my mind. This is only the straight section up to the lip of the weld where it meets the flat flywheel (hopefully that makes sense). I wanted to keep that "lip" in my measurements to help align the frame but also the sanding belt later on.
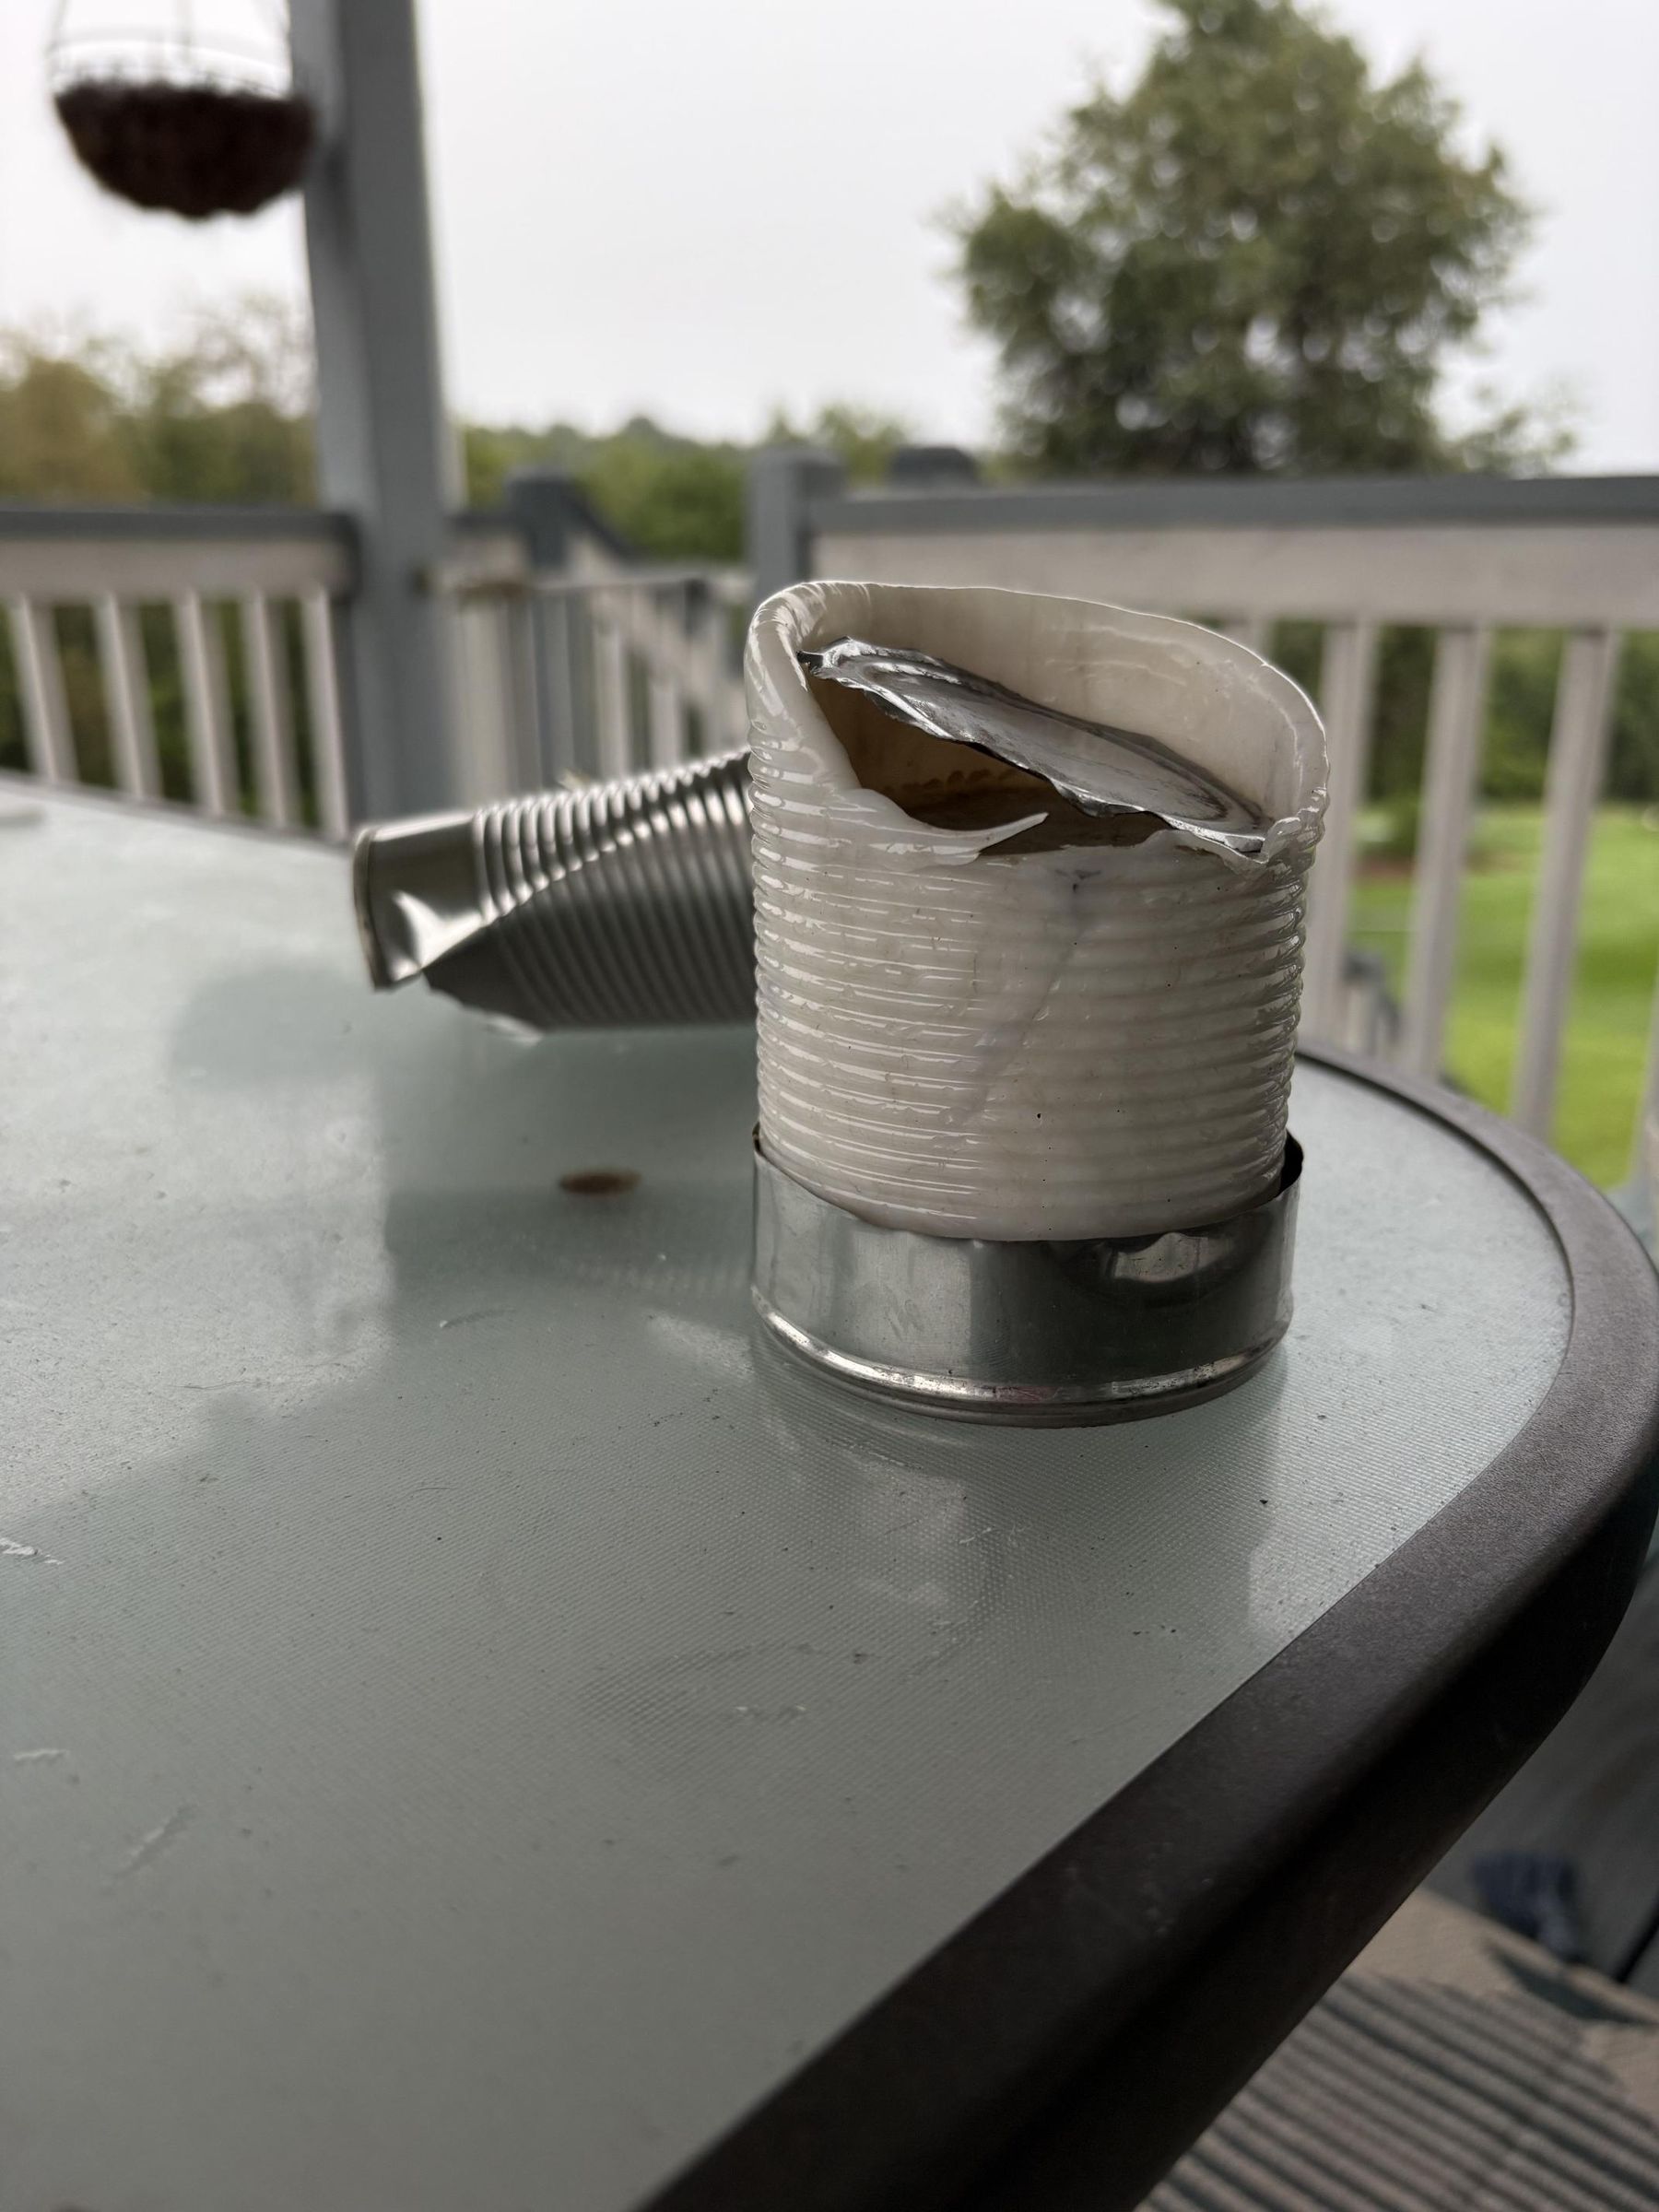
However, I needed a proper contact wheel so I made my own out of recycled HDPE water jugs (pic 1-3). Using a soup can as my mold since it measured 3-inches in diameter, I melted and stuffed ~300 grams of shredded HDPE in it (pic 1).
I used my DIY hydraulic press (link HERE) to help ensure there were absolutely NO air bubbles!
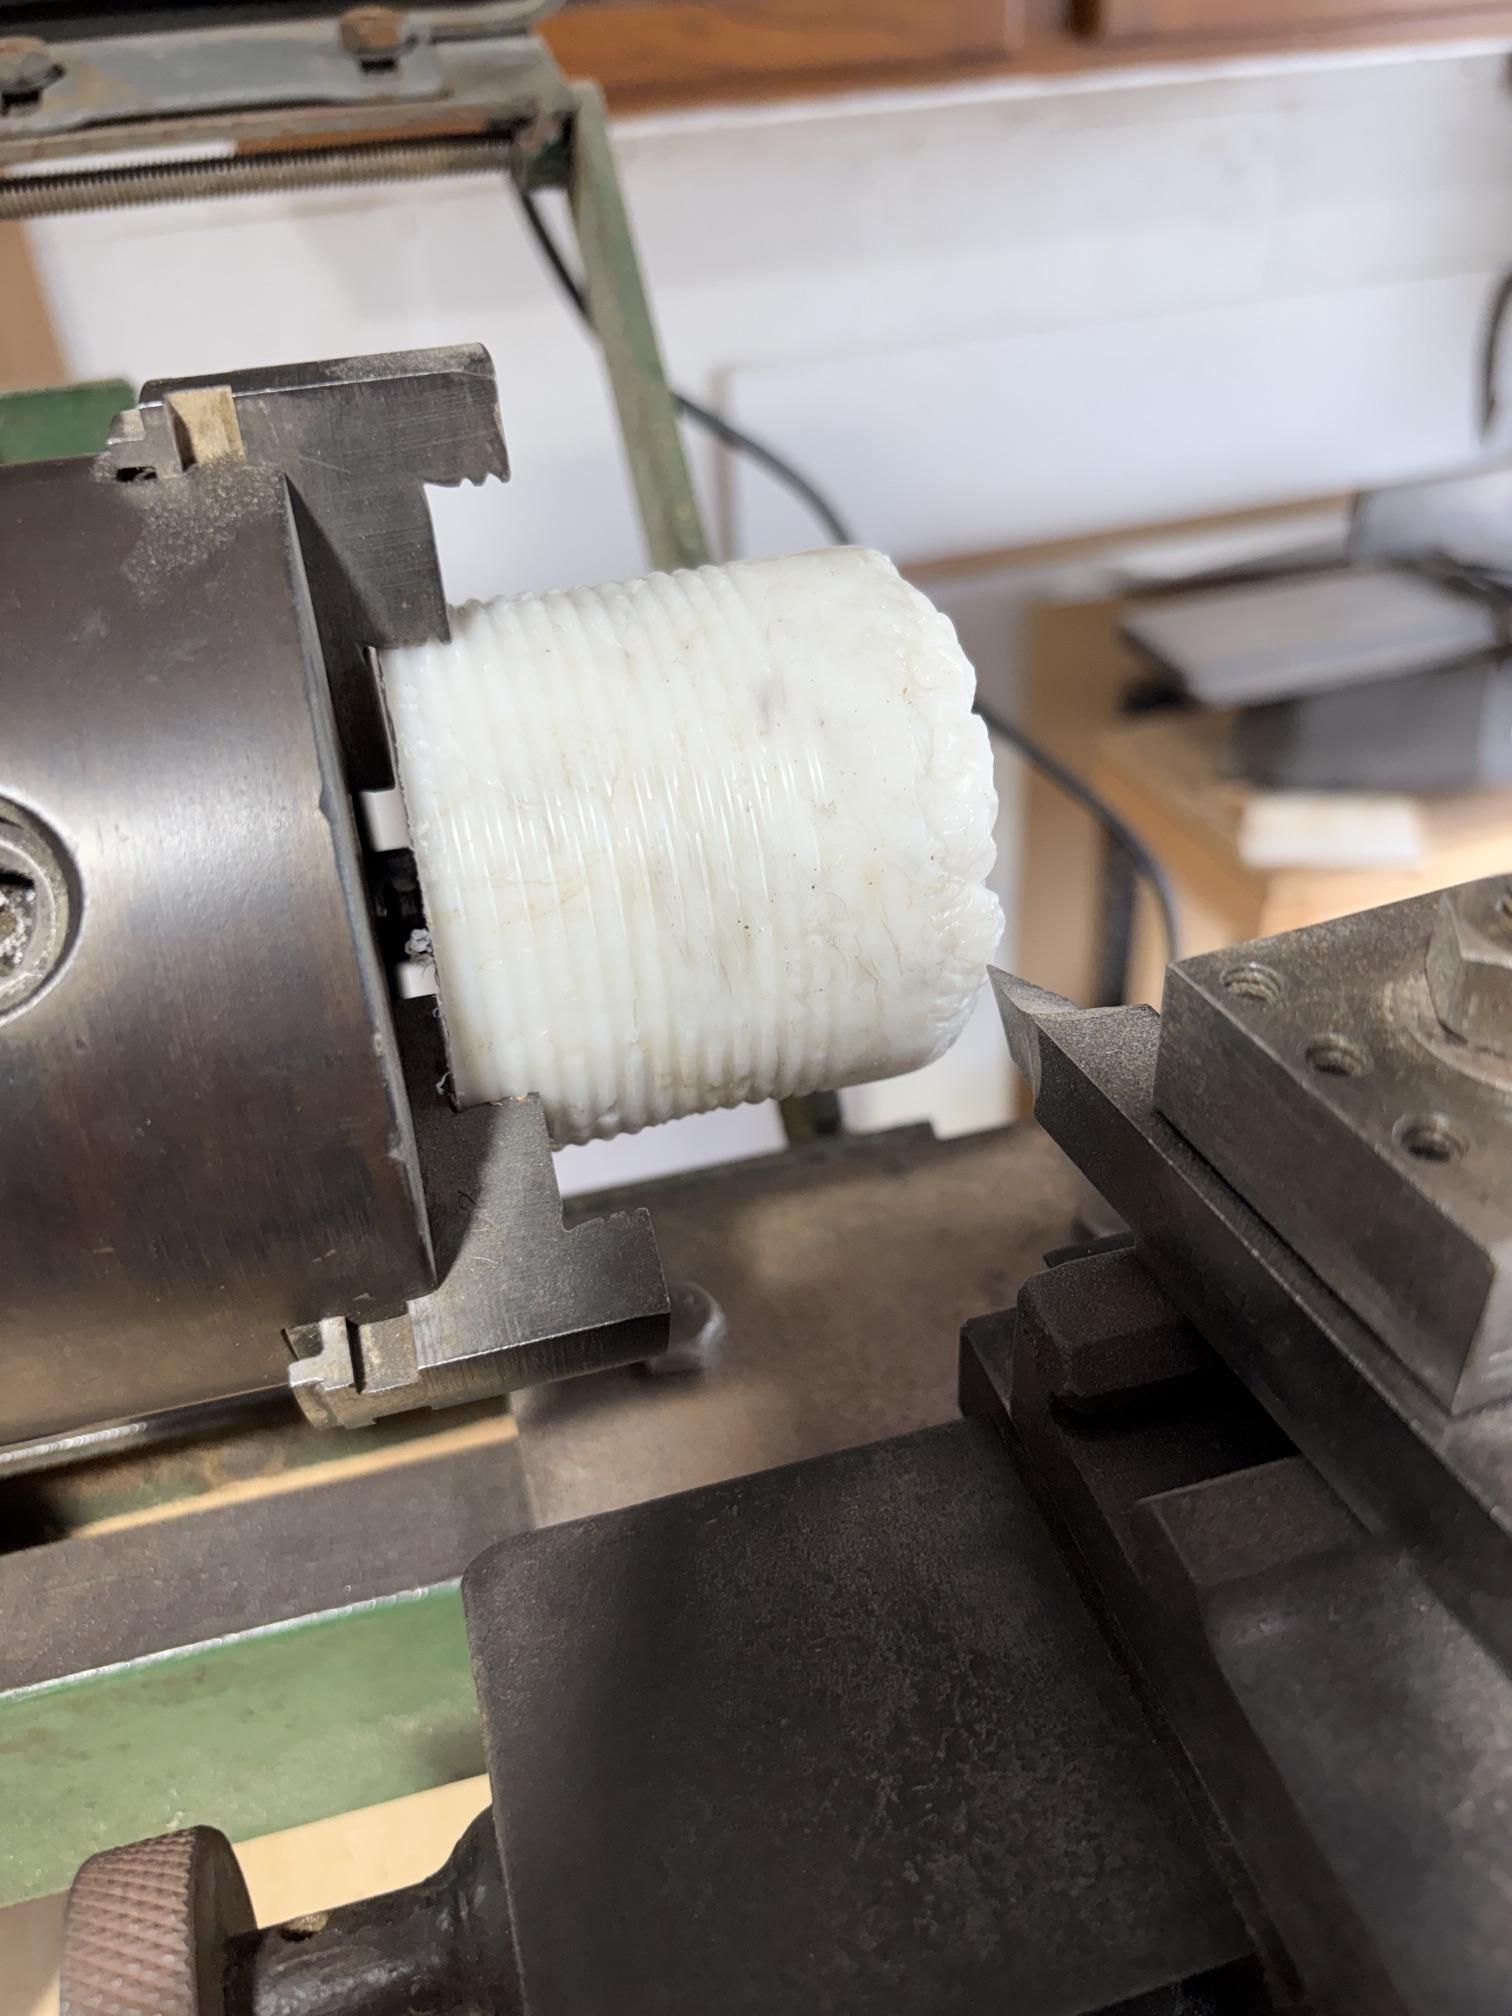
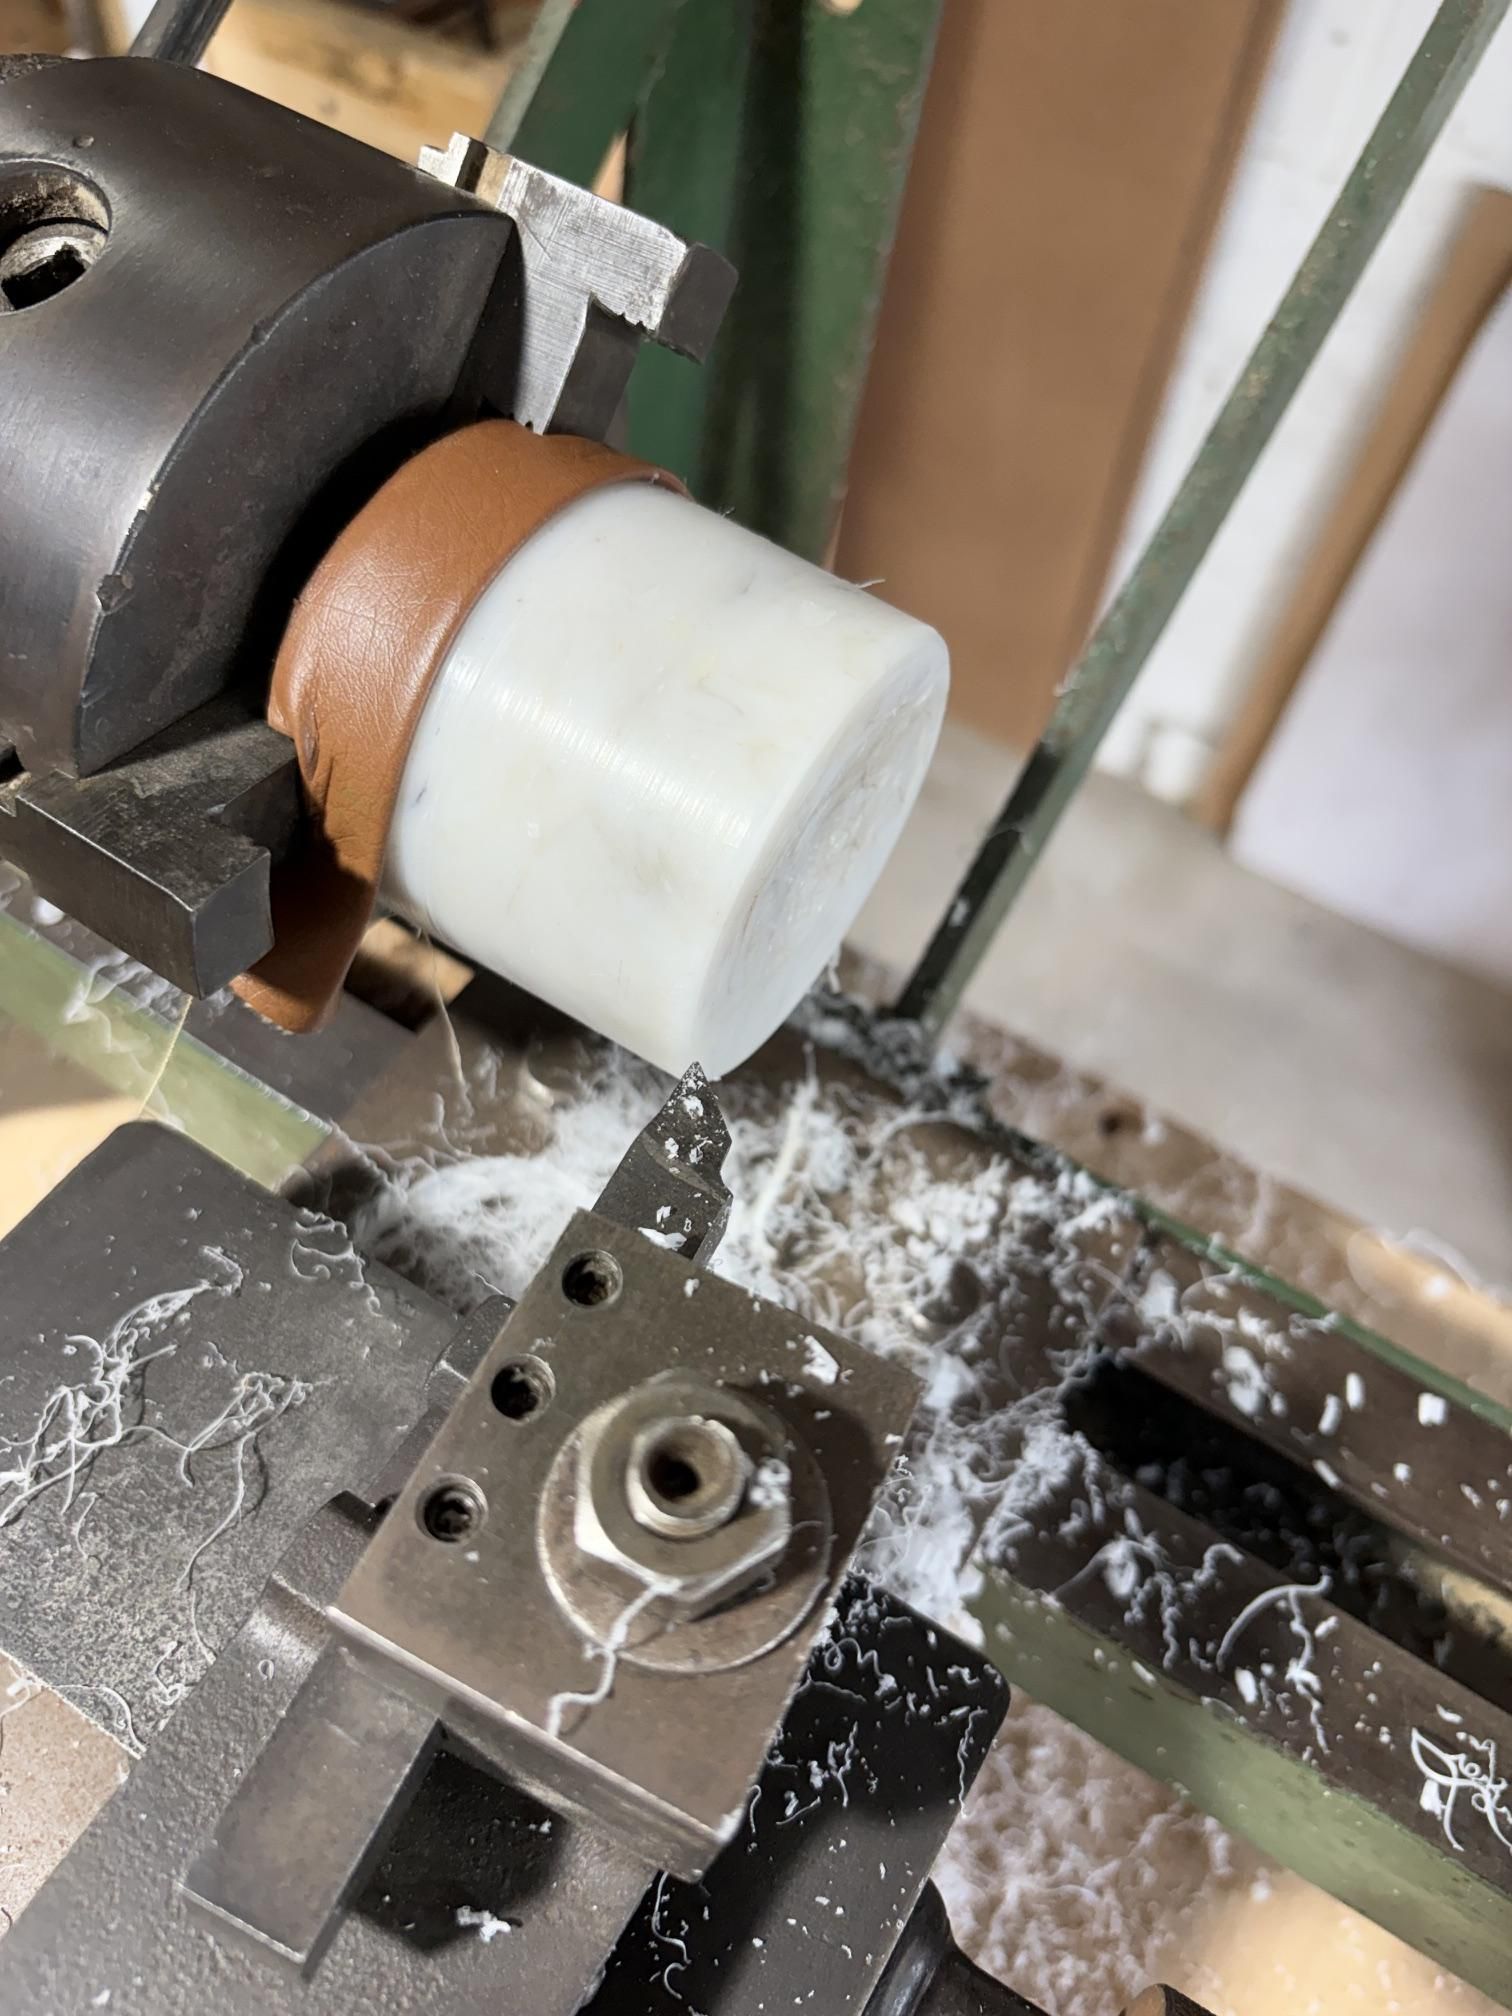
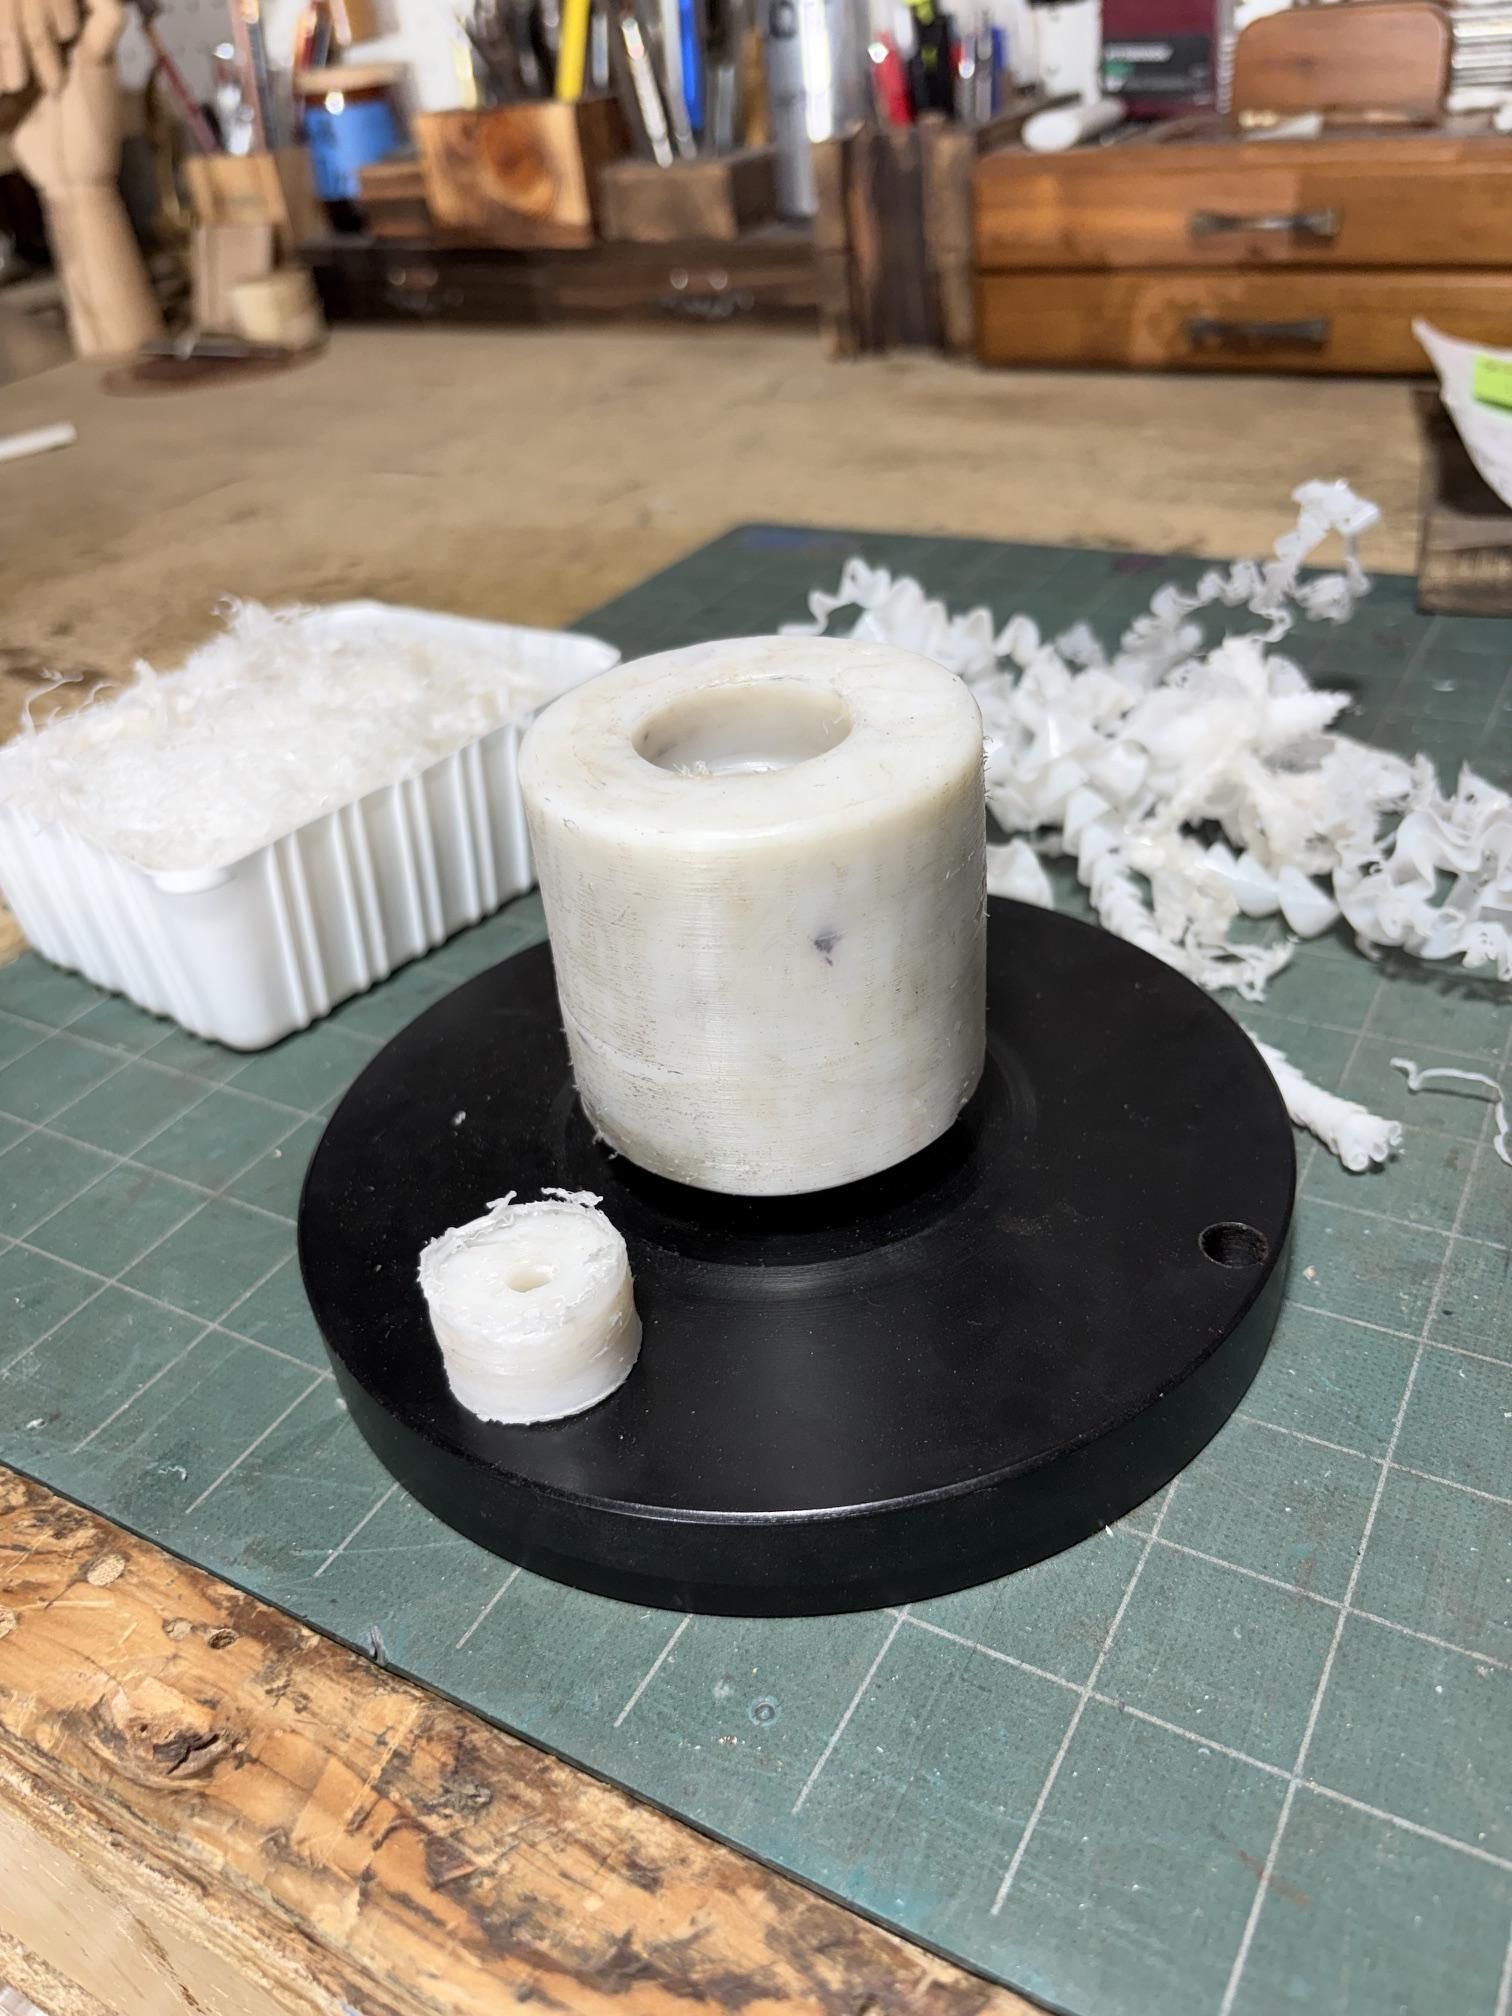
I let it cool overnight and released it from the can (pic 2). The block looked great but needed to be cleaned up on the lathe (pic 4 & 5). Being "soft" HDPE, I used my lathe tools to even out the sides and the faces as much as possible to help reduce unwanted vibration during operation. I wound up with a cylinder roughly 2 1/2-inches tall and 2 3/4-inches in diameter.
"Kozi, I don't have a lathe..." Good point! If you don't have a lathe just use your 5-axis CNC. Just kidding. You can drill out your hole to mount the wheel and using a drill and a file while the trigger is taped down. Get creative. It is fun to problem solve when faced with restrictions. IMO.
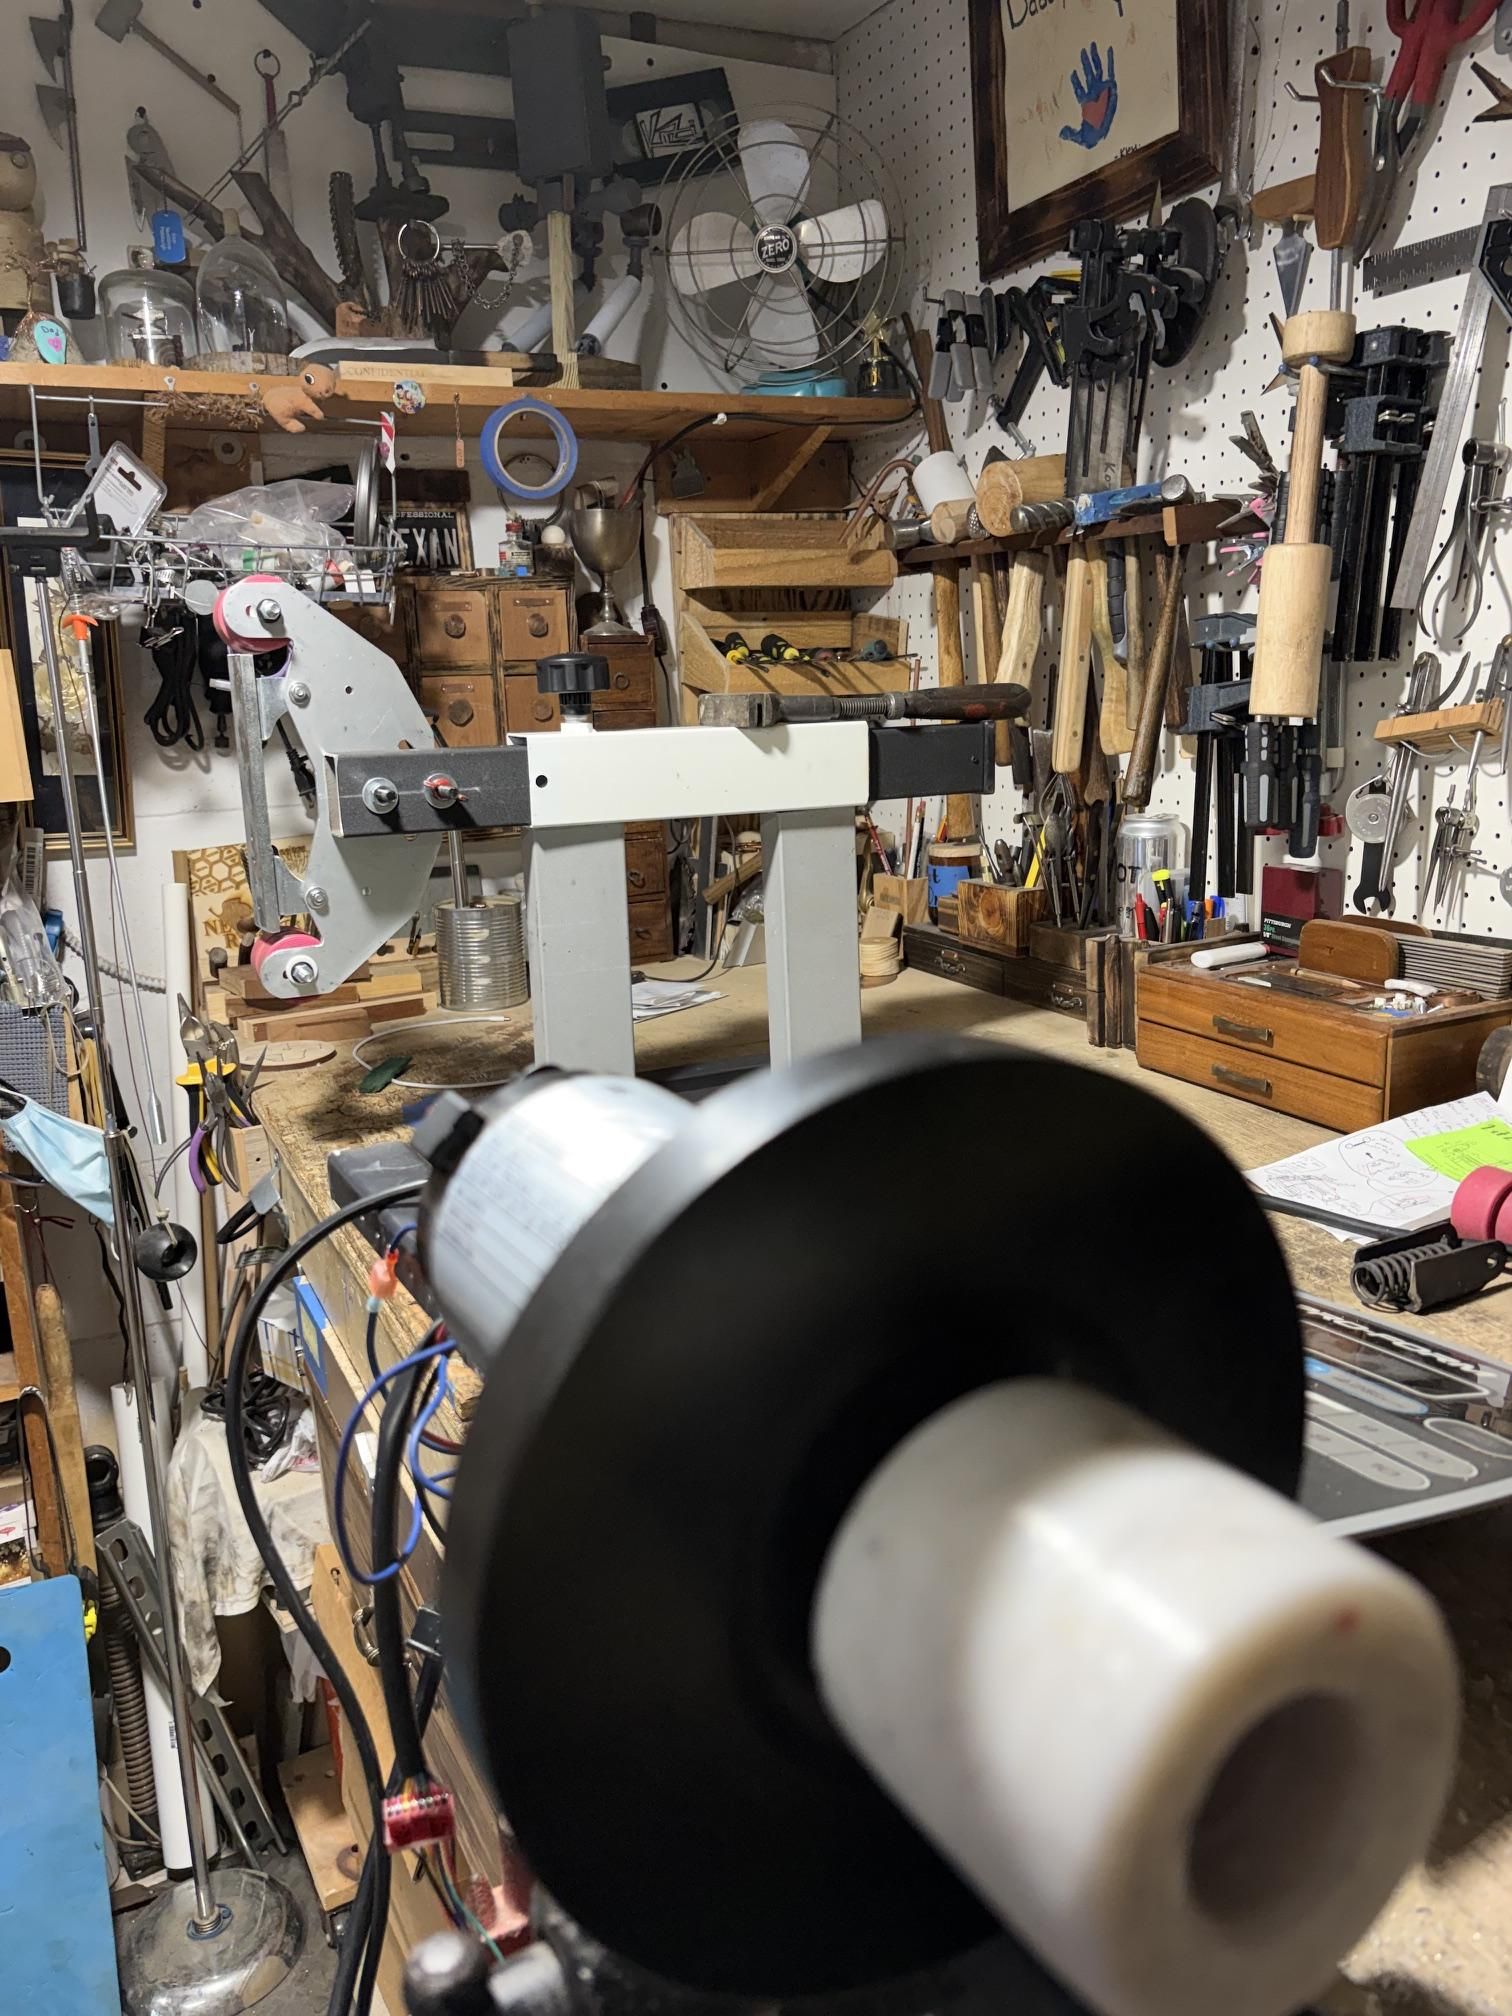
Knowing the dimensions of the flywheel belt hub (and the fact that it was "ribbed") helped me press fit my HDPE wheel. I had to drill the recess (pic 6) and attempt to hammer it into place but the clearance was really tight, even for HDPE. I used my plastic press again to get it the rest of the way (pic 7 & 8). I should have just used what I had to begin with... Hammering would have worked but it would have taken longer and more sweat.
Tension Arm


At this point, I put all the pieces I had together to:
- bask in my glory so far, but
- I needed to know how tall to make my tension arm, and how..??
I saw a lot of options but I needed to keep in mind the crown of the wheel that would help with tracking and, once again, alignment.
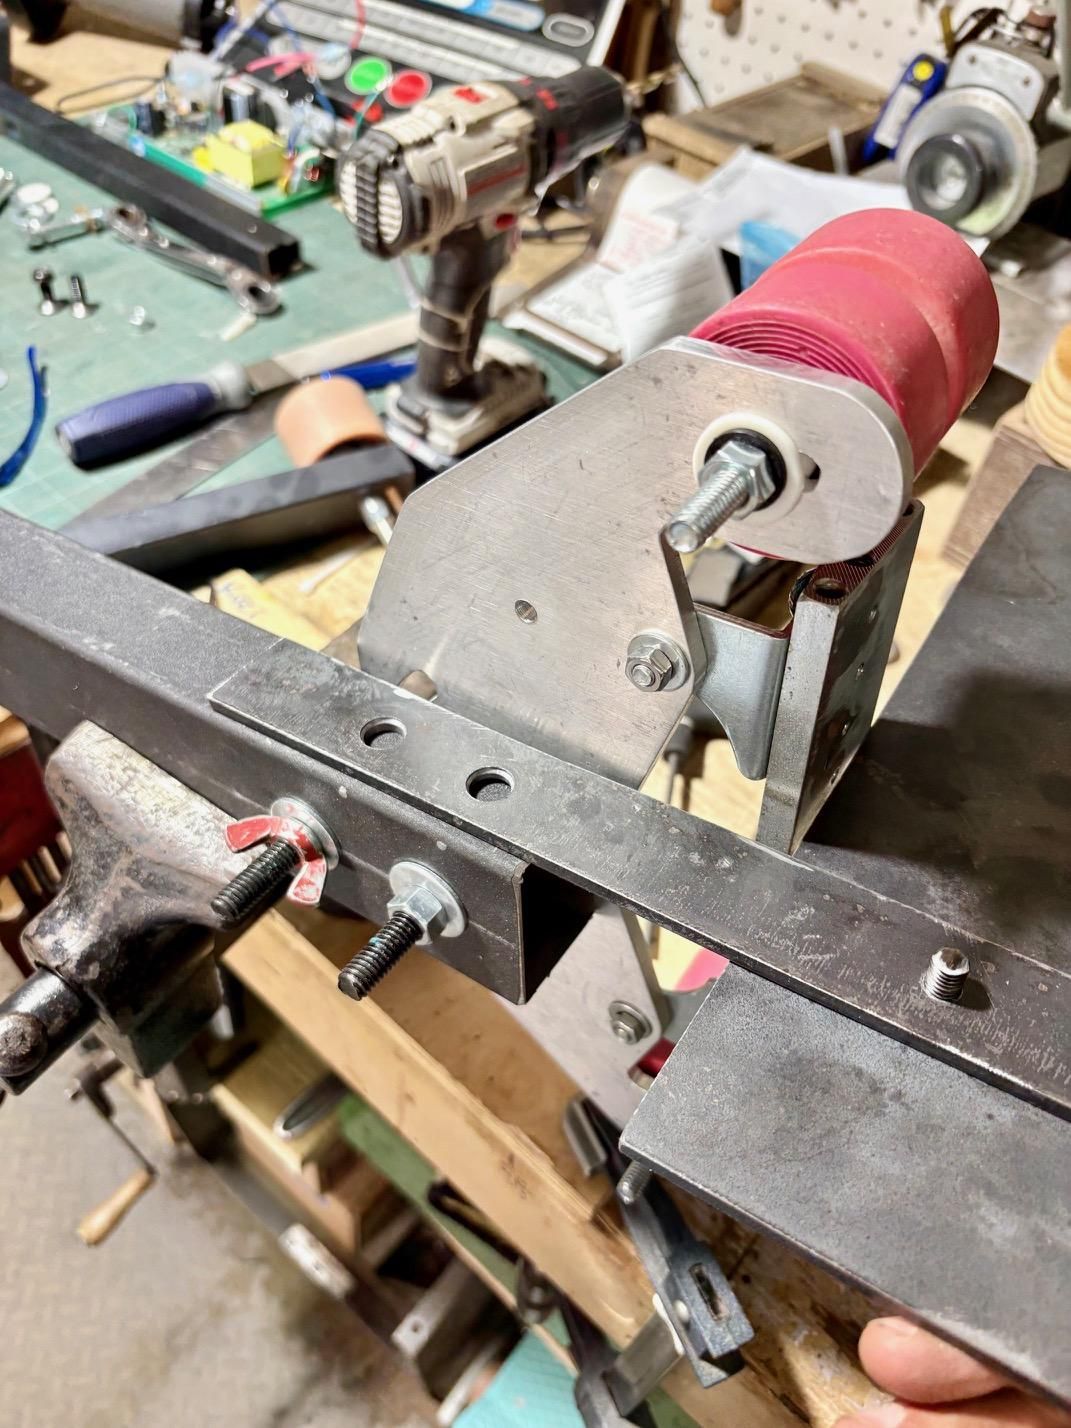
I figured out that I needed to good and buy a 3 1/8-inch gate extension spring to mount to the frame as well as the arm (see pic 1 & 2). Since this would be stretched, the spring action would keep tension needed on the belt.
I used another piece of the silver treadmill frame ultimately cut to 7-inches & 60-degree angles (pic 1). I chose this because the measurement from the top of the tooling arm to the center of where the crown wheel will go was about 8-inches. Angling this would force the 12-inch long 1x1.5-inch black frame arm to be angled upwards to keep tension but also allow for quick belt change outs (pic 2 & 3). Recesses in the silver angle were also removed via the angle grinder and filed to remove the rough edges (pic 1-2).
One of the complaints I have with my 1x42 belt sander is that changing the belts requires the work rest to be removed and re-squared...every time... I don't have the patience for that.
The silver support was welded and modified to allow the 1x1.5 black frame to be bolted on. Holes were drilled for the spring and for the crown wheel to be attached via a common hinge to allow for tracking the belt.
My advice for the tracking lever: Don't get summit fever.
This was one of the last things [I thought] I had to do and drilled way too many ancillary holes than needed. Seriously, my hinge looks like Swiss cheese and is easily the ugliest component on my grinder...
Tool Bed




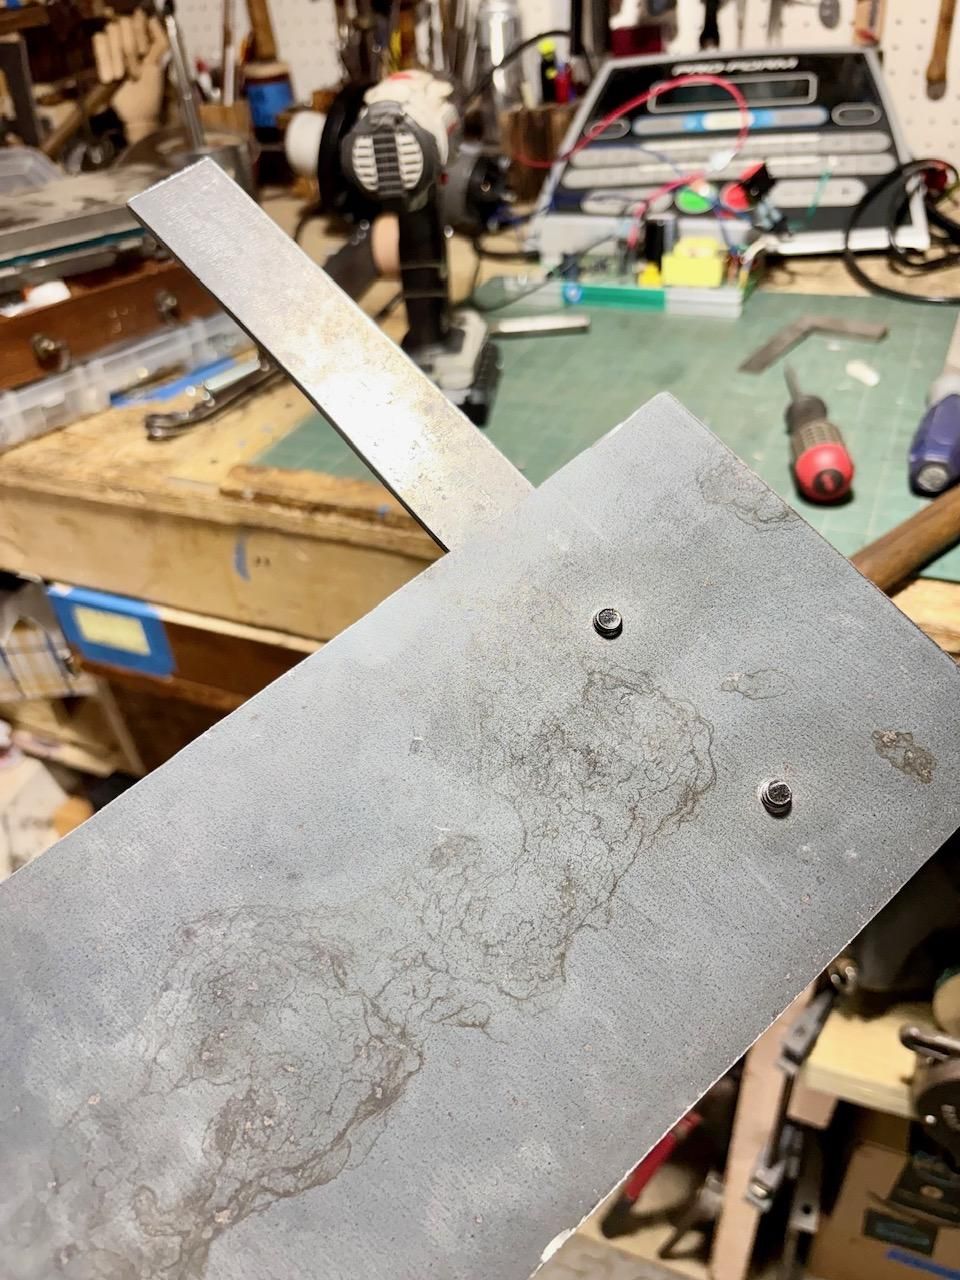
I need a tool rest and just so happened to have some 12-inch x 12-inch A36 steel plate just lying around (pic 1).
Full disclosure: I called around to a lot of different fabricators for cut offs / scrap and none were willing to help. They didn't really say why when prompted but I won my plate from auction so ce la vie. I got lucky once again.
I decided to cut two parallel plates; one 1.5x12-inches to bolt underneath the tooling arm (pic 12) and the other 6x12-inches for the actual work rest (pic 2).
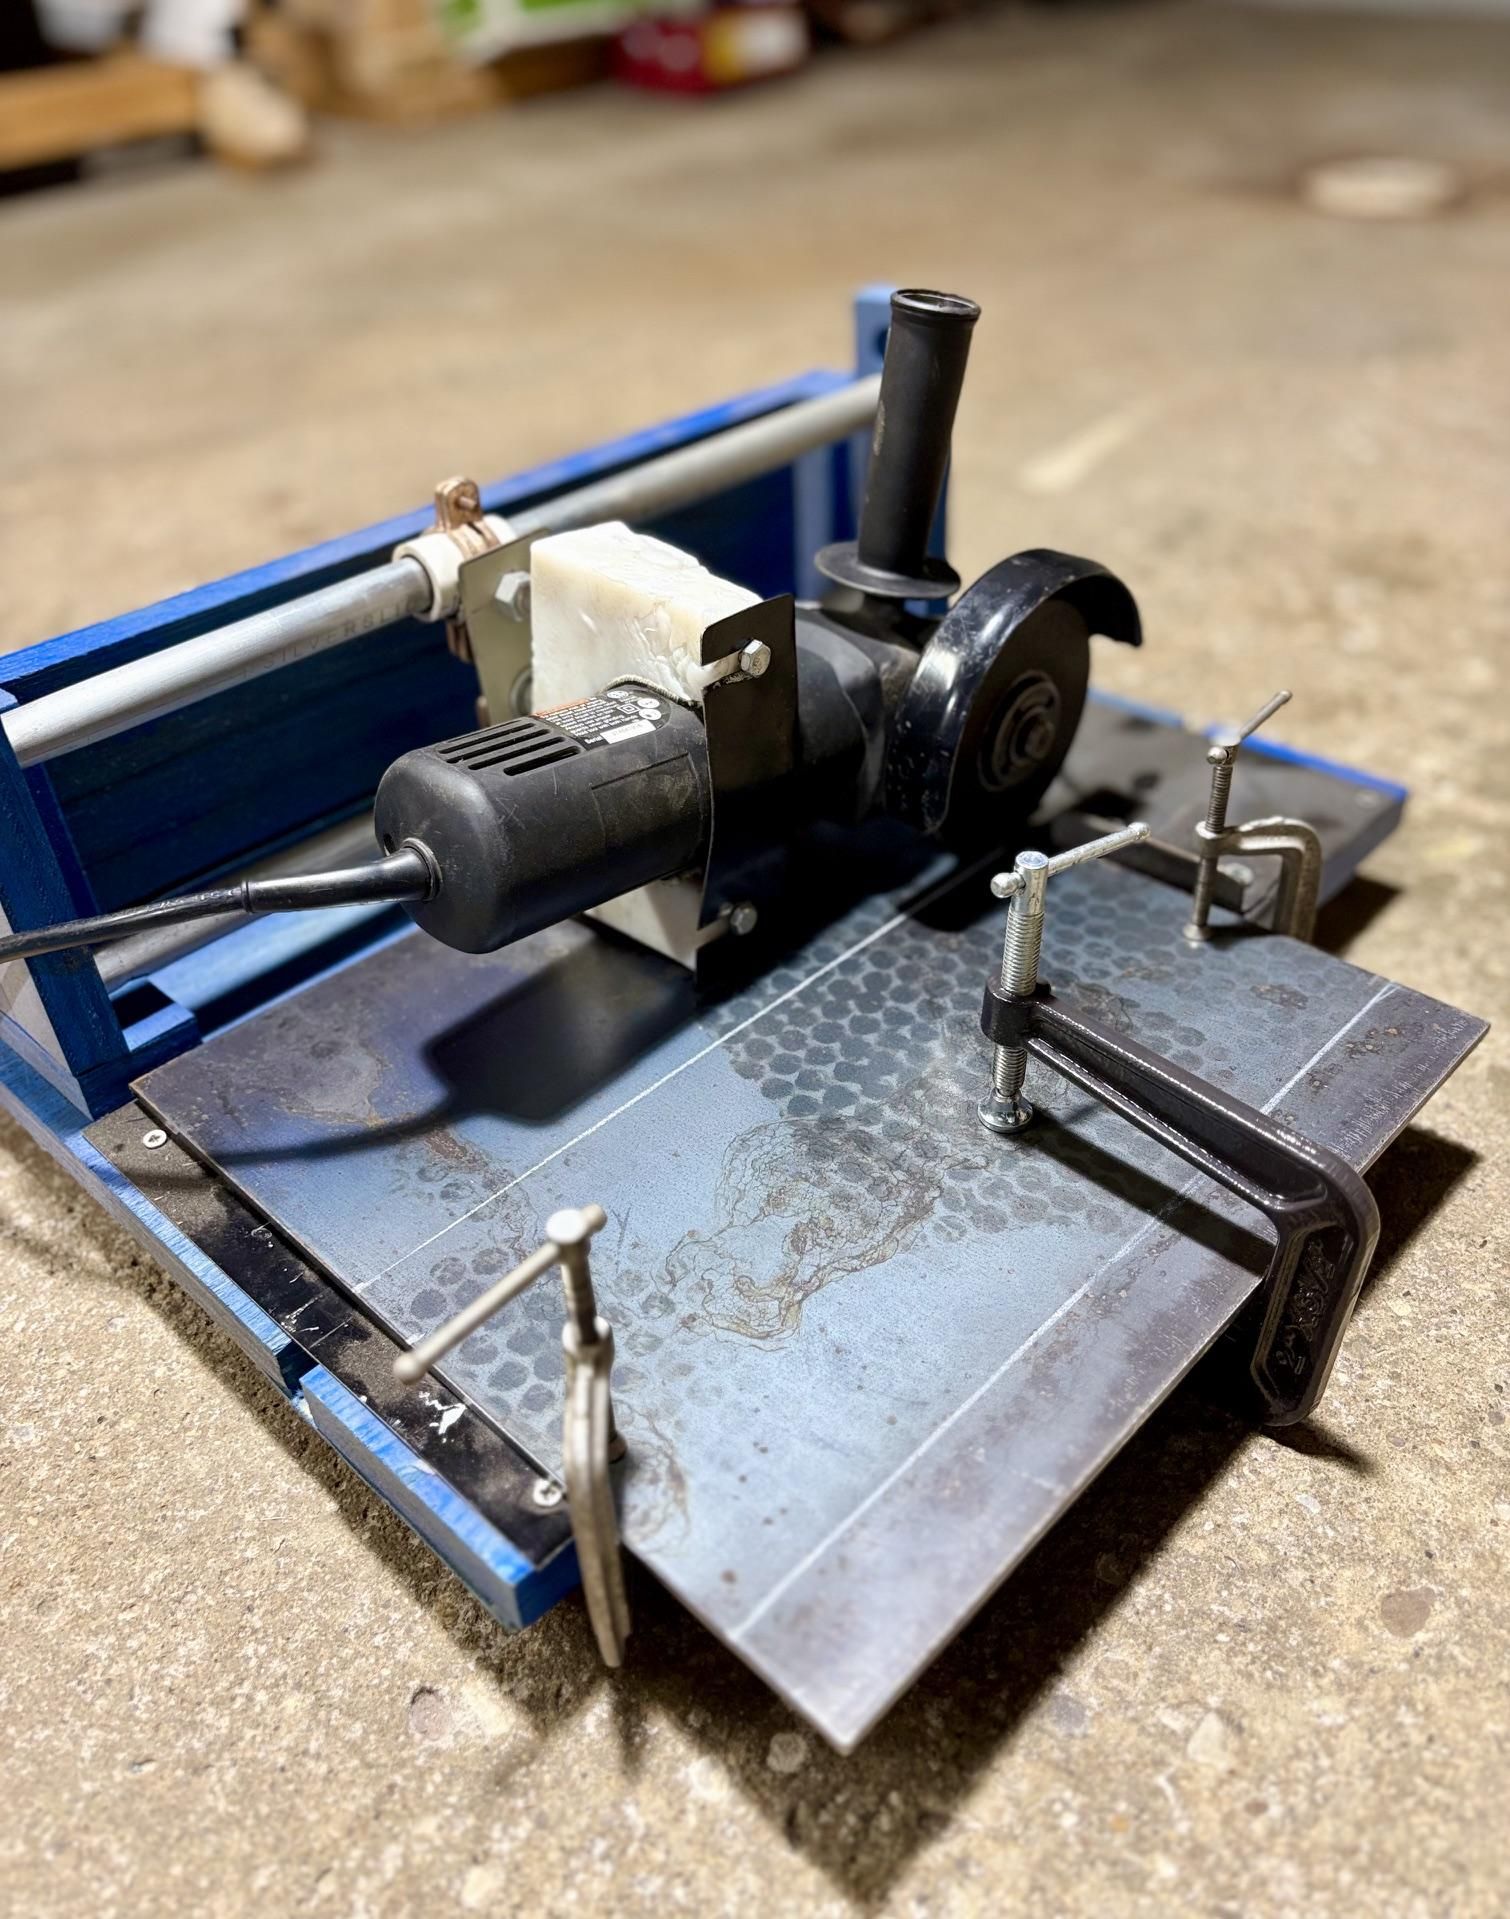
I am using my angle grinder jig (pic 3) to help me get as straight lines as possible (pic 4). Once I score the guide line, I did the rest by hand (pic 5). After removing the rough edges (pic 6), I lined everything up and drilled & tapped holes for mounting (pic 7-9).
Using the 1/2 turn followed by the 1/4 turn backwards to cut the threads and using plenty of lubrication, this wasn't nearly as daunting of a task as I thought (pic 9-10). Thankfully, didn't break any taps!
I will need to grind down the screws flat (pic 11) for the final product so they won't catch but still showing the process.
Paint Job


With the 2x72-inch belt sander almost done, I decided to give it a paint job to spiff it up a little. I chose my teal spray can to match other projects I have done.
I did go back and redo the black base. I didn't leave stray teal spray on the bottom as shown in the pics. Don't worry.
Failures & Final Tweaks
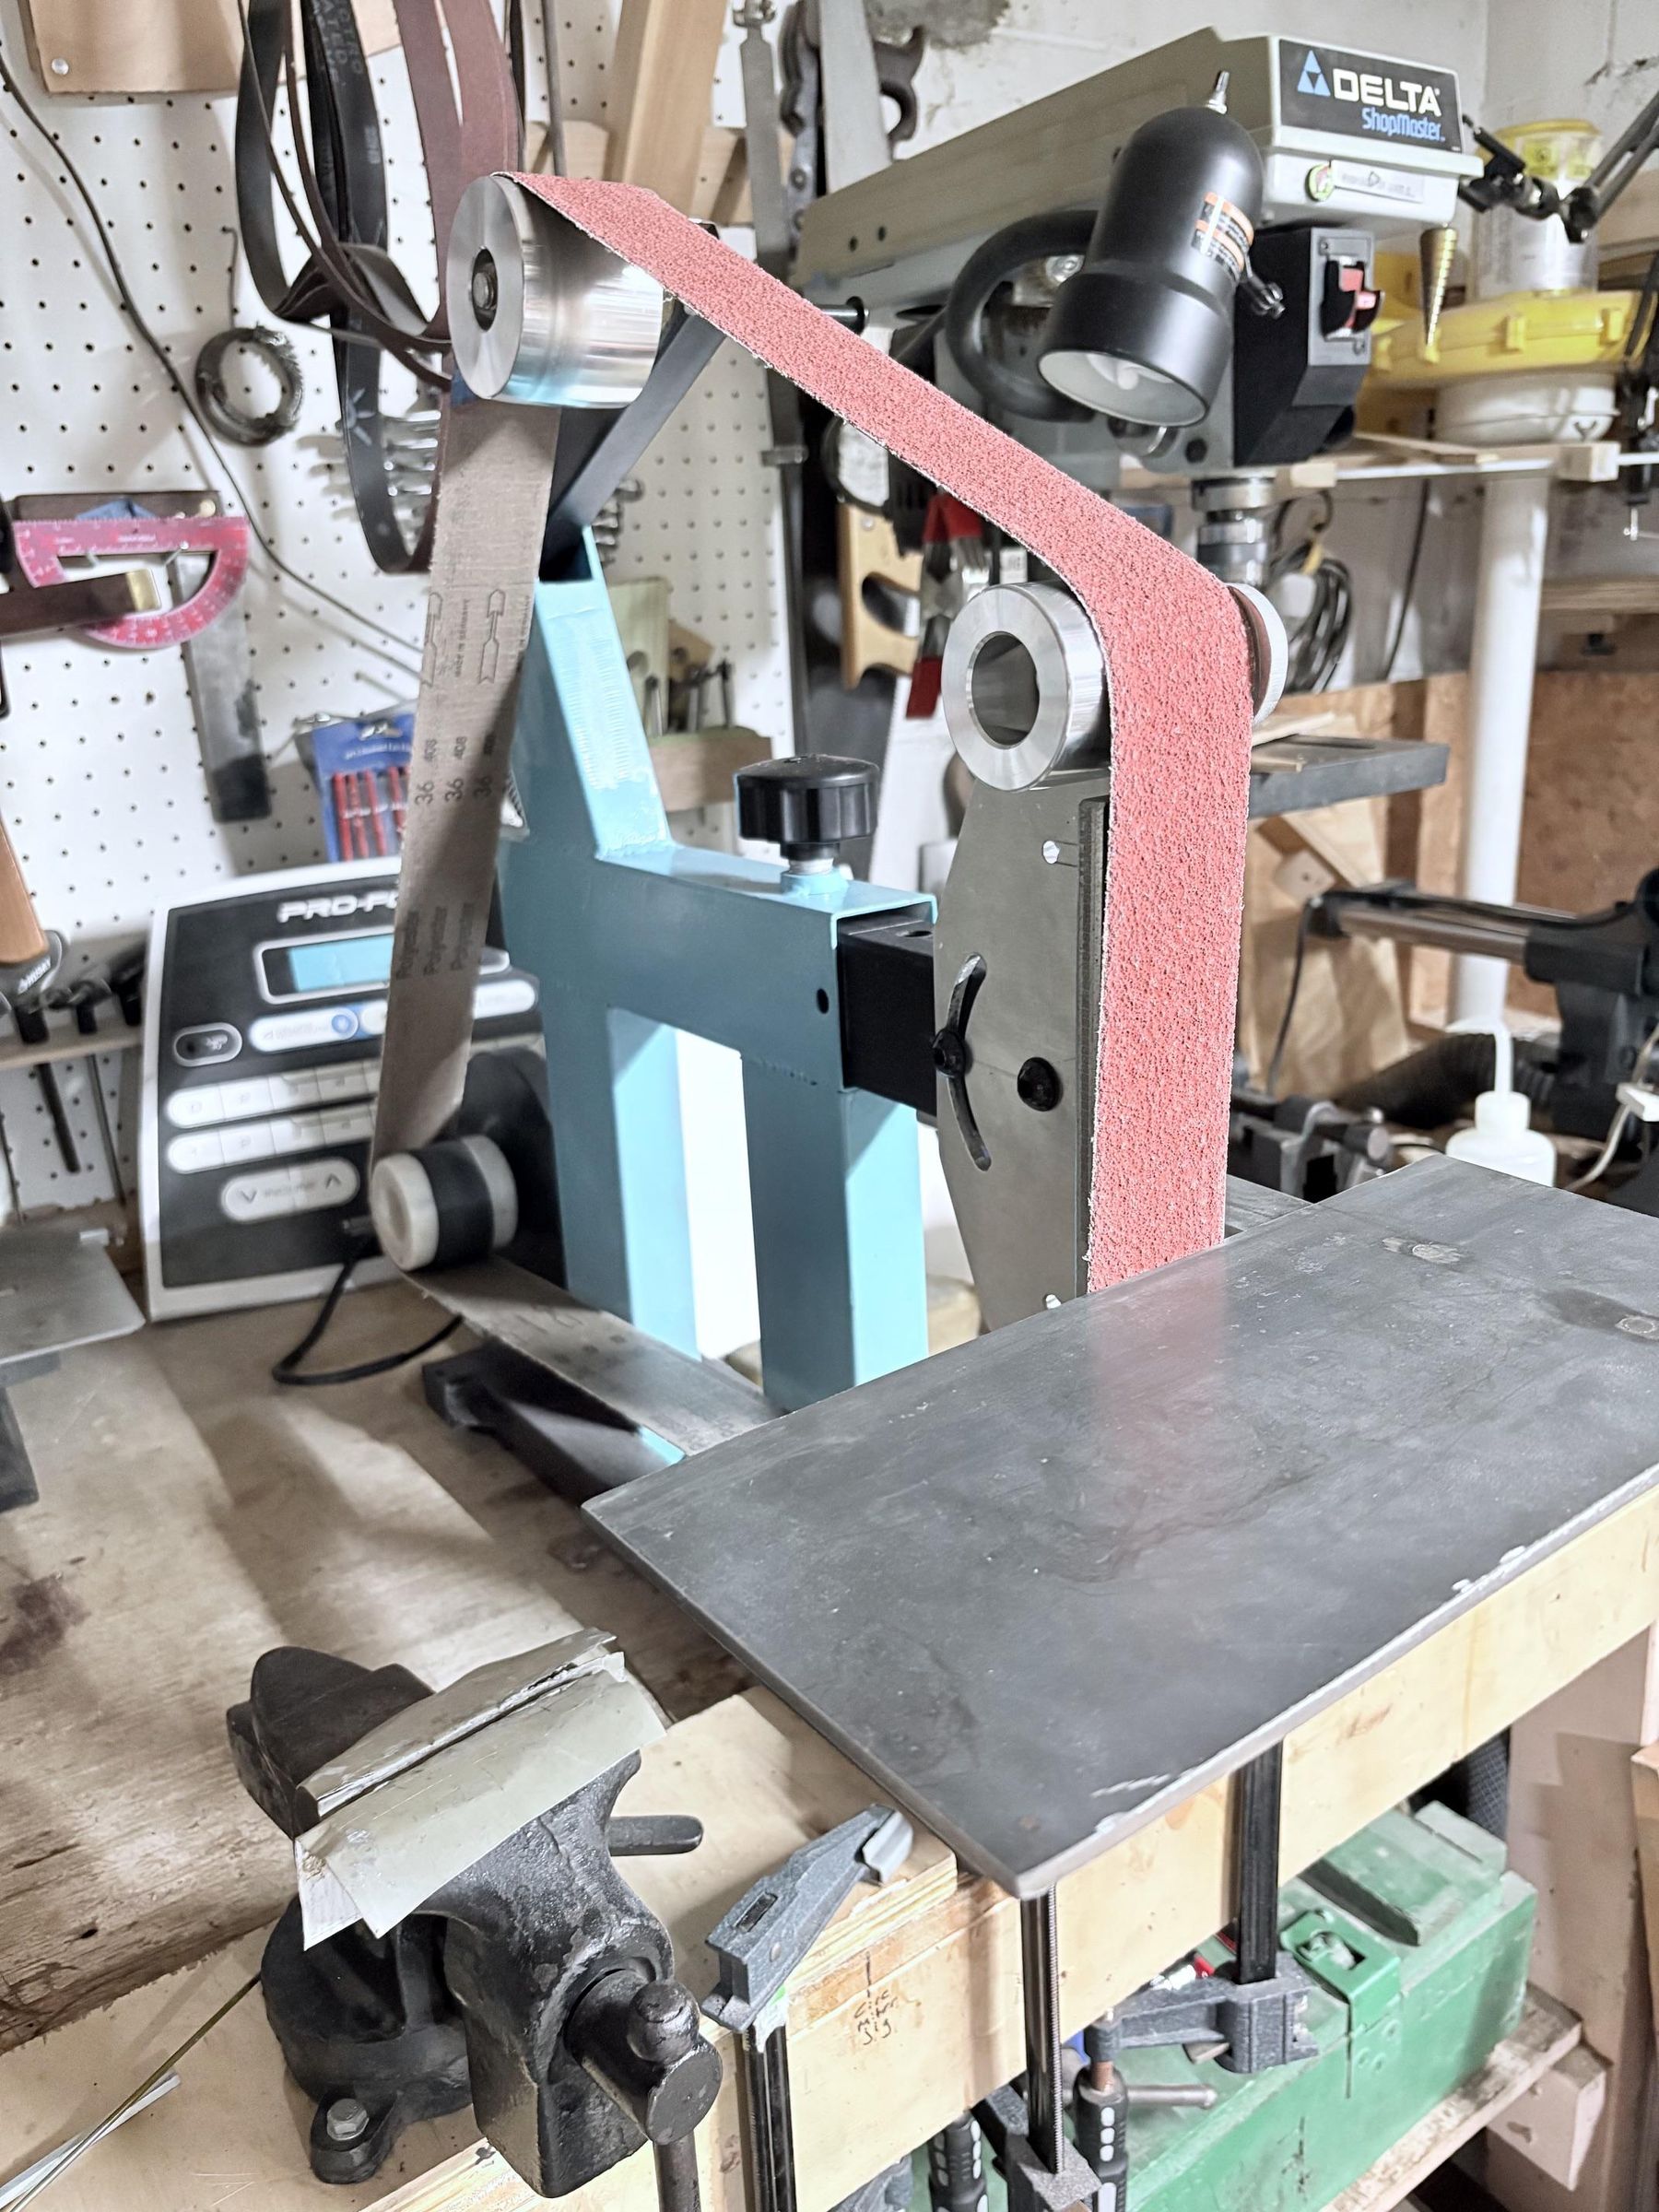

It is alive!
I was nervous to fire this up for the first time with everything being DIY, I am not going to lie. I had glasses and and face shield, lol! But it worked and tracked for a while before slipping off over and over again. The belt just would not stay on no matter how many adjustments I made to all of the contact wheels. Remember when I said it may come back to bite me? I guess imprecisely stacking small child roller skate wheels isn’t effective?!
That being said, I decided to bite the bullet and order an aluminum contact wheel set online. It was relatively cheap especially since everything else is DIY. I am still saving a lot of money.
I was looking online at forums for troubleshooting advice, how others dealt with tracking challenges, adjusting the crown wheel with tape, a lathe, machining, rubber, etc. I had so many thoughts / ideas for how to rectify this challenge myself for the upcoming weekend.
Then, I read a line that immediately stopped me in my tracks:
"There is a point when saving a buck costs more than just spending it."
After that realization, I hit the purchase button and waited for delivery.
I swapped out the roller skate wheels for my purchased ones and after making some adjustments, it worked! I had to modify my setup due to needing to swap my 1/4-inch bolt with a 1/2-inch one, but a small price to pay. This also involved drilling out my hinge to help with tracking.
With the machine fired up, using the 36 grit ceramic belt, I ground down some scrap steel and It Was So Cool! This thing eats up the metal which is why I set out to make this in the first place. I really enjoyed this and can see this reigniting my desire to make more blades.
Now I needed to reduce the vibration and decided to mount rubber feet on the bottom of the belt grinder (pic 2). These were actually swapped from the old 1x42 so penny pinching once again.
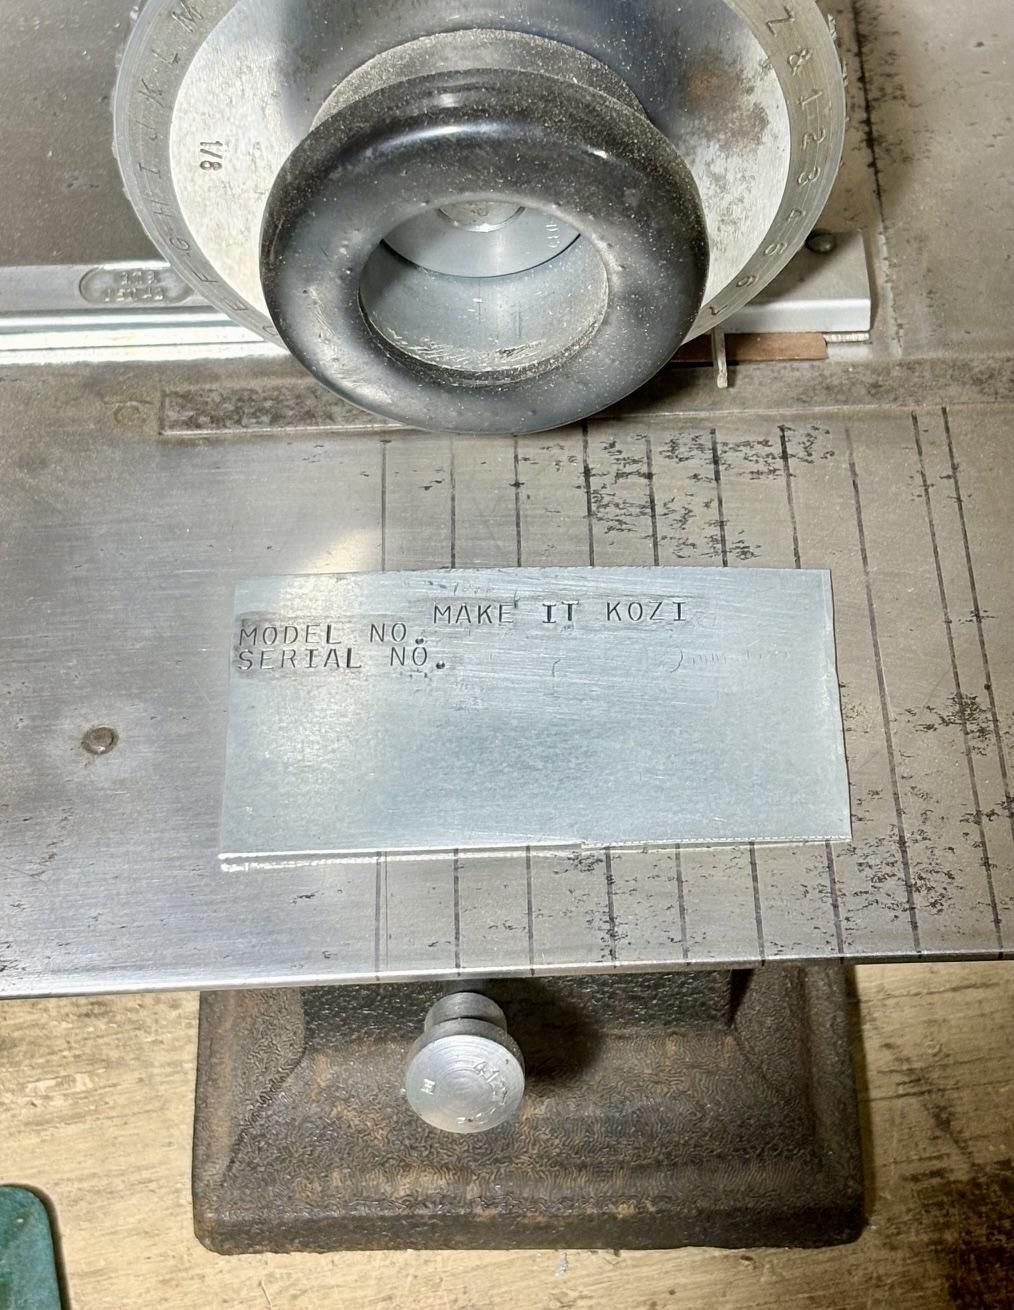
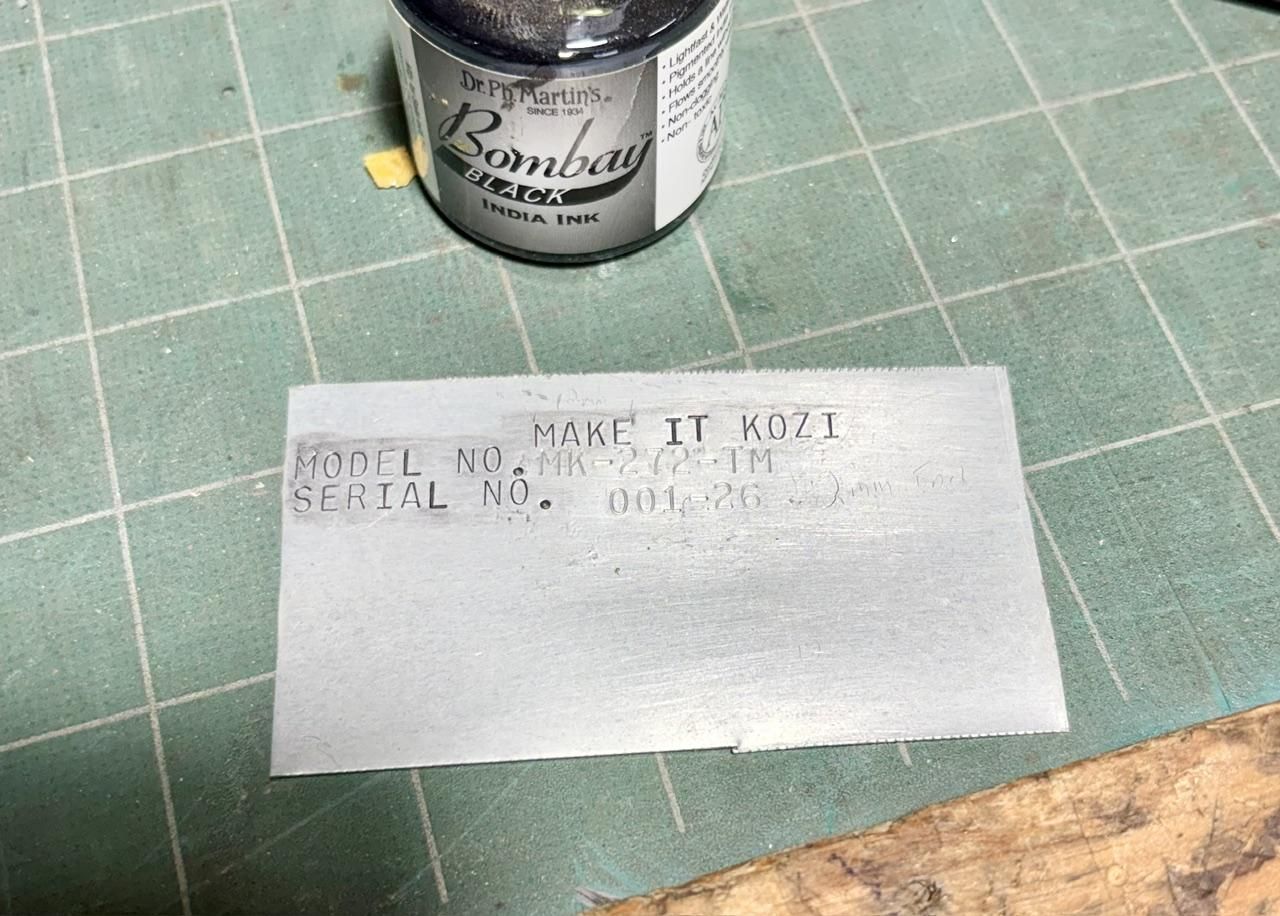
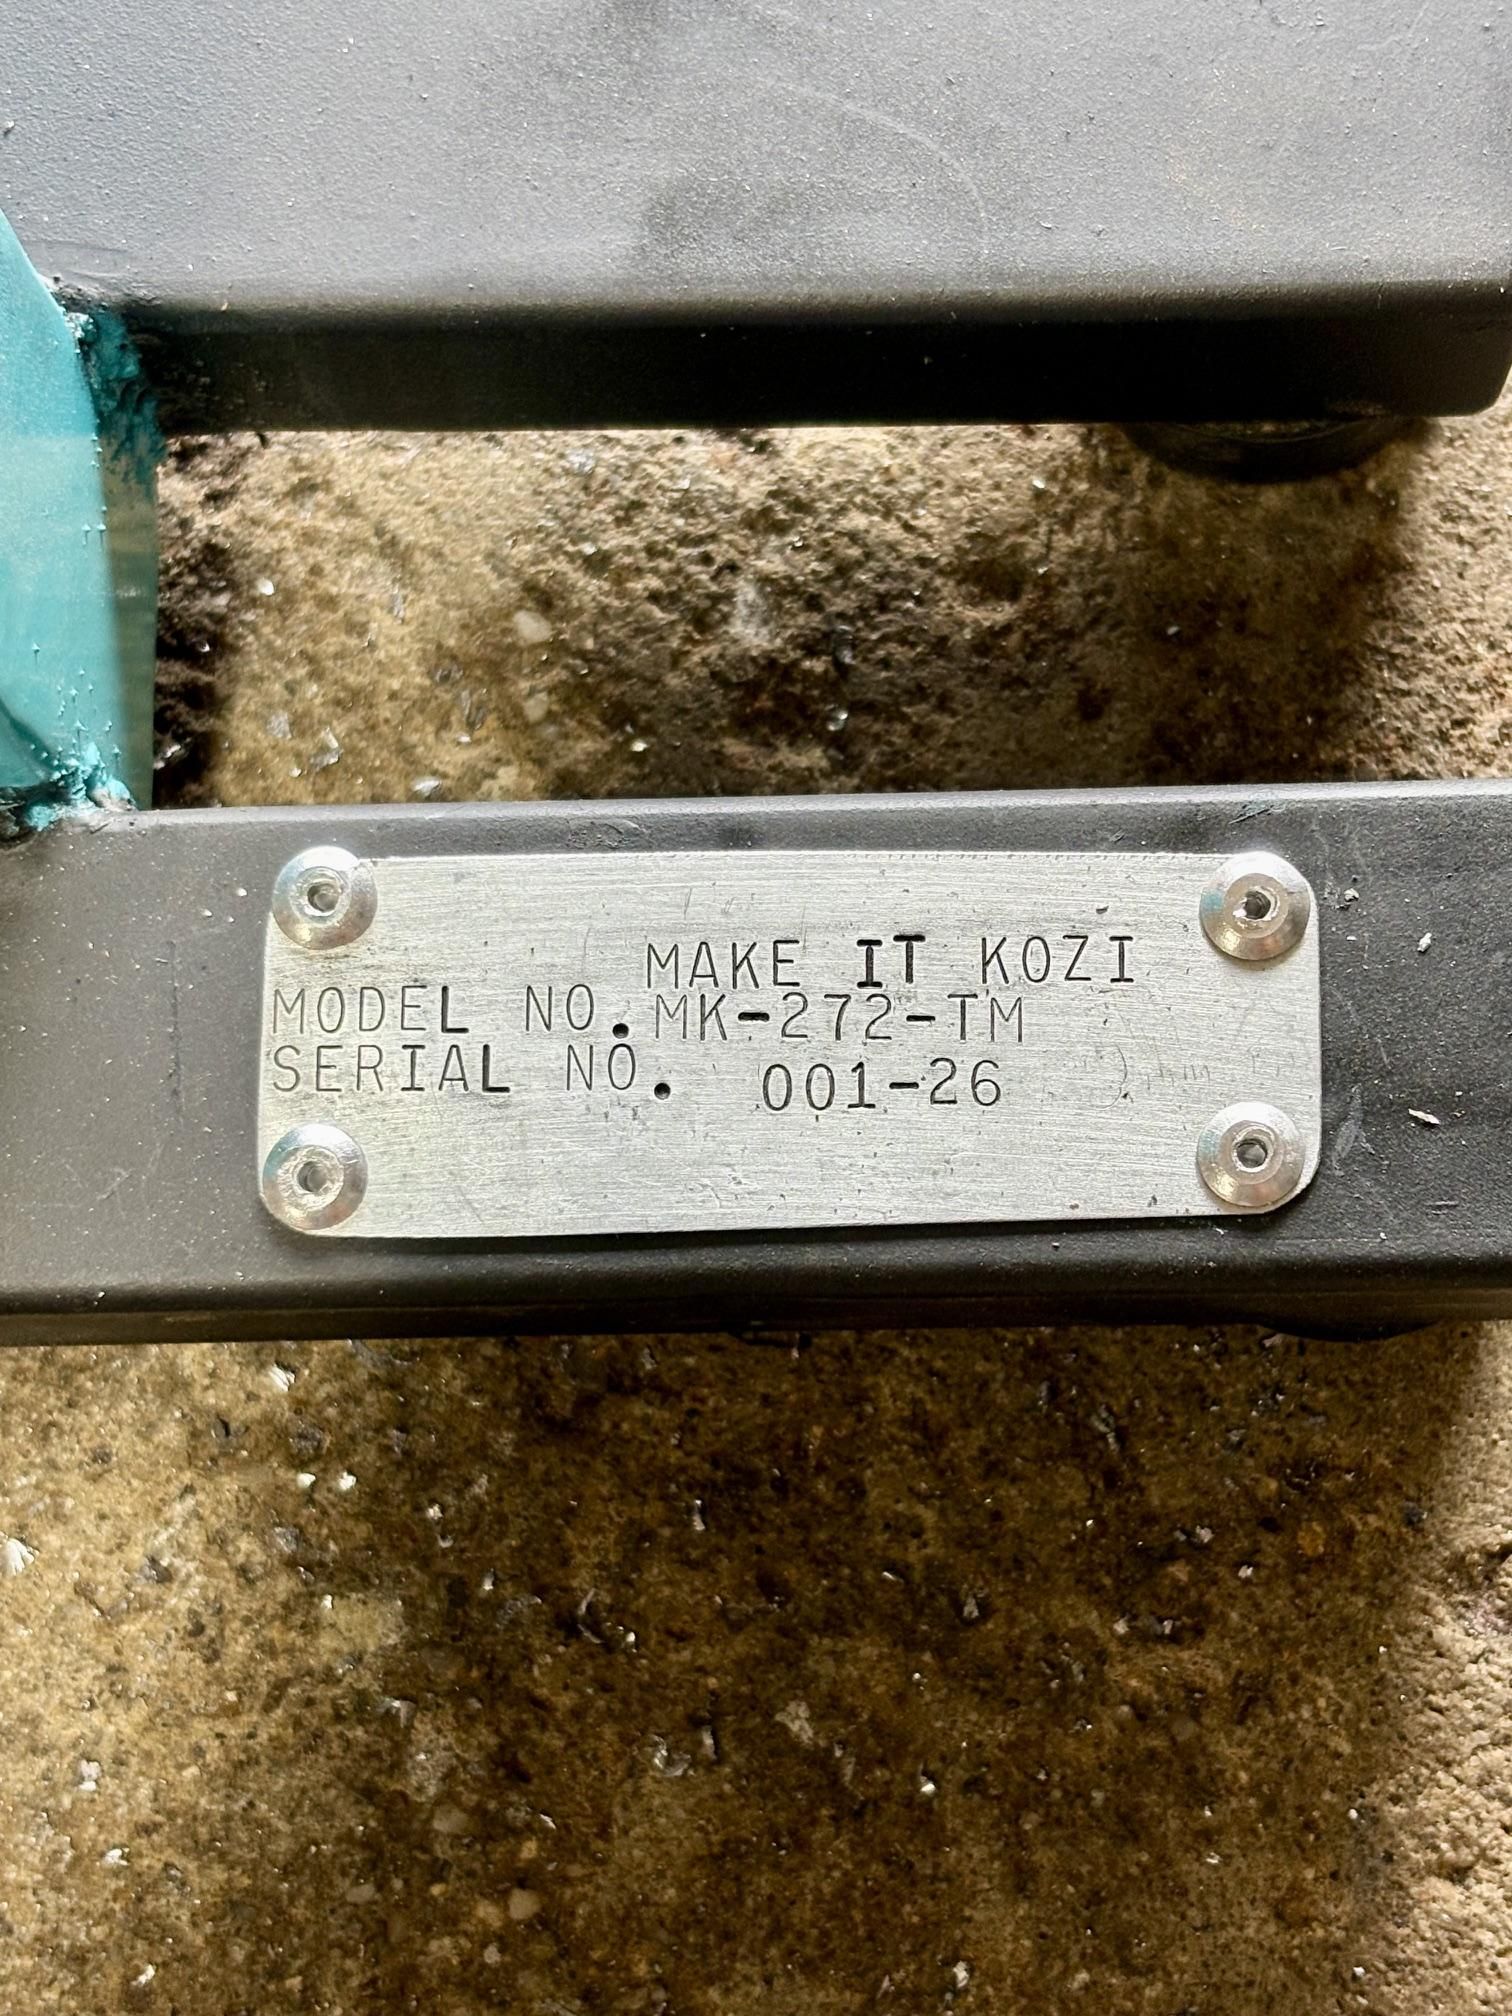
Now that I have come this far, I wanted to swap my Kozi dog tag from Step 4 above with something more "official." Using a piece of scrap sheet metal and my restored Geo T Schmidt Model 4 manual stamping tool, I gave this 2x72 its own name plate. I chose the serial number and Model based on the following:
MK = Make it Kozi (for my YouTube channel) and also like how equipping is mark 1 or mark 2.
272 = 2x72 belt grinder
TM = Treadmill
001 = the first go, so #1
26 = 2026
I think I am sooooo clever (and humble).
Test Run



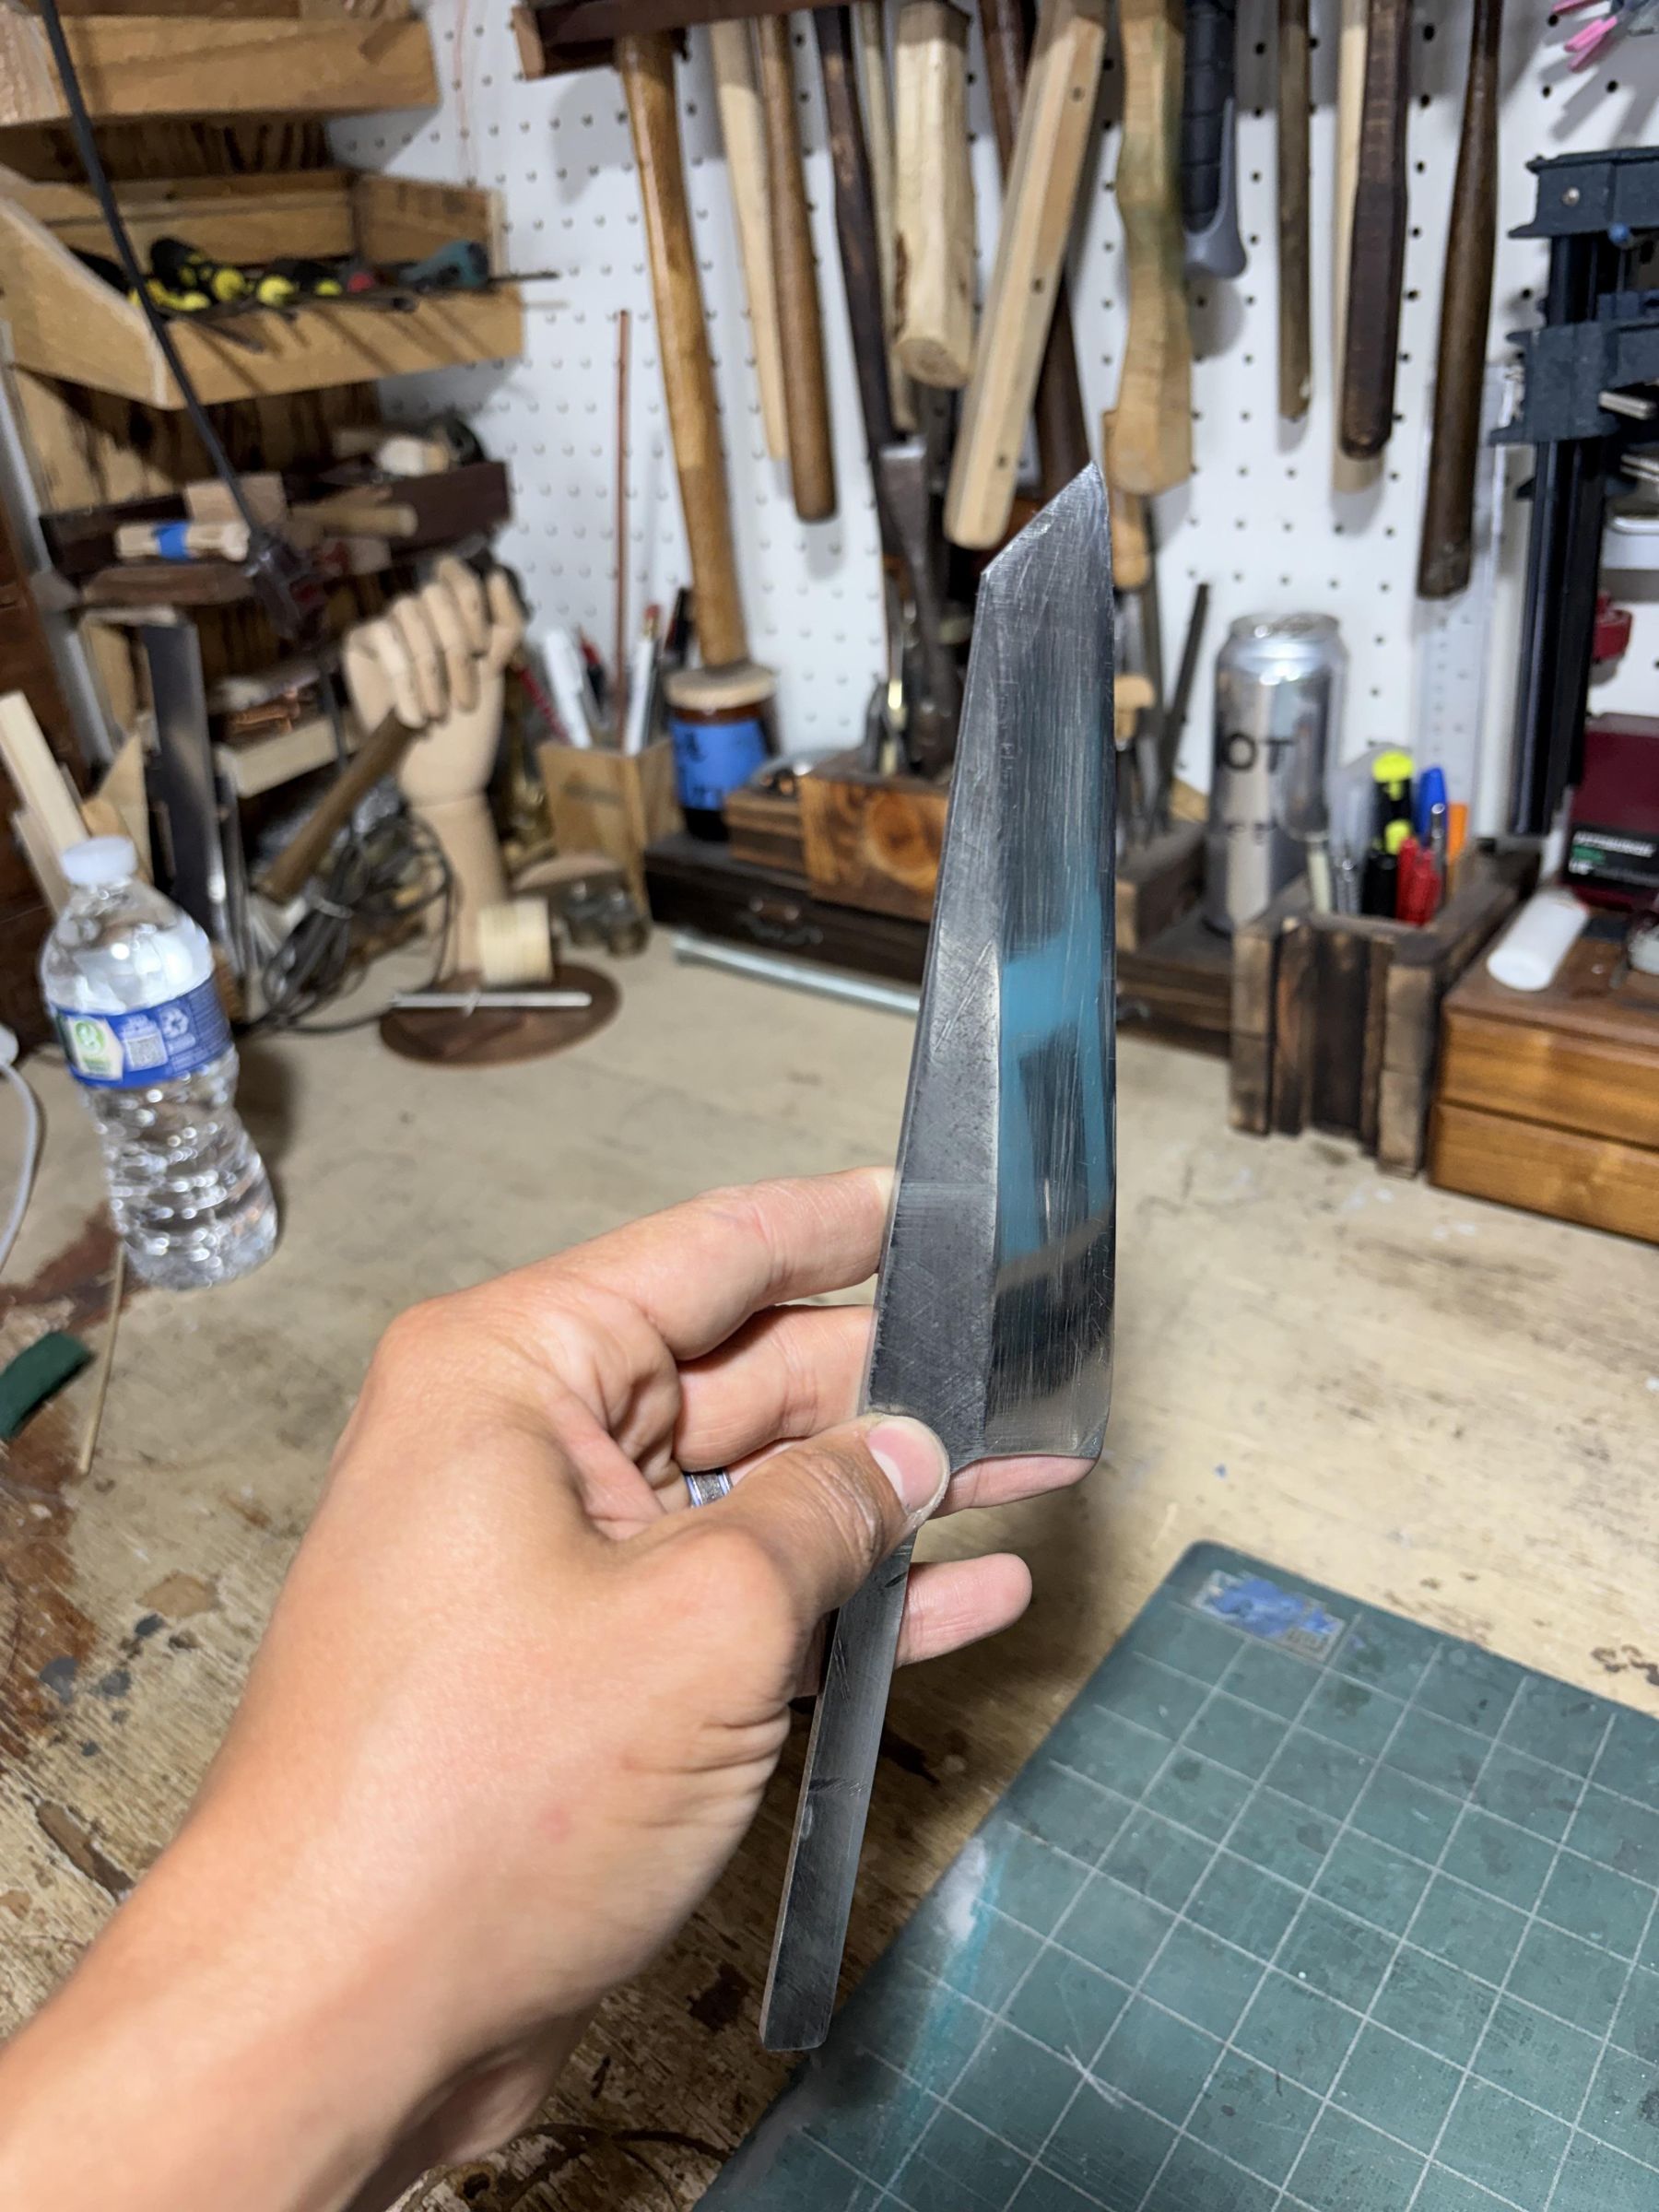
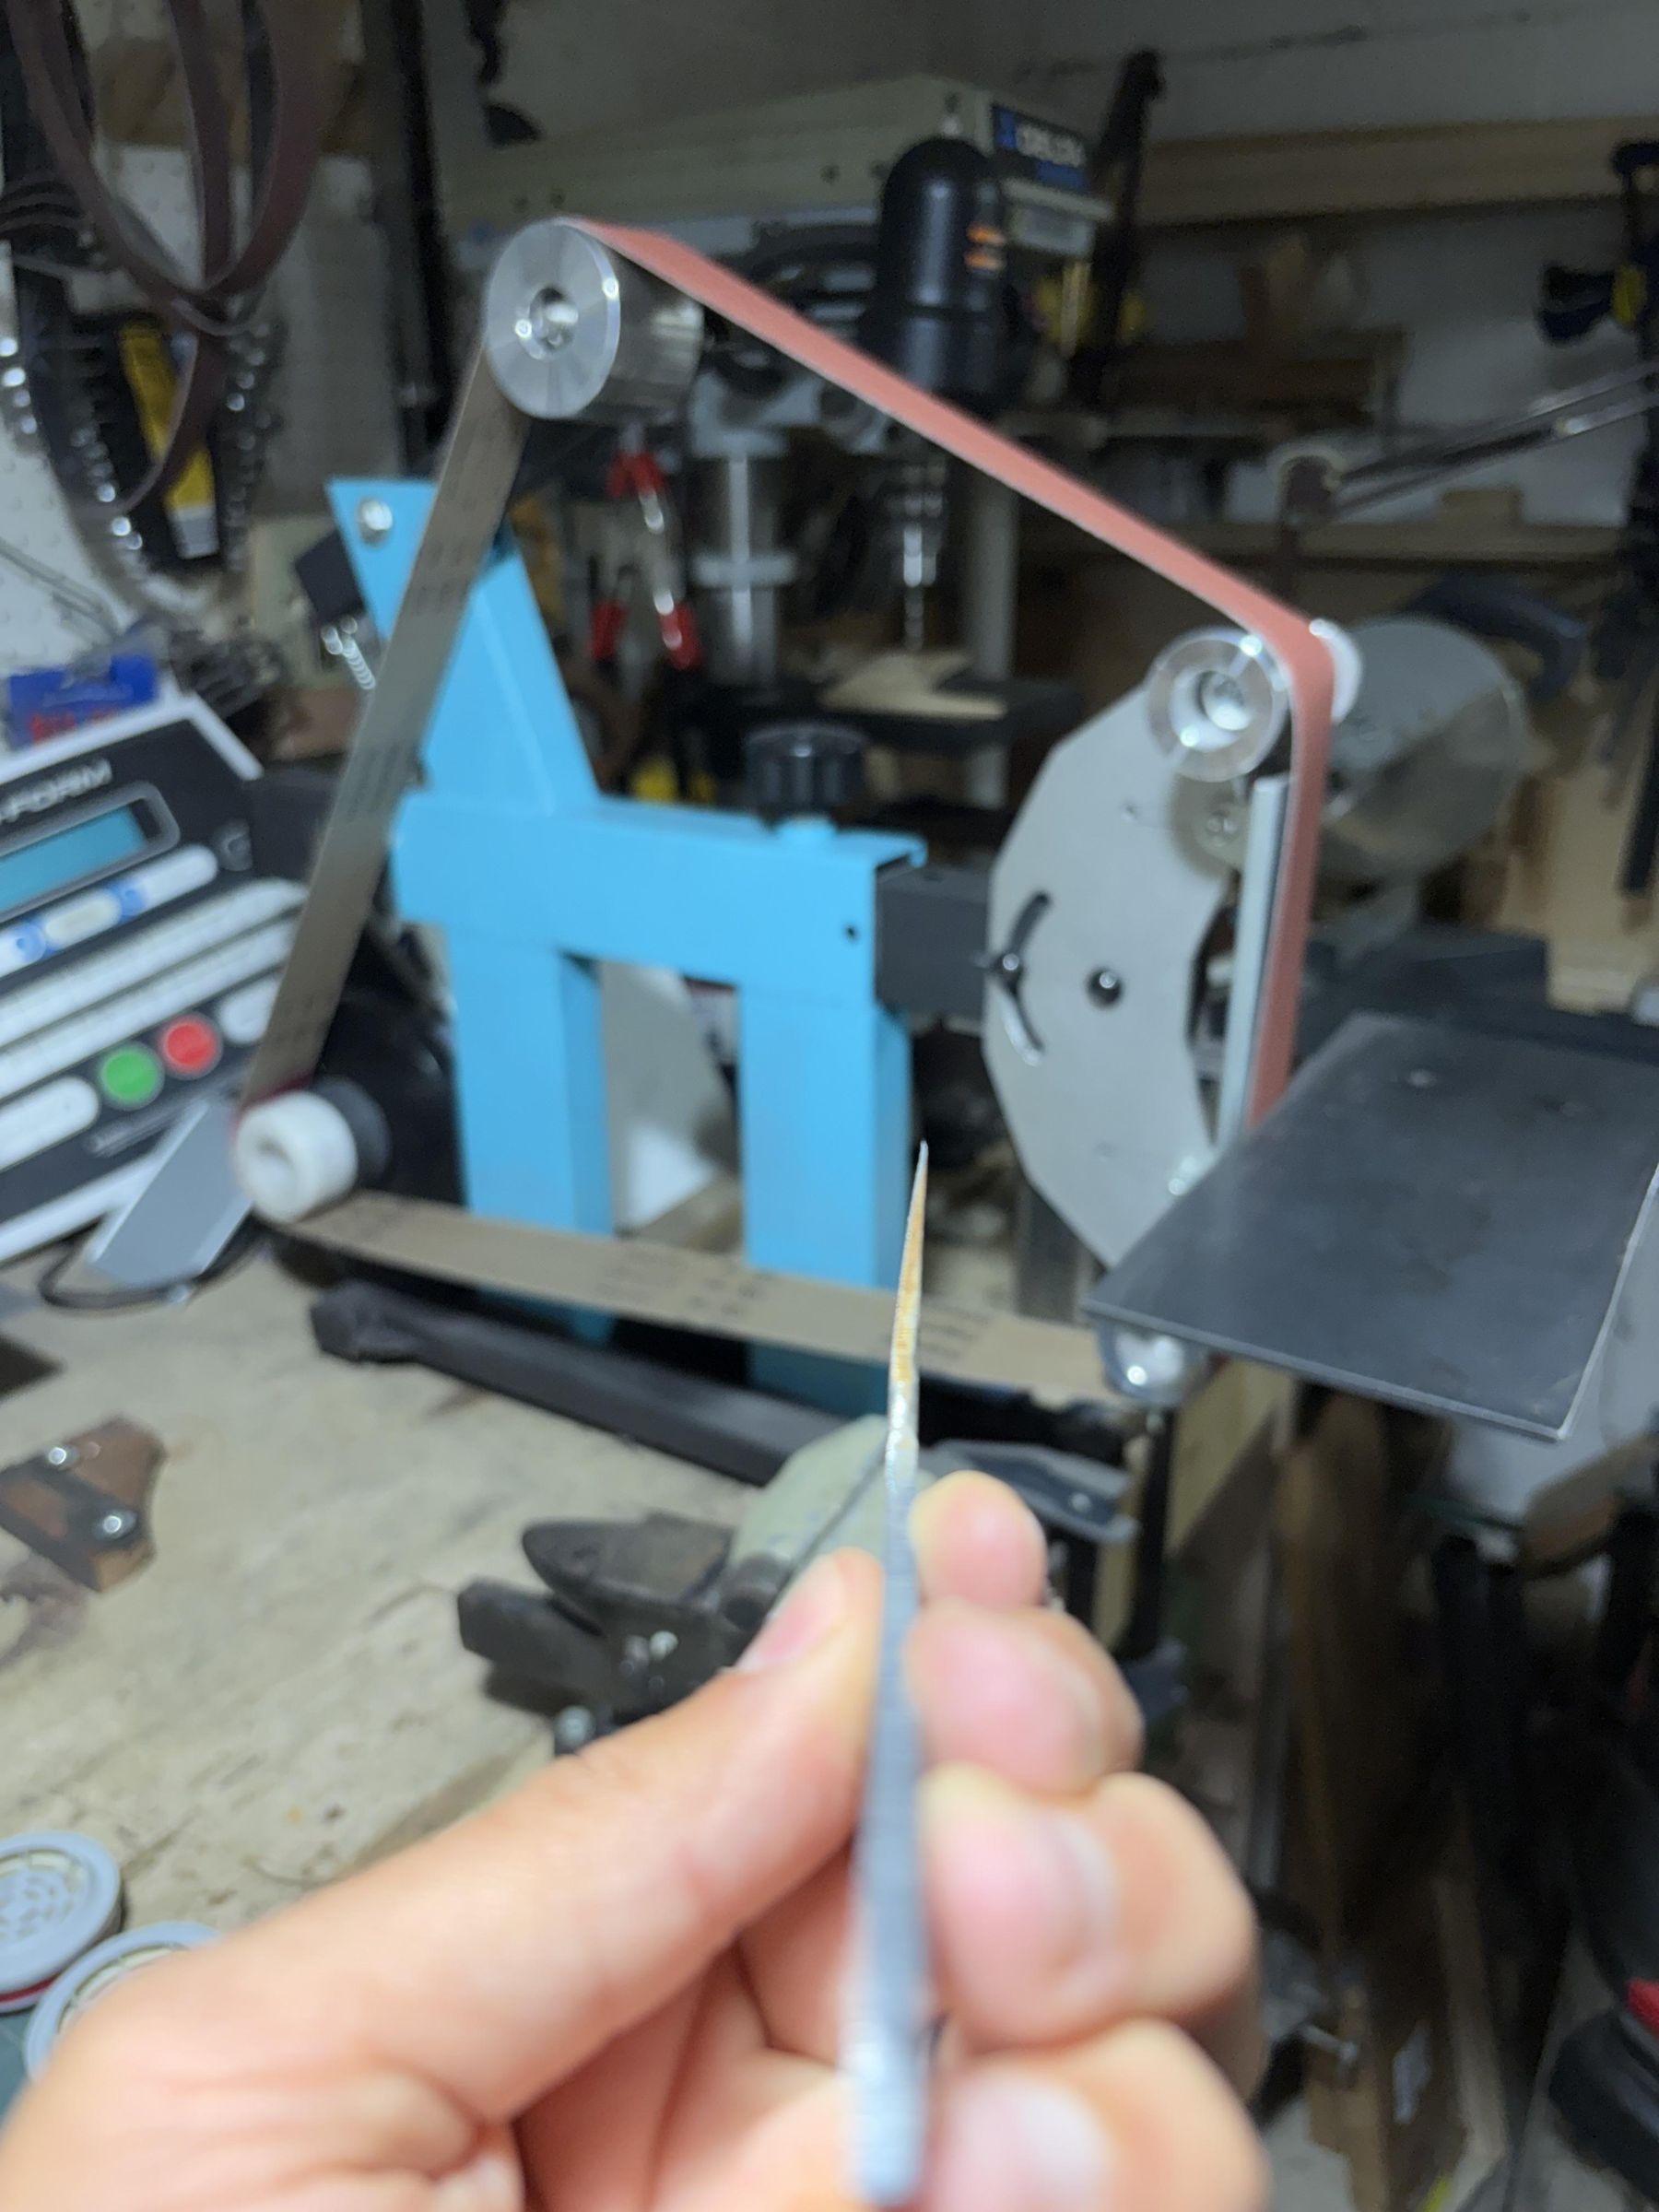
Enough talk, Let's do this!
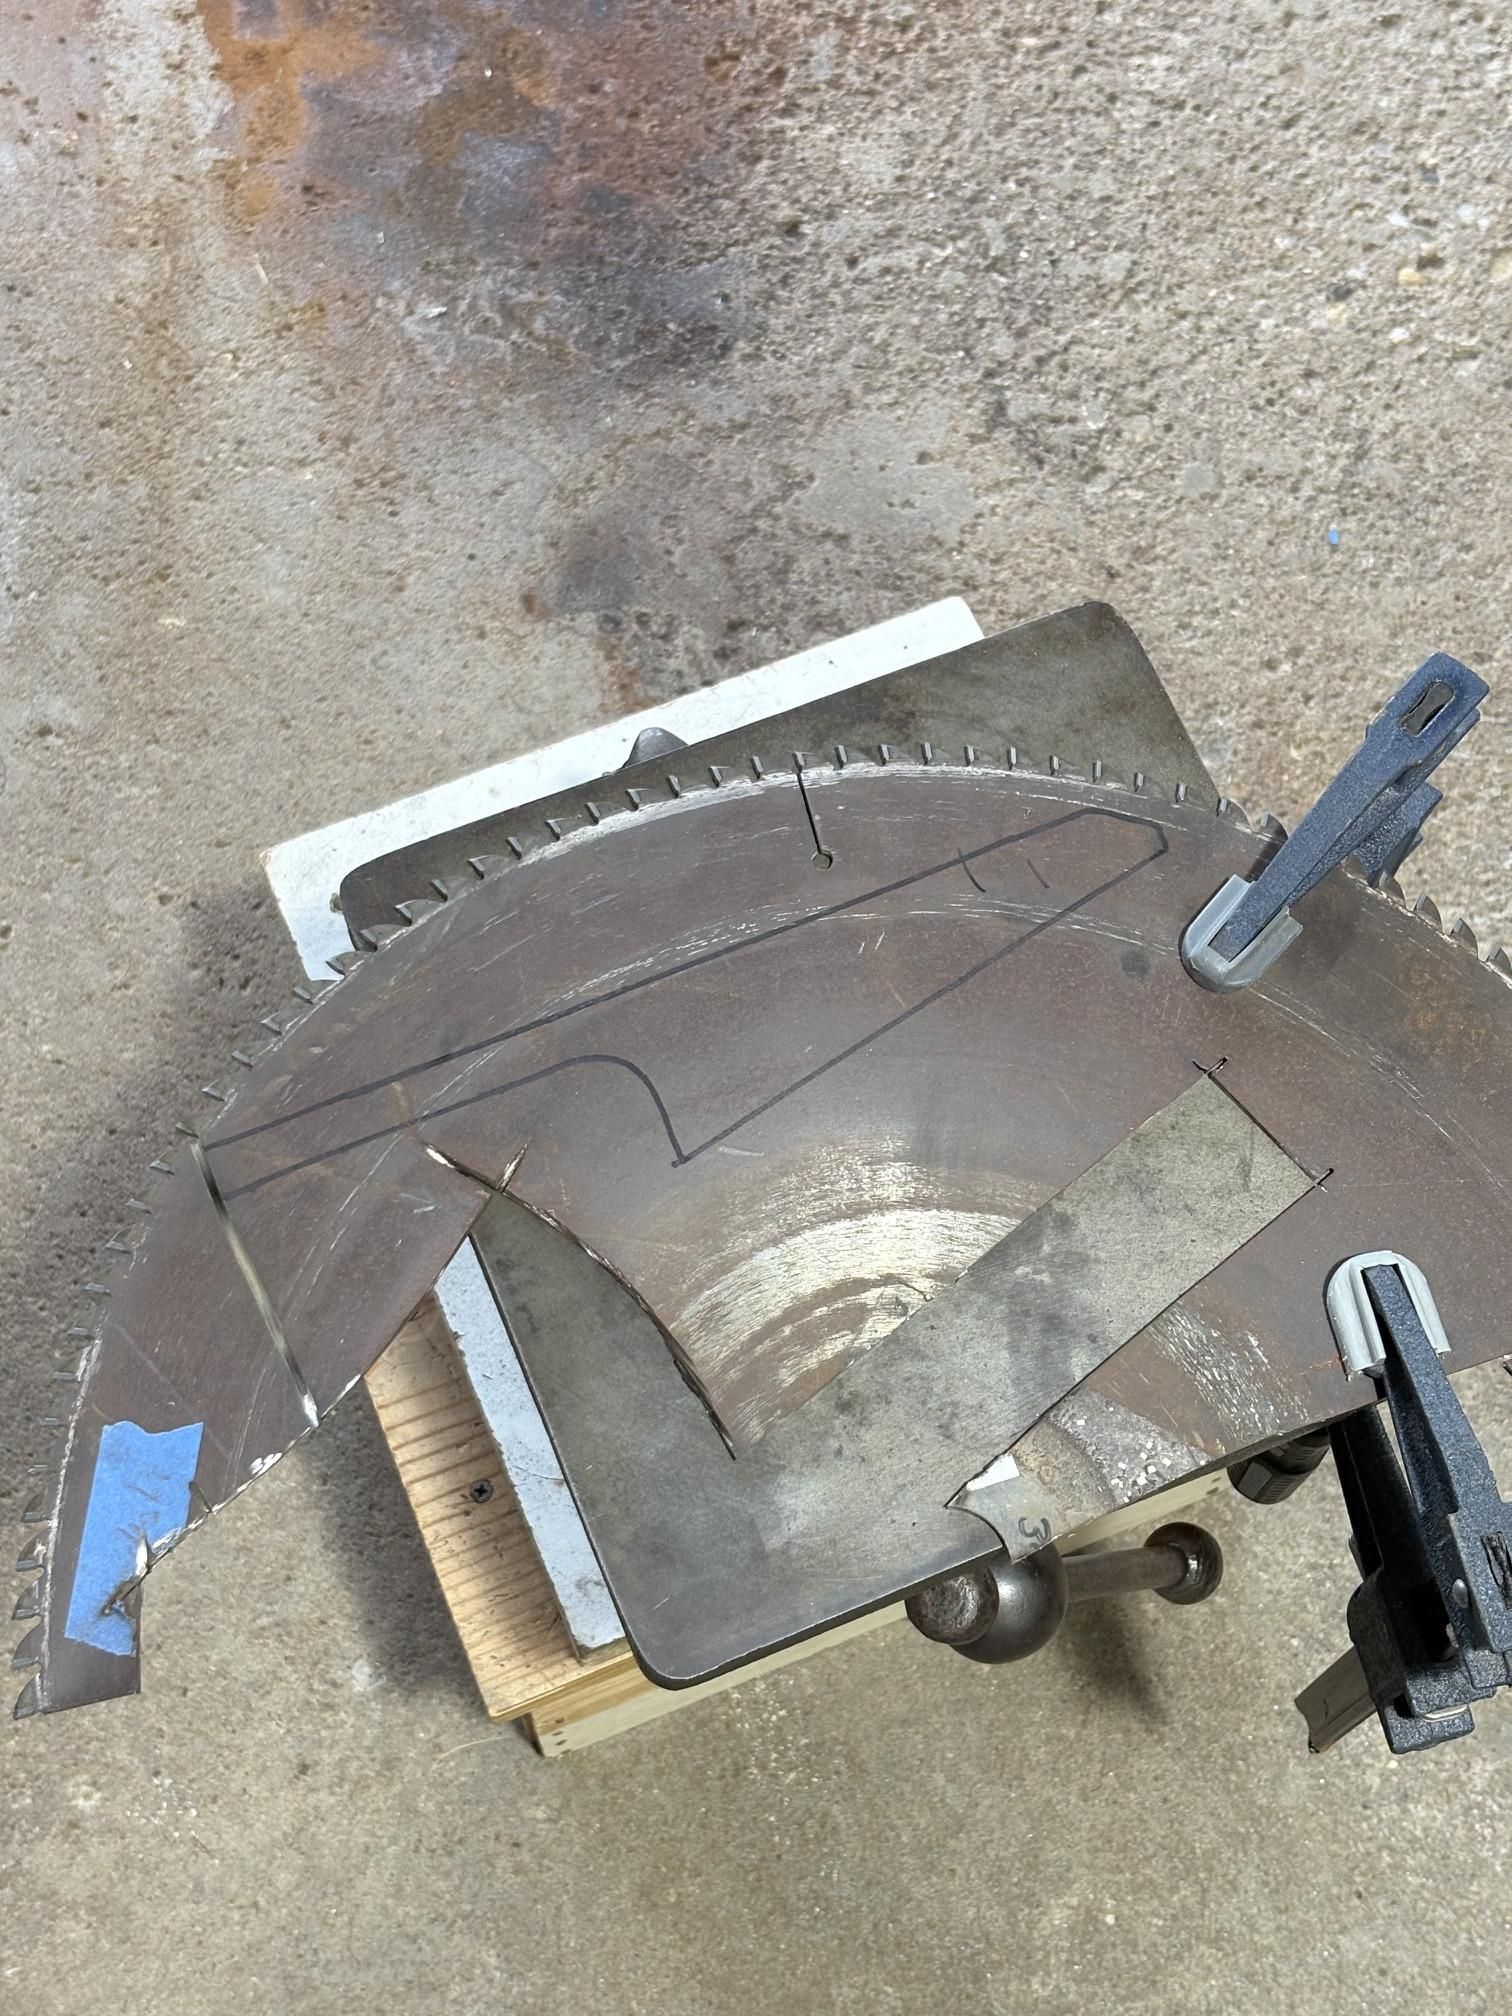
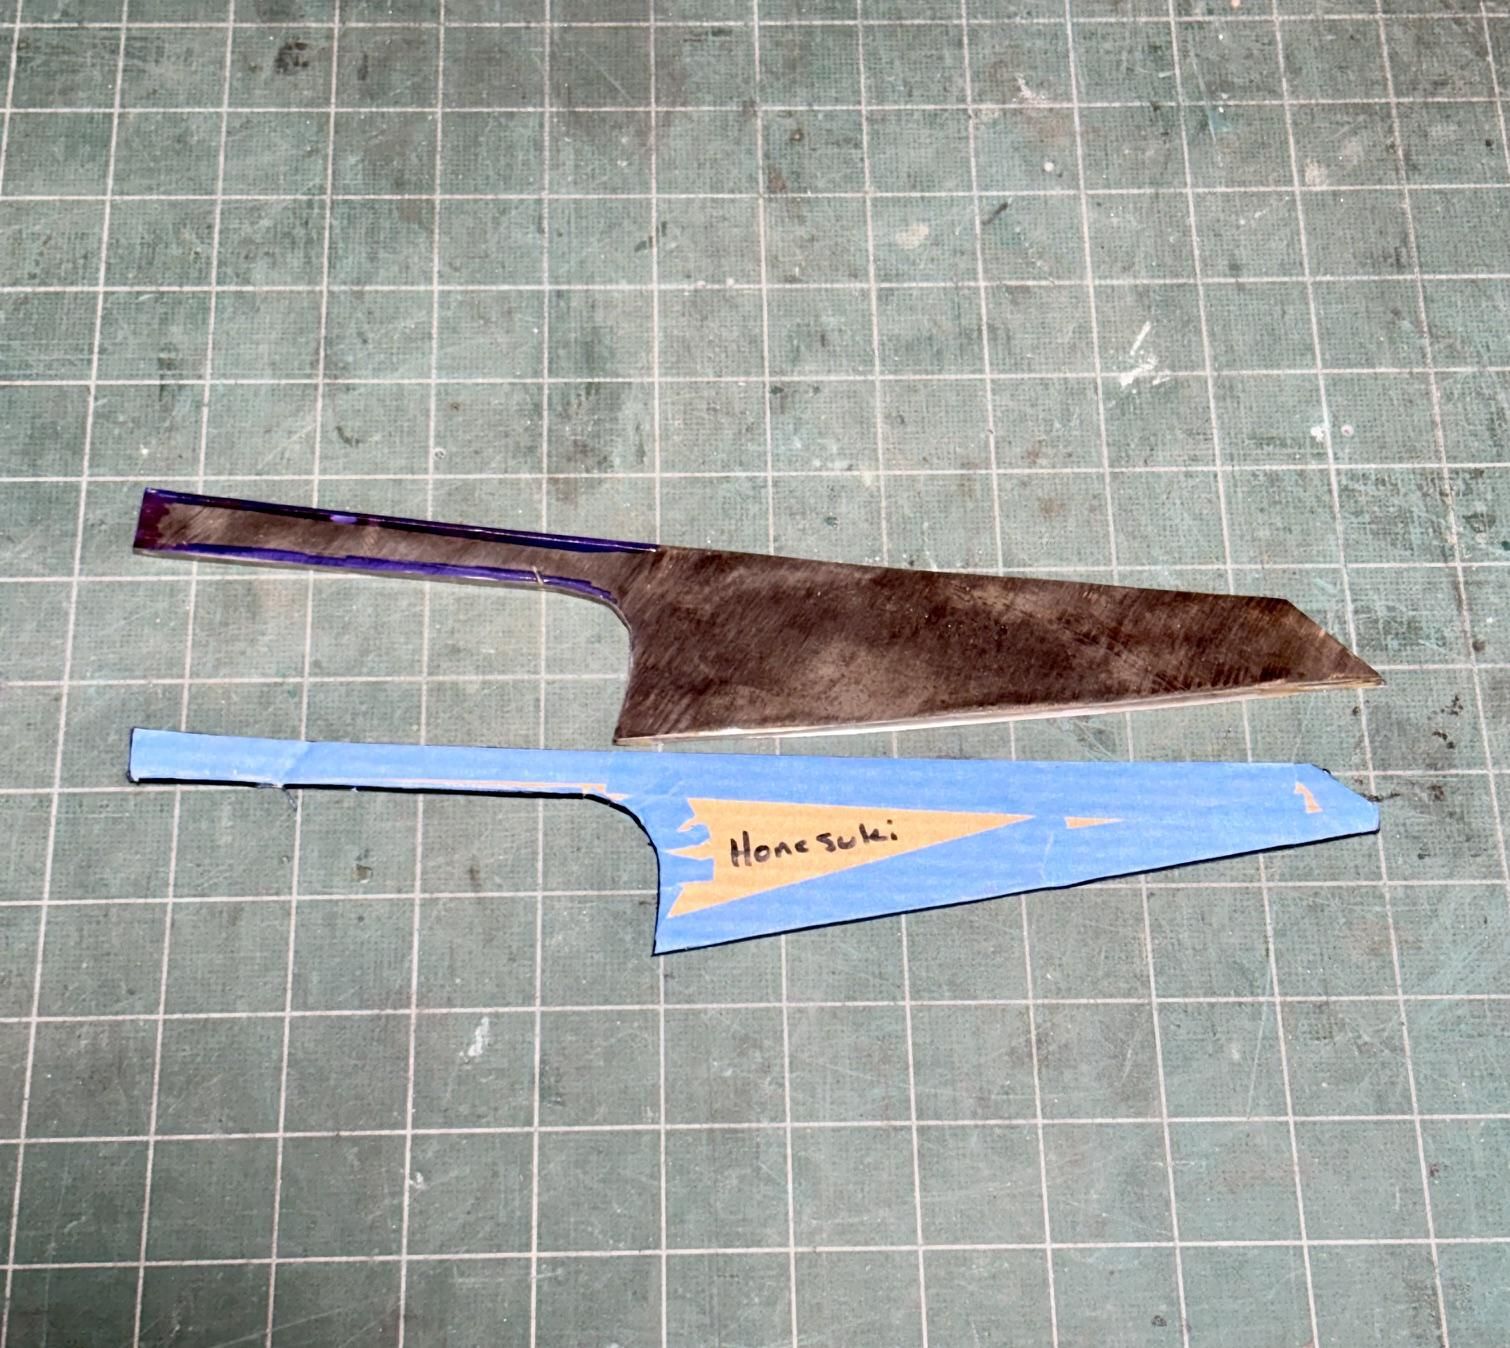
I revisited my Honesuki blank because it was probably my favorite knife to create/make. You can see the full Honesuki Instructable HERE.
TL;DR = In pic 3, you will see some of the handle marked in blue ink & scribed to signify excess metal to be removed. The 2x72 took it down, even with periodic stops to cool the handle, in record time. Well, my own record.
The build prior used a hand-held belt sander and the 1x42 to get the rough shape. This took the better part of a couple weekends. Here, I did it in < 30 minutes (pics 4-9).
I cannot wait to do more projects with this thing! Building/Shaping a different Wa Handle for the new Honesuki also comes to mind!
I hope this gives you some inspiration to create what you want but also to give those throw aways a second look. This may be an extreme example when it comes to maker-ness but isn't that why we are here?
I appreciate your time and hope to see you again!
Take care everybody.