DIY Japanese Concrete Lantern With Fully 3d Printable Molds.
by Pierre Marcotulli in Workshop > Molds & Casting
612 Views, 4 Favorites, 0 Comments
DIY Japanese Concrete Lantern With Fully 3d Printable Molds.


Hi there! Are you looking for a way to make your own japanese concrete lantern even without any mold-making or concrete casting experience? Well, you've come to the right place.
I spent years wanting to make one for myself, ever since I first discovered them in anime scenes. Now I can´t help to notice them every time they appear on screen. Which, as it turns out, is a lot!
The issue is that, unless you are an expert stone carver, they require very intricate molds to make. Making such detailed molds is usually the biggest hurdle, specially if they are to be reusable. Oftentimes a DIY option has to compromise on the shape to make demolding feasible or even forgo demolding entirely and opt for one-use molds that are broken down after the concrete has cured.
All that kept me from making one for several years. I had a model in mind. I read the wonderful instructable here on the platform about them (you can check it here). I event went as far as to make the CAD model for the lantern. But I could't solve the mold geometry for the firebox.
That is until very recently. With a little nudge from the contest and a bit of inspiration I switched my approach entirely. I discarded the heavy draft angles and went instead for a combination of flexible shells and hard casings. And after some initial tests and a few refinements I finally had a full set of molds.
So I got mysef a bucket, some sand and cement and went in for my very first cast. And the results? Spectacular. Some bubbles here an there, mainly from my inexperience casting. But the shape, down to the lines and the proportions was all there!
And the good thing? Now you can do it too!
Part of my idea was for all the mold components to fit a standard 3D printer bed. So if you have a printer or you can have someone print the parts for you then you can definitely make one for yourself.
Below you will find the full set of printable files, instructions for assembly, tips for casting and curing and a bit of the design process that went into making it.
Hope you like it and keep making!
Supplies


As the focus was to have a fully 3D printable mold, the materials required are pretty straightforward:
For printing the mold you will need:
- Around 1650g of PLA or PETg (PETg is better for reusability, but PLA works just fine. I had some unused PLA spools so I used that).
- Around 200g of TPU.
- A fine amount of patience to wait for all the prints to be ready.
As for casting the lantern:
- Basic safety gear. Glassses, gloves and a dust mask (N95).
- Canola oil or similar to prevent the parts from sticking to the mold.
- A piece of cord or twine to secure the firebox inserts ( 1m is plenty)
- A bit of tape to secure the bottom of the roof mold.
- Some Plastiline (oil based modelling clay). Optional, but it helps covering seam lines and reduces the need for sanding. Which leads me to...
- Sandpaper (60-80 grit for aggressive removal, 120-220 for seam lines and minor surface details). Optional, I personally didn't have to sand mine thanks to the plastiline but maybe I will still use 180 grit on the seams for good measure.
- Concrete mix: aim for anything in between 1:1 to 1:1,5 cement to sand ratio. I used 5 parts cement to 7 parts sand. You will need at most 3,5 kg cement and 4,15 kg sand (including a 15 % safety margin for bowl leftovers and compression). Personally I used 2.75kg of cement, 4,15kg of sand and about 1,25l of water.
- Additives (optional): Dish soap or a plasticizer to help with flow (might have helped me since I did get some bubbles, but turned out fine without).
- Different aggregates options: you can swap part of the sand with some perlite or similar. I tried using some crushed natural pumice stone but I had very little and it barely made a dent in the overall mix. It is not essential but the porous stones help achieve a grainy texture and also reduce the lantern weight.
Model Refference and Early Design Choices

This entire journey began more than five years ago. I was going through a ¨concrete phase¨ and I was looking at things that could be made with concrete. And somehow I landed into japanese lanterns. It didn't go farther as the molds required were pretty complex and I was not very confident in my printing or modellling skills yet.
But something had definitely stuck.
Years passed and I got a little more experienced and a bit more involved with japanse culture and something pushed me to take a crack at it.
First thing Idid was to find an existing model that I liked and that seemed would translate well into casting. Normally I would be against trying to copy the look of a preexisting moel, but when it comes to traditonal objects the line becomes kind of blurry. It's hard to keep up with tradition without well imitating it.
So I ended up selecting the model shown in the picture. It was a part of a catalogue/infographic in https://japanesegardens.jp/explanations/japanese-garden-history/. I wanted to refference it directly but it seems to be gone now from their site. And I wanted to do a dwarf version of it because I liked the look of short ones better (so much for keeping with tradition)
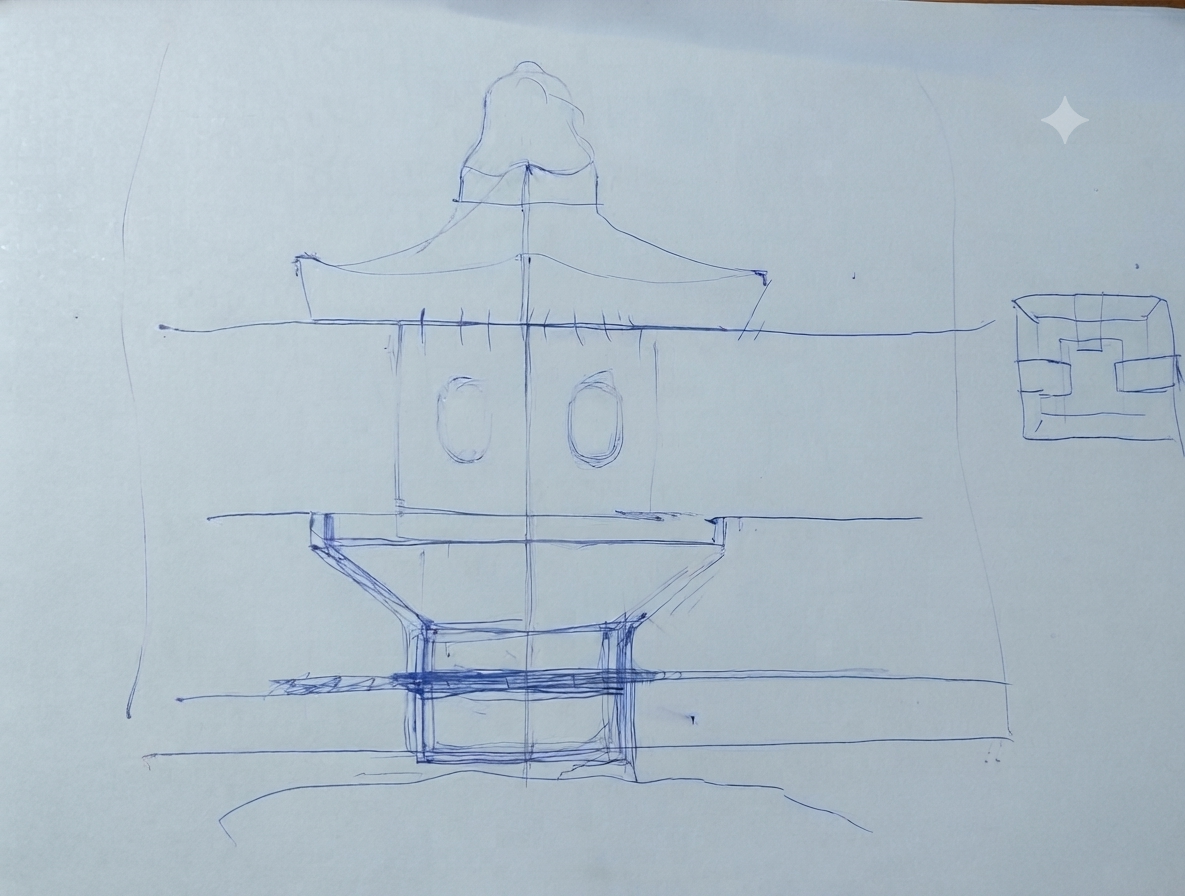
The second image is a sketch I managed to dig out from some of my very first drawings a that time. First I was checking components, draft angles and the like until I got to what would be the most fundamental design choice of all. I decided I would scale it so that all the components could fit the 3d printer I had at that time.
The rest, as they say, is history. I verified that at that scale the firebox had enough space for the side walls and a cavity large enough for a standard candle and I knew right there it was (theoretically) viable.
CAD-from Model to Mold


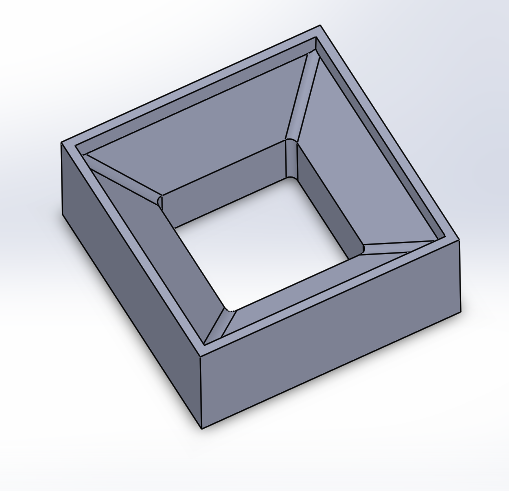

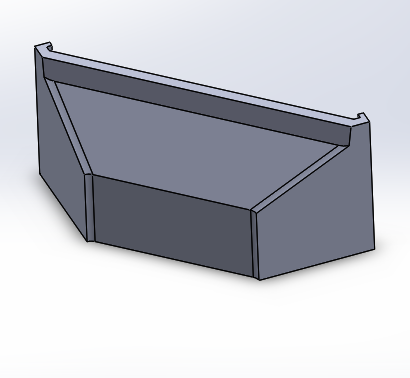
I could do a step by stem analysis of how I got to my model of the lantern. But at the end of the day i think it is not as useful as knowing hou something you modelled can be reliably turned into 3d printable molds.
The Path is fairly simple. It goes as follows:
- Start with the component you want to make the mold of.
- Make a box larger than the part (on x y, z stays the same) . The extra size becomes the thickness of the mold (here its 6mm)
- Now subtract the component you started with to be left with the cavity
- Split the cavity as needed for better printability or to avoid concave sections that are hard to demold.
- Add brackets compatibility to the corners.
What are the brackets? well it's what makes it so simple to make a mold in so few operations, as you will see in the next section.
CAD- Standardizing Joinery


Another of the early decisions I made when designing the molds was to standardize the joints used for assembly.
This serves a couple of purposes: first, I can test a single case, optimize it, tune in the tolerances, then replicate it. So it saves a lot of time and material in test prints.
Second, it makes it easy to model. In all subsequent molds I know I just need to add a certain shape on the corners and it will be compatible with my existing brackets. And this not only extends to this project. I can even do another mold for a different project and use the same system (and even use some of the brackets from my previous mold instead of printing new ones).
Third, it makes it so sometimes you don't even need to model. The slicer itself allows for non-uniform scaling. So if I need a different height bracket I can just ... scale it to size
CAD-firebox Iteration


Now you may have asked yourself. Why take that many years to make the mold if everything was already done by the looks of it?
The problem was the firebox insert. As it was very deep I realised that if I gave it the draft angle it needed it would eat away at the space alotted to the side walls, leading to either too fragile a final part or one that was impossible to demold without breaking.
So I was stuck for many years, until I started to print more with TPU.
Then I realized that I could use a flexible outer sleeve over a solid core to make the inserts. The idea was for the sleeve to be pre-cut to make later de molding easy.
That lead to the first prototype seen in the picture. It was, to be frank, a total disaster. But it taught me I needed an internal bracket (to keep the sleeve closed) and that the core support could and should be more airy to prevent suction from creating too much friction upon removal.
Literally that second prototype is what was used in the final cast
Printing the Mold

Here are the files needed to print the set of molds.
Prints are not complex ones so no weird settings. For the large or tall parts I recommend a small brim just to be on the safe size. And maybe add supports to the holes in the Firebox side panels. (just so the circle comes out crisper).
You'll see I have grouped the parts according to the printing material this way it's easier to divide them into batches.
The rigid ones as noted can be printed in both PLA and PETg. In theory PETg is better as it is not as heavily degraded as PLA by the high alcalinity of concrete. Basically a PLA mold is not as good for reusability.
But that might not be the deciding factor. In my case I used PLA simply because I had some spools that had been lying around for over a year and It was a great oportunity to put them to use. So keep that in mind as the material use is pretty hefty. So why not give that brownish greenish spool you are keping ¨just in case¨ a chance?
Notes on Part Orientation

Although all parts in the files are already set in their intended printing orientation there is one case where it can be a bit counterintuitive so I thought I'd better explain it. Just in case someone making the mold thought it was a mistake.
And if I was going to explain one orientation choice I might as well mention the other few cases where orientation is important.
So here it goes:
- The brackets: even if printing them flat might seem better for part stability and a reduced print time It would create weak spots during use right where the parts they are holding would be trying to push apart. In regular situations it might be ok but with the heavy alcaline environment of concrete a point like that mainly relying on layer adhesion greatly reduces the durability of the mold. All the more if you are using PLA.
- The firebox casing walls: Similar situation here. Printed flat the part is weakest where the brackets go during assembly. Moreover. if you print them standing up you can fit more parts on the printbed so you can reduce the number of batches needed to print all of the mold components.
- The slanted roof segments: Here is the one that I was talking about in the intro. Even if the suggested orientation might look a bit unstable it is highly suprior in the context of making a mold. You see by changing the orientation the curved slopes of the roof can be reproduced perfectly. If you went for a more conventional orientation the smooth curves would be translated into ¨steps¨ by the slicer. Those steps would definitely show on the final piece and would need to be sanded out. Furthermore, the irregularities in the mold would make the concrete parts stick more and make demolding harder.
So in all this cases I highly recommend the suggested orientation. If you are worried about part stability during printing just make sure to add a brim for extra adhesion. That and keeping the bed clean. As we all know a little bed cleaning every other day keeps the spaghetti monster away!
Assembling the Mold


Lo and behold! After finishing all those print hours you will be left with a pretty large gathering of parts. How colourful really depends on how many leftover spools were sacrificed in the making. They may seem like a lot but the end result is quite compact as you can see.
In the following sections I will be showing how to assemble each part of the mold. However, you don't really need to do it before you are ready to cast the lantern. In reality you would oil each component individually before putting the whole thing together.
Now I dont think its hard to explain why I would choose to take the pictures before every single part was covered in oil right?
You can still build it to check tolerances and the like but just know you will have to disassemble it later to get it ready fo casting.
Assembling the Mold I- Hoju -the Top Ornament


Pretty straightforward really. Just make sure the seam of the flexible mold does not match the seam of the outer casing. It reduces filtrations and applies a more even pressure on the seams.
Assembling the Mold II- Kasa-The Roof


The assembly is even simpler in the newer version. I realized that I could make the brackets brace the outermost yellow part, so the green casing was completely unnecesary.
The funny part is that I realised this before printing. When I set out to print the roof mold a few days had passed since completing the changes to the model. I simply... forgot, and printed the whole set before realising I was using the old stl.
So yeah, don't do that. The newer version is much better.
Assembling the Mold III- Hibakuro- the Firebox


Nothing too complex here either. There's only a little step you can do ahead of casting and that is cuting open the sleeve of the central insert. Carefully cut along the corner where the inner bracket goes. Mak sure the cut goes all the way through.
Why not print it already split? even with the best printer settings you would not get a better seam than by printing it whole and then cutting it. You would either need to leave a gap so it wouldn't stick (leading to a bad seam and filtrations durin casting) or model it as an open shape that then is closed tobridge the final gap (much more complex and still not as good a seam).
Assembling the Mold IV- Chudai- the Pedestal


Also not overly complicated. The central insert was quite a last minute addition. I will upgrade it to work just like the firebox insert soon enough. As for the purpose I will explain it in greater detail later but it's basically to be able to add an electrical lamp later on (there's an alternative part in the files if you want to stick to candles and have no need for the central insert)
Getting Ready to Cast


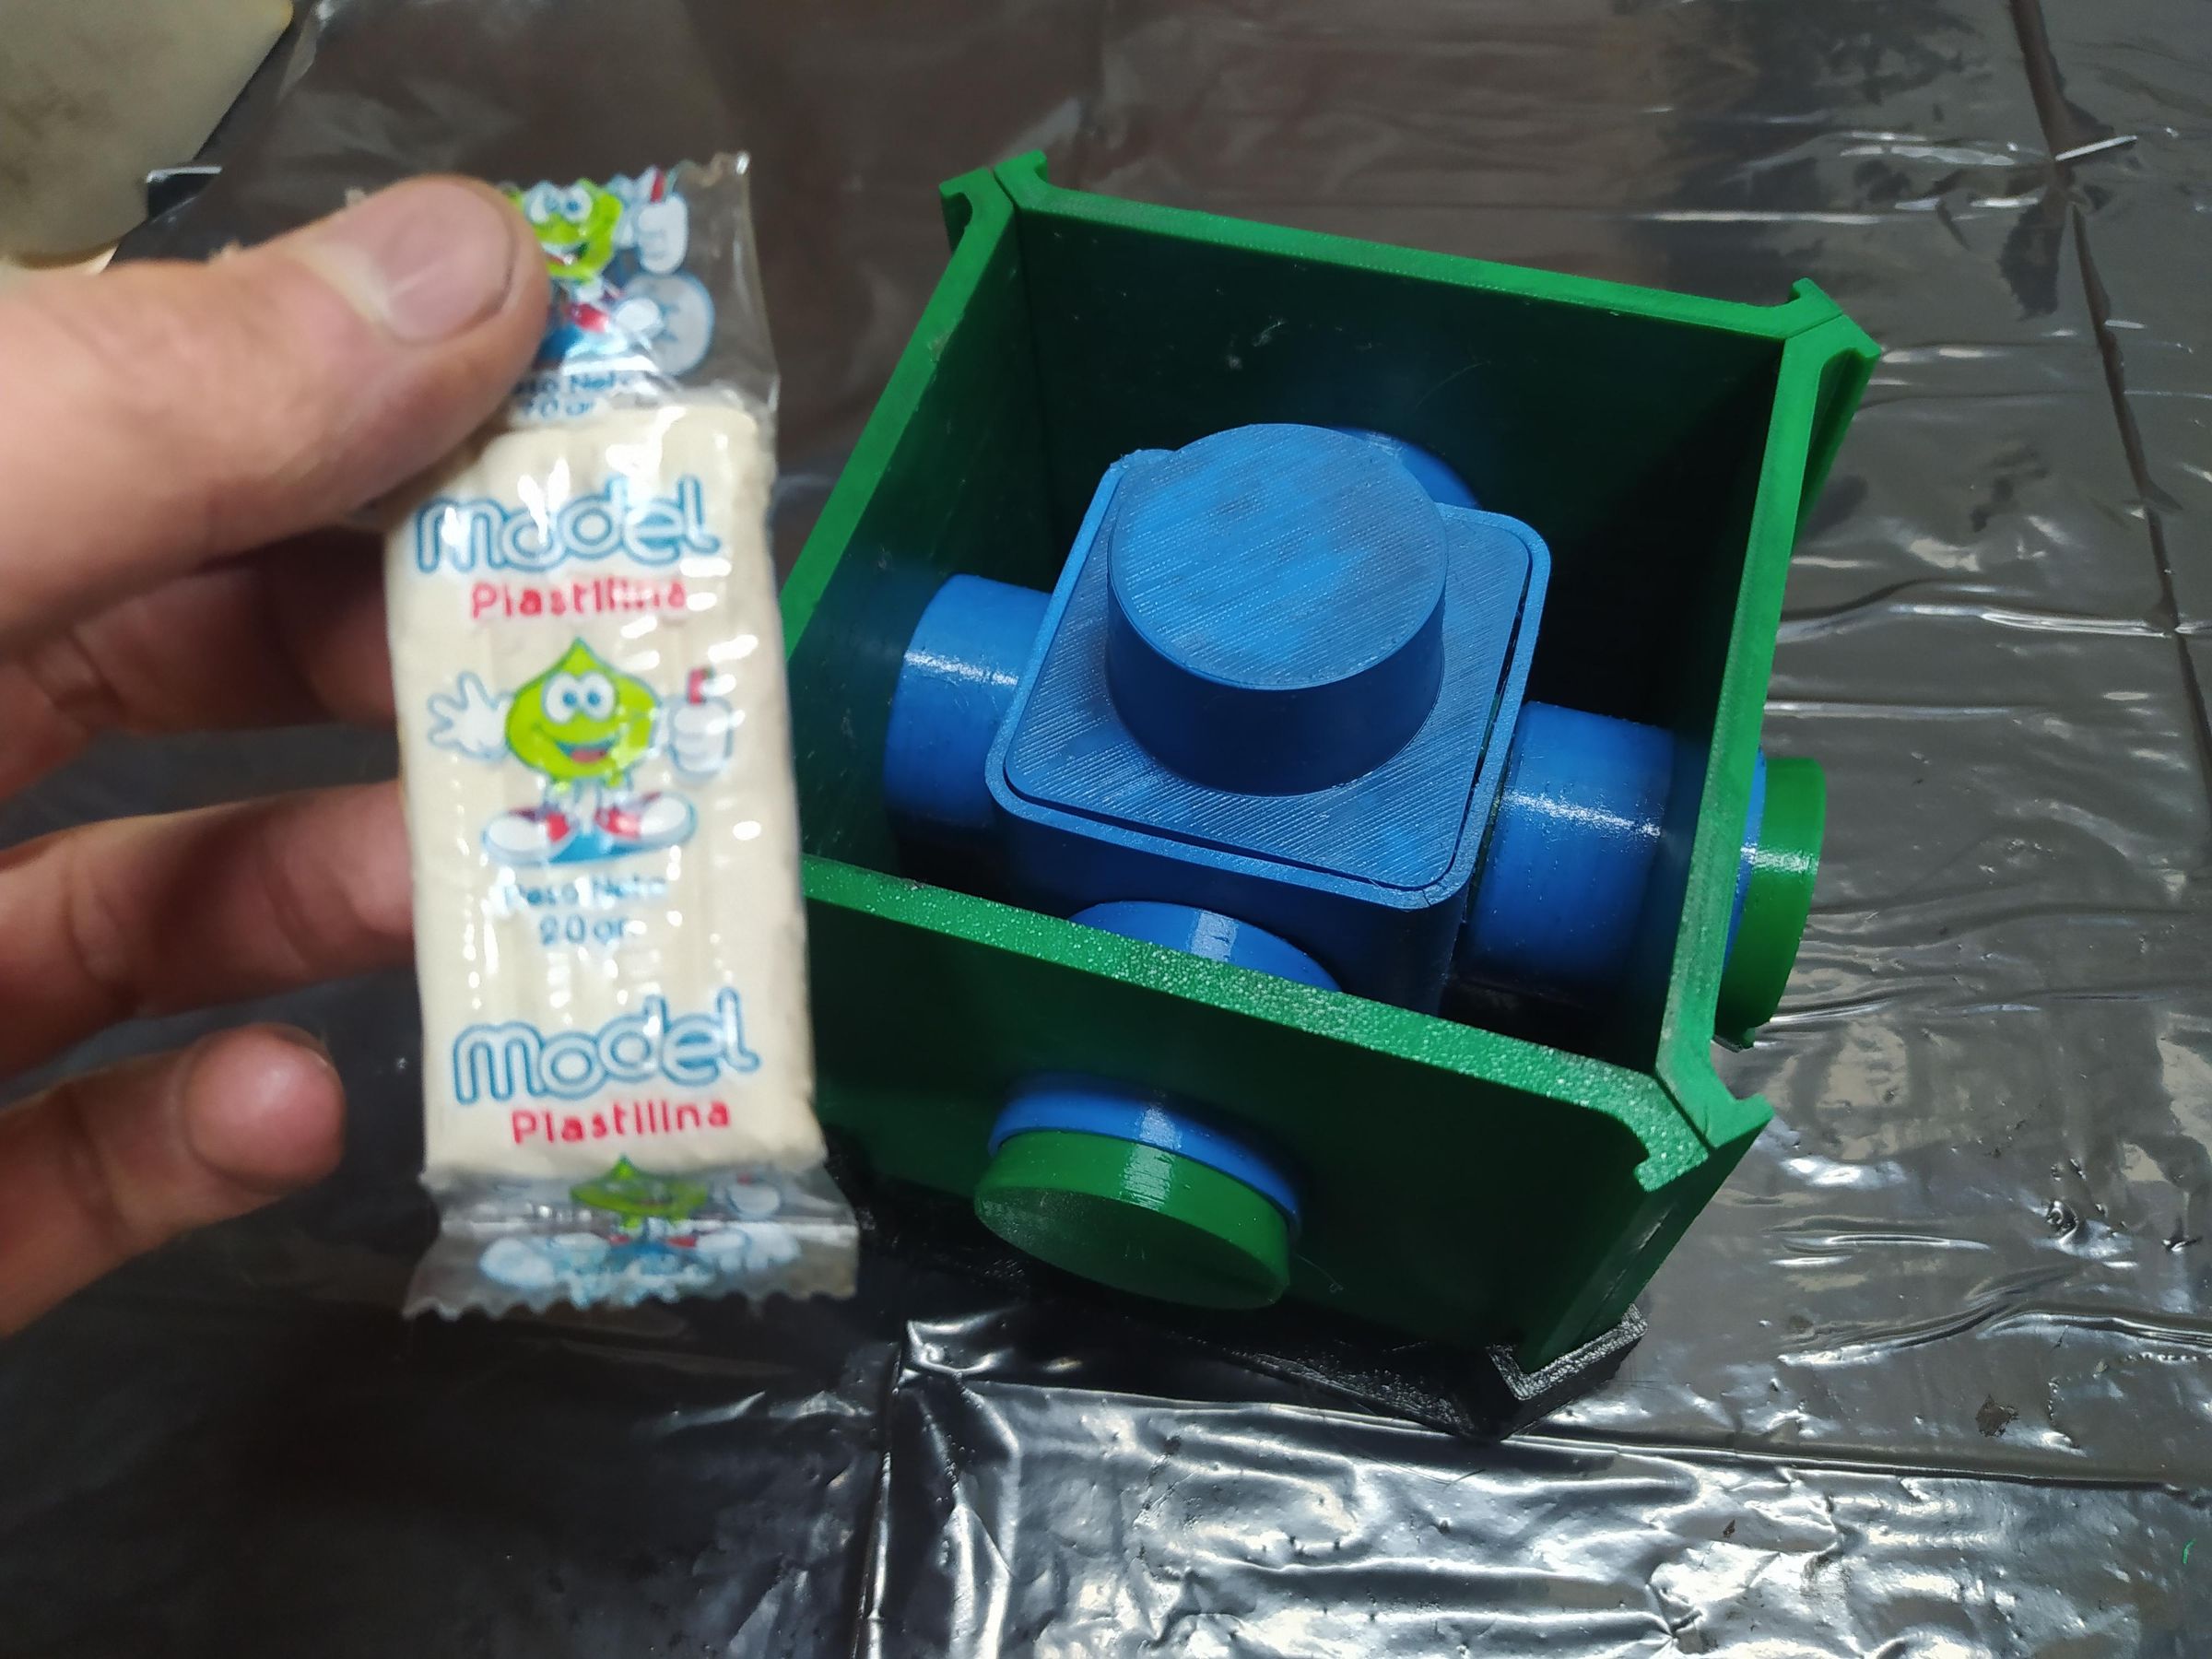


First thing first, get a nice plastic bag, a tarp or something similar. The future you that has to do the cleanup will thank you.
Next make sure you have your safety gear in hand. You will need it for mixing the concrete. It's not the usual ¨just a precaution¨ case. There will be dust in the air and you will get your hands dirty with cement. And its pretty irritating, even without the long term effects. Think like sandpaper hands afterwards. So yeah, get some gloves. And glasses, and a dust mask.
Then start preparing the molds for casting. You want to oil each part thoroughly, even in the parts that wont be in contact with the casted parts. Why? because any splatter or filtration wont stick or damage them as much that way. And Later you can crub them clean easily by just using some dishsoap. Aim for an even sheen of oil without any pools. Use a dry napkin or similar to wipe off the excess.
Next you can assemble the mold set as shown before in the pictures. Of course less glamourously so now because everything is oily (even you). The two additional steps in this case are: to tie the cord around the firebox to keep the side-hole supports in place and to secure the TPU flap at the bottom of the roof mold with tape.
Then, once all parts are in their place you can add plastiline if you have some. Anywhere on the seams where you see visible cracks. Again, just enough to fill the gaps, then remove the excess. The Plastiline works well in this situation because it's also oil based so it isnt affected by the oily mold walls.
And that's it! you are now ready to cast your lantern.
Preparing the Mix


Once you have your molds ready to go you can start preparing the concrete mix.
Making it is pretty straightforward. Specially if you know there is no single perfect ratio of cement to sand. As I mentioned before you can aim for anything in between 1:1 to 1:1,5 (cement to sand) and you won't mess it up.
The only thing to watch out for is the water content. Don't add it all at once. Mix everything well, add most of the water, mix again and use the remaining water to adjust the texture.
The idea is to get it malleable enough to flow into the mold and not much else. As long as you lean for it to be a little on the thicker side you will be in the clear (texture will be similar to mashed potatoes).
If you add too much water the aggregates (stone and pebbles) start to separate and decant to the bottom (which is very bad for casting).
Having said that, here are the amounts I used, measured by weight:
- 2.75kg of cement,
- 4,15kg of sand
- 1,25kg of water.
It's a single full bucket with a ratio of 5:7:2 concrete to sand to water, mesured by volume,
Pour, Shake,Repeat


Once the mix is ready you can start the pouring. Or rather, the spooning of the concrete into the molds.
It's best to work in stages. Add some mix. Make sure it is distributed evenly, tap the walls to release any bubbles and then continue.
This is particularly important for the firebox. Use a stick or a wire to make sure its completely packed around the side holes. Tap the sides of the mold thoroughly too to help any bubbles rise to the surface.
I thought I had done enough tapping and shaking myself and I still got some bubbles. So keep at it for as long as you have patience for.
And ..thats about it. I guarantee it will be a little bit anticlimactic, there is just not much more to it. Now it's just a matter of letting the concrete cure.
Initial Curing

After the hectic mess that is doing the casting comes a rather dull part.
First comes the cleaning. Remember not to wash any of the items used for the concrete mix in the sink as the cement can clogg the drain. Do it outdoors with plenty of water.
Next comes the waiting. Leave the molds alone for 48 to 72 hours for an initial curing. You don't want the concrete to dry out or get too hot/cold so a place in the shade that stays tempered is ideal. Another thing you can do is to cover the molds with plastic to keep the moisture from escaping. (the concrete does not cure as it dries but from a chemical reaction that requires water. If it dries up too quickly the reaction stops).
Its also important not to move the molds during the initial curing so pick a spot where they wont be a nuisance!
Once the 3 days are up the concrete will have reached about 50% of its final strength, which makes it safe for the big reveal!
Demolding I- Hoju -the Top Ornament


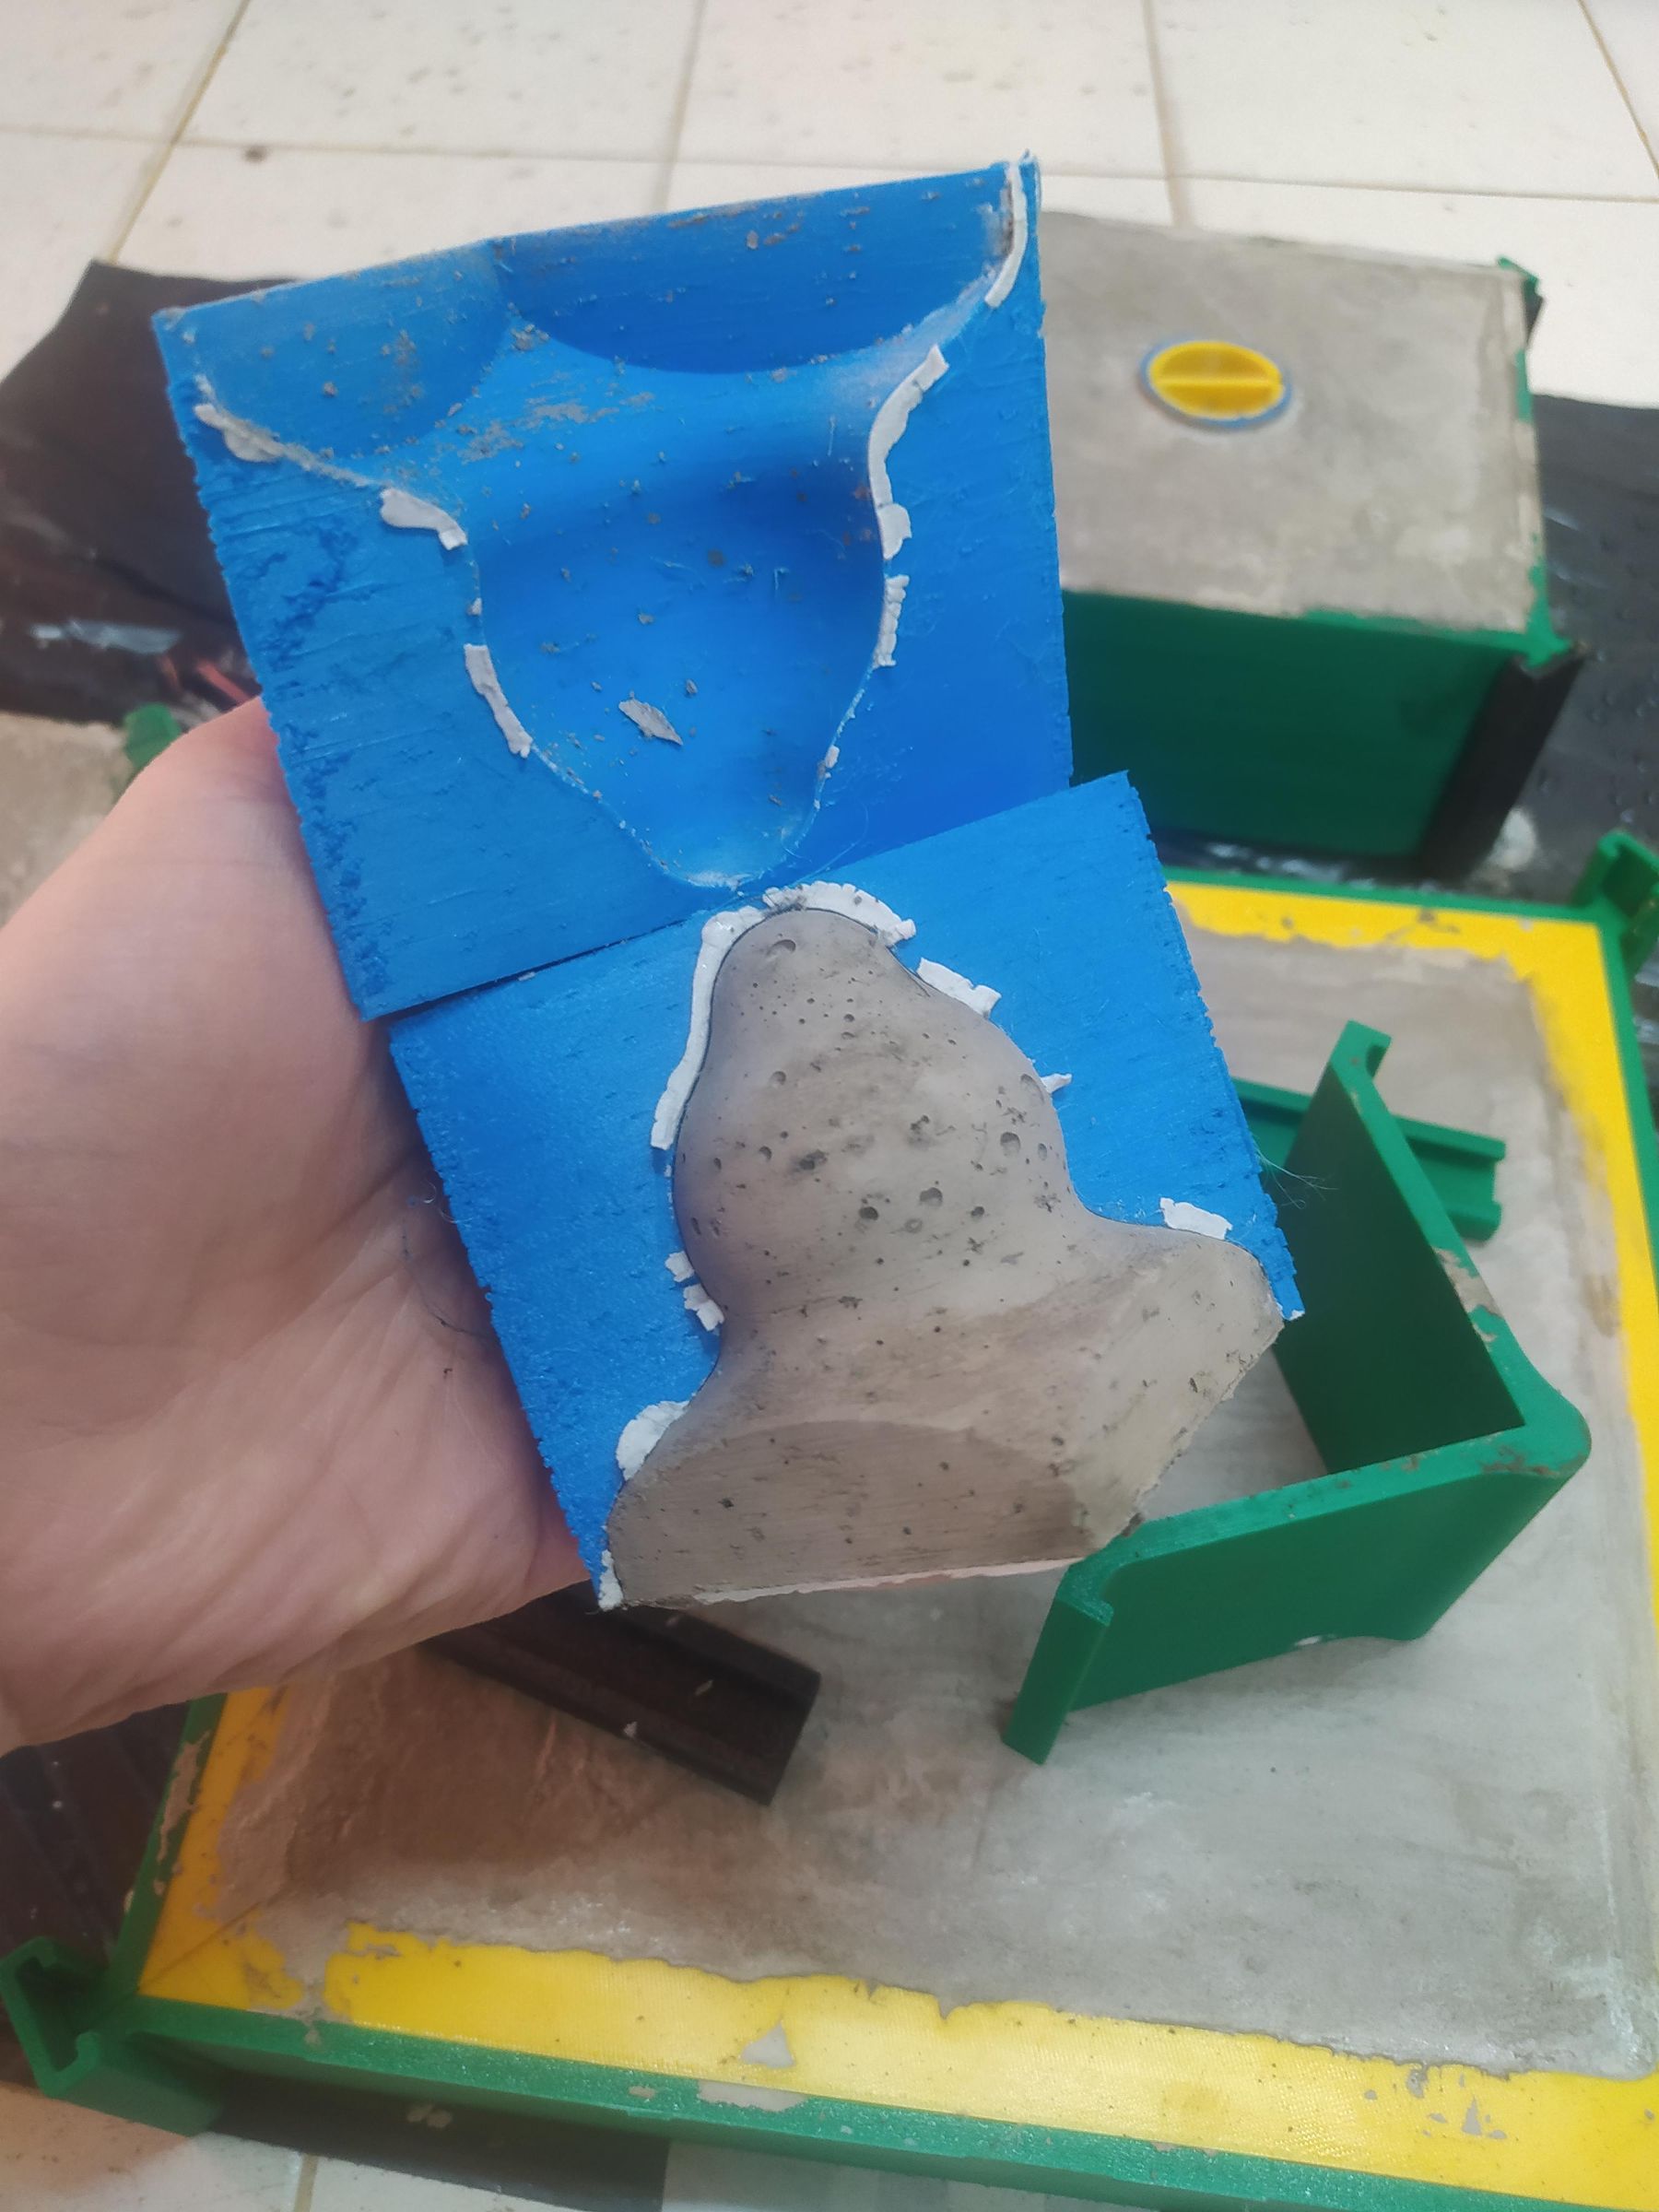

I apologise in advance for the quality in some of the following pictures. But you see, you have to put it into context
As much as I wanted to document the process, for me this was the culmination of several years of on an off efforts. Needless to say I was very eager (and nervous) to see it demold and most importantly if it would demold.
So I was very relieved when this fist part came out cleanly, barely sticking to the TPU and looking amazing.
Demolding II- Kasa-The Roof


By now I was pretty much in a demolding frenzy. It was looking pretty much like a christmas gift unwrapping, with dicscarded mold parts being tossed aside left and right.
Luckily, this part was as easy to de-mold as the other one. Moreover I was surprised to see the plastiline had done a wonderful job at preventing any major filtrations.
All in all, aside from a little cavity in one of the corner the roof came out great which leads to...
Demolding III-Uke-The Pedestal


Now you might be wondering why I skipped the order and went for the pedestal instead of the firebox.
Well, I was nervous. I knew the firebox was the make-it-or-brake-it section. The hardest features to demold had to be the inserts and I was very wary of the fact.
And for a good reason. As I started to demold the pedestal all parts but the insert sleeve started to come out without a hitch. But when it came to the insert it wouldnt budge.
I might have panicked if I didn't half expected it. I had some hopes that the flexibility of the sleeve would be enough but as it was a last minute addition I hadn't applied the same method as in the firebox. So hope was still there.
I left the insert inside ( I later cut it out in pieces) and went to face the final boss.
Demolding IV- Hibakuro- the Firebox


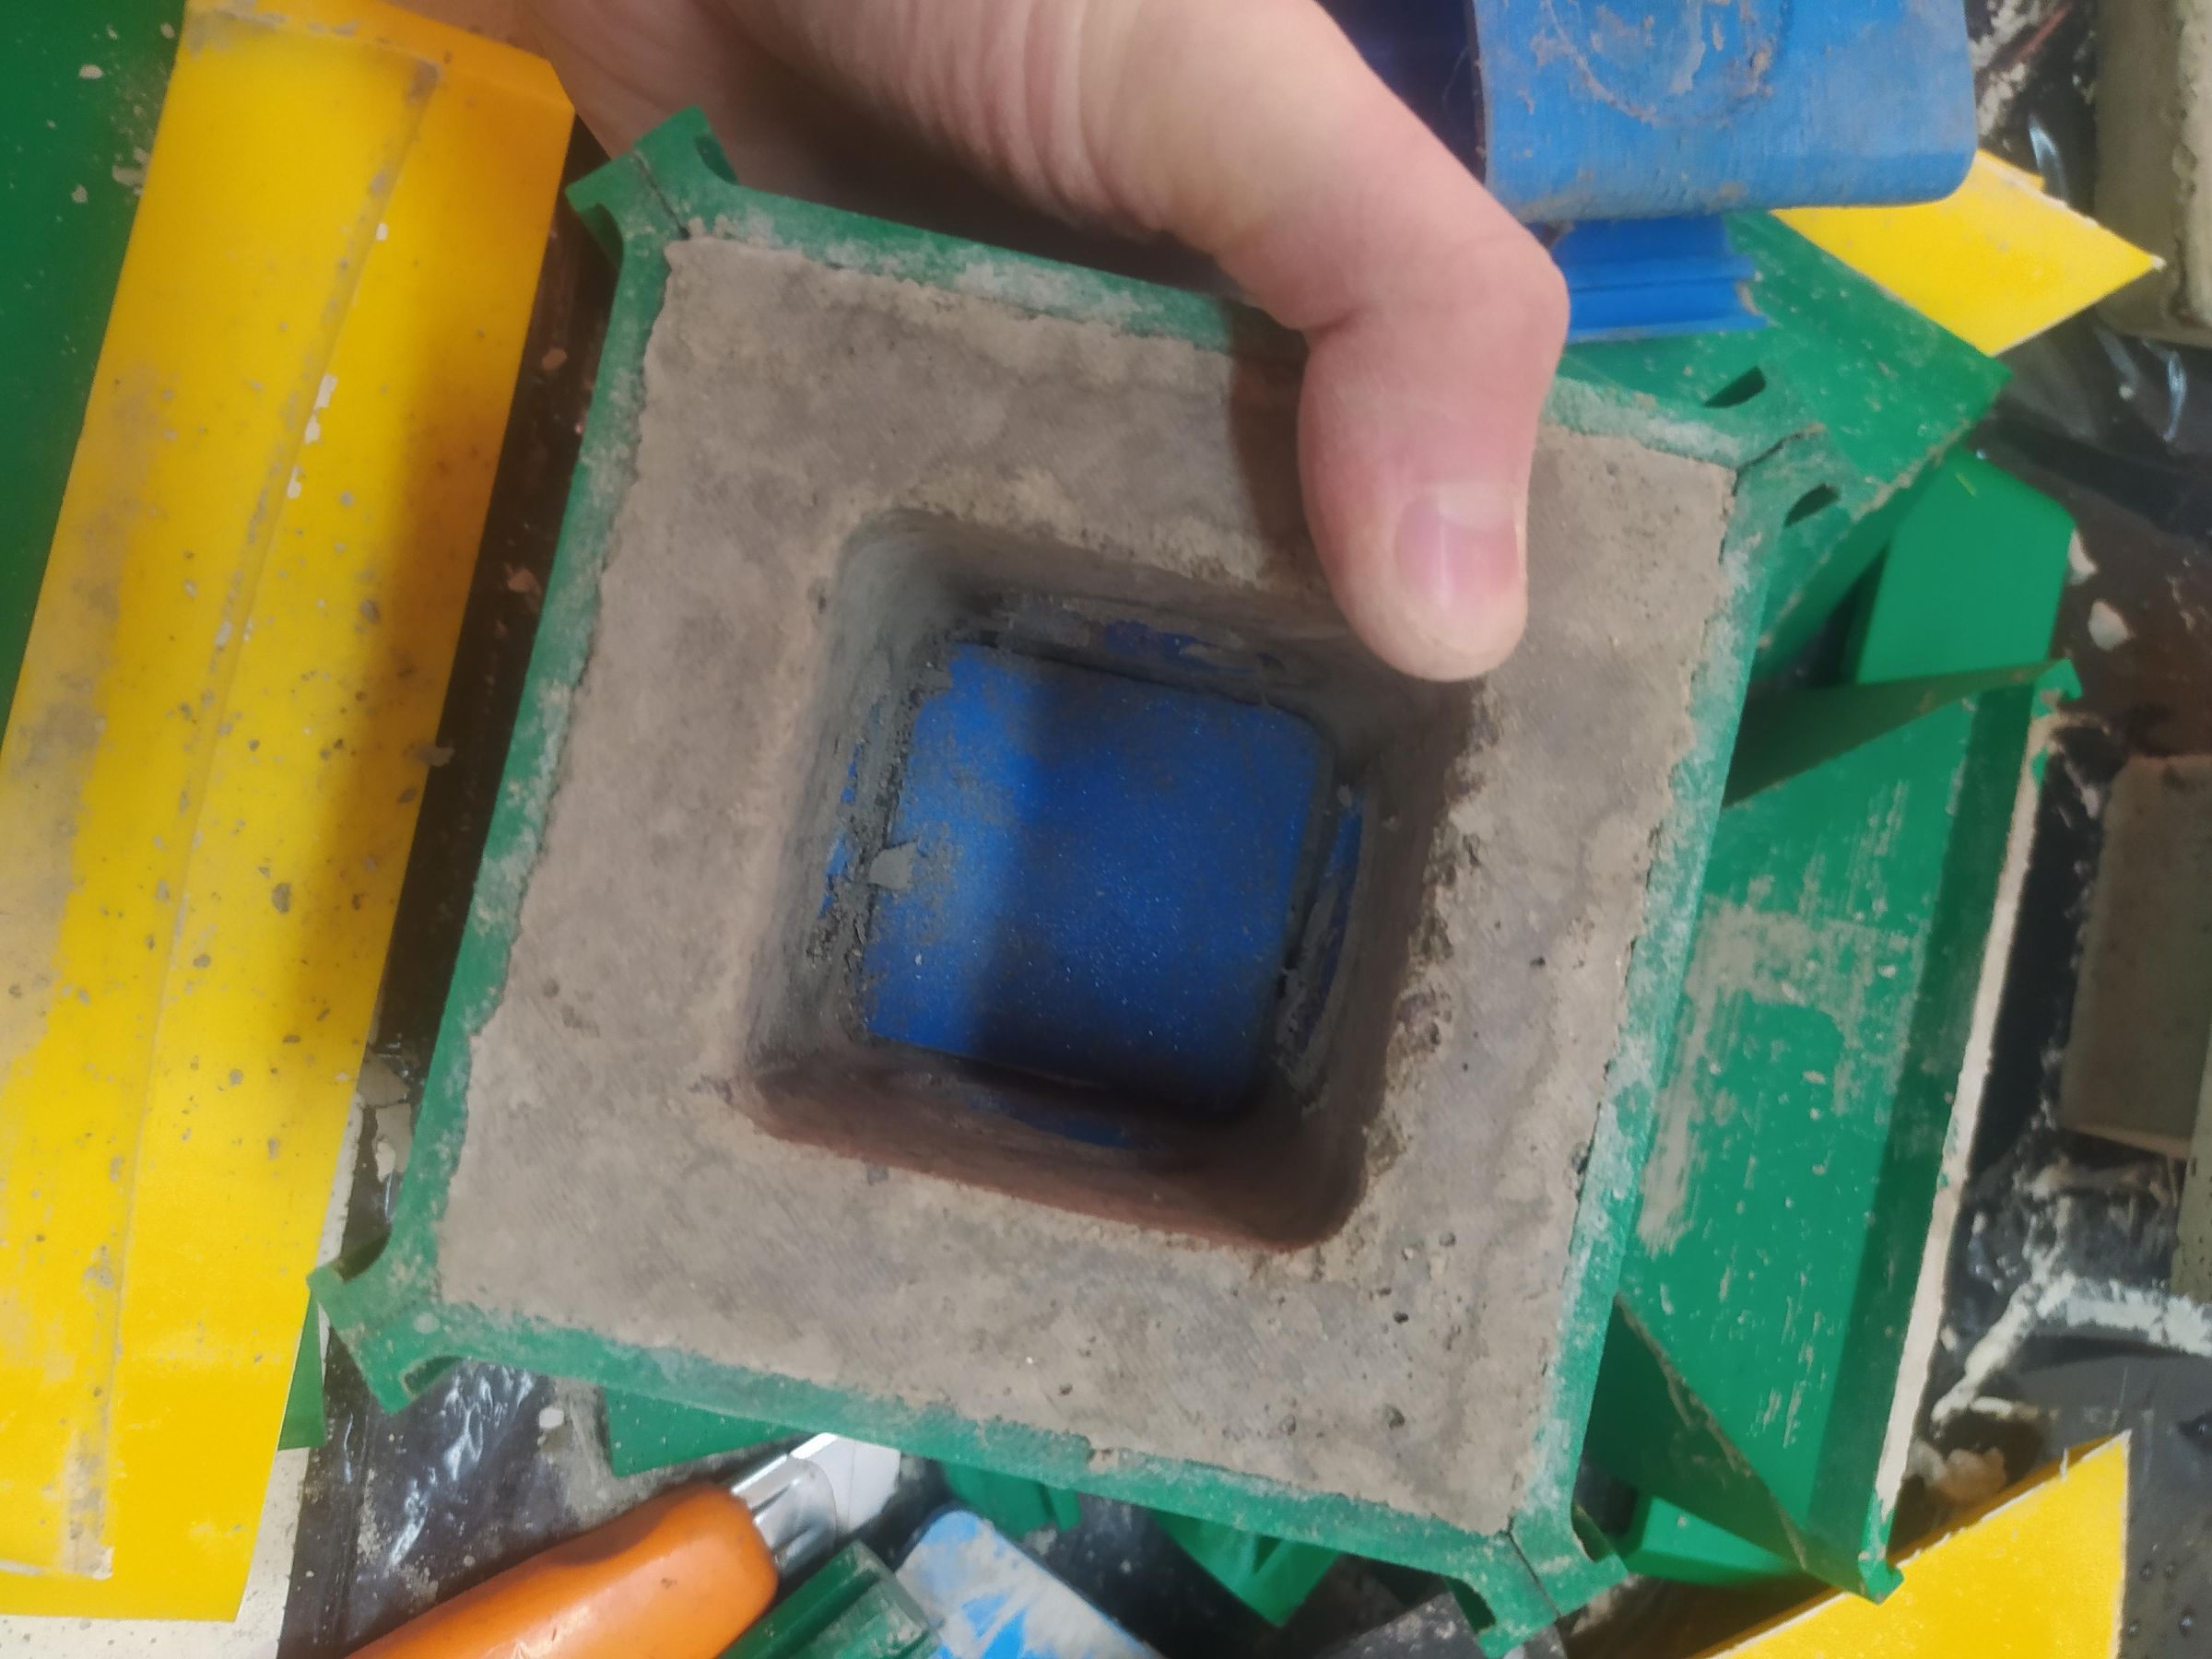


This was it. The most complex part of the lot. It was time to see if the planned demolding sequence would work as intended.
And to the greatest extent it did! the side holes internal supports slid right off and the base was quick to follow.
Next were the internal supports for the central insert. The big one was very easy to pull out. The small one that is also a bracket was slightly harder, but nowhere near what I had feared (I was worried filtrations might get it stuck).
Then was the moment of truth, as I began to unwrap the insert sleeve from the internal walls. It worked perfectly, all without a draft angle.
The top cap of the insert followed soon , after some pressure from the outside, and all that was left were the side holes.
These would prove to be a little more difficult. The trick turned out to be to not try to release the whole perimeter then work your way inwards. Rather you had to separate the sleeve from the wall in a single spot to create a groove and then push to have it propagate all the way down. Once that happens the pressure releases and the whole part comes right off.
By that time I figured the trick however, I had already broken two of the sleeves trying to demold them.
It was a little setback but again, I knew it was a possibity. I was mostly hoping I didn't have to cut the sleeve and add a bracket like I did with the central insert. If flexibility was enough then all the better!
The central insert working was key because it showed that the path for full mold reusability and fuss-free demolding is entirely within reach.
And so I finally, after more than three years and on the very first cast had a perfectly good looking concrete japanese lantern.
What are you waiting for?
Taste of Success and Back to Curing


Now you will probably go a little crazy (like me) and want to see how your lantern looks placed on the garden.
It doesn't do much harm provided you take care while moving it but remember: it is not fully cured yet. If left to air out or in direct sunlight it could dry out too quickly and lead to cracks and a weakened internal structure.
So take some pictures, show friends and family your creation and then carefully get the lantern back into a humid, temperate place.
One thing you can do is, like I did, place the whole lantern inside a plastic bag along with a drenched sponge or rag)
After 7 days have passed since the casting the concrete should have around 75% of its strength and should be ready to be transported and placed on your spot of choice.
(note: it actualy takes about 28 days for it to fully cure)
So maybe you should hold up until then before...
Making It Glow!


I don't know about you, but when I wanted a japanese lantern I was not just looking for an ornamental piece. I really liked the idea of it to perform its intended purpose.
One option is of course candles! As you can see in the pictures. It looks outstanding and can work really well for special occasion.
However I wanted it to be lit more often. So, while doing the final stretch of the mold design I was looking for options to install LED lighting.
Thats where I found this solar lights which -very conveniently- had a nice cilindrical shape and also showed the measurements. So that last minute change to the pedestal I mentioned? Is the necessary cavity required to install a solar light andupgrade your japanese lantern to a fully automated garden lantern!
I haven´t received mine yet but I will make sure to add some pictures of the results as soon as I have them.
Upgrades!

Here are the new versions of the inserts, made so they demold easier and don't well break in the process.
I wanted to put them out there just in case someone is already thinking of making one. I haven't had time yet to print and test the new version so consider it a beta. I will do a more detailed explaination of the changes and add some pictures once I have.
Downloads
Zen Intensifies

Thanks for reading my Instructable!
I dont envy your printer-owning friend who might soon be tasked with printing a full set of molds.
Jokes aside, I was really surprised with the results and how easy it was to cast, specially given I didn't have all that much experience with casting concrete.
I would love to see someone else's dream of owning a japaneese lantern come true, so make sure to share the pics if you do.
Thanks again for reading and keep making!