DIY Mirror Nickel Plating Guide for Tools (Low Current Density)
by kovancapol in Workshop > Metalworking
57 Views, 2 Favorites, 0 Comments
DIY Mirror Nickel Plating Guide for Tools (Low Current Density)

WARNING: Safety First!
Nickel electroplating involves chemicals that require careful handling. Solutions containing nickel salts are toxic if swallowed, can cause severe skin allergies (nickel itch), and are classified as suspected carcinogens.
Always strictly adhere to the following safety protocols:
• PPE Required: Always wear heavy-duty nitrile gloves, safety goggles, and a chemical-resistant apron or long sleeves.
• Ventilation: Work exclusively outdoors or under a highly efficient laboratory fume hood. Do not inhale the vapors or mist generated during electrolysis.
• No Air Sparging: To minimize hazardous chemical aerosols and mist, avoid using air sparging (air bubbling) in the tank. Increase cathode rod movement speed instead to agitate the electrolyte safely.
• Disposal: Never pour used electrolyte or rinse water down the household drain. Collect all chemical waste in a designated sealed container and dispose of it at a local hazardous waste recycling facility.
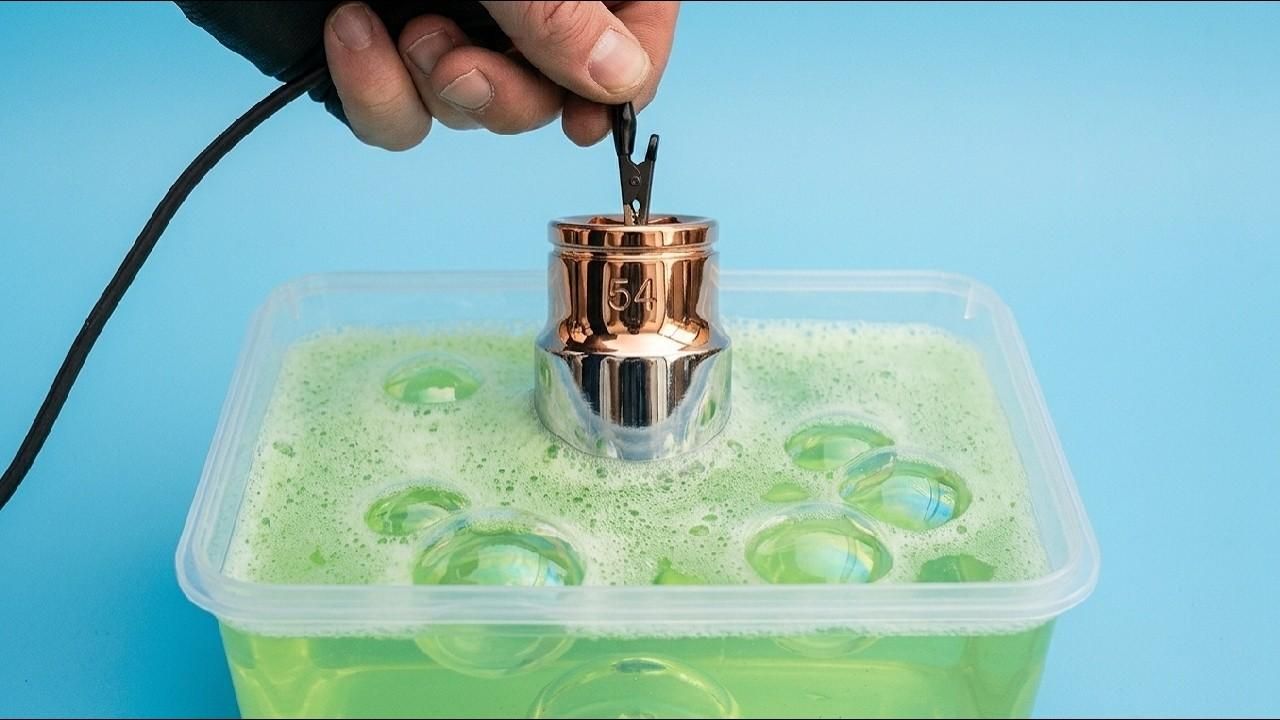
Electroplating at home allows you to create durable and highly protective decorative coatings on metal parts. This guide provides a step-by-step chemical workflow for modifying a standard Watts nickel bath to achieve a mirror-like finish on hand tools and hardware. By introducing specific organic brighteners and surfactants, the solution is optimized to work efficiently at very low current densities (0.1-0.5 A/dm2). This modification eliminates the need for professional industrial equipment, making it highly accessible for workshops and garages. The text instructions below cover the complete electrolyte preparation process scaled precisely for a 1 Liter working volume.
Supplies

Chemical Reagents for 1 Liter Bath:
- Nickel Sulfate (NiSO4 * 7H2O) - 180 g
- Nickel Chloride (NiCl2 * 6H2O) - 45 g
- Boric Acid (H3BO3) - 35 g
- Saccharin Sodium Salt - 2.0 g
- Commercial Formalin (37% Formaldehyde solution) - 2 mL
- Sodium Lauryl Sulfate (SLS) powder - 0.5 g
- Distilled Water - approximately 1.5 Liters total for solutions and final top-up
Laboratory & Safety Equipment:
- Digital scale with 0.1g or 0.01g precision
- Glass beakers (100 mL, 250 mL, and 1000 mL) or a plastic plating tank
- Graduated laboratory syringes (1 mL, 10 mL, and 50 mL)
- Laboratory hotplate stirrer or a heat source with a thermometer
- Paper coffee filters or quantitative filter paper
- Pure Nickel Anodes wrapped in polypropylene filter bags
- Adjustable DC Power Supply with fine current control
- Personal Protective Equipment including nitrile gloves, chemical apron, and safety goggles
Mixing the Base Watts Nickel Solution

1. Pour about 500 mL of distilled water into your main 1 Liter plating beaker and heat it up to 60-70 C.
2. Add 180 g of Nickel Sulfate (NiSO4 * 7H2O) and stir until completely dissolved.
3. Add 45 g of Nickel Chloride (NiCl2 * 6H2O) to the same beaker and stir until fully dissolved.
4. Set this base solution aside for a moment. Do not add the rest of the chemicals yet.
Preparing Stock Solution B (SLS Surfactant, 10g/L)

The surfactant prevents pitting (gas bubbles sticking to the part). Because it is used in tiny amounts, it requires pre-mixing.
1. Weigh exactly 0.5 g of dry Sodium Lauryl Sulfate (SLS) powder.
2. Pour 50 mL of separate warm distilled water (40-50 C) into a small container.
3. Add the SLS powder and stir gently. Avoid rapid movements to prevent heavy foaming.
4. You now have 50 mL of Stock Solution B.
5. For our 1 Liter bath, we will later measure and use exactly 15 mL of this solution.
Adding Saccharin and Filtering the Bath

1. Let your main nickel solution from Step 1 cool down to below 40 C.
2. Dissolve 2.0 g of Saccharin Sodium Salt in 30-40 mL of warm distilled water.
3. Pour the dissolved Saccharin into the main nickel solution and stir well.
4. Crucial Step: Filter the whole mixture through a dense paper filter or cotton pad into your final plating tank.
5. Note: You must filter the solution strictly before adding the surfactant, otherwise the filter will get completely blocked by foam.
Preparing and Adding Stock Solution a (Formalin 1:50)

Formalin cannot be dosed directly into 1 Liter of water without ruining the precision. We must make a diluted stock solution first.
1. Take exactly 2 mL of commercial 37% Formalin using a lab syringe.
2. Add 98 mL of distilled water into a small container and mix thoroughly. You now have 100 mL of Stock Solution A.
3. Measure exactly 40 mL of this prepared Stock Solution A and pour it into your filtered main plating tank. Stir gently.
Adding Boric Acid, Surfactant, and Final Dilution

1. Dissolve 35 g of Boric Acid (H3BO3) in 150-200 mL of separate hot distilled water until the liquid becomes perfectly clear.
2. Let the Boric Acid solution cool down slightly, then pour it into your main plating tank.
3. Use a syringe to measure 15 mL of your prepared Stock Solution B (SLS) from Step 2.
4. Slowly inject the 15 mL of SLS into the plating tank. Stir very gently without rapid movements.
5. Top up the tank with distilled water until you reach the exact 1 Liter mark on your tank or beaker. Give it a gentle final mix.
Working Parameters & Maintenance


To achieve the professional results shown in the video, follow these strict rules:
- Current Density: Keep it low, between 0.1 - 0.5 A/dm2.
- Temperature: 20-30 C (Standard room temperature).
- Acidity (pH): Maintain between 4.0 - 4.5. If the nickel coating loses its shine and looks cloudy, add a few drops of 10% Sulfuric Acid (H2SO4) to lower the pH back into range.
- Agitation: Do NOT use heavy air bubbling (it creates endless foam). Use only a slow, gentle mechanical rocking or swinging of the part.
- Deposition Speed: Around 1.5-2.0 microns per hour at 0.2 A/dm2.
Maintenance over time:
- Formalin evaporates: Every 4-5 hours of continuous electroplating, add 10-15 mL of Stock Solution A to the bath.
- Surfactant depletion: Only add 2-3 mL of Stock Solution B if you start seeing tiny gas pits forming on your tool.