Laser Engraved Coated Stainless Steel Tumbler
by thunderlaser-nolan in Workshop > Laser Cutting
60 Views, 0 Favorites, 0 Comments
Laser Engraved Coated Stainless Steel Tumbler

A coated stainless steel tumbler is a practical item that becomes much more personal with a custom laser-engraved name, logo, or graphic.
This project uses a Thunder Bolt and a rotary attachment to engrave the coated surface of a tumbler, revealing a clean contrast underneath. It is a great option for personalized gifts, branded drinkware, event items, and small custom orders.
Once the basic setup is ready, you can easily change the artwork for different names, patterns, or business logos while keeping the same workflow.
For more laser engraving ideas and machine information, explore the Thunder Bolt series and browse more projects in the Inspiration Library.
Supplies
- Thunder Bolt laser cutting machine (or another Thunder Laser model)
- Coated Stainless Steel Tumbler / Rotary Attachment
- LaserMaker software (free) — LightBurn or RDWorks also work
- Project file (.dxf), attached to this Instructable
Laser settings for 3mm plywood (engraving): speed 800mm/s, max power 35%, min power 10%, LOW air assist.
Laser settings for 3mm plywood (cutting): speed 10mm/s, max power 30%, min power 10%, HIGH air assist.
Install the Rotary Attachment & Position the Tumbler


Install the rotary attachment on the Thunder Bolt and make sure it is connected properly before placing the tumbler.
Mount the coated stainless steel tumbler securely on the rotary attachment and align it so the engraving area faces upward. Check that the tumbler rotates smoothly, stays level, and does not slip during processing.
Import & Adjust the Design File
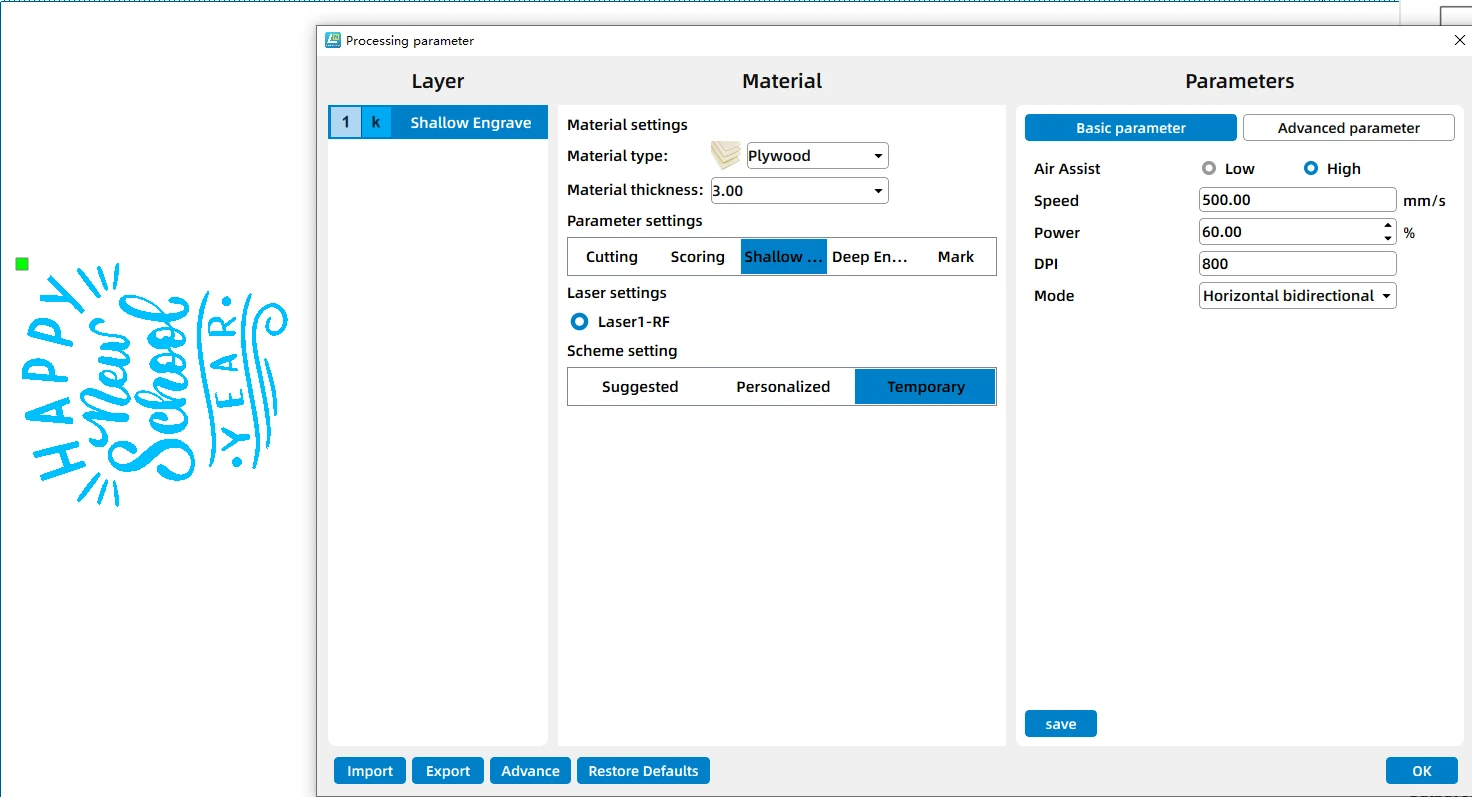
Import your design into LaserMaker and adjust the artwork size to fit the available engraving area on the tumbler.
Check the artwork position and orientation carefully, especially if you are engraving a name, logo, or one-sided graphic. Set the engraving parameters to 1700mm/s speed, 25% max power, 50kHz frequency, DPI 0.02, and 5 passes.
Set the Correct Laser Focus


Set the focus at the center of the coated stainless steel tumbler surface where the design will be engraved.
You can use auto focus first and then confirm the height manually if needed. Since the tumbler is curved, keeping the design within a suitable marking width helps maintain more consistent engraving results across the surface.
Frame the Design & Start Laser Engraving


Run the Frame function first to preview the engraving position and verify that the design sits in the correct area on the tumbler.
Once the position is correct, start engraving at 1700mm/s speed, 25% max power, 50kHz frequency, DPI 0.02, and 5 passes. Monitor the machine during processing and make sure the tumbler rotates smoothly and remains secure on the rotary attachment.
Post Processing


Remove the tumbler from the rotary attachment and inspect the engraved result for clean contrast, clear edges, and correct placement.
Wipe the tumbler gently with a soft cloth to remove dust or residue from the engraved area. If needed, clean the surface again so the exposed stainless steel detail looks crisp and ready for use or gifting.