Team Condor's Aluminum 7475 Competition Alloy
by DMSE OSU Team Condor in Workshop > Metalworking
62 Views, 0 Favorites, 0 Comments
Team Condor's Aluminum 7475 Competition Alloy

Team Condor was tasked with crafting an aluminum alloy with an optimal balance of yield strength, percent elongation, and percent electrical conductivity for a competition amongst peers. The specific criteria are as follows:
- High Al content: alloy must be at least 90% aluminum
- Maximize the .2% offset yield strength (YS)
- Maximize the total elongation (%EL)
- Maximize electrical conductivity
- Thickness of final testing material is 2-3 mm
After investigating the Granta software—which provided baseline information on various aluminum alloys—Team Condor selected to use aluminum 7475-T6 with target composition: 90 wt% Al, 0.18 wt% Cr, 1.9 wt% Cu, 1.92 wt% Mg, and 6 wt% Zn. The alloy was strategically manipulated using thermomechanical processing techniques—homogenizing, rolling, and ageing—to further enhance desired properties. Below are the step-by-step instructions on creating the mighty Al alloy used by Team Condor in competition (2nd place overall):
Supplies


Here are the supplies required to replicate Team Condor’s aluminum alloy:
- Raw Materials: Al, Cr, Cu, Mg, Zn
- Casting Equipment: balance/scale, rectangular casting mold, crucible, tongs, high temperature kiln/induction furnace, PPE/safety equipment (close-toe leather shoes, face shield, safety glasses, heat resistant suit, thermal gloves)
- Rolling: furnace, rolling mill (Team Condor used an International 2050 Rolling Mill with in-line furnace), calipers, tongs, PPE/safety equipment (closed-toe shoes, safety glasses, thermal gloves)
- Homogenizing, Heat Treating, Ageing: furnace, tongs, quench bucket, PPE/safety equipment (closed-toe shoes, safety glasses)
- Metallography: mounting press, grinding station (equipped with 240, 320, 400, and 600 grit sandpaper), polishing station (6-micron diamond paste and extender, 3-micron diamond paste and extender, 0.5-micron colloidal silica solution), etchant (Papageorge two-step), optical microscope (brightfield)
- Testing: MTS Criterion (for tensile testing) with appropriate software to measure yield strength and elongation, Zetec DC-2 (electrical conductivity meter), Wilson Rockwell Hardness Tester
Casting


Commercial pure Al, Cu, and Zn were combined with alloyed samples of 50% Mg in Al, and 20% Cr in Al to create the alloy. Sample metals were massed to account for the aluminum present in the alloy components. Proper mass calculations are recorded in the attached table. The total mass of all components added 1000g. Before adding Al, the Mg and Zn were wrapped in Al foil. The mass of Al foil used was subtracted from amount of pure Al needed, and the resulting mass of Al was added to the induction furnace. 400g of Al was placed in a crucible to start melting. After the initial 400g melted, the remaining 473.6g of Al was added with 19.0g of Cu and 9.0g of Cr. The Mg and Zn samples of 38.4g and 60.0g (tightly wrapped in Al foil) were submerged in the crucible using tongs to prevent them from boiling off. After the solution has melted completely, the fluid was mixed to attempt to disperse the alloy components evenly. The crucible contents were then poured into book molds and allowed to cool.
Homogenization

Subject the aluminum to a low temperature hold before traditional homogenization. Pre-treat the alloy by heating it to 240°C for 48 hours. Then, hold the Al alloy at 470°C for 24 hours. This two-step homogenization process has been shown to effectively reduce dispersoid size. Homogenization after casting allows for a more even distribution of alloying components.
Hot Rolling Reduction
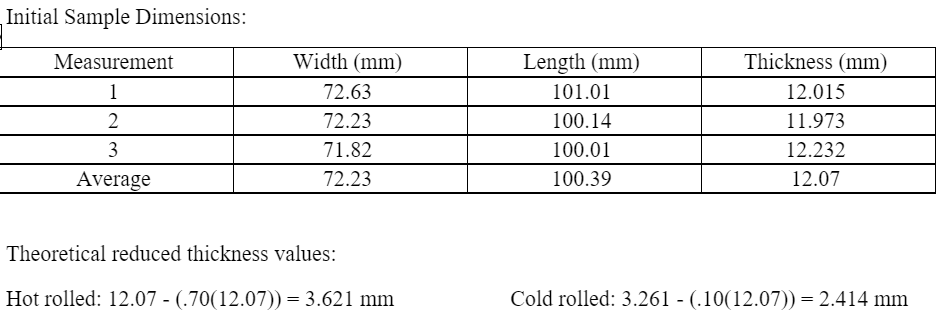

Team Condor's reduction calculations are provided in the table above.
In order to achieve the desired 2-3 mm final sample thickness, hot rolling was required to make major reductions in a short amount of time. Measure the original dimensions, and hot roll at 470°C to achieve a 70% reduction in thickness. The reduction steps used by Team Condor are as follows:
- Roll 0 (“slack roll”): 5% reduction (drop 0.77mm; not counted in total reduction)
- Roll 1: 10% reduction (Total reduction: 10%)
- Roll 2: 10% reduction (Total reduction: 20%)
- Roll 3: 10% reduction (Total reduction: 30%)
- Roll 4: 10% reduction (Total reduction: 40%)
- Roll 5: 10% reduction (Total reduction: 50%)
- Roll 6: 10% reduction (Total reduction: 60%)
- Roll 7: 10% reduction (Total reduction: 70%)
Cold Rolling Reduction

An additional 10% cold roll reduction was performed to enhance strength and produce a clean finish. Ensure that the working piece is within the required 2-3 mm range at the end of processing. Cold rolling was done in .1 mm reductions as follows:
- 12 rolls of accumulating .1 mm reductions for an 80% total reduction (drop 1.2 mm for 10% reduction cold rolling)
Heat Treating & Artificial Ageing
For aluminum alloy 7475-T6, the T-temper designation indicates that the material underwent heat treatment followed by quenching and ageing:
- 1. Solution Heat Treating – 1 hour at 516°C (+/- 10 degrees)
The alloy underwent solution heat treatment. The aluminum was heated to 516°C and held for an hour. This allows the alloying constituents within the material to be taken into solution, thus forming a single phase.
- 2. Quench – 4 minutes, room temperature water
Immediately after the solution heat treating, the alloy was quenched by placing it in room temperature water for 4 minutes. The rapid plunge in temperature maintains the previously established single phase and grain structure.
- 3. Ageing – 5 hours at 121°C
After quenching, precipitation heat treatment (ageing) was performed on the alloy for 5 hours at 121°C. The heat treating + quenching process makes the alloy softer, so ageing the material regains strength.
- 4. Preparation for machining
Once the sample cools, 4-inch sections were cut out of the Al sheet. The cut segments were machined into tensile bars for mechanical testing.
Metallography and Microscopy

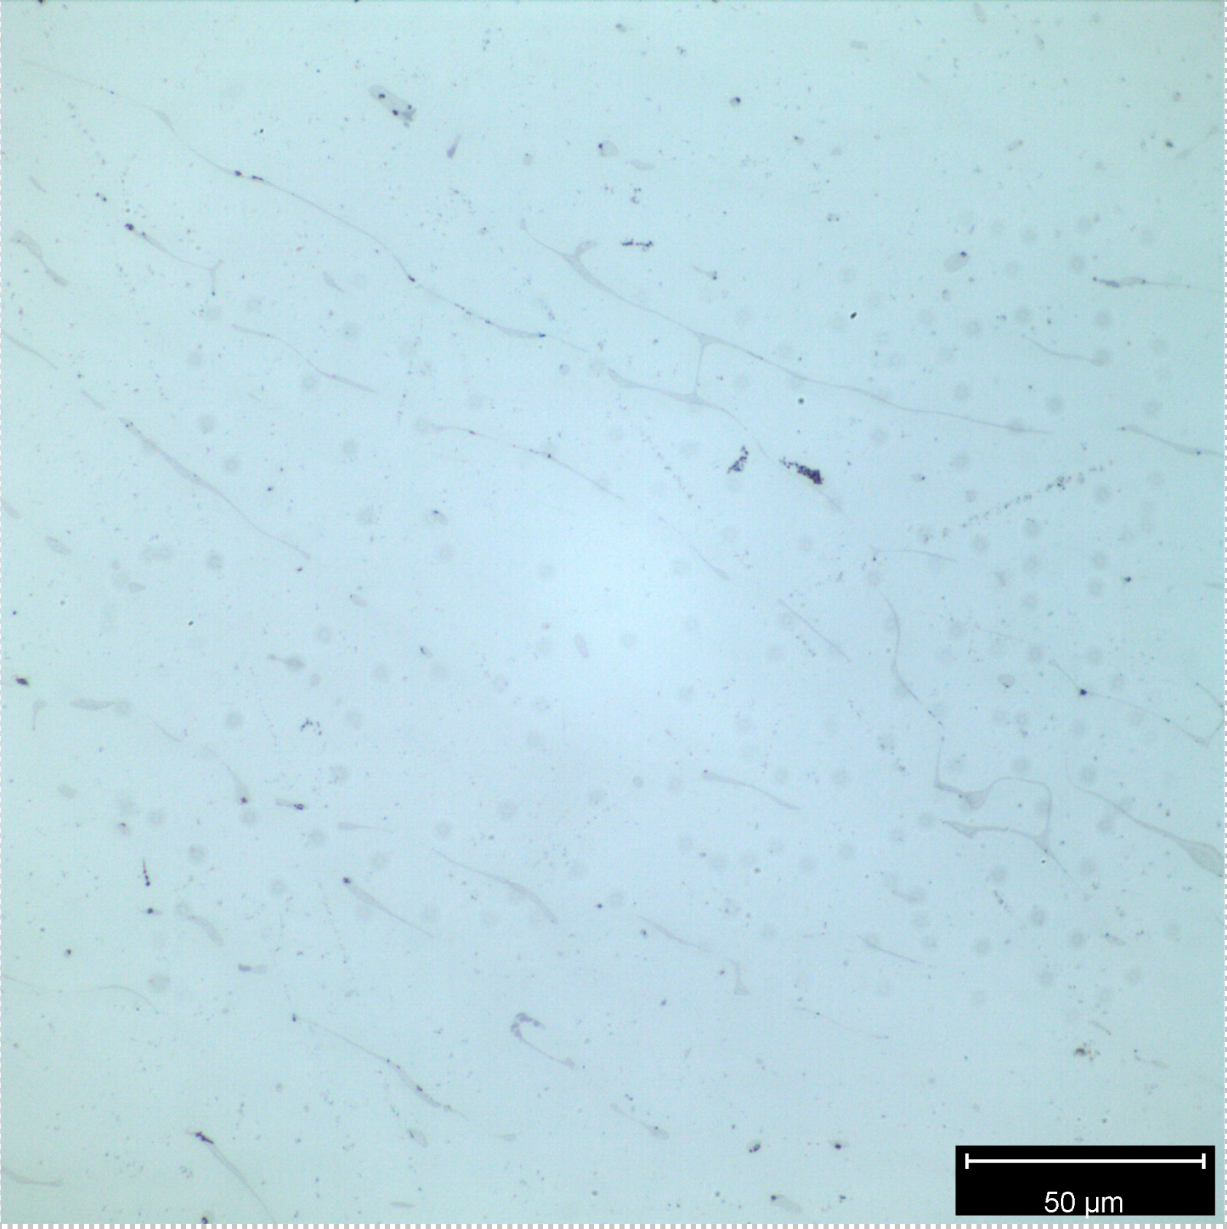
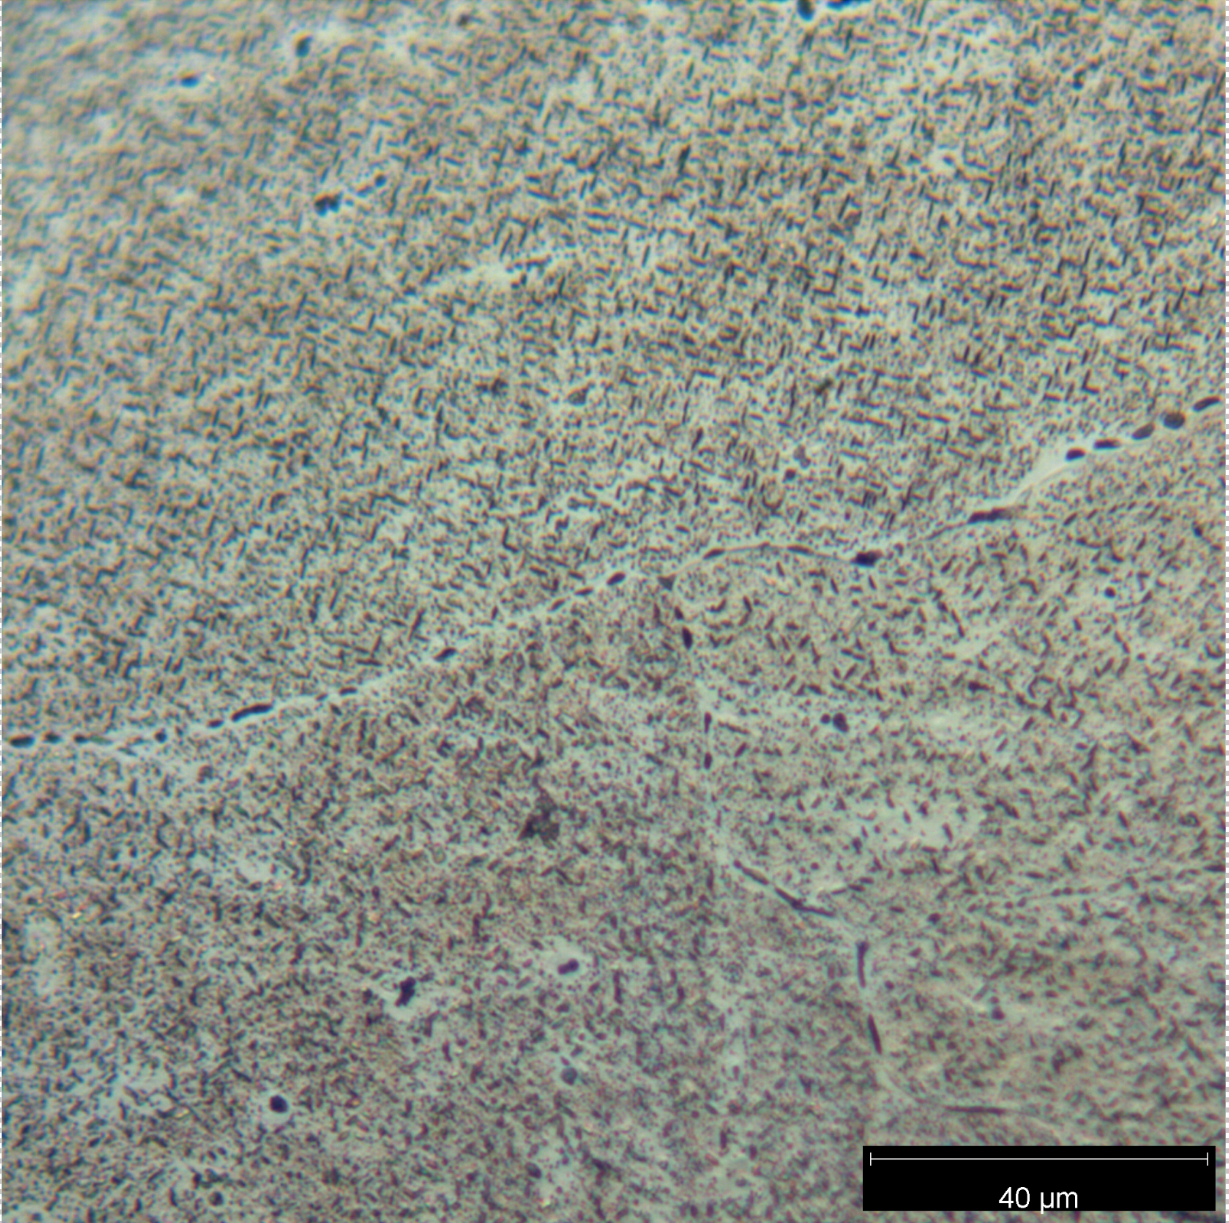

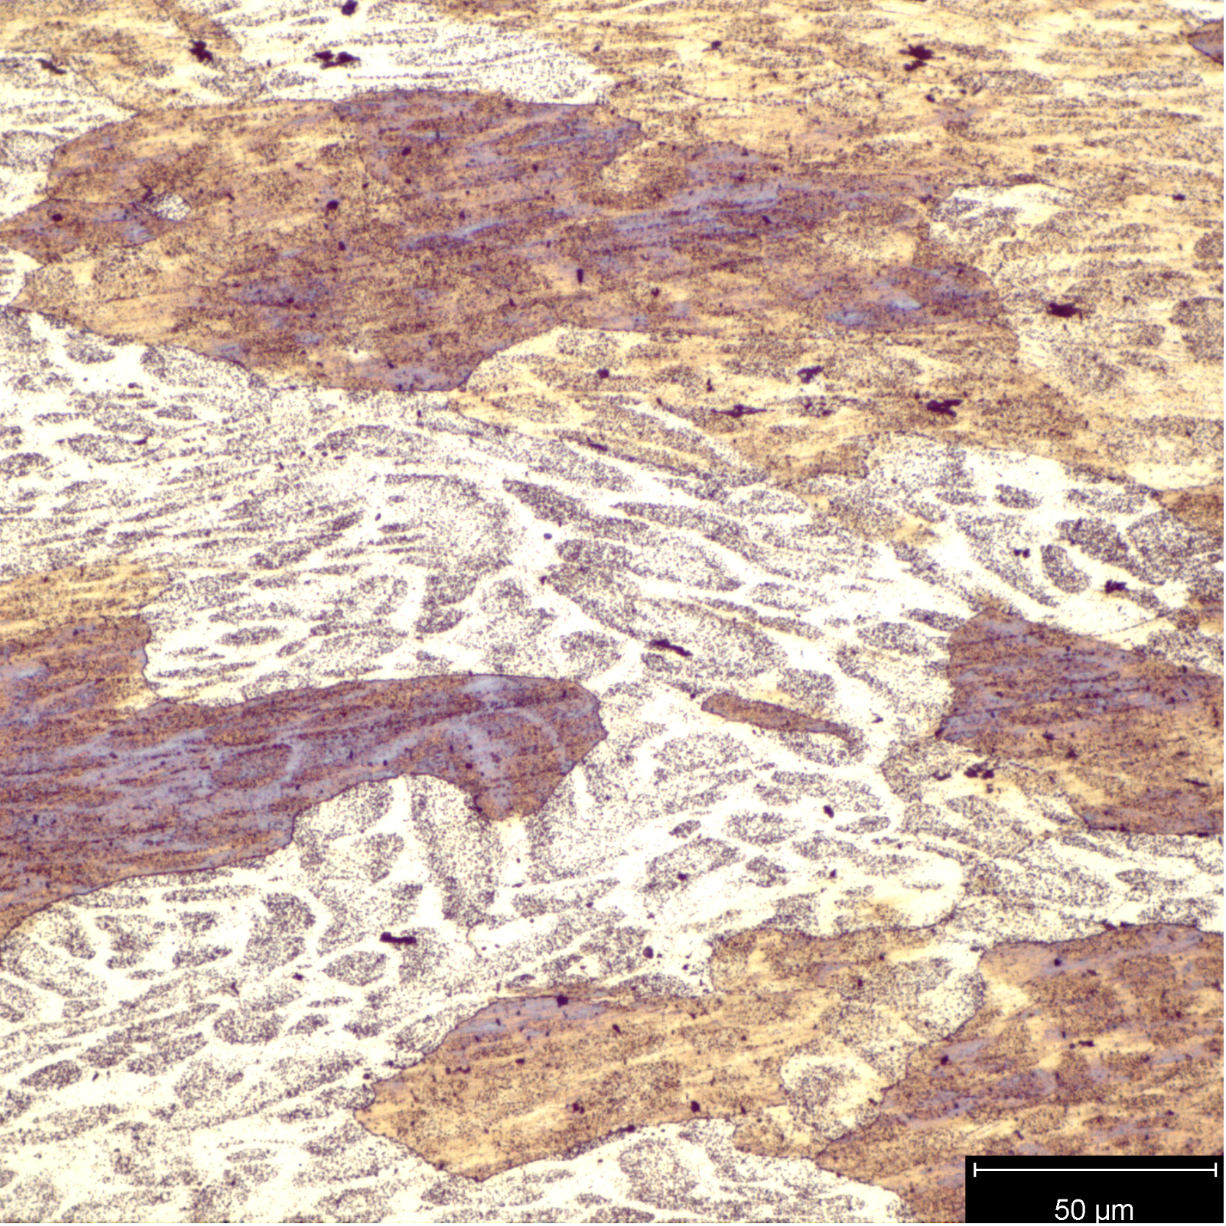

Metallography:
Samples of the alloy were mounted for imaging before and after each thermomechanical process. A total of 7 samples were mounted using heated presses and Bakelite powder. Plastic clips were used to stabilize thinner pieces of metal to ensure the correct orientation. Mounted samples were engraved with a Dremel tool so they could be distinguished, and rough edges were smoothed on a course grit belt sander. Mounted samples include the following:
- As-cast center
- As-cast edge
- Homogenized edge
- Homogenized center
- Hot rolled (80% reduced)
- Cold rolled (70% reduced via hot rolling, 10% reduced via cold rolling)
- Aged (from hot rolled sample)
Grinding:
Each sample was grinded using 240, 320, 400, and 600 grit sandpaper. The sample was moved from course to fine grit and rinsed before moving to the next sandpaper. The mounted samples were rotated 90 degrees between each paper for an even grinding to ensure that no deep scratches would be left after the final grinding.
Polishing:
Following grinding the samples were polished on a wheel using a 6-micron diamond paste for 3 minutes. The sample was rotated 90 degrees at 30 second intervals, and diamond extender was added as needed. This exact process was followed a second time using 3-micron diamond paste. After this, a final polish was carried out using 0.5-micron colloidal silica solution.
Etching:
Samples were etched to reveal grains and other hidden structures within the samples. To do this, a two-part etch was applied to each sample. The etch (Papageorge two-step) contains an attack element to strip metal, and a stain element to create contrast for better imaging. All samples except for the as-cast samples were etched.
Microscopy:
A brightfield optical microscope was used to capture images of Team Condor's sample. The processed samples were imaged before and after the etching process. For each sample our team captured one 200x, two 500x, and two 1000x magnified images.
*Note images are given in the following order:
- As-cast center
- As-cast edge
- Homogenized edge
- Homogenized center
- Cold Rolled
- Aged
Testing Alloy Properties & Predictions


Due to the alloy’s makeup, it was numerically predicted that, after T6 processing, the sample would have a yield strength of 406.791-461.941 MPa, an elongation of 9-10.5%, and an electrical conductivity of 45.4-47.9% IACS. The samples processed using varying techniques were tested for yield strength, elongation, hardness, and electrical conductivity. Yield strength and elongation testing were conducted using standard ASTM E8M technique. Electrical conductivity was tested using an electrical conductivity meter (EC meter). Hardness was tested using a Wilson Rockwell Hardness Tester. After testing and data collection, the data was graphed and analyzed thus allowing for the most competitive sample to be chosen for the competition.
Following these steps creates a sample equivalent 2AC (labeled on attached graphs). This sample had mediocre conductivity compared to other samples, but the superior elongation and yield strength were why it was chosen for the competition. Based on the results of testing two tensile bars cut from the same sheet as the competition bar, the competition results were expected to be as follows:
- Yield Strength (MPa): 401.98
- % Elongation: 9.8
- Electrical Conductivity (%IACS): 33.3
Conclusion
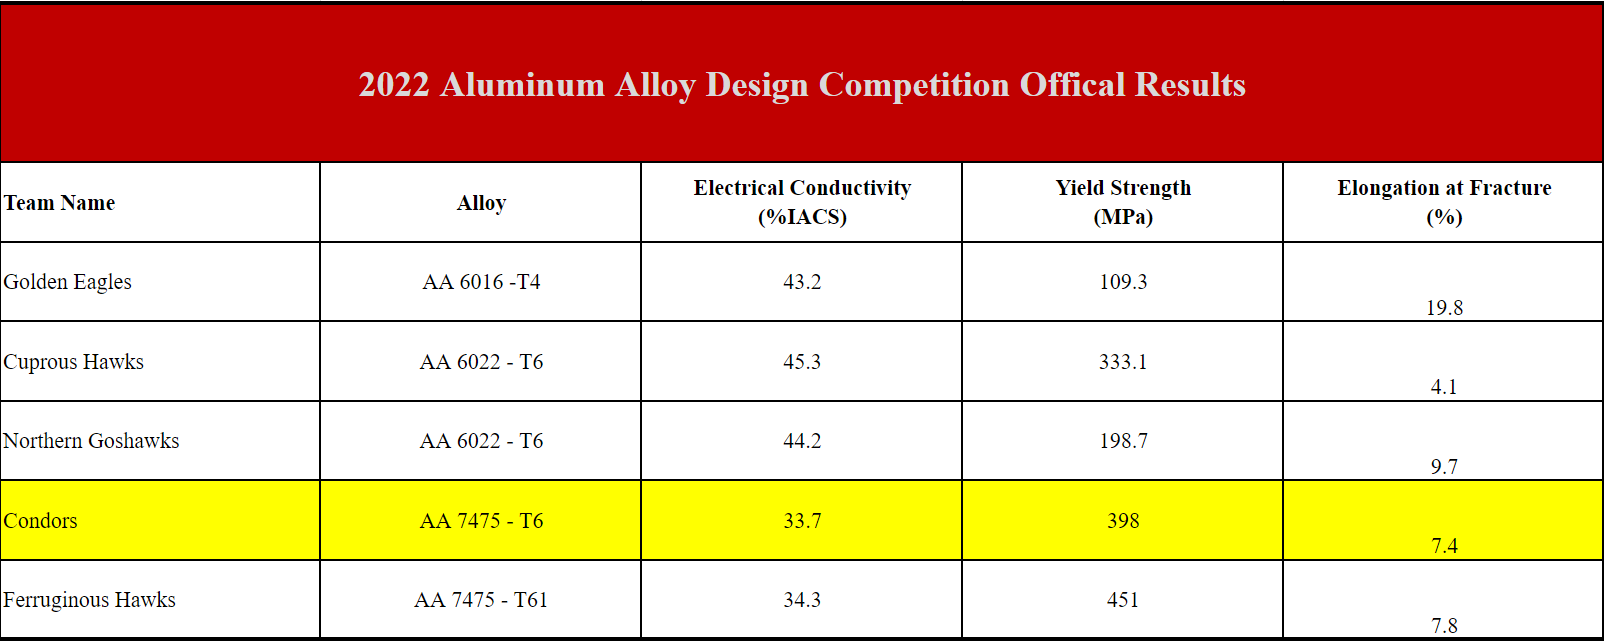
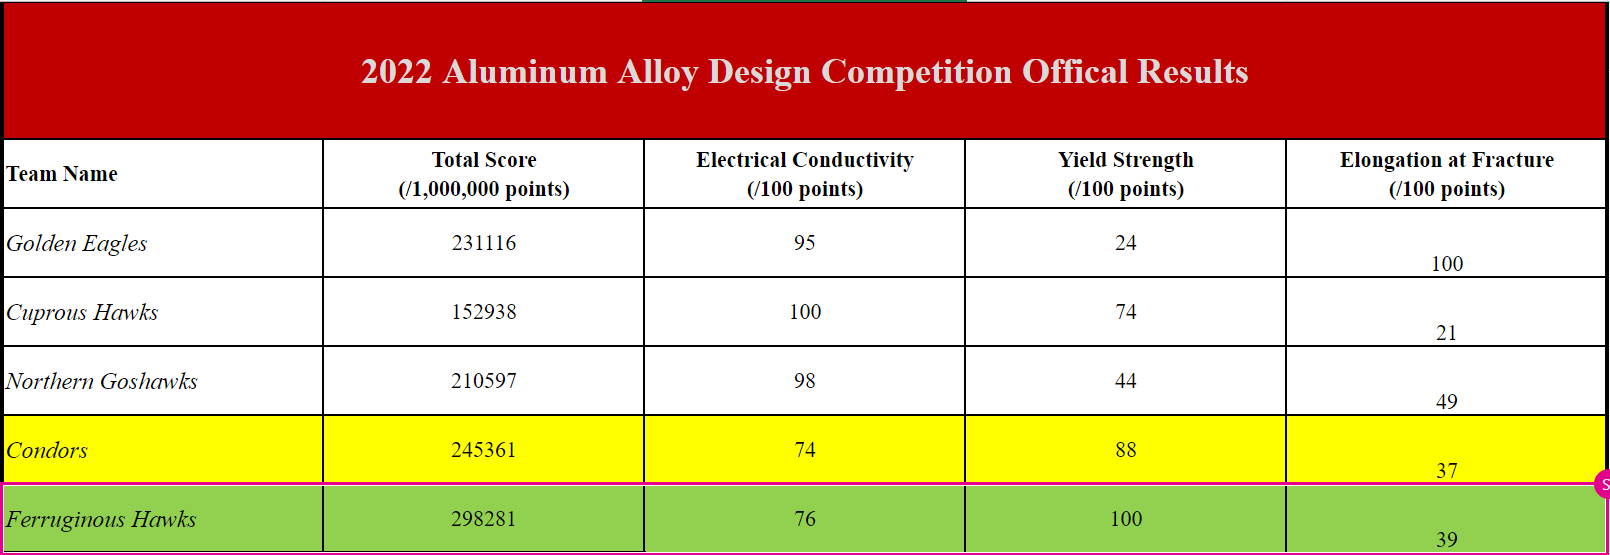
There you go! You have now created the 7475 alloy that Team Condor used to take home second place in the aluminum alloy competition! Enjoy the outstanding properties of the material that you have just crafted.
Throughout this process, Team Condor was able to demonstrate casting and various thermomechanical processing techniques. The microstructural changes in the alloy were examined to explore the impact of processing on overall yield strength, percent elongation, electrical conductivity, and physical grain structure.