Turn a Soda Can Into a PCB Solder Paste Stencil
by Saheen Palayi in Circuits > Soldering
794 Views, 8 Favorites, 0 Comments
Turn a Soda Can Into a PCB Solder Paste Stencil
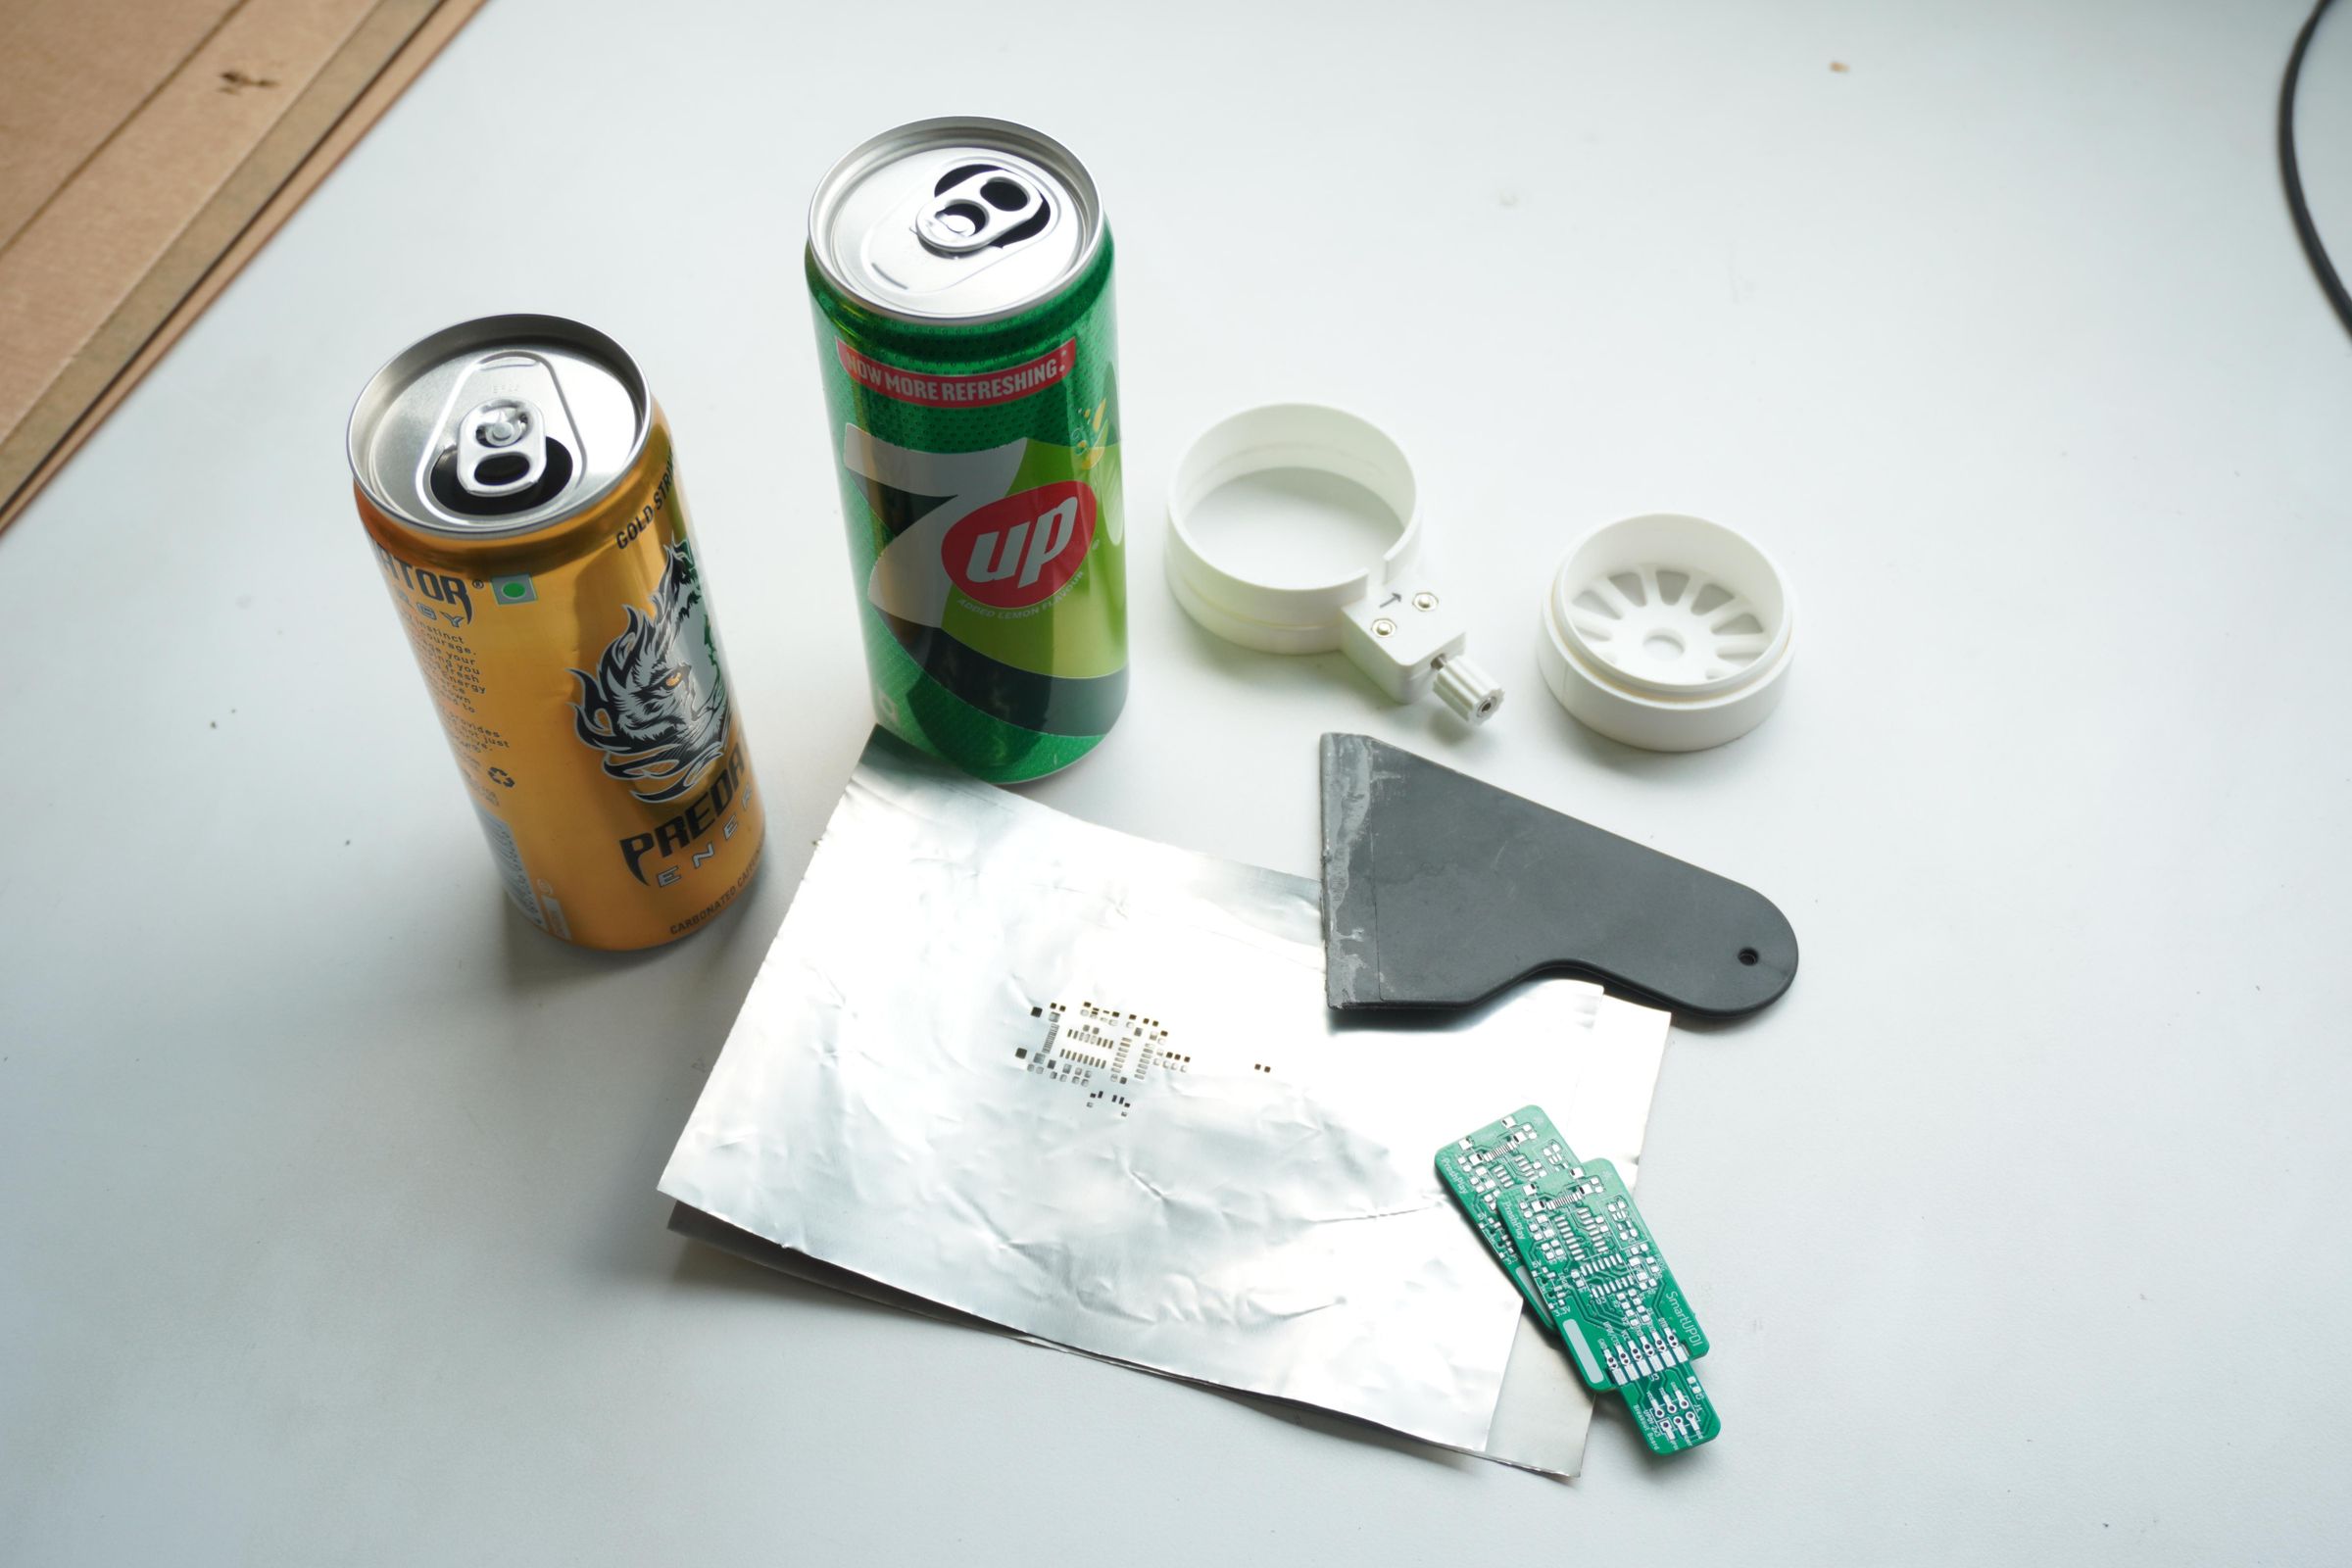
Every SMD board I make starts with the same question: how do I get solder paste onto those tiny pads neatly? A stainless steel stencil is the proper answer, but ordering one for every prototype costs money and takes days. At our fab lab we prototype boards all the time, so I wanted something we could make ourselves, on the spot. And the perfect material was sitting in the recycling bin: an empty soda can.
The aluminum in a can is thin, stiff and smooth, which is what a stencil needs. The hard part is getting a clean, flat sheet out of a curved can without sharp, crinkled edges. So I designed a 3D-printed cutting jig in Fusion 360. It's fully parametric: measure your can, change two values, and print a jig that fits it, whether that's a slim can or a regular one.
In this Instructable I'll show you how to:
- customize and print the can-cutting jig
- turn an empty can into a flat aluminum sheet
- laser-cut a solder paste stencil from it
- use it to paste and reflow a real PCB
Note: Cutting aluminum needs a fiber laser; a CO2 laser won't cut it. If you don't have one, check your local fab lab or makerspace.
One can, a little patience, and your trash becomes a tool for your next circuit board.
Supplies


Materials
- Empty soda can
- 3D-printed jig (PLA)
- 1 × M3 × 25 mm screw, for the knob
- 2 × M3 × 12 mm socket head screws, for the knife cover
- 3 × M3 nuts
- 9 mm snap-off utility knife blade
- Solder paste
- A blank PCB and its SMD components
- Masking or Kapton tape
- Baking paper or a Teflon sheet
Tools
- 3D printer (I used a Bambu Lab A1 Mini)
- Vernier caliper
- Hex key or screwdriver for the M3 screws
- Pliers, for snapping the blade
- Scissors
- Safety gloves
- Fine sandpaper
- Clothes iron or heat press
- Fiber laser (xTool F1 Ultra or similar)
- Squeegee or old credit card
- Tweezers
- Hot plate, hot air gun or reflow oven
- Fume extractor
Why a Jig? (and the Designs That Inspired It)


There are more than a dozen ways to cut an empty soda can and turn it into a sheet, and you can find most of them on YouTube or online. The simplest method is a utility knife and a pair of scissors. But I wanted a process that is easy enough for anyone to try without much effort or time.
There's also a safety concern: a soda can is made of thin aluminum, and its cut edges are sharp enough to cut your skin. A jig and a pair of safety gloves make the whole process safer and easier.
While searching for the perfect jig, I came across a few very useful and promising designs:
- Parametric Soda Can / Bottle Cutter by fmtuve
- Soda Can Edge Guard by sthone
- Soda Can Cutter write-up on The Neverending Projects List
I downloaded and printed them to test, and quickly realized that can sizes vary by brand and country (Red Bull, 7UP, Predator and so on). Luckily, the cutter was parametric, but it's written entirely in code, so I had to install OpenSCAD just to adjust the parameters.
After trying the jig, I also found that it lacked a good top support for cutting the second end of the can smoothly. The edge guard helps with this, but it's a separate design made only for standard 355 ml cans.
So I decided to design my own jig in Fusion 360: fully parametric, with the cutter and an improved top holder combined into one design. Just change the values in the parameter table, print it (a few hours), add a few screws and a utility knife blade, and you have a jig that fits your cans.
How the Jig Works


The jig has five 3D-printed parts:
- Base: a ring that holds the can upright. The can sits inside it and rotates freely while you cut.
- Knife holder: a block on the side of the base that holds a utility knife blade. The blade pokes through a slot in the ring wall into the can.
- Knife cover: clamps the blade in place so it doesn't slip while cutting.
- Knob: turns a screw that pushes the blade deeper, a little at a time. This lets you control the cut depth.
- Top support: fits into the open end of the can after the first cut. It holds the can steady and gives you a firm grip for cutting the second end, and it covers the sharp edge so it doesn't cut your hand.
How it's used:
- Place the can in the base, bottom end first.
- Tighten the knob slightly so the blade just touches the can.
- Rotate the can a full turn, tighten a bit more, and repeat until the end is cut off.
- Flip the can, fit the top support into the cut end, and cut the other end the same way.
- Slit the remaining tube lengthwise, and you have a flat-ish aluminum sheet.
The idea is to cut slowly and evenly instead of forcing the blade through, which keeps the edge clean and the sheet free of dents.
Make It Fit Your Can
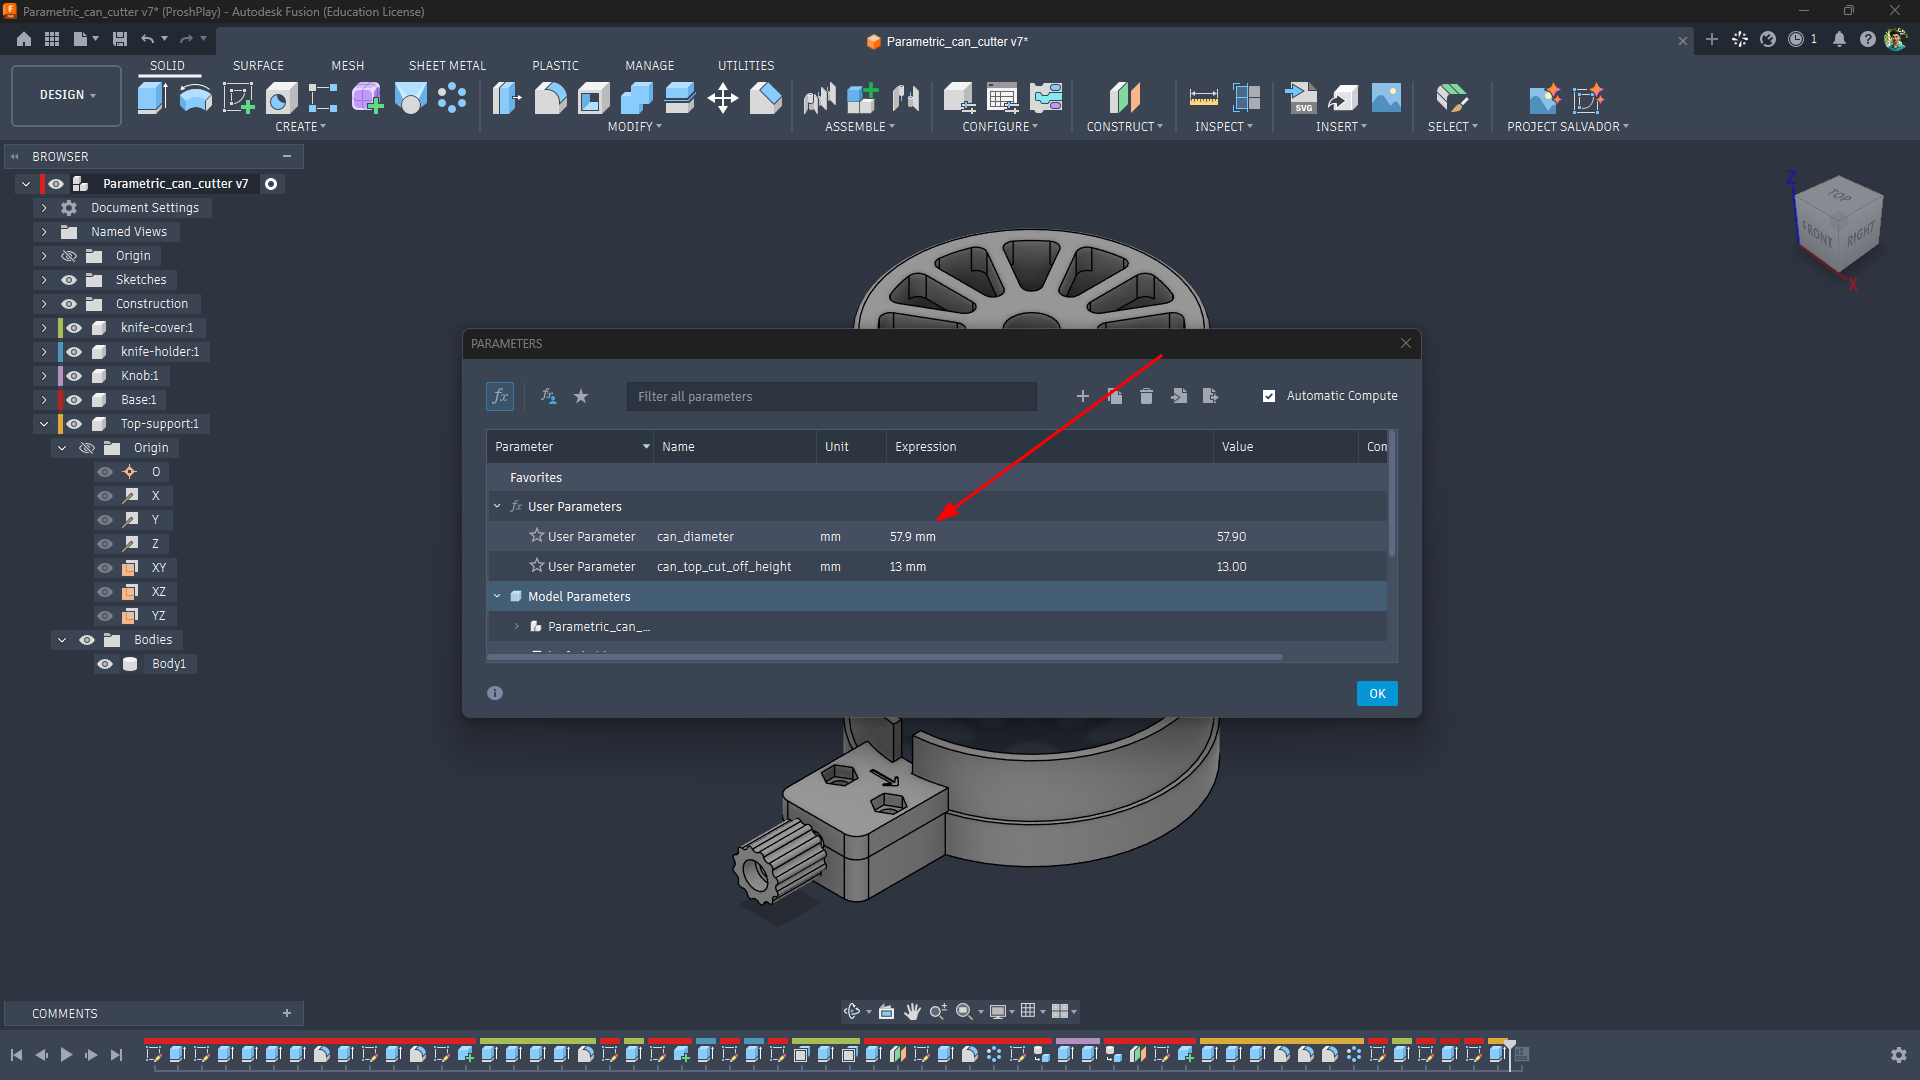


Cans come in different sizes depending on the brand and country, so I made this jig parametric. You only need to change two values, and the whole design updates to fit your can.
1. Measure your can.
Use a vernier caliper to measure:
- Diameter: across the straight body of the can, not the rim at the top or bottom.
- Top cut-off height: from the top rim down to where the straight wall begins, just below the tapered neck. Cutting here gives you a flat, even sheet.
2. Open the design in Fusion 360.
Download the attached .f3d file, open it, and go to Modify → Change Parameters.
3. Edit the two user parameters.
- can_diameter (default 57.9 mm): sets the size of the base ring and the top support.
- can_top_cut_off_height (default 13 mm): sets where the blade cuts off the top of the can.
Enter your measurements and click OK. All the parts update automatically.
4. Export for printing.
Right-click each body, choose Save as Mesh, and export it as an STL or 3MF. Or go to File → Export, choose 3MF, give it a name and save.
Downloads
Print the Jig


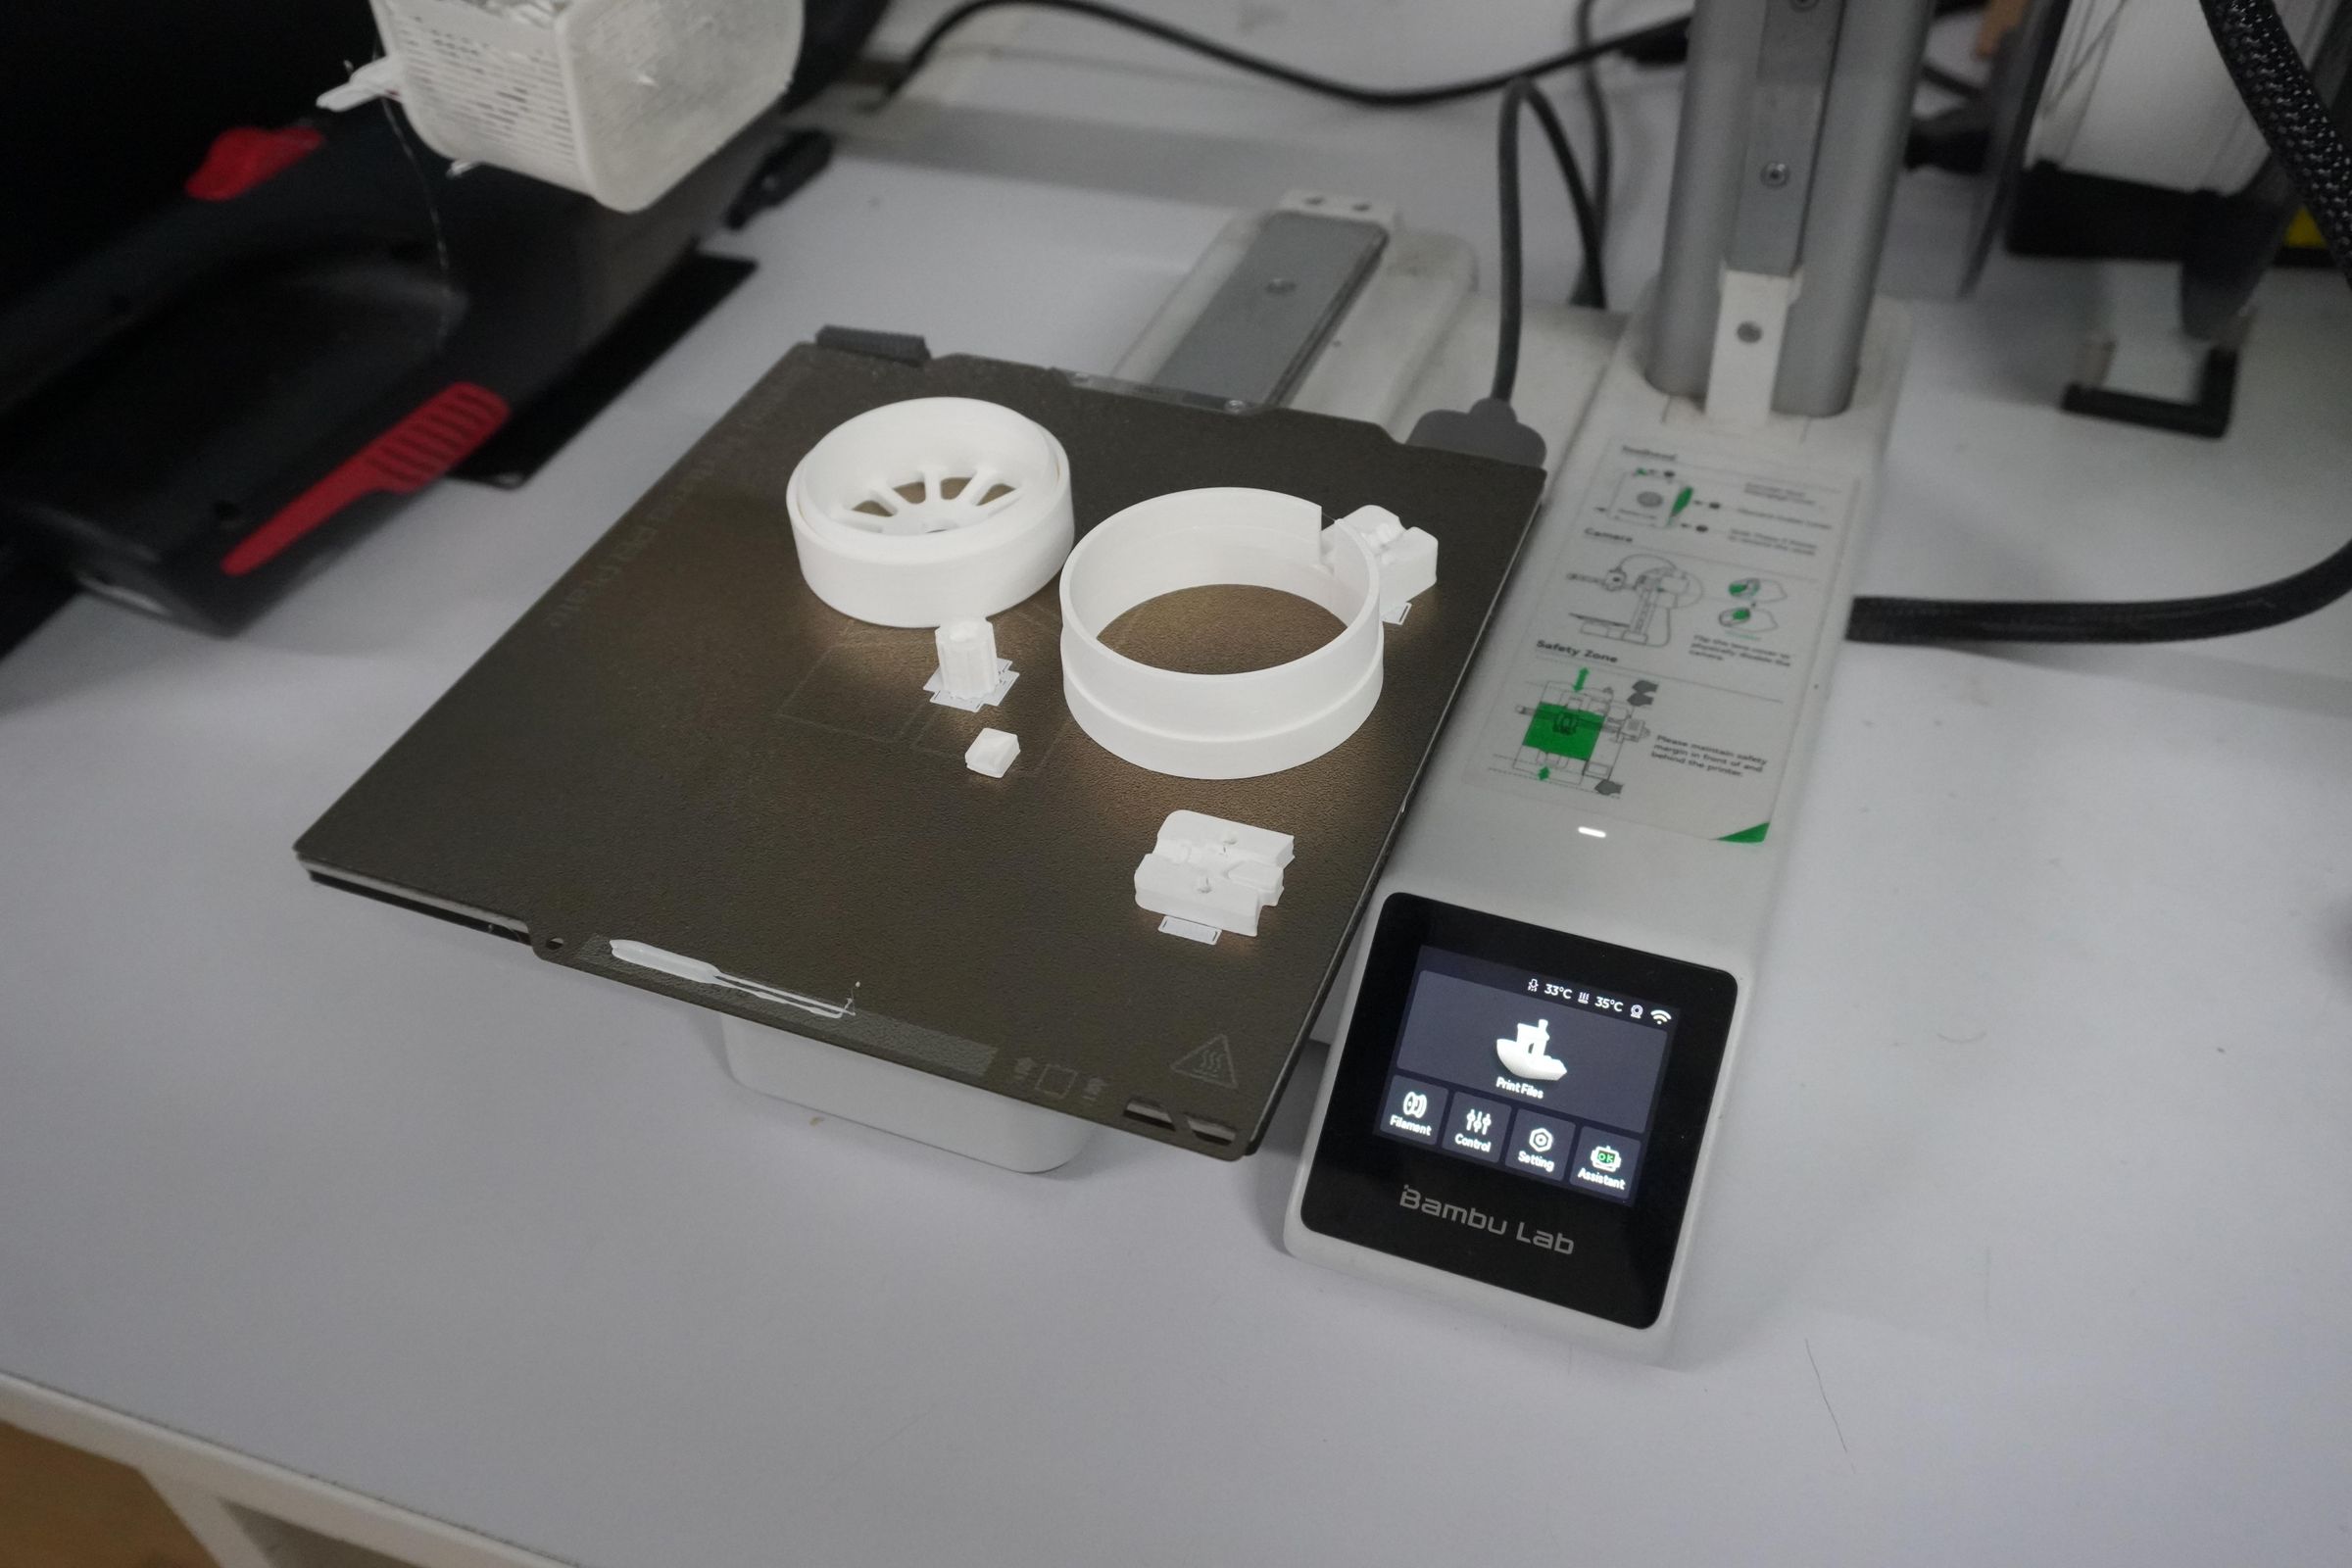

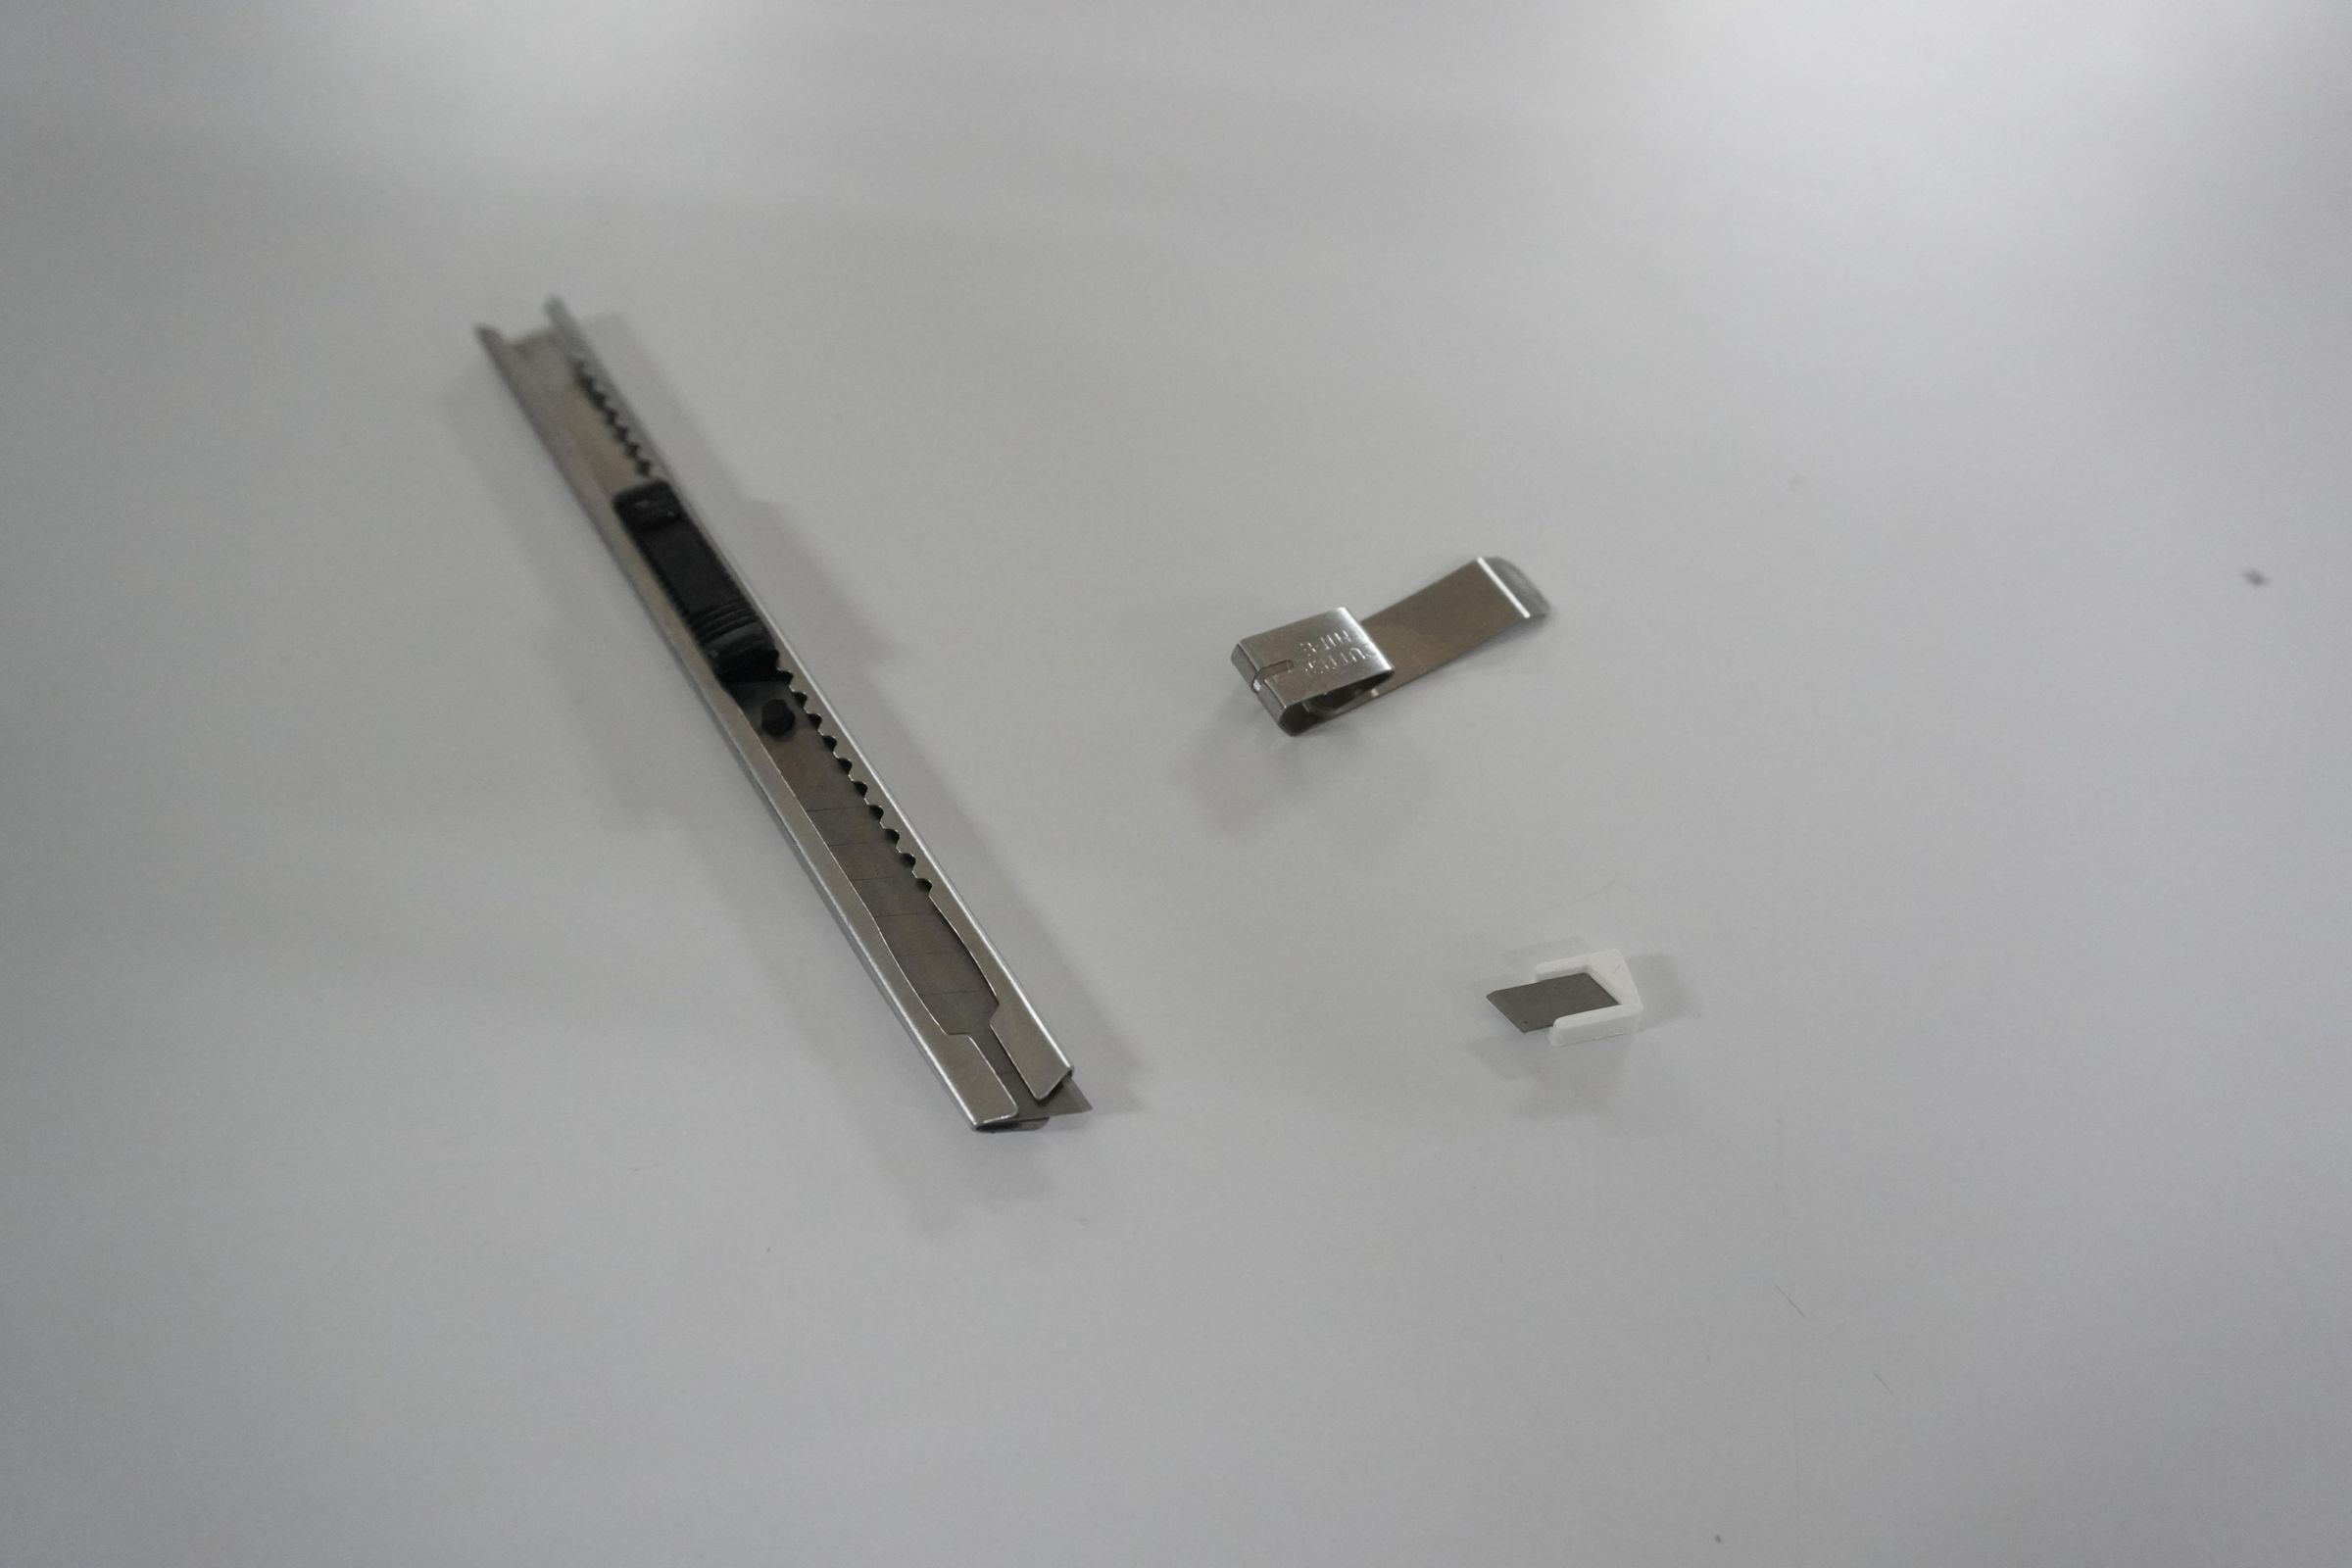
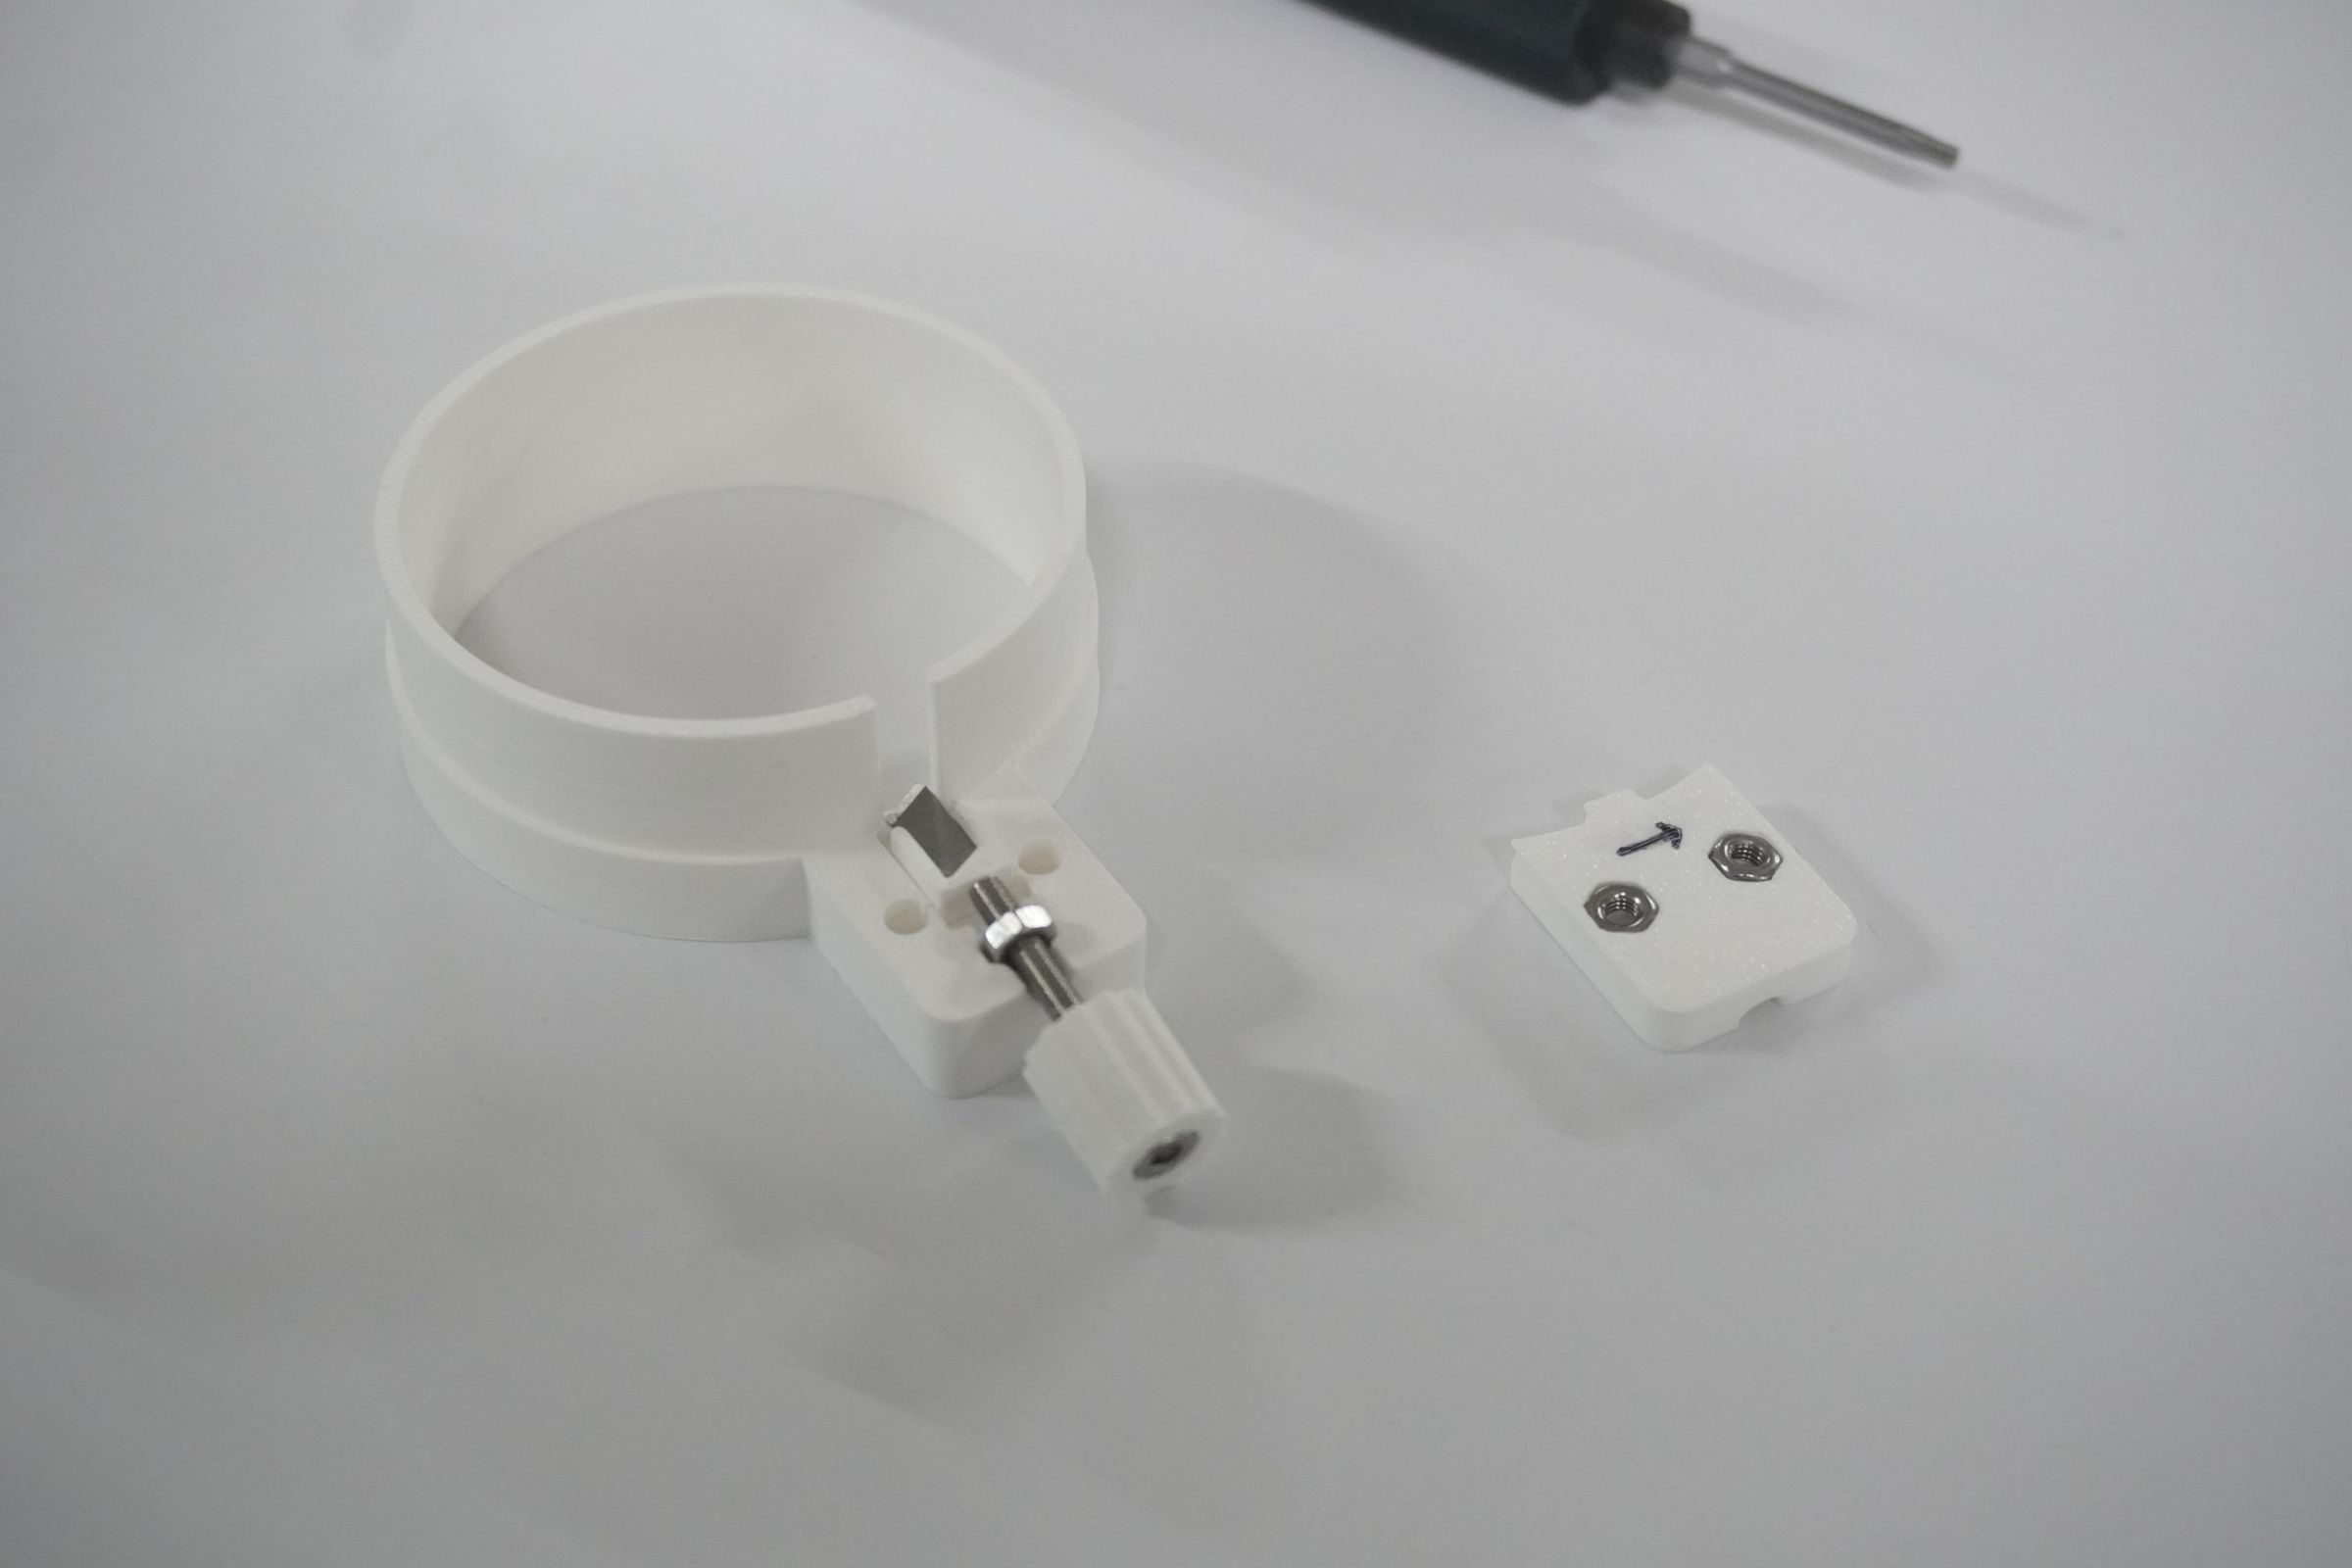
After setting the parameters for my can, I exported the parts as a 3MF file and printed them in PLA on my Bambu Lab A1 Mini.
Print settings:
- Layer height: 0.2 mm
- Infill: 20%
- Walls: 3 (use 4 for the knife holder so the blade stays rigid)
- Supports: on build plate only
- Print time: about 1 hour 11 minutes for the full set
Print each part flat side down, as shown in the picture.
Hardware you'll need:
- 1 × M3 × 25 mm screw and 1 × M3 nut, for the knob
- 2 × M3 × 12 mm screws and 2 × M3 nuts, for the knife cover
- 1 × 9 mm snap-off utility knife blade
Assembly:
- Remove the supports from the printed parts.
- Snap one segment off the utility knife blade. Use pliers for this; the blade can break unpredictably.
- Press the M3 nuts into their pockets.
- Screw the knob in.
- Slide the blade segment into the knife holder.
- Fit the knife cover and tighten its two screws.
Your jig is ready!
Prep the Can


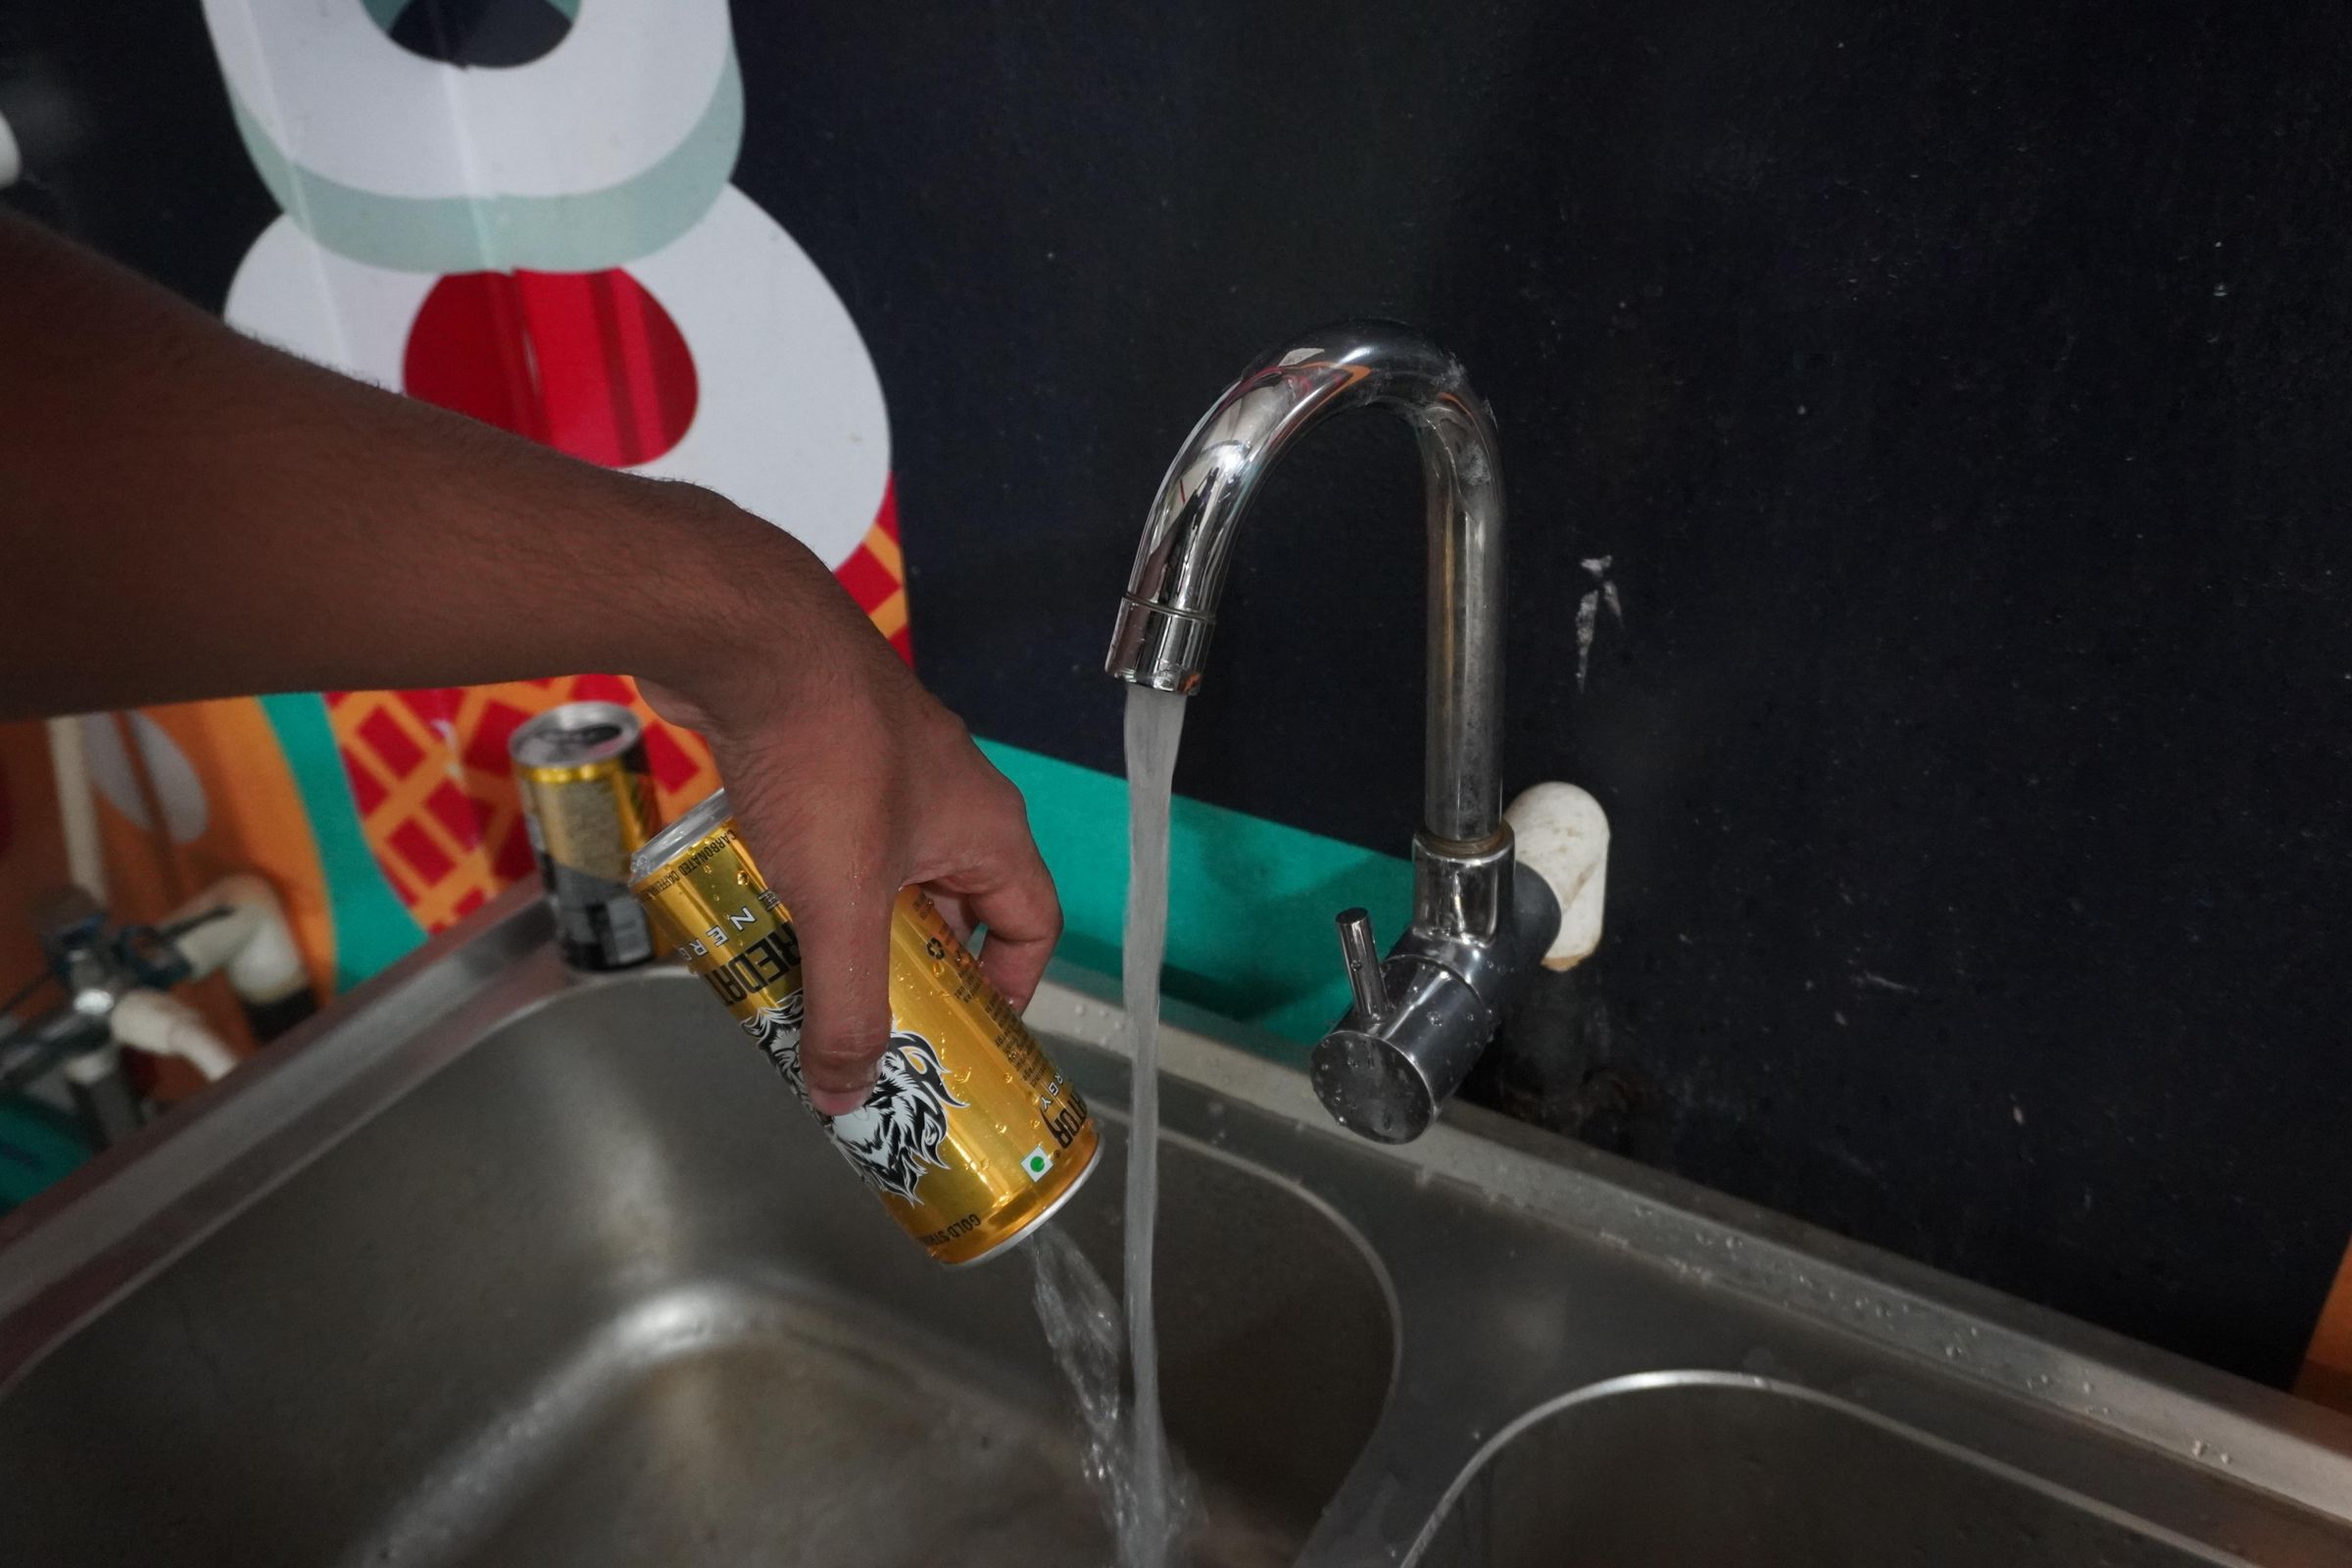
Take an empty can, rinse the inside well with water, and let it dry completely. Choose cans with no dents, or only very minor ones. Dents make the cut uneven and leave marks on the sheet.
Also check the pull tab (the opening lever) on top. It should lie flat against the lid, not stick up. If it's raised, it acts like a spring and gets in the way when you rotate the can in the jig later. You have two options:
- Snap it off by bending it back and forth a few times. Be careful of the sharp edges.
- Fold it back over the opening and press it down into the hole so it stays level with the lid.
Cut the Can With the Jig


Wear safety gloves for this step. The cut edges are very sharp.
First cut: bottom of the can
- Loosen the knob so the blade sits back inside the knife holder.
- Push the can into the base, bottom end first, until it sits flat.
- Turn the knob until the blade just touches the can wall.
- Hold the jig still with one hand and rotate the can one full turn with the other. The blade scores a line around the can; you can feel it while rotating.
- Tighten the knob a little and rotate again.
- Repeat until the blade cuts through and the bottom comes off.
Take it slow. Small depth changes with full rotations give a clean, straight cut. If you push the blade in too far at once, the can wrinkles or tears.
Second cut: top of the can
- Loosen the knob and pull out the can.
- Flip the jig upside down. This side sets the blade at the right height for cutting off the top.
- Fit the top support into the open, cut end of the can. It holds the can round and keeps your hand away from the sharp edge.
- Flip the can and put it back into the jig, top end first, with the top support facing up.
- Repeat the same process: touch, rotate, tighten a little, rotate, until the top comes off.
Open the tube
Remove the top support. You now have an open aluminum tube. Cut it straight down the side with scissors, following a straight line or letter edge in the can's printed design as a guide, to open it into a sheet.
Tip: Keep the offcuts and the top and bottom rings in a separate bin as you go. They're sharp and easy to forget on the bench.
Open and Flatten the Sheet


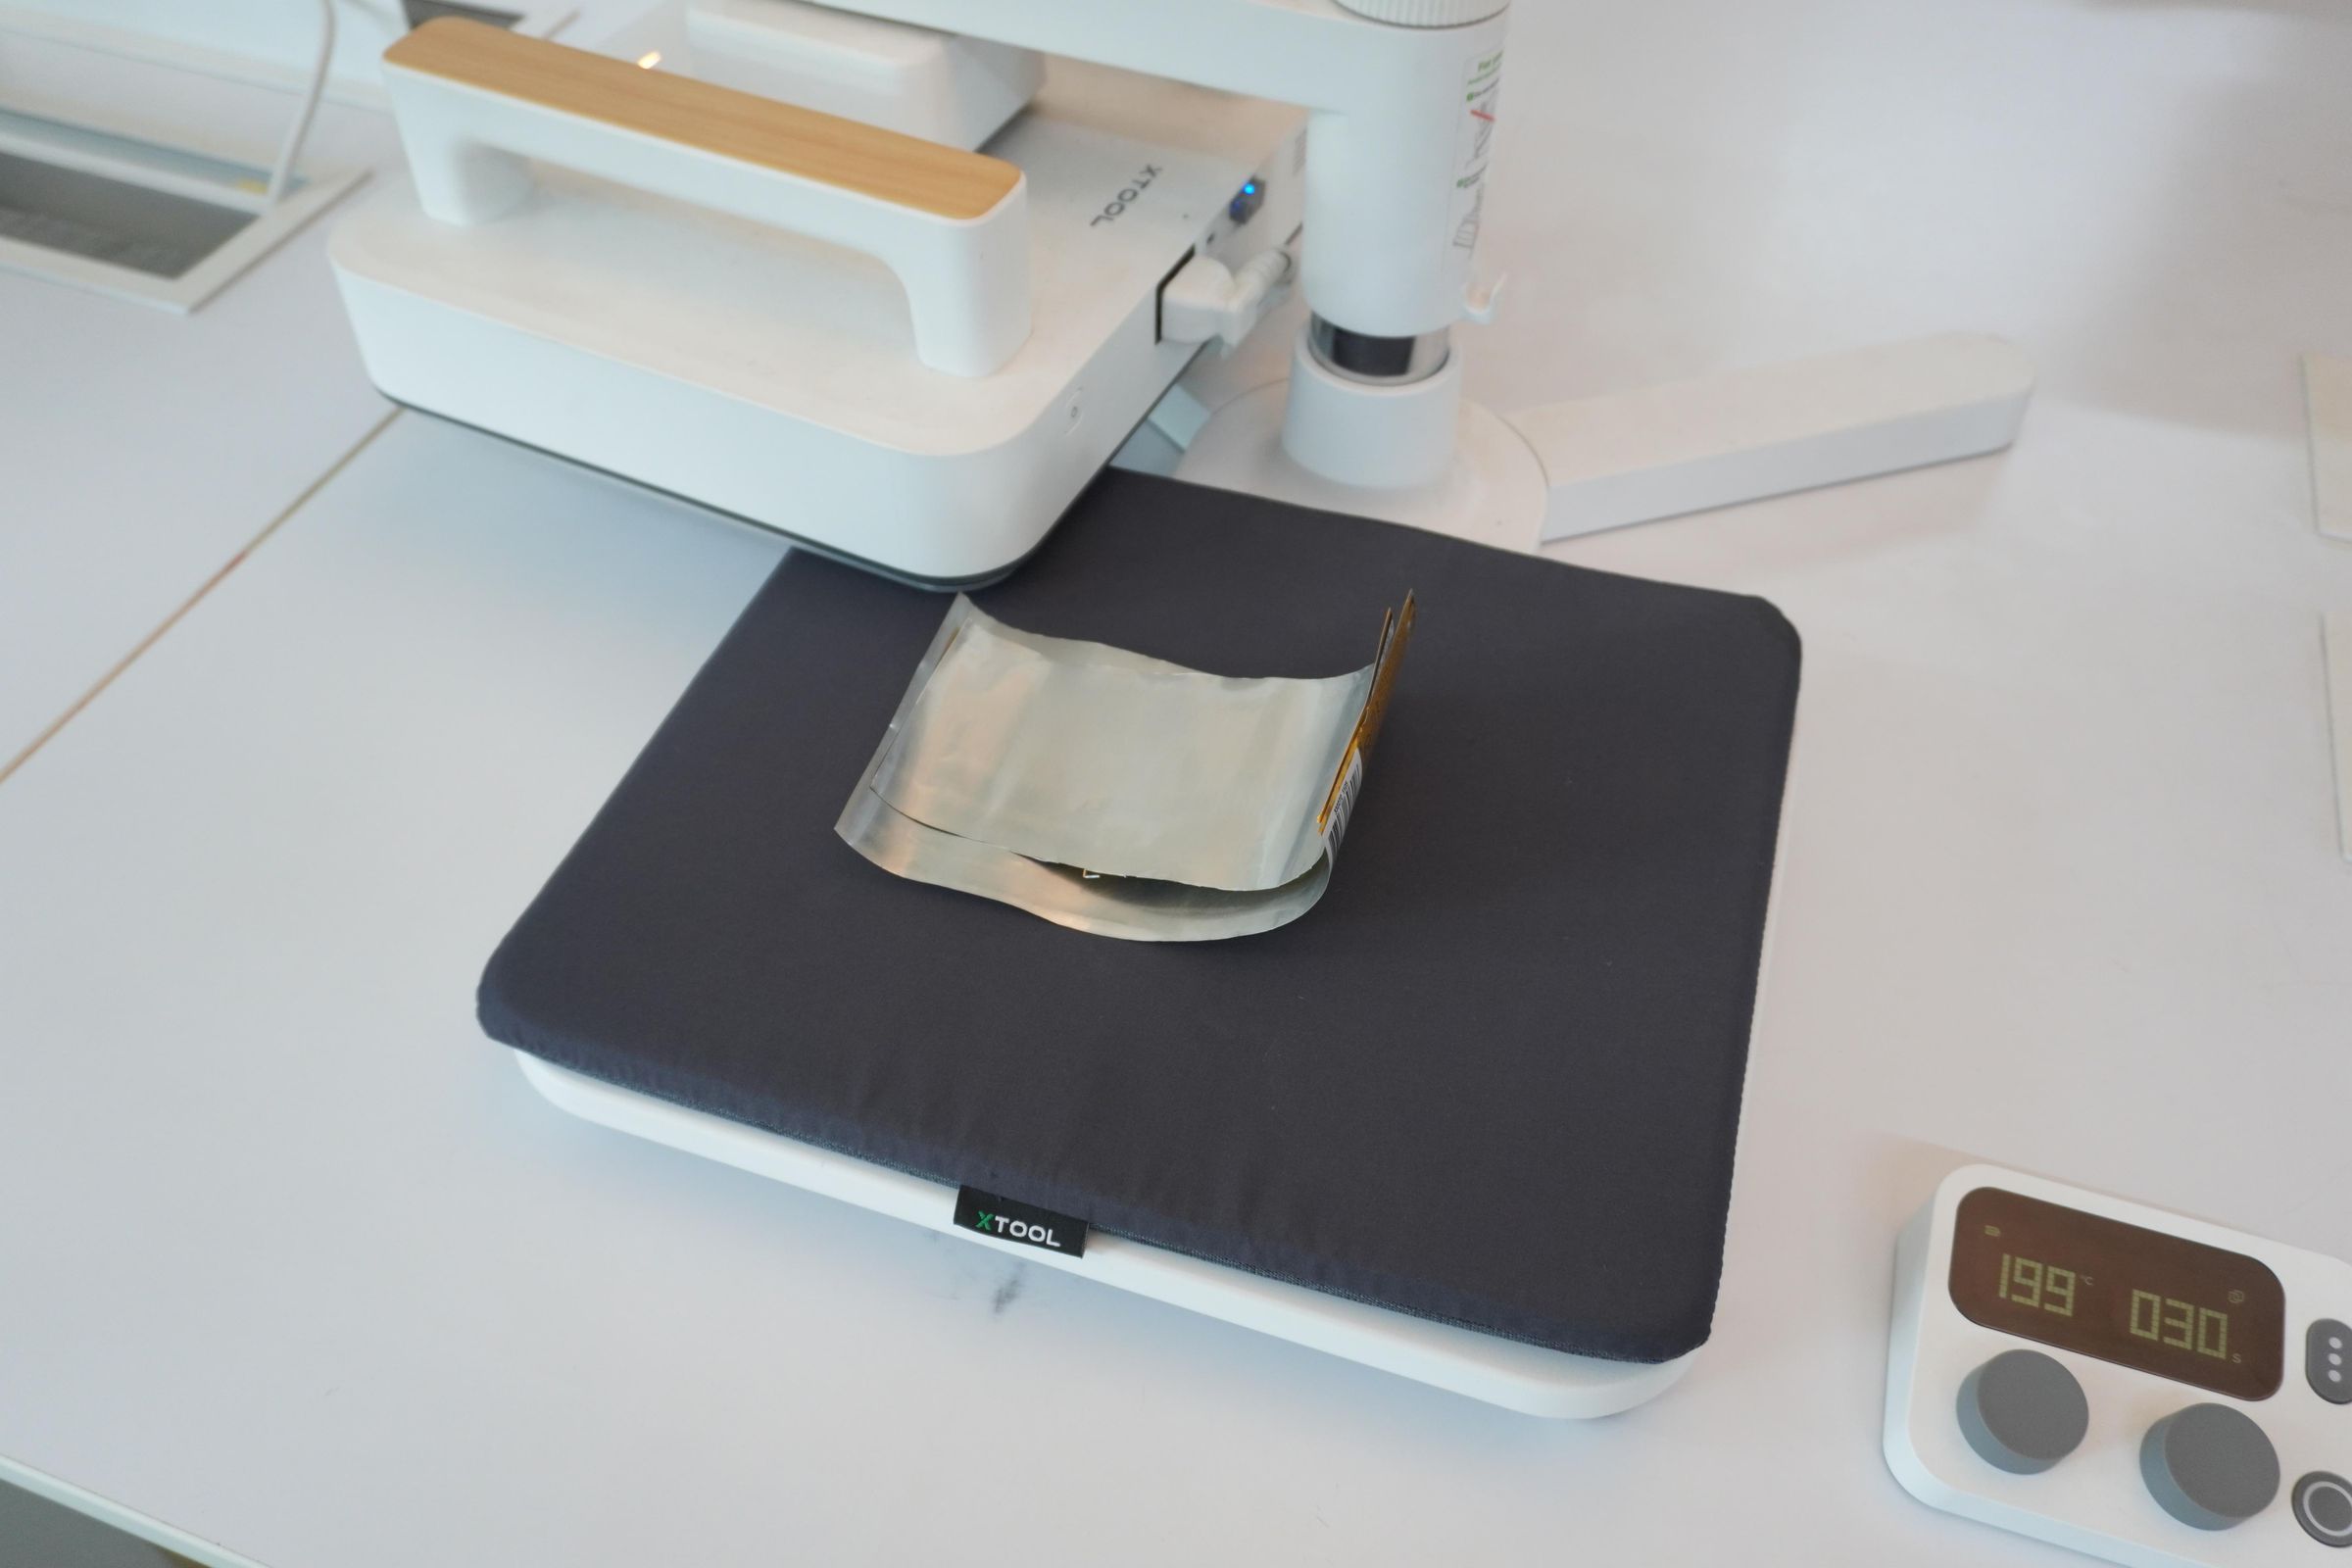


Step 7: Open and Flatten the Sheet
After opening the tube, you have a sheet of aluminum, but it's not really flat yet. It still wants to curl back into a can. There are a few ways to flatten it. Wear gloves for all of them, since the edges are sharp.
Desk edge: Hold the sheet by its edges and pull it over the edge of a desk, curl side facing up. This bends the curl the other way and relaxes it.
Heat and scrape: Warm the sheet with a hot air gun, then press and stretch it flat by sliding a plastic or acrylic ruler across the surface.
Iron and press (my recommendation): The easiest method I found is ironing the sheet with a small clothes iron. I also tried the xTool heat press, which is designed for transferring vinyl designs onto fabric, and it worked best for me. Heat the sheet, press it, and let it cool down under pressure. It stays flat once it cools.
It takes a little practice, but you'll get the hang of it quickly.
Tip: Put a sheet of baking paper or a Teflon sheet between the can and the iron or heat press. The can's paint can soften with heat and stick to the hot surface.
Make the Stencil File
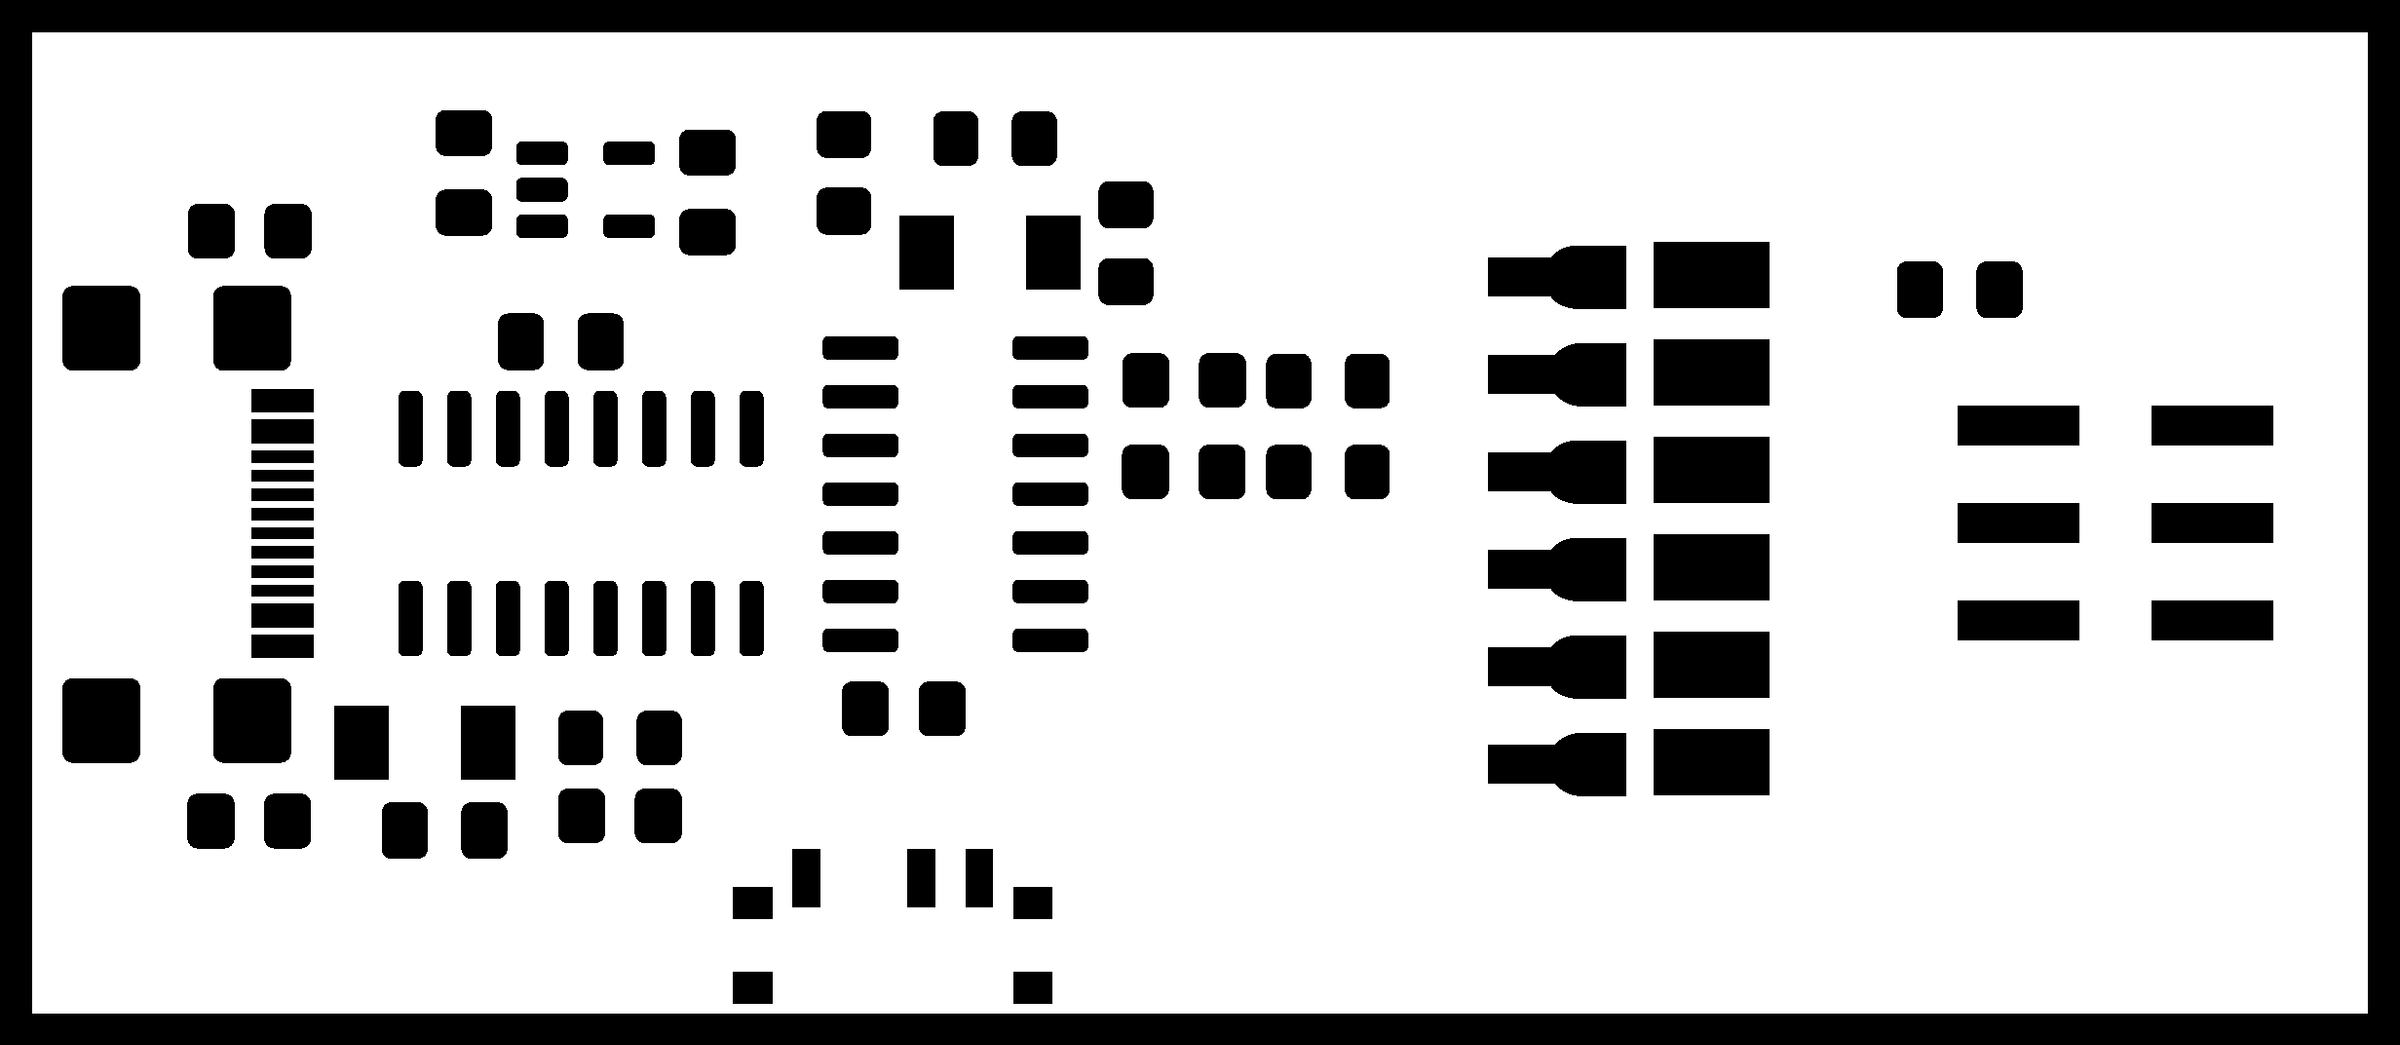


For this stencil, I used the Gerber files of one of my older PCB designs, since I had some blank (unassembled) boards left. You can use your own Gerber files.
Convert the Gerber to an image
- Open gerber2png in your browser and load your Gerber files.
- Turn off the traces, silkscreen, drill and outline layers, so only the pads are visible.
- Turn on the B/W invert option.
- Export the image as a PNG.
Trace it in xTool Studio
- Import the PNG into xTool Studio and click Trace. Let it auto-generate the outlines, then click Save.
- Delete the original image: open the Layers panel, right-click the image layer and delete it. Only the traced vector should remain.
- Select the compound vector and click Edit.
- Remove any pads you don't need paste on. I removed the pads for the header pins, since I'll solder those by hand later.
- Remove the board outline too; the stencil only needs the pad openings.
The file is now ready for cutting.
Laser-cut the Stencil


Set up the cut in xTool Studio
Select the compound vector. In the settings panel on the left, set:
- Operation: Cut
- Laser type: Fiber IR
- Power: 100%
- Speed: 600 mm/s
- Passes: 10
Prepare the machine
- Place a cutting plate on the F1 Ultra's bed, then lay the aluminum sheet on top. Don't skip the cutting plate, or the laser can damage the machine's base plate.
- Put small weights on the edges of the sheet. The heat of the laser makes the thin aluminum warp while cutting, so it needs to be held flat and secure.
- Connect the F1 Ultra and adjust the focus to the top surface of the aluminum sheet.
Position and cut
- Capture the camera preview in xTool Studio and place the design on the sheet.
- Run Framing to check that the design fits within the sheet and stays clear of the weights.
- Close the lid, send the file to the machine, and press Start on the F1 Ultra.
The cut took only about 10 seconds, which is very fast. You can see it in the video.
Safety: Cans have paint on the outside and a plastic lining inside, and the laser burns both off. Keep the lid closed and use the machine's fume extraction or good ventilation.
Clean Up
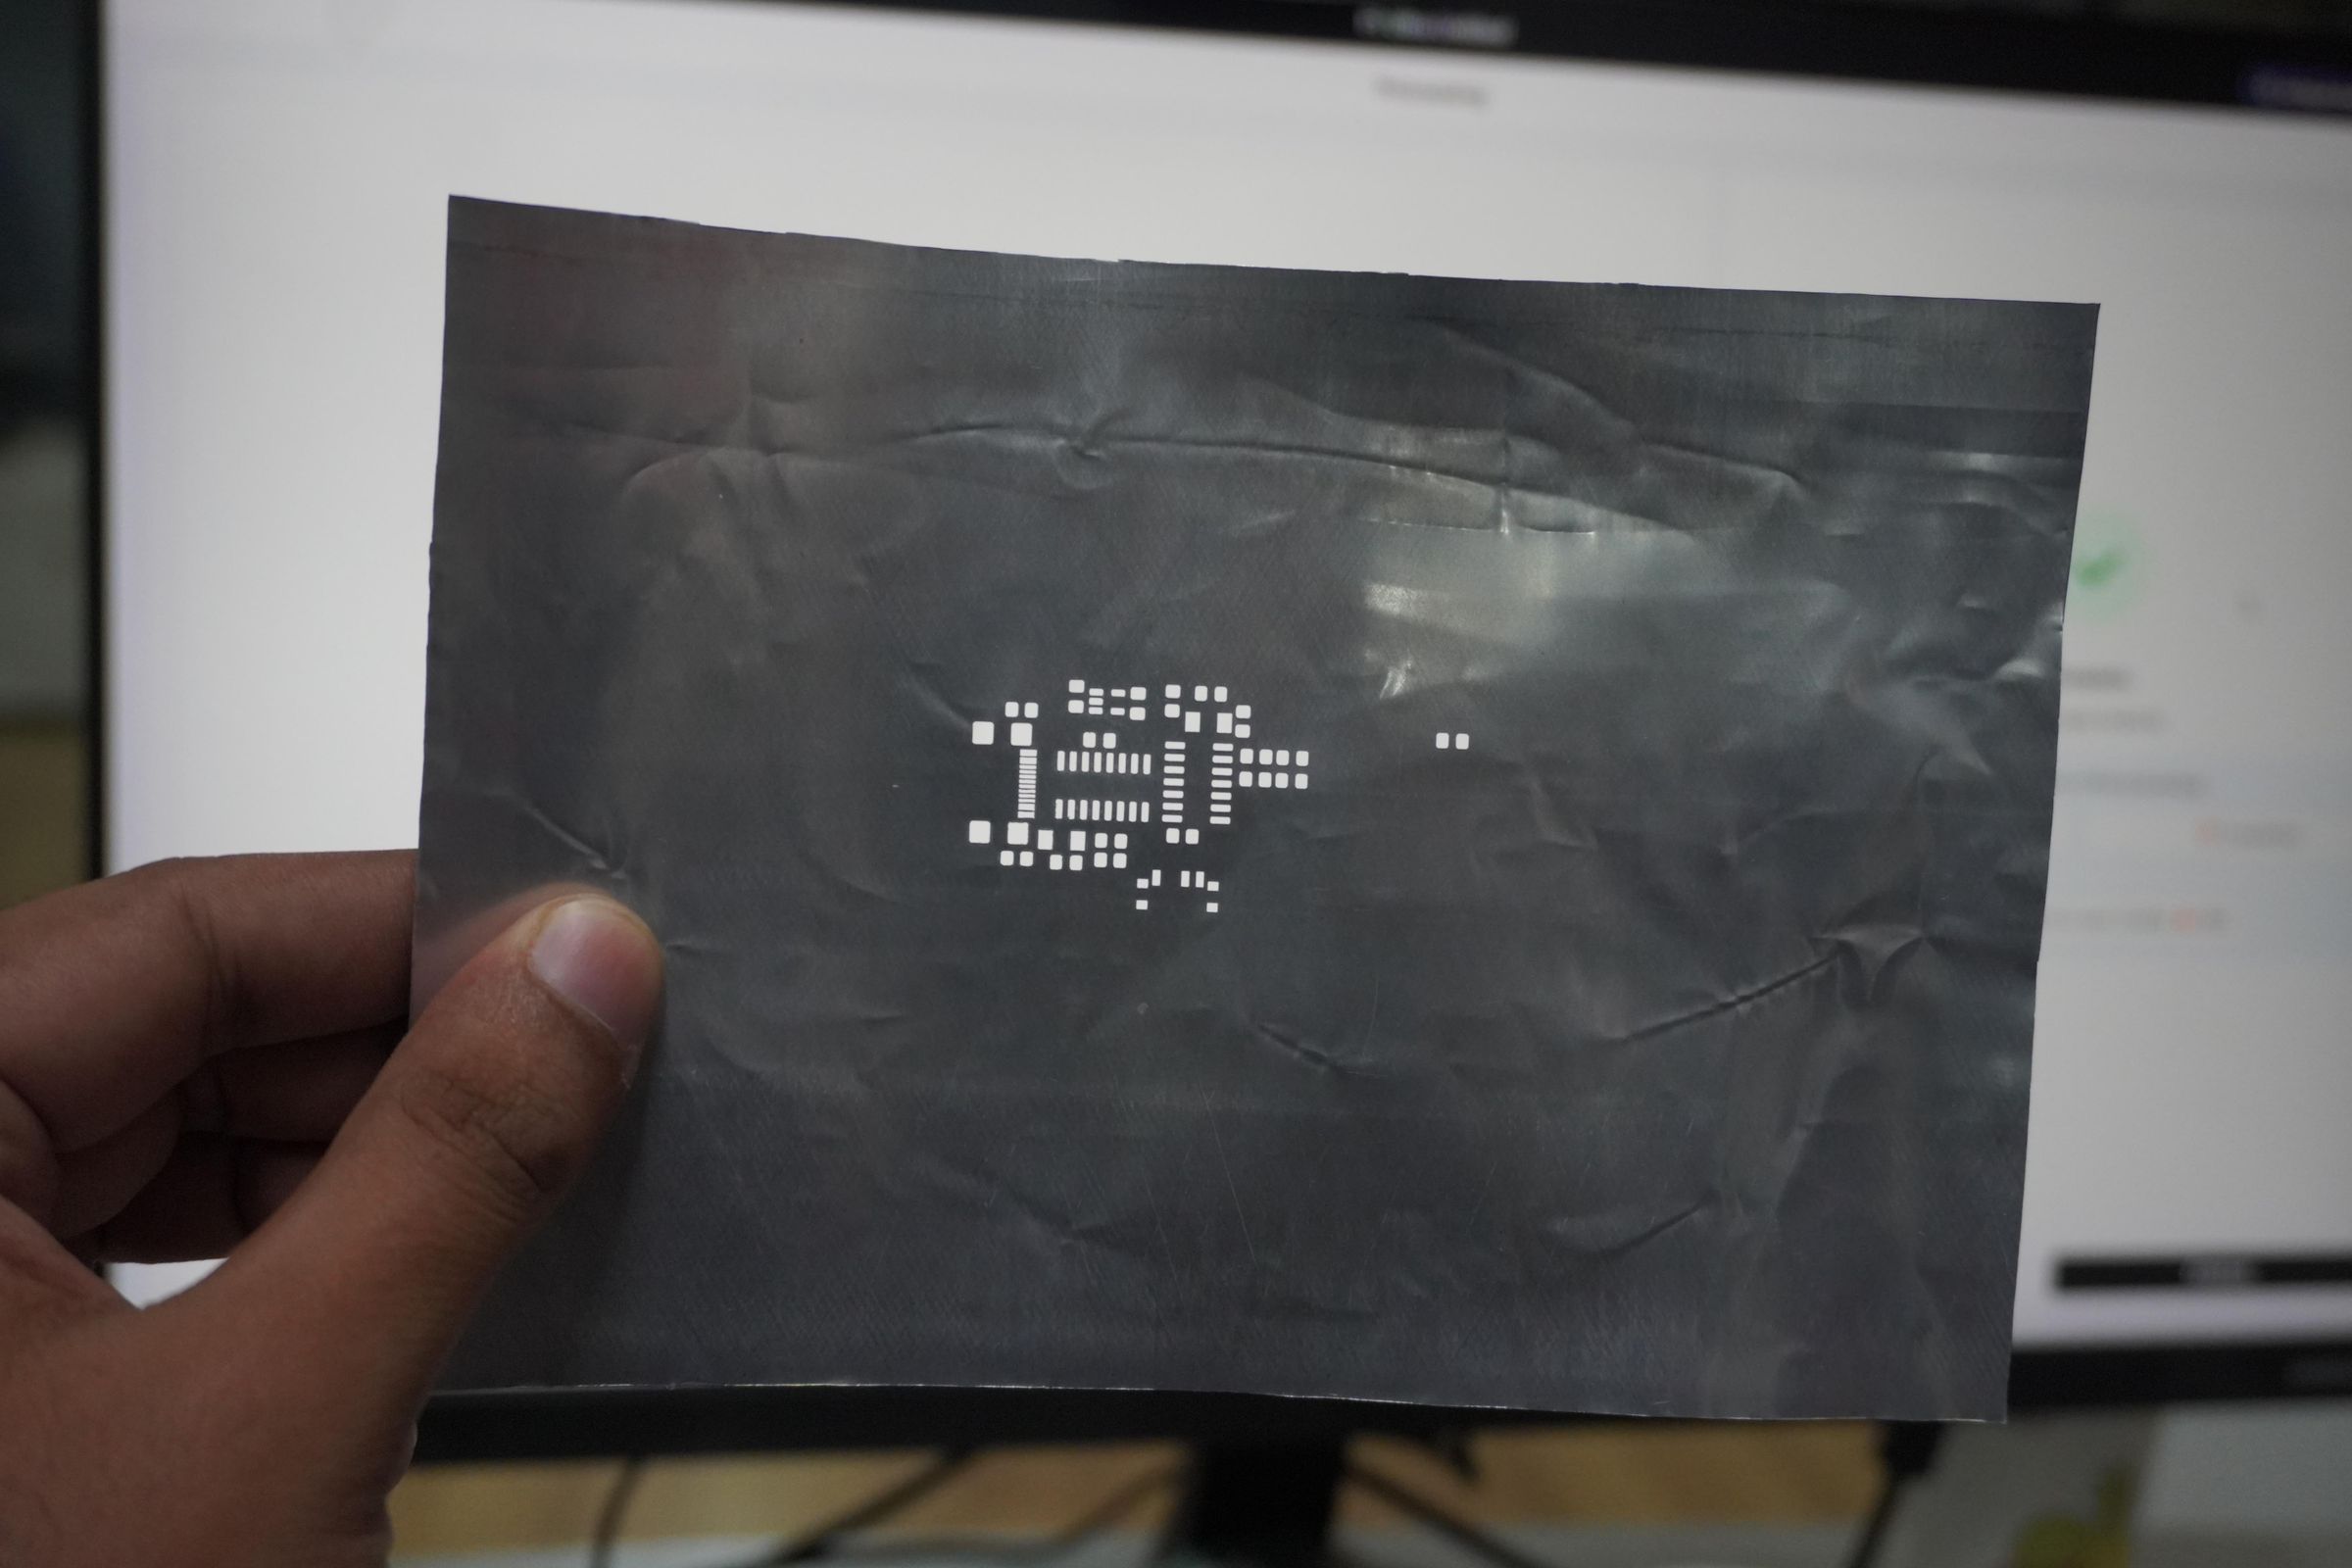


That was fast, and the results look great! A few pieces of debris may stay stuck in the pad openings. Push them out gently with fine tweezers or a needle, or blow them out with compressed air.
I didn't get any visible burrs around the cuts, so the power settings worked well. If you do see burrs, sand them lightly with fine sandpaper so the stencil sits flat on the PCB.
Don't forget to clean the xTool's bed after cutting too.
Apply Solder Paste


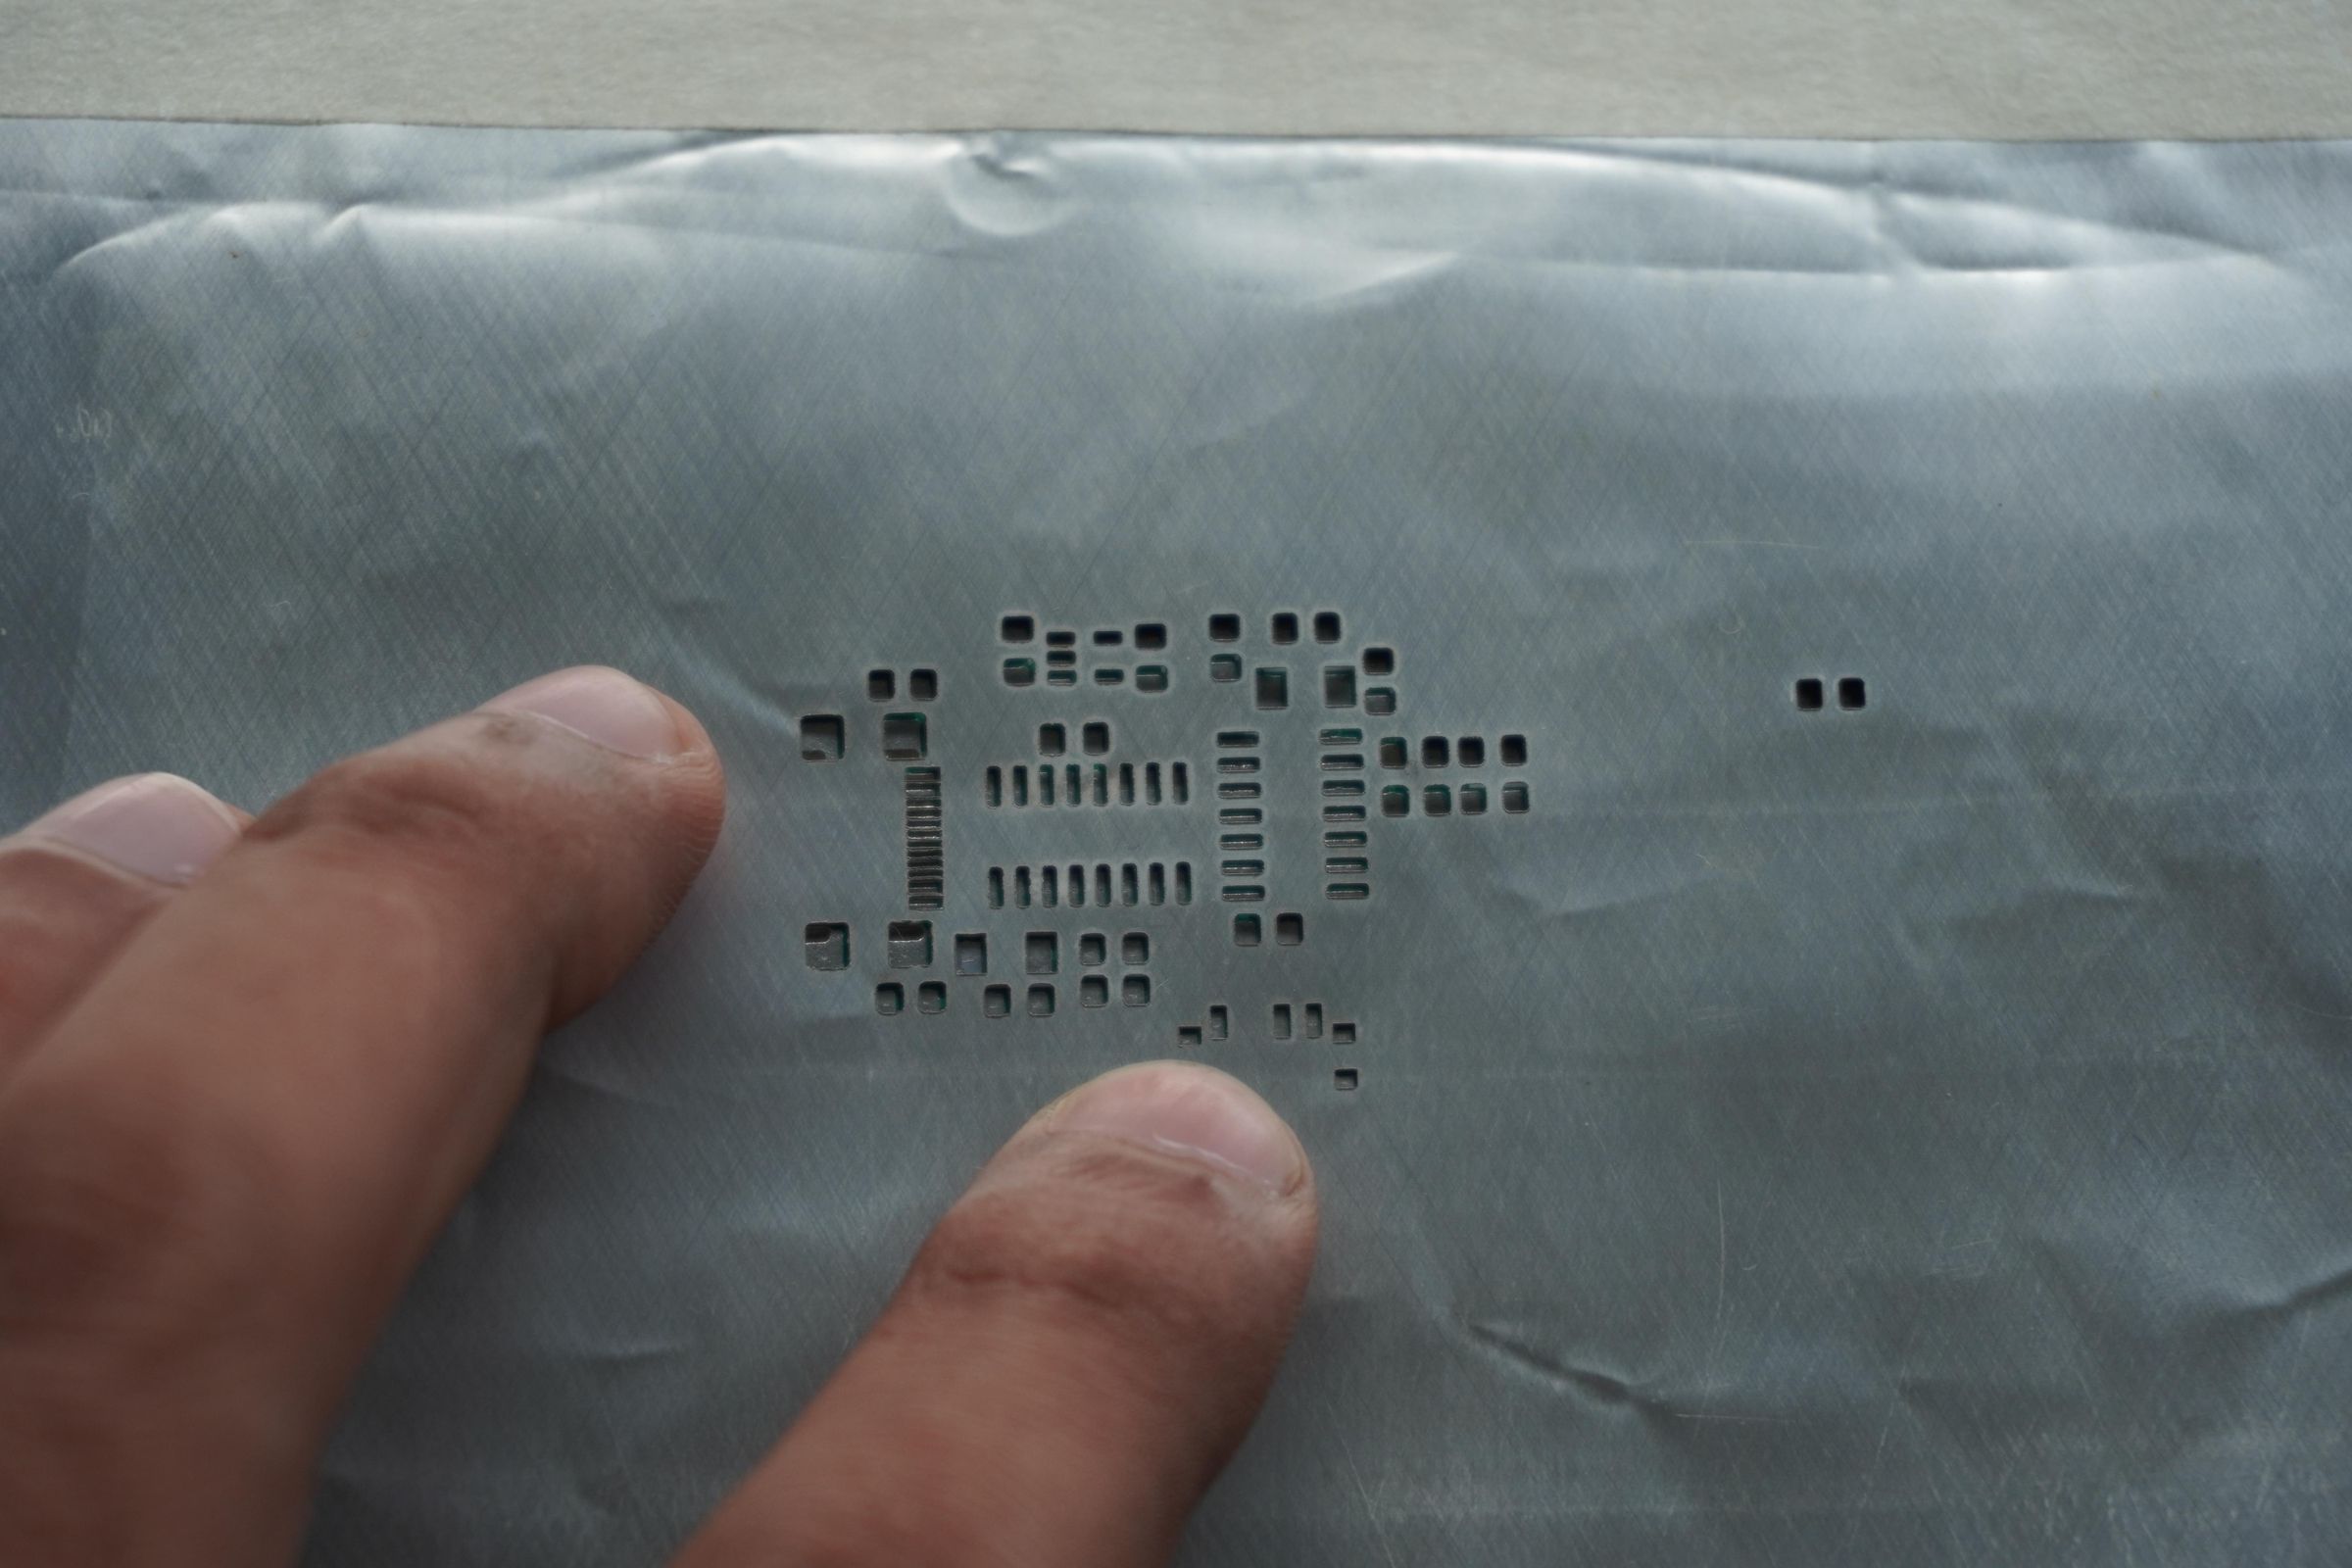
Make a simple PCB fixture
An easy way to hold the board is to use a few spare PCBs of the same thickness. Arrange them around your target PCB so it's trapped in the middle and can't move. This also gives the stencil a flat, level surface to rest on.
Align the stencil
Place the stencil on top and line up the openings with the pads carefully. Alignment is the most important part of this step, so take your time. Once it's aligned, fix the stencil in place with masking tape along the edges.
Apply the paste
- Put a small line of solder paste along one edge of the stencil, above the openings.
- Hold a squeegee (or an old credit card) at an angle and swipe it across the stencil in one smooth, firm pass. One pass fills the openings cleanly; going back and forth tends to push paste under the stencil and smear it.
- Lift the stencil straight up, carefully, so you don't smudge the paste.
Now the PCB is ready for component placement.
Safety: Solder paste often contains lead. Wear gloves if you can, and always wash your hands before and after handling it.
Place and Reflow

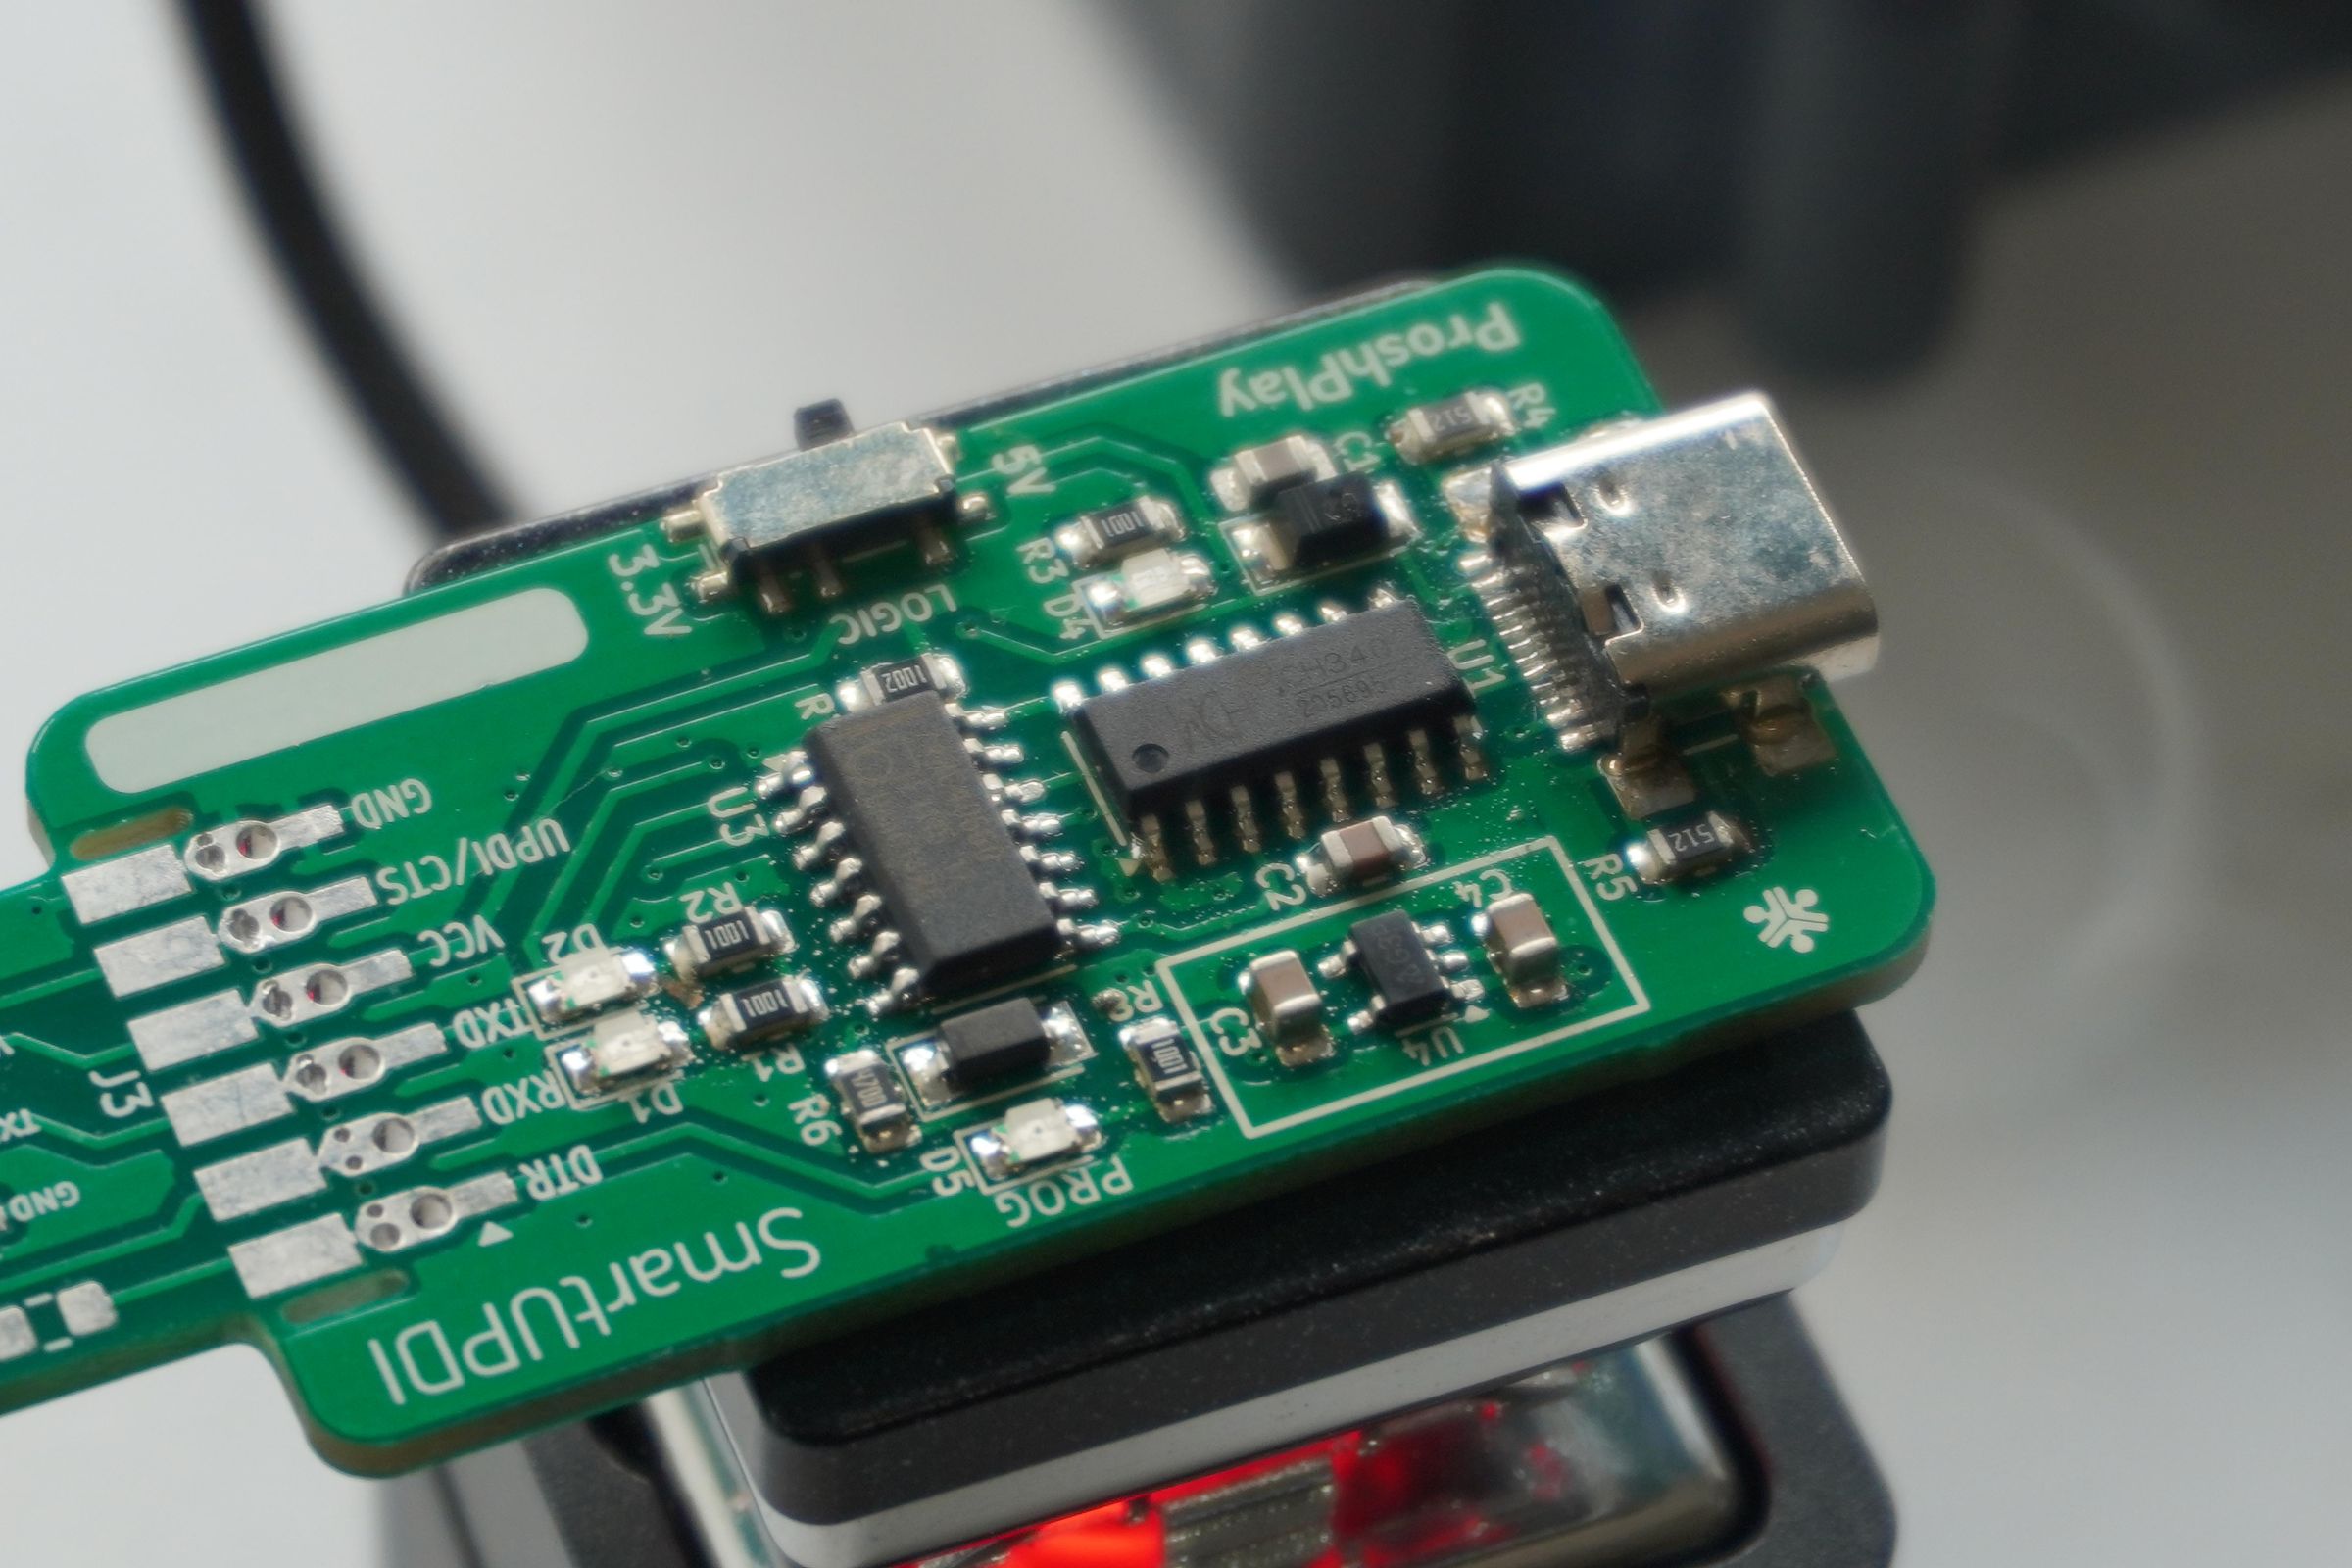


Place the components
Place all the components on the pasted pads by hand, using tweezers. Don't worry if they're slightly off. When the solder melts, surface tension pulls each part into line with its pads.
Reflow
Now it's time to cook! I used a hot plate, which is more than enough for small boards like this, with a fume extractor fan next to it. Heat to about 280°C, following the temperature on your solder paste's datasheet.
You can also use a hot air gun, heating the board slowly and evenly, or a reflow oven if you have one.
Watching the paste melt and the components snap into place on their own is very satisfying.
Results, Limits and Tips
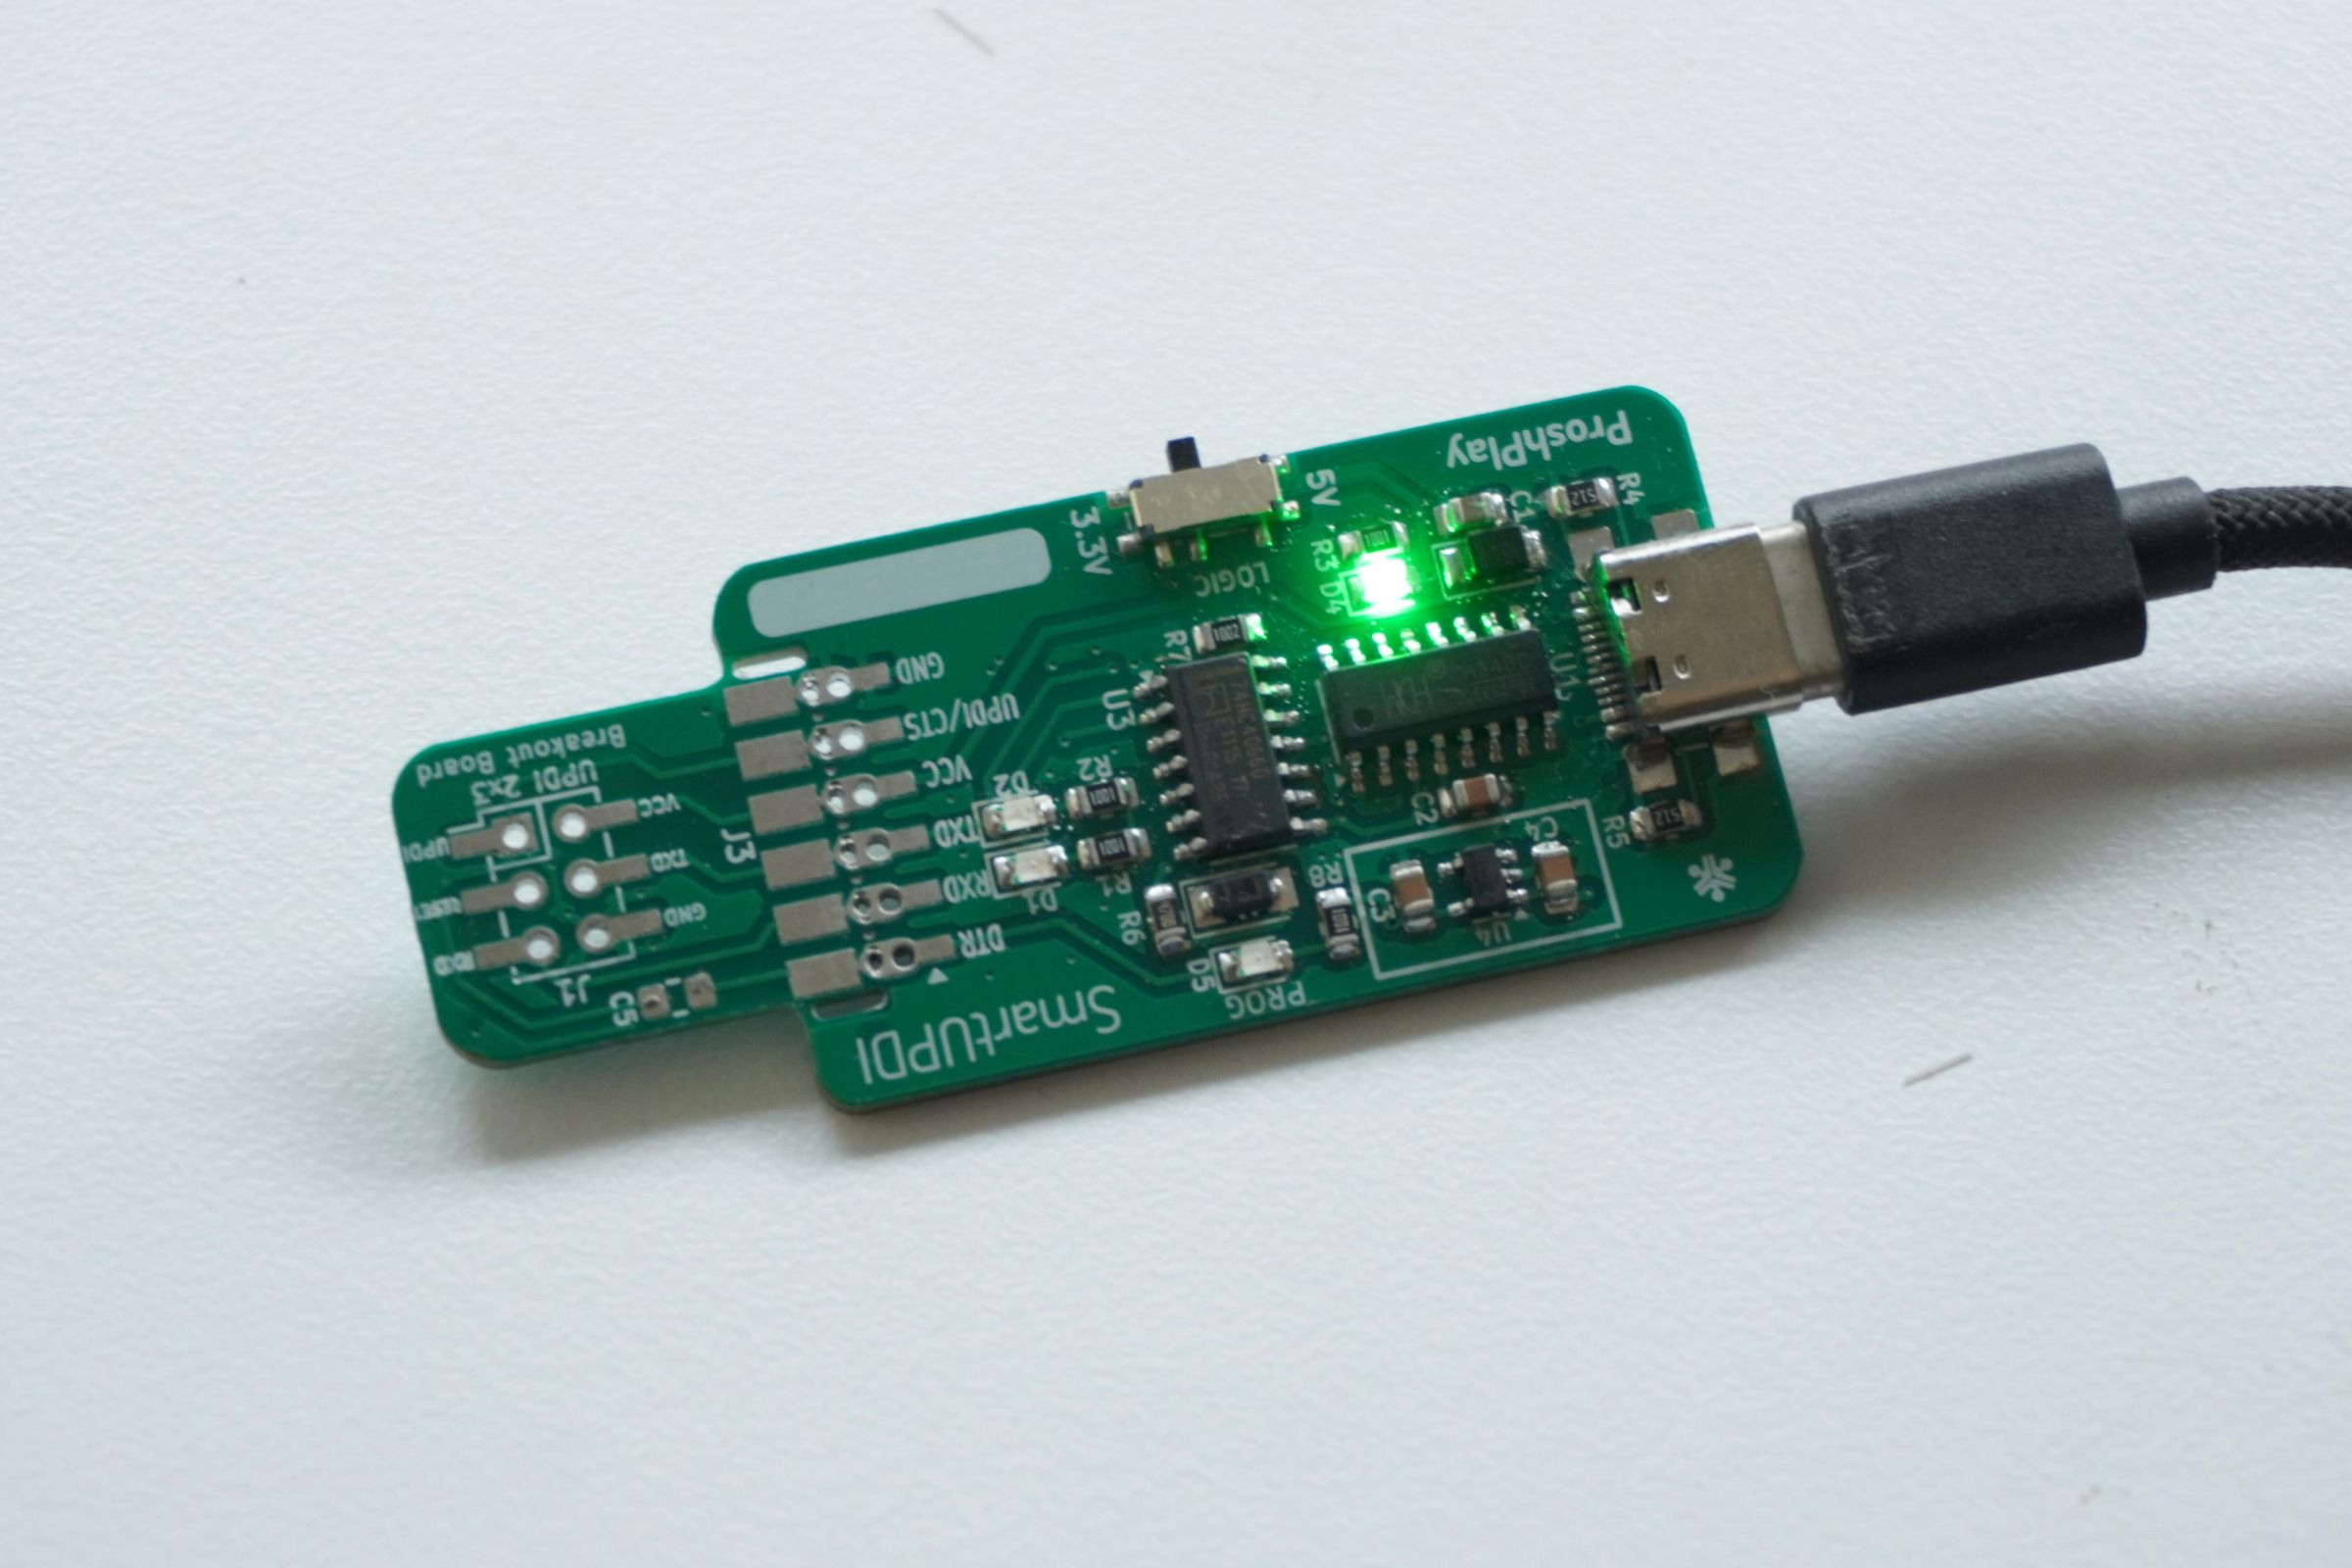


Results
The results are very promising for any maker who wants to do small-batch PCB production in a home lab or makerspace. A stencil costs almost nothing: just an empty can. You do need a fiber laser, but these are becoming more and more common in makerspaces and among hobbyists.
With the jig, turning a can into a sheet is easy, and once you get the hang of it, the whole process takes about 10 to 20 minutes, from can to stencil.
Limits
The main limit is how small the openings can go. The smallest package I've tried is LGA-14. The results were usable, though not perfect. Still, the stencil handles most of the packages I use for prototyping, and even the 16-pin USB Type-C connector came out really well.
Tips
- Take your time flattening the sheet. A flat sheet gives much cleaner cuts.
- Weigh the sheet down well on the laser bed; it warps from the heat while cutting.
- For very fine-pitch parts, lightly sand the sheet before cutting and experiment with the laser settings.
- Always align the stencil carefully before applying paste. Most problems come from alignment, not the stencil.